Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM


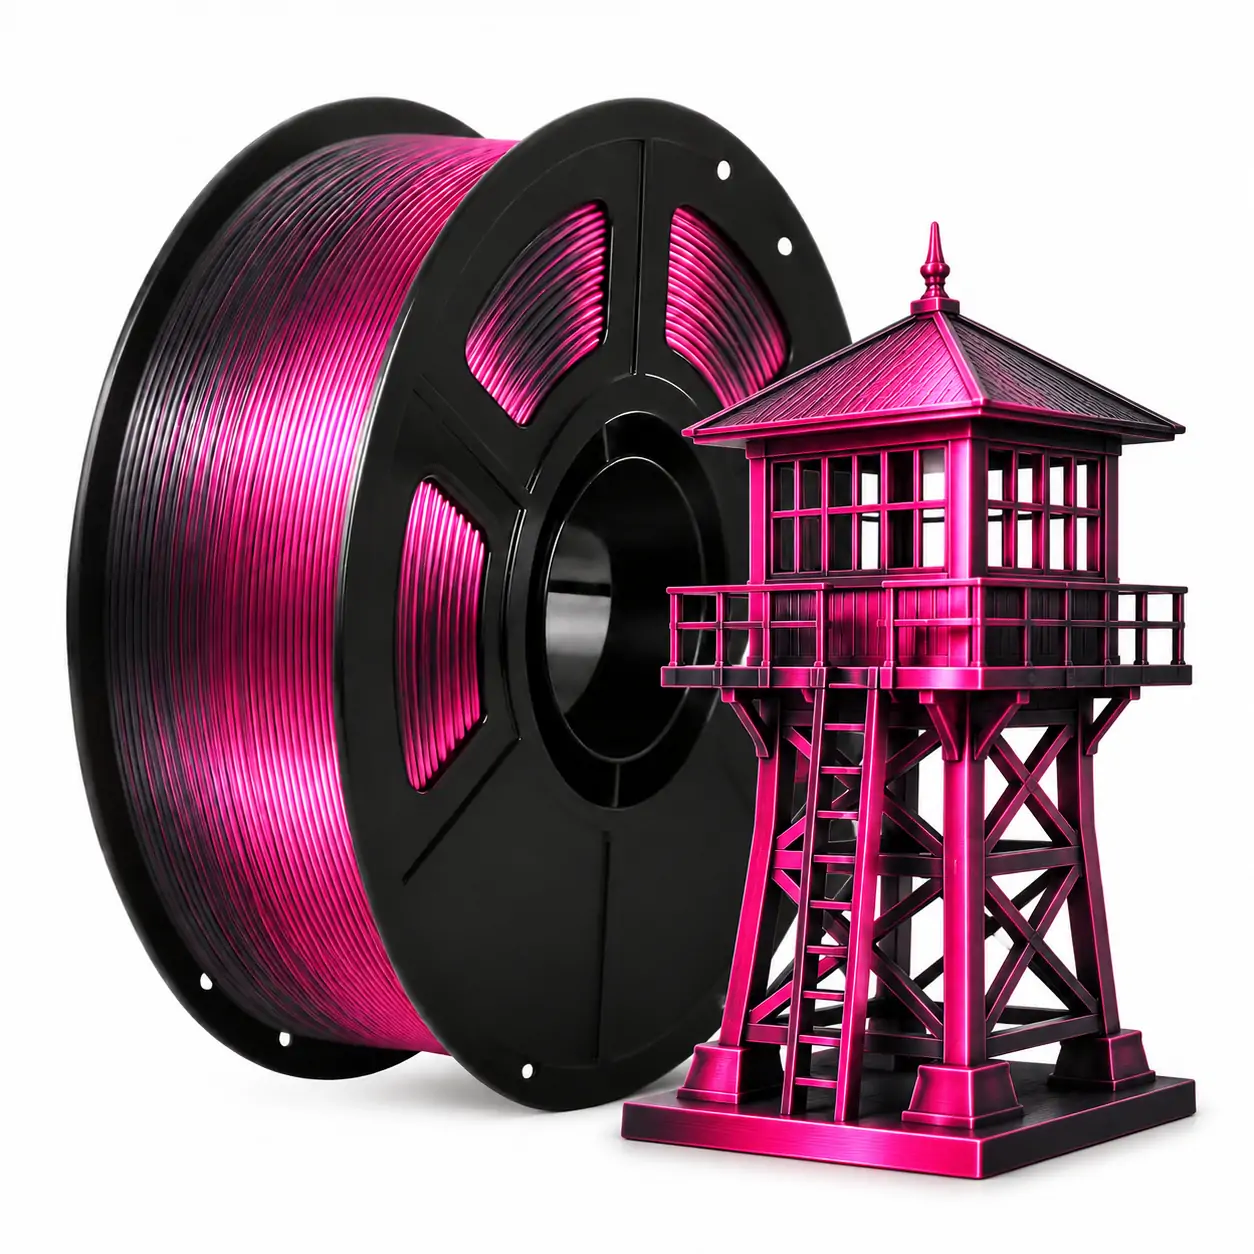
SSSray PLA Silk Series | Sequential Black & Magenta Color | Factory Wholesale & OEM / ODM
SSSray Black & Magenta Dual-Color Silk PLA 1.75mm 3D Printer Filament – dwukolorowy filament PLA for Decorative & Display Models
Sequential Black & Magenta Silk PLA for decorative FDM/FFF prints, display towers, spiral forms and distinctive retail filament ranges.
Black and vivid magenta run in distinct sections along the filament length. As the spool feeds through a standard single-nozzle FDM/FFF printer, each color section is extruded in sequence to create bands along the printed toolpath—without a second extruder or manual filament change. SSSray supplies this 1.75mm, 1kg Silk PLA spool with ±0.03mm diameter tolerance for wholesale, distribution and private-label programs.
MaterialSequential Two-Color Silk PLA
SeriesPLA Silk Series
Color EffectSequential Black / Magenta Sections
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp.210–230°C
Bed Temp.50–60°C
Print Speed60–120mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time for This SKU: Standard orders 7–15 working days; customized orders 15–25 working days, subject to confirmed specifications and order arrangement.
Product Overview
SSSray Black & Magenta Sequential Silk PLA is designed for decorative FDM/FFF prints where color changes along the toolpath are preferred over a side-by-side two-tone effect. Black and vivid magenta occupy distinct sections along the filament length. As the spool feeds through a compatible single-nozzle hotend, each section is deposited in sequence to form successive color bands—without a second extruder or manual filament change. The visible band spacing depends on the length of each color section and the amount of filament used by the model, so tall walls, spiral vases and continuous paths make the sequence easier to see. The high-gloss silk surface adds reflective highlights to both colors. Each spool contains 1kg net filament on a plastic spool, with a 1.75mm diameter and ±0.03mm tolerance, and is vacuum-sealed with desiccant. SSSray supplies this SKU to distributors, wholesalers, importers and private-label brands. Neutral packaging starts at 50 rolls; OEM packaging typically starts at 500–1,000 rolls.
How the Color Sequence Works
Black and vivid magenta occupy separate sections along the filament length. As the filament enters a standard single-nozzle hotend, each section is deposited in feed order and creates successive bands along the printed toolpath. Unlike side-by-side dual-color silk filament, this effect is not selected by rotating the filament or changing the model’s viewing angle. It is also different from a continuous-gradient filament: the color change comes from separate sections reaching the nozzle in sequence. The visible pattern depends on the section length and the amount of material used by the model.
| Color-Sequence Factor | What It Means for the Printed Result |
|---|---|
| Color-section length | Determines how much filament is consumed before the next color reaches the nozzle; confirm the visible interval with a representative print sample. |
| Material consumption | Line width, layer height, wall count, infill and model size affect when each color section appears on the printed part. |
| Toolpath design | Tall walls, spiral-vase paths and long continuous lines make sequential color bands easier to see. |
| Printer setup | Uses a compatible 1.75mm FDM/FFF printer with a standard single-nozzle filament path. |
| Sample evaluation | Print the intended model or a representative test piece before confirming the visual result for a retail or OEM program. |
Why Choose SSSray Black & Magenta Sequential Silk PLA
Lengthwise Black & Magenta Sections
Separate color sections reach the nozzle in sequence, creating successive bands along the printed toolpath rather than simultaneous two-face color effects.
Single-Nozzle Printing
The color sequence is built into one 1.75mm filament strand, so a compatible single-nozzle FDM/FFF printer can print it without a second extruder or manual color swaps.
High-Gloss Silk Finish
The reflective silk surface gives both the black and magenta sections a polished appearance for decorative and display models.
1.75mm Diameter / ±0.03mm
The specified diameter and tolerance provide a defined dimensional reference for compatible 1.75mm FDM/FFF systems.
Wholesale & OEM Supply
Neutral packaging starts at 50 rolls; OEM packaging typically starts at 500–1,000 rolls for private-label programs.
A Distinctive SKU for Decorative Filament Ranges
This SKU gives distributors a clear point of difference within a Silk PLA range: black and magenta reach the nozzle in separate lengthwise sections, so the printed color sequence follows filament consumption rather than changing with viewing angle. It is suited to decorative towers, spiral vases, sculptural vessels, trophies, faceted models and other display-focused products.
The 1kg spool fits a familiar retail unit. Neutral packaging starts at 50 rolls, while OEM packaging typically starts at 500–1,000 rolls. Use a representative print sample to evaluate the color-band appearance before confirming the SKU for a retail or private-label assortment.
Our 6-Step Order Process
1
Requirement Review2
Specification & MOQ Confirmation3
Sample Evaluation4
Label & Packaging Approval5
Production Arrangement6
QC Review & ShipmentFilament Construction & Material Comparison
| Material / Construction | Appearance & Construction | Typical Print Conditions | Typical Applications | Selection Consideration |
|---|---|---|---|---|
| Black & Magenta Sequential Silk PLA | Separate black and magenta sections along the filament length; high-gloss silk surface; colors extrude in sequence. | Nozzle 210–230°C; bed 50–60°C; 60–120mm/s recommended. | Display towers, spiral vases, trophies, decorative vessels and faceted models. | Choose when sequential color bands along the toolpath are the intended visual effect. |
| Side-by-Side Co-Extruded Silk PLA | Two colors share the filament cross-section and can appear on different faces of the same printed path. | Typically 210–230°C nozzle and 45–60°C bed; tune speed to the specific formulation. | Two-tone figurines, medallions, reliefs and models where contrasting faces are desired. | Choose when simultaneous side-by-side color presentation is required. |
| Gradient / Rainbow PLA | Color changes gradually along the filament over a product-specific cycle; cycle length and transition profile depend on the manufacturer’s design. | Follow the exact product’s published material settings and cycle guidance. | Rainbow vases, long decorative prints and models where gradual color progression is preferred. | Choose for gradual transitions rather than separate sequential color sections. |
| Single-Color Silk PLA | One color throughout the spool with a reflective silk surface. | Typically 210–230°C nozzle and 50–60°C bed. | Decorative prints, figurines, ornaments and display models. | Choose when a consistent single-color silk finish is preferred. |
| Standard PLA | Single-color PLA with matte, satin or standard surface options depending on formulation. | Typically 190–230°C nozzle and 50–60°C bed. | Concept models, education, general prototypes and everyday decorative prints. | Choose for broad-purpose PLA printing without a sequential silk color effect. |
| PETG | More ductile than common PLA grades; typically different stringing, cooling and bed-adhesion behavior. | Typically 230–250°C nozzle and 60–80°C bed. | Functional housings, brackets and parts requiring greater ductility than standard PLA. | Choose when the part requirements call for PETG material behavior rather than a silk appearance. |
| ABS / ASA | Higher-temperature thermoplastics with greater shrinkage and enclosure considerations than PLA. | Typically 230–260°C nozzle and 90–110°C bed; an enclosure is commonly used. | Functional housings, engineering components and outdoor-oriented ASA parts. | Choose when heat or environmental requirements justify the different printing setup. |
Technical Specifications
| Product Name | SSSray Black & Magenta Dual-Color Silk PLA 1.75mm 3D Printer Filament – dwukolorowy filament PLA for Decorative & Display Models |
|---|---|
| Material | PLA (Polylactic Acid), Sequential Two-Color Silk Finish |
| Product Series | SSSray PLA Silk Series – Dual-Color Display Collection |
| Color / Effect | Black & Vivid Magenta; distinct color sections along the filament length with a high-gloss silk surface |
| Filament Construction | Lengthwise-segmented color sections; sequential color feed during printing |
| Filament Diameter | 1.75mm standard for this SKU |
| Diameter Tolerance | ±0.03mm |
| Net Filament Weight | 1kg per spool |
| Gross Weight | 1.3kg per packaged unit |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Printing Technology | FDM / FFF; standard single-nozzle filament path |
| Recommended Nozzle Temperature | 210–230°C |
| Recommended Bed Temperature | 50–60°C |
| Recommended Print Speed | 60–120mm/s; calibrated high-flow systems can be tuned toward 200mm/s |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, subject to printer, hotend and slicer setup |
| OEM / ODM | Available for qualified B2B projects |
| MOQ | Neutral packaging: 50 rolls; OEM packaging: typically 500–1,000 rolls |
| Lead Time | For this SKU: standard orders 7–15 working days; customized orders 15–25 working days after order details are confirmed. |
| Trade Terms | FOB Ningbo Port, China, Incoterms® 2020; EXW at the agreed named place, to be stated in the quotation, Incoterms® 2020. |
| Compliance Document | SKU-specific RoHS documentation available |
Recommended Starting Print Settings
| Parameter | SSSray Starting Value | Performance / Tuning Range |
|---|---|---|
| Nozzle Diameter | 0.4mm | Use a clean nozzle; match diameter to the required detail and flow. |
| Nozzle Temperature | 210–230°C | 190–240°C after a temperature and extrusion check; adjust in 5°C steps. |
| Bed Temperature | 50–60°C | 45–60°C according to build plate and first-layer adhesion; selected cool / adhesive plates may use 35–45°C. |
| Overall Print Speed | 60–120mm/s | 40–200mm/s after flow and temperature calibration on a suitable high-flow system. |
| Outer-Wall Speed | 30–50mm/s | 25–50mm/s; use the lower end for stronger silk gloss and clearer surface detail. |
| Retraction – Direct Drive | 0.8–1.2mm at 30–40mm/s | Fine-tune by extruder and hotend to control stringing without grinding. |
| Retraction – Bowden | 3–5mm at 30–40mm/s | Adjust to tube length, hotend path and stringing result. |
| Layer Height | 0.16–0.20mm | 0.12–0.24mm with a 0.4mm nozzle, depending on detail and build time. |
| Part Cooling Fan | 100% after the first layers | 80–100%; maintain first-layer adhesion and check bridges and overhangs. |
| Wall Count | 3 perimeters | 2–4 perimeters according to the model wall design and display geometry. |
| Infill | 15–20% for decorative models | 25–40% for larger display pieces; 40–60% for heavier bases where the design requires it. |
| First-Layer Speed | 20–30mm/s | 15–30mm/s according to plate condition and first-layer stability. |
| Bed Adhesion | Textured PEI at 50–60°C | Smooth PEI or glass with a plate-compatible adhesive when required. |
These SSSray starting profiles are designed for practical throughput and a clean silk surface. Increase overall speed only after flow and temperature calibration; keep visible outer walls slower when silk gloss and clear color bands are the priority.
Print Tips for Consistent Color Bands and Silk Gloss
| Optimization Item | SSSray Printing Guidance |
|---|---|
| Plan the Color-Band Scale | Print a representative tower wall, trophy stem or vase section first. Visible band spacing follows the filament section length and the amount of material used along the toolpath. |
| Use Continuous Outer-Wall Paths | Where the model allows, use long continuous walls or spiral-vase paths so color transitions remain visually connected along the print. |
| Keep the Toolpath Consistent | Use the same layer height, line width, wall count and model orientation when comparing samples or approving a production profile. |
| Preserve Silk Gloss | Keep visible outer walls around 30–50mm/s; raise internal and infill speed after flow calibration. |
| Set Temperature & Flow | Start at 210–230°C and calibrate flow so both color sections extrude evenly through the same nozzle. |
| Control First-Layer Adhesion | Clean and level the build plate, set the first layer to 20–30mm/s and match bed temperature to the plate surface. |
| Calibrate Retraction | Set Bowden and direct-drive systems separately. Adjust one parameter at a time to isolate stringing. |
Printer-Specific Starting References
| Printer Platform | Nozzle | Bed | Print Speed | Setup Notes |
|---|---|---|---|---|
| Bambu Lab | 210–230°C | 35–45°C on compatible cool plates with adhesive; 50–60°C PEI starting reference | 50–120mm/s | Start with a PLA base profile and a single-spool feed path; keep visible outer walls around 30–50mm/s and calibrate flow before increasing internal speed. |
| Prusa | 210–220°C | 50–60°C | 50–100mm/s | Begin near the standard PLA temperature profile; check first-layer adhesion on the selected PEI sheet and keep visible outer walls slower for silk gloss. |
| Creality | 210–230°C | 50–60°C | 40–80mm/s | Confirm whether the printer uses Bowden or direct-drive extrusion, then tune retraction before longer prints. |
| Flashforge | 210–230°C | 25–60°C | 60–120mm/s | Start with a 0.4mm nozzle profile; raise speed only after hotend flow, cooling and surface finish are stable. |
| Anycubic / Elegoo | 210–230°C | 50–60°C | 50–100mm/s | Use a standard single-spool feed path and print a tall continuous-wall sample to evaluate color-band placement. |
Start with these SSSray profiles, then tune the exact printer model, extruder path, hotend, build plate and slicer settings for your production setup.
Recommended Applications
| Application Focus | Practical Notes |
|---|---|
| Decorative Towers & Architectural Models | Tall walls and continuous vertical paths give the black-magenta sections room to appear as successive bands. |
| Spiral Vases & Ribbed Vessels | Spiral and repeated-rib geometry makes sequential color changes easy to follow around the printed surface. |
| Faceted Display Models | Angular faces and larger model volumes reveal more of the filament sequence as material is consumed. |
| Trophies, Awards & Desk Décor | Use the black-magenta sequence on trophy stems, decorative bases, commemorative pieces and statement ornaments. |
| Figurines & Sculptural Prints | Choose taller or larger forms when the design needs enough extrusion length to show multiple color sections. |
| Retail Samples & Giftware Collections | Pair a tall continuous-wall sample with a detailed display model to demonstrate the sequential color effect and silk surface. |
Storage Guide
- Keep unopened spools in their vacuum-sealed bags with the supplied desiccant until use.
- After opening, return unused filament to a sealed bag or dry storage box with fresh desiccant.
- Store in a cool, dry indoor environment and keep the spool away from direct sunlight and heat sources.
- Avoid prolonged exposure to humid workshop air; use a filament dry box during extended printing sessions when needed.
- If moisture-related popping, bubbling or rough extrusion appears, dry the filament at 50–55°C for 6–8 hours only when the spool is rated for that temperature; otherwise transfer the filament to a heat-rated spool before drying.
OEM / ODM Services
SSSray manufactures filament for distributors, wholesalers, importers, retailers and private-label brands. For this Black & Magenta Sequential Silk PLA program, our team can coordinate branded spool labels, retail box artwork, barcode and language labeling, carton marks, spool presentation and packaging for a wider color collection.
Share your target market, pack format and planned order volume; we will align the product specification and packaging route with your buying plan. Neutral packaging starts from 50 rolls, while OEM packaging typically starts from 500–1,000 rolls. We finalize the approved sample, artwork and packing specification before mass production.
Production Quality Checks
- Raw Material & Batch Identification: We record the material, color batch and production lot before extrusion.
- Inline Laser Diameter Monitoring: We monitor the 1.75mm filament during production against the specified ±0.03mm diameter tolerance.
- Color-Section Inspection: We inspect the black-magenta sequence, transition appearance, opacity and silk surface against the approved color reference.
- Moisture & Melt-Flow Checks: We test material condition and melt-flow behavior to support controlled extrusion and consistent processing.
- Winding, Weight & Spool Inspection: We check winding alignment, spool condition, filament-end retention and 1kg net weight.
- Print Validation & Final Packing: We review representative print samples and inspect the vacuum seal, desiccant, product label and export-carton configuration.
Our factory quality-control capabilities include online laser diameter measurement, colorimeter / spectrophotometer checks, moisture analysis, melt-flow testing, precision weighing and 3D-printer validation. Review SSSray batch QC information.
Compliance & Technical Documents
SSSray has SKU-specific RoHS documentation for this Black & Magenta Sequential Silk PLA. The applicable RoHS file is available for buyer compliance review and order documentation.
For technical qualification, ask our sales team for the current TDS and SDS / MSDS documents relevant to your order. Visit the SSSray TDS / SDS document centre.
Frequently Asked Questions
What is the MOQ for Black & Magenta Sequential Silk PLA?
Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls, depending on the label, retail box and customization scope.
How are the black and magenta colors arranged in the filament?
Black and vivid magenta are arranged in separate sections along the filament length. As the spool feeds, each section passes through the hotend in sequence and creates color bands along the printed toolpath.
Does this filament need a dual-extruder or multi-color printer?
No. The color sequence is built into one 1.75mm filament strand, so a compatible standard single-nozzle FDM / FFF printer can produce the color changes without a second extruder or manual filament swap.
How can I control the printed color-band pattern?
Band placement depends on the filament section length and the amount of material used along the model toolpath. Use a representative tower wall, vase or continuous-path sample to evaluate the result before choosing a production model.
What print settings should we start with?
Start at 210–230°C nozzle temperature, 50–60°C bed temperature and 60–120mm/s overall speed. A calibrated high-flow setup can be tuned toward 200mm/s. Keep visible outer walls around 30–50mm/s when silk gloss is the priority.
Which printer types can use this 1.75mm filament?
It is designed for most open-material 1.75mm FDM / FFF printers, including Bambu Lab, Prusa, Creality, Flashforge, Anycubic and Elegoo platforms. Match the profile to the exact hotend, extruder path, build plate and slicer setup.
Can I request samples and OEM packaging?
Qualified B2B buyers may apply for up to 3 free sample rolls after project review. SSSray supports private-label labels, retail boxes, barcode and language labeling, carton marks and coordinated packaging programs.
Is RoHS documentation available, and what are the lead time and payment terms?
SKU-specific RoHS documentation is available for this product. For this SKU, standard orders are typically 7–15 working days and customized orders 15–25 working days after order details are confirmed. Standard payment terms are 30% deposit and 70% balance before shipment. T/T is accepted for orders; PayPal is available for small trial orders, while L/C is considered only for evaluated large-volume customers.
Add Sequential Black & Magenta Silk PLA to Your Product Range
Bring a lengthwise-segmented Silk PLA option into your decorative filament assortment. Black and vivid magenta print in sequence through a standard single-nozzle FDM workflow. Contact SSSray for bulk pricing, sample evaluation and a private-label packaging program built around your target market.

Related products
-

SSSray PLA Signage Grade 3D Printing Filament – Translucent & Solid 1kg (Custom OEM & Wholesale)
-
Metallic Bronze PLA Filament 1.75mm 1kg – Premium Metal Effect Filament with High Gloss Finish for Engineering Prototypes & Decorative FDM Printing
-
Pastel Rainbow PLA Filament 1.75mm 1kg – Smooth Color Transition Multicolor PLA for FDM 3D Printing, Ideal for Creative Decor & Designer Toys
-
Pure White PLA+ Filament by SSSray – Filament PLA+ Biały for Detailed Architectural & Display Models, Low-Sheen 3D Printer Filament