Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

SSSray PLA Multi-Color Series | Dual-Color Silk | Wholesale & OEM / ODM
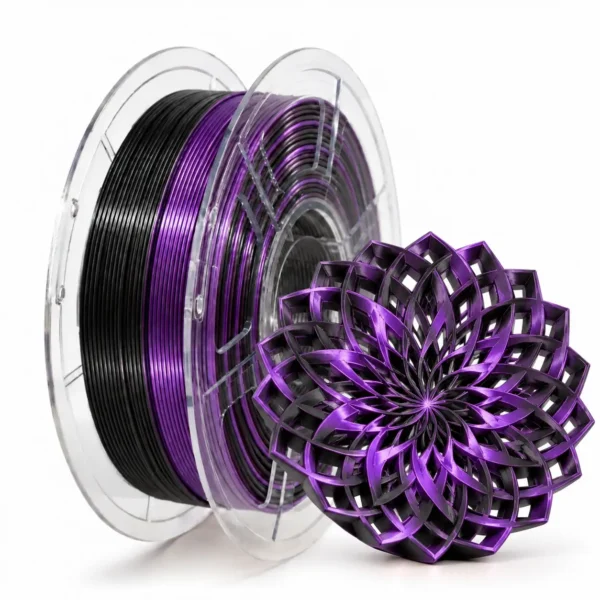
SSSray Dual-Color Silk PLA 3D Printer Filament 1.75mm, Black & Purple Multicolor – Çift Renkli İpek PLA Filament for Decorative Prints & Display Models
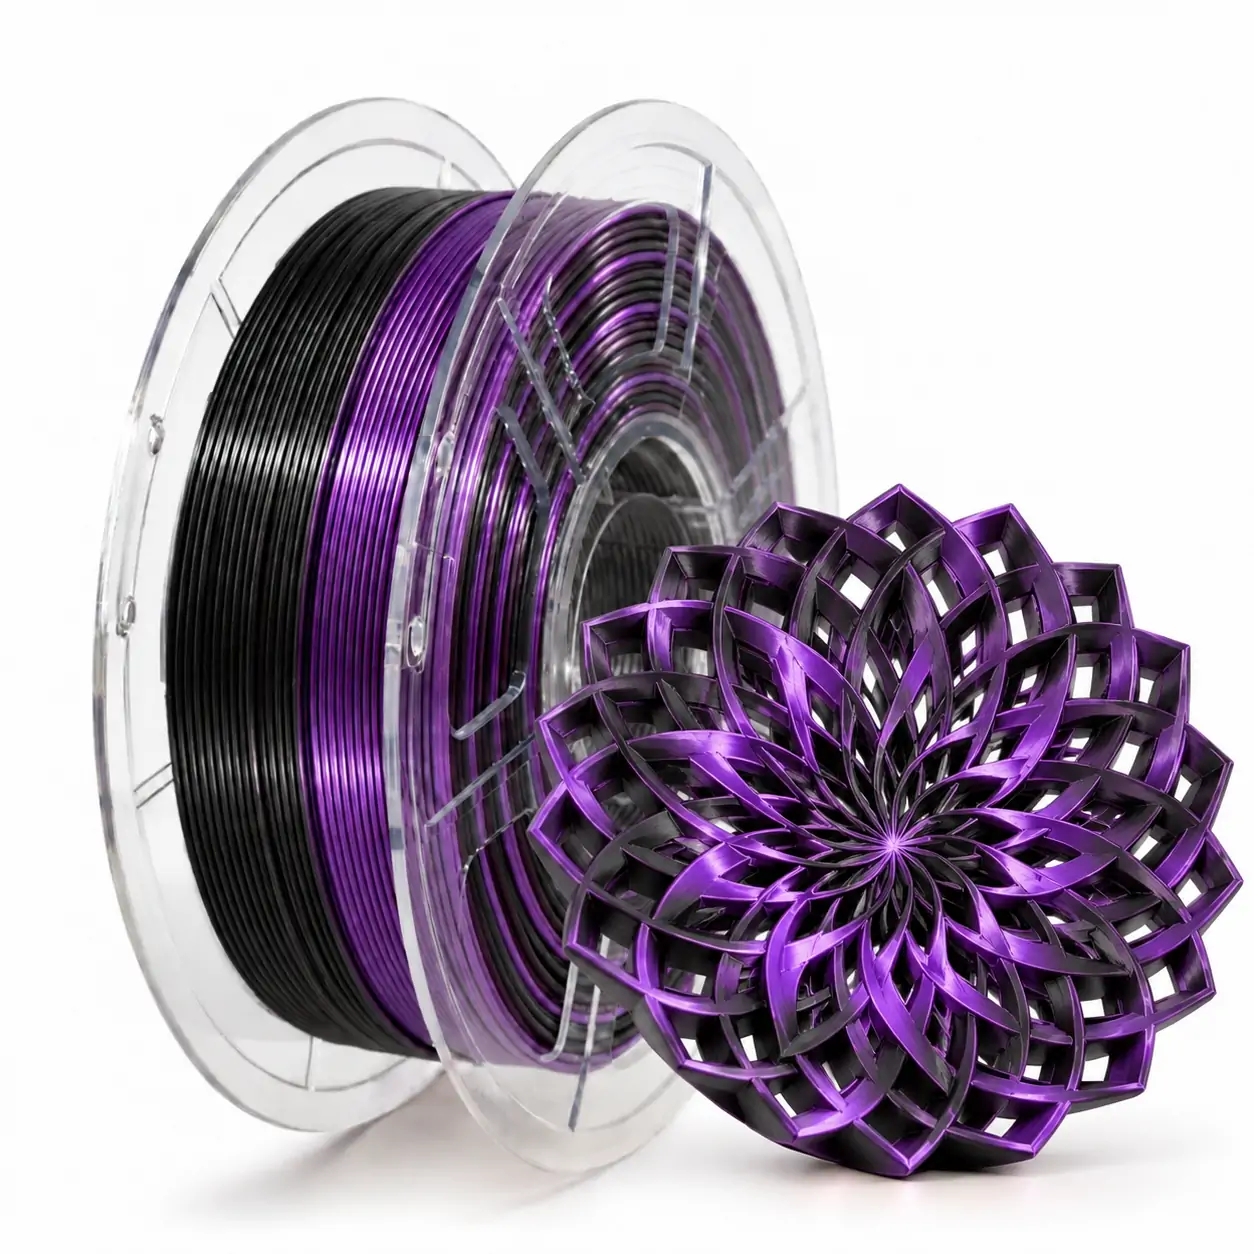
Black-and-purple co-extruded silk PLA for decorative prints, display models and distinctive private-label filament ranges.
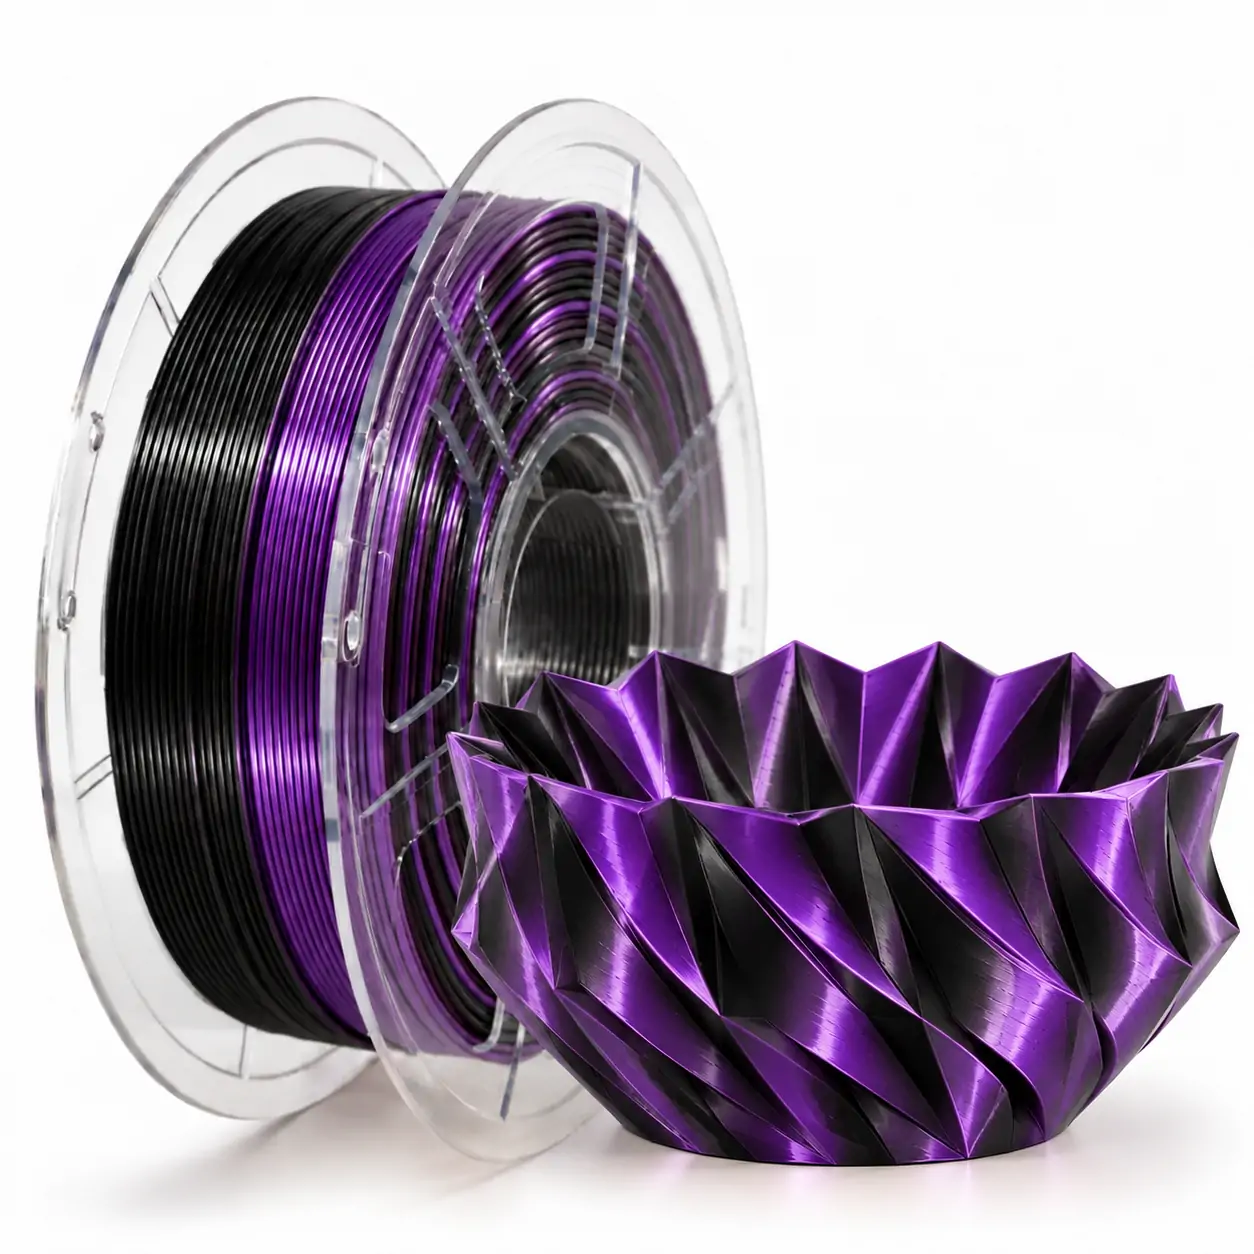
One filament strand combines deep midnight black with saturated royal purple. Printed faces reveal contrasting tones as the model turns, with bright silk highlights on the purple side and a smooth, lightly reflective black side. The color does not transition along the spool length.
MaterialSilk PLA
SeriesSSSray PLA Multi-Color Series
Color EffectBlack / Royal Purple
Diameter1.75mm
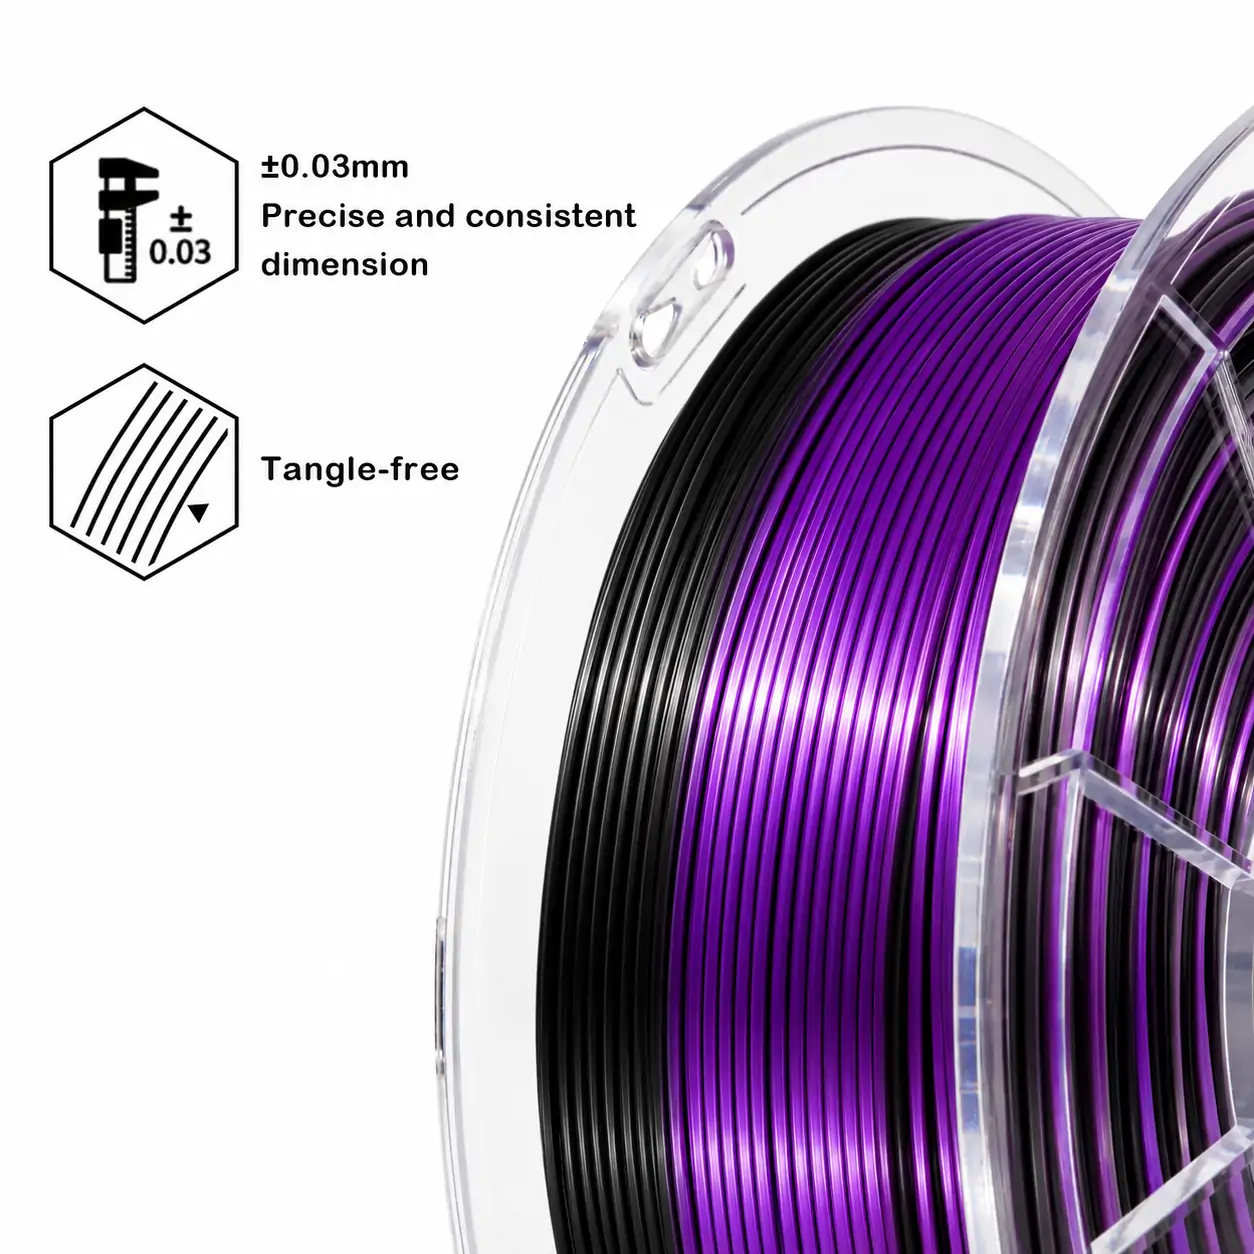
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp210–230°C
Bed Temp45–60°C
Print Speed50–150 mm/s
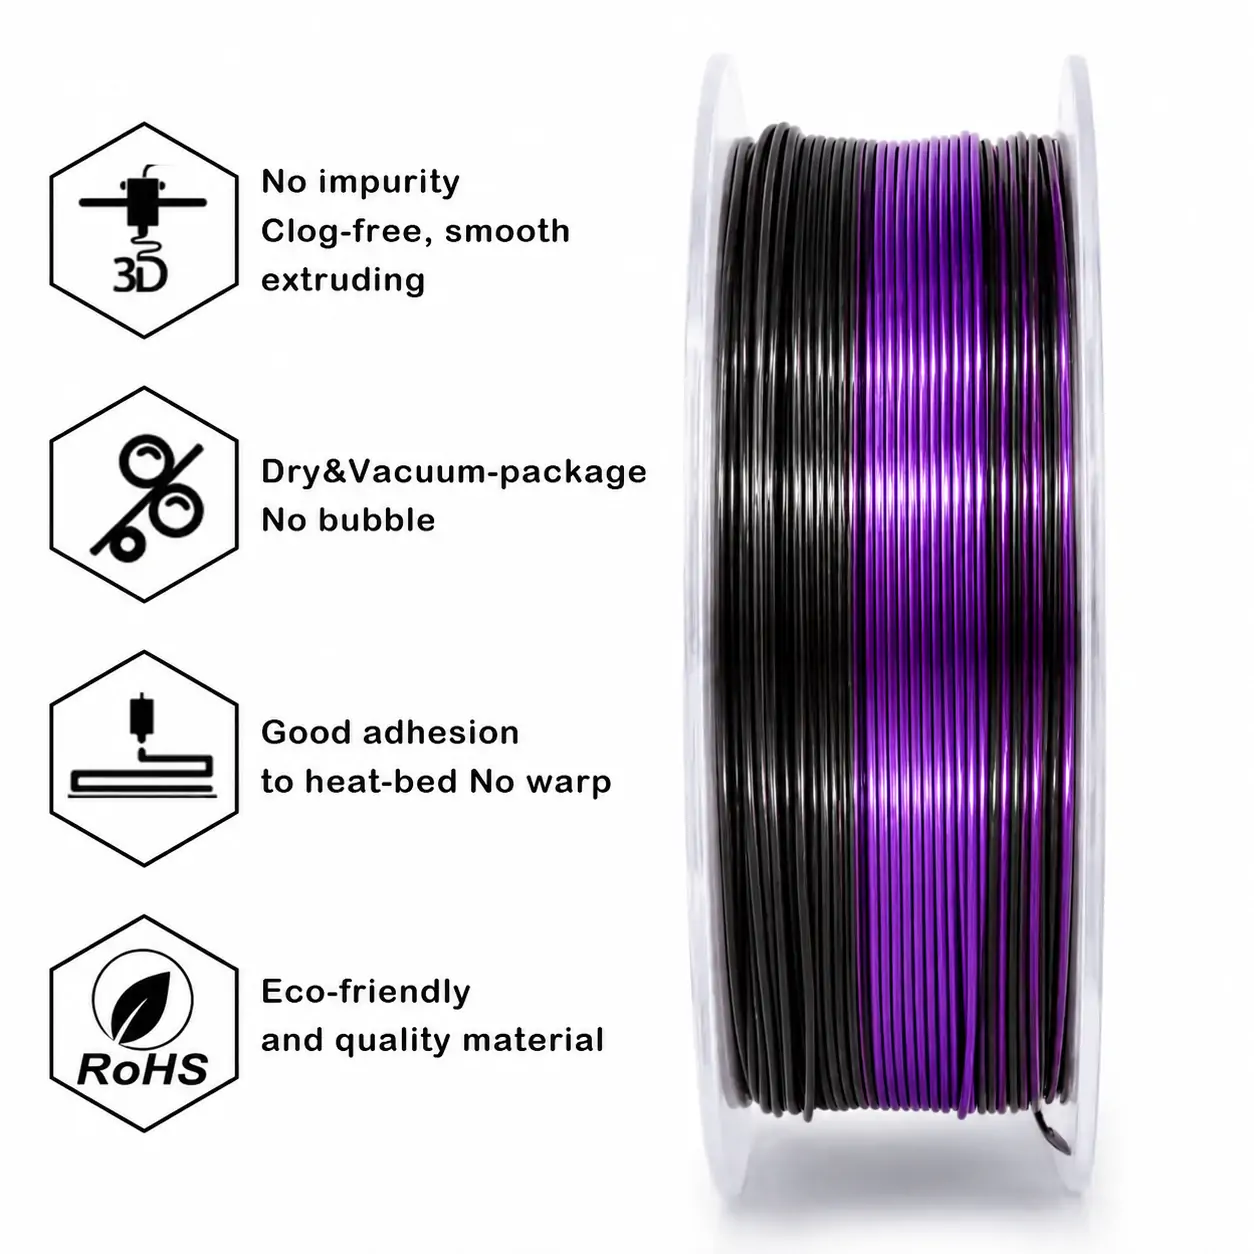
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time: Standard orders 7–15 days; customized orders 15–25 days.
Product Overview
We manufacture this black-and-purple co-extruded Silk PLA for FDM/FFF buyers who want a clearly recognizable decorative SKU rather than another generic rainbow filament. One strand combines deep midnight black with saturated royal purple; as the model turns, opposite faces reveal different tones, with bright silk highlights on the purple side and a smooth, lightly reflective black side. The construction stays black-and-purple along the spool instead of changing through a lengthwise rainbow sequence, and the finished appearance is neither transparent nor metal-filled. With 1.75mm diameter, ±0.03mm tolerance, a 1kg net spool and vacuum-sealed packing, it is built for display models, sculptural décor, decorative vessels, figurines, awards, desk accessories and other appearance-led prints. From our filament manufacturing operation in Jinhua, Zhejiang, China, we support neutral wholesale supply, sample qualification, OEM packaging and private-label programs for distributors, importers and filament brands.
For range planning, browse our PLA Silk filament series and wholesale PLA supply. Buyers comparing suppliers can also use our Filament Qualification Program and bulk filament test protocol before releasing a volume order.
Key Selling Points
Co-Extruded Two-Color Strand
Black and royal purple are combined in one filament strand, creating contrasting faces without a lengthwise gradient.
Silk Purple Highlights
The royal-purple face reflects light with bright silk highlights that bring definition to curved and faceted surfaces.
Deep Black Contrast
The midnight-black face stays deep, smooth and lightly reflective, balancing the brighter purple side.
Distinctive Display Finish
Designed for decorative vessels, lattice forms, figurines, display models and other appearance-led prints.
Controlled Diameter Specification
The stated 1.75mm diameter and ±0.03mm tolerance give buyers a clear dimensional target for product qualification.
Wholesale & Private-Label Supply
Neutral packaging starts at 50 rolls, with OEM packaging programs typically arranged for 500–1,000 rolls.
Commercial Value for Wholesale Buyers
We built this black-and-purple Silk PLA as a sellable effect-color SKU for distributors and private-label brands: the color pairing is easy to demonstrate with one printed model, the 1kg format fits mainstream retail programs, and the dual-face silk finish gives buyers a clear reason to list it beside standard PLA colors. Neutral packaging starts from 50 rolls for market testing, while OEM packaging programs typically run from 500–1,000 rolls for branded range launches and repeat orders.
How We Work
1
Market & SKU Brief
2
Black / Purple Color Approval
3
Printer Sample Qualification
4
Packaging & Artwork Lock
5
Batch Production & In-Process QC
6
Final QC & Export Shipment
Material Comparison Guide
| Material | Visual / Material Characteristic | Typical Starting Print Conditions | Typical Application Focus |
|---|---|---|---|
| SSSray Dual-Color Silk PLA | Co-extruded black and purple strand; angle-dependent two-face appearance; silk sheen on the purple face. | Nozzle 210–225°C; bed 50–60°C; outer walls 30–45 mm/s. | Decorative vessels, figurines, display models and appearance-led consumer products. |
| Single-Color Silk PLA | One dominant color with a reflective silk-style surface; no dual-face black/purple construction. | Common silk PLA starting range: nozzle 190–230°C; bed 45–60°C; slow outer walls for gloss. | Glossy ornaments, display pieces and single-color decorative models. |
| Standard PLA / PLA+ | Usually matte or standard colored surface; no silk sheen or co-extruded two-color effect. | Common PLA starting range: nozzle 190–220°C; bed 45–60°C; speed depends on grade and printer. | General models, prototypes, figures and everyday non-high-temperature prints. |
| PETG | Typically less silk-like surface reflection; material behavior and flexibility differ from PLA. | Often uses a higher nozzle and bed range than PLA; follow the selected PETG grade’s TDS. | Functional covers, brackets and parts where PETG’s material behavior is preferred. |
| ABS / ASA | Engineering-oriented thermoplastics with different thermal behavior from PLA; enclosure and warping control are commonly important. | Higher-temperature printing; heated bed and controlled enclosure conditions are commonly required. | Engineering parts and, for suitable ASA grades, outdoor-oriented components. |
Technical Specifications
| Product Name | SSSray Dual-Color Silk PLA 3D Printer Filament 1.75mm, Black & Purple Multicolor – Çift Renkli İpek PLA Filament for Decorative Prints & Display Models |
|---|---|
| Material | PLA (Polylactic Acid), dual-color co-extruded strand with silk finish |
| Product Series | SSSray PLA Multi-Color Series |
| Color / Visual Effect | Midnight Black & Royal Purple Dual-Color Silk; opposite faces and viewing angles show different tones. |
| Purple Surface | Saturated violet-purple with a silk sheen and bright highlights. |
| Black Surface | Deep, smooth black with light reflectivity. |
| Color Transition | No lengthwise gradient along the spool; not transparent and not metallic. |
| Filament Diameter | 1.75mm standard; 2.85mm only for selected products or projects after confirmation. |
| Diameter Tolerance | ±0.03mm |
| Net Filament Weight | 1kg standard; 3kg / 5kg formats subject to SKU and spool confirmation. |
| Gross Weight | 1.3kg per packed unit |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Recommended Nozzle Temperature | 210–230°C |
| Recommended Bed Temperature | 45–60°C; 35–45°C with glue on selected Bambu build plates |
| Typical Print Speed | 50–150 mm/s for production; usable up to 250 mm/s after flow and temperature tuning, with slower visible outer walls for maximum silk gloss. |
| Recommended Nozzle Diameter | 0.4mm standard nozzle |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, subject to the printer’s filament path and spool dimensions. |
| Typical Applications | Decorative prints, display models, figurines, decorative vessels, awards and desk accessories. |
| OEM / ODM | Supported for qualified B2B projects; packaging, labels and private-label arrangements subject to order confirmation. |
| Compliance Documents | TDS, SDS and available compliance records for this SKU can be supplied with the order documentation. |
Recommended Print Settings
| Parameter | Recommended Value | Usable / Adjustment Range |
|---|---|---|
| Nozzle Temperature | 210–230°C | 190–240°C; use the higher end for calibrated high-flow printing. |
| Bed Temperature | 45–60°C | 35–60°C depending on build surface; use 35–45°C with glue on low-temperature high-adhesion plates. |
| Print Speed | 50–150 mm/s | 40–250 mm/s after flow, temperature and cooling tuning; use the lower end for maximum silk gloss. |
| Outer-Wall Speed | 35–60 mm/s | Use 35–45 mm/s for maximum gloss; 45–60 mm/s for a stronger balance of finish and throughput. |
| Direct-Drive Retraction | 0.5–1.0mm | Starting range; tune distance and speed to the extruder and hotend. |
| Bowden Retraction | 2–4mm | Starting range; avoid excessive retraction that can cause inconsistent extrusion. |
| Retraction Speed | 25–35 mm/s | 20–40 mm/s starting range, depending on the printer’s extruder system. |
| Layer Height | 0.12–0.24mm | 0.12–0.28mm for a 0.4mm nozzle, depending on detail and print time. |
| Cooling Fan | 80–100% after the first layers | Use up to 100% for bridges and overhangs; tune for layer bonding on large parts. |
| Wall Count | 2–3 perimeters | 3–4 perimeters for display pieces that need a more substantial shell. |
| Infill | 15–20% for decorative models | 30–40% for added rigidity in non-load-bearing display parts. |
| First-Layer Speed | 15–25 mm/s | Reduce further if the first layer does not bond evenly. |
| Bed Adhesion | Clean PEI, satin PEI or smooth PEI | Textured PEI or glass with a suitable adhesion aid after a small first-layer test. |
| Nozzle Diameter | 0.4mm | 0.6mm can be evaluated for larger models after flow and finish calibration. |
| Drying | 55°C for 6–8 hours when moisture control is needed | Store sealed with desiccant after drying to protect gloss, extrusion consistency and surface finish. |
For production, start with the recommended window above, then lock temperature, flow, cooling and retraction on the printer profile that delivers the required gloss and color-face consistency.
Print Optimization Guide
| Optimization Item | Practical Guidance |
|---|---|
| Show the Two-Color Faces | Use a small orientation test piece first. Model geometry and viewing angle determine where the black and purple faces are most visible. |
| Preserve Silk Gloss | Keep visible outer walls around 30–45 mm/s and avoid excessive speed on the surfaces intended to catch highlights. |
| Set Nozzle Temperature | Begin at 210–225°C, then compare a short temperature test for layer bonding, stringing and surface appearance. |
| Control Cooling | Start at 80–100% after the first layers. Use strong cooling for bridges and overhangs, then adjust if layer bonding needs improvement. |
| Secure the First Layer | Clean the build plate, use a 50–60°C bed and start with a 15–25 mm/s first layer. |
| Reduce Stringing | Check filament condition and nozzle temperature before increasing retraction. Tune Direct Drive and Bowden distances separately. |
| Position the Seam | Place the Z-seam on a rear edge or less visible face when the model design allows it. |
| Maintain Dry Storage | Return unused filament to a sealed bag or dry box with desiccant. Dry only with a spool-safe setup when moisture symptoms appear. |
Printer Brand Starting Settings
| Printer Ecosystem | Nozzle | Bed | Initial Speed | Setup Notes |
|---|---|---|---|---|
| Bambu Lab X1 / P1 Series | 210–230°C | 35–45°C with glue | 60–200 mm/s | Use a Silk PLA profile; keep visible outer walls around 40–60 mm/s when gloss and color separation matter most. |
| Bambu Lab A1 / A1 mini | 210–230°C | 35–45°C with glue | 50–160 mm/s | Use a Silk PLA profile and run a small orientation test before production. Confirm the visible black / purple face on your actual setup before locking a customer sample or batch profile. |
| Prusa MK4 / CORE One / XL | 210–230°C | 50–60°C | 50–120 mm/s | Start from the PLA material profile and keep outer perimeters slower when the visual silk finish is the priority. |
| Creality K1 / K1C / K1 Max | 210–230°C | 45–60°C | 60–180 mm/s | Use the high-speed platform for throughput, but keep the visible outer wall below the infill speed to retain silk sheen. |
| Creality Ender Series | 200–225°C | 50–60°C | 40–100 mm/s | Use a Silk PLA profile with strong part cooling and tune first-layer adhesion to the installed build surface. |
| Flashforge Adventurer / Guider Series | 210–230°C | 45–60°C | 60–180 mm/s | Use the platform’s higher throughput for infill and inner walls while keeping visible outer walls slower when maximum gloss is the buying priority. |
Use these platform profiles to get the first successful print quickly, then save the tuned profile for repeat orders and buyer qualification samples.
Performance Characteristics
| Characteristic | Product Specification / Behavior | Production or Application Note |
|---|---|---|
| Strand Construction | Black and royal purple co-extruded in one strand. | Printed color presentation depends on model geometry and viewing angle. |
| Color Structure | The spool keeps the same black / royal-purple dual-face construction along the filament length. | This creates an angle-dependent two-color appearance instead of a sequential rainbow color change. |
| Purple Face | Saturated violet-purple with silk sheen and bright highlights. | Slower outer walls help maintain a consistent visible gloss. |
| Black Face | Deep, smooth and lightly reflective black. | Creates a dark visual counterpoint to the purple surface. |
| Optical Appearance | Non-transparent and non-metallic. | The finished surface shows a two-tone silk sheen without the look of transparent or metal-filled filament. |
| Diameter | 1.75mm with ±0.03mm tolerance. | Controlled diameter supports consistent feeding and repeatable extrusion across wholesale and OEM production runs. |
| Application Positioning | Decorative PLA-based grade for appearance-led models, display items and retail-facing printed products. | Choose our engineering filament ranges instead when the part requires sustained heat or structural loading. |
Applications
| Application Focus | Practical Notes |
|---|---|
| Decorative Vessels & Lattice Bowls | Faceted and open-lattice geometry gives the black and purple faces room to create visible contrast. |
| Figurines & Sculptural Models | Curved surfaces and raised details can catch the purple silk highlights against the darker black areas. |
| Display Models & Product Showpieces | Useful for presentation pieces where color contrast and surface appearance are more important than structural loading. |
| Home Décor & Desk Accessories | Suitable for decorative organizers, ornaments, desk pieces and other indoor display products. |
| Awards, Trophies & Promotional Models | The black-and-purple combination gives brands a distinctive visual option for non-load-bearing display items. |
| Creative Retail & Design Samples | Printed samples help buyers demonstrate the angle-dependent dual-color effect to retail customers. |
Storage Guide
- Keep the filament in its vacuum-sealed bag with the included desiccant until it is ready for use.
- After opening, return the spool to a sealed bag or dry box with fresh desiccant.
- Store in a cool, dry place away from direct sunlight, heaters and high-temperature areas.
- Limit unnecessary exposure to humid room air between print jobs, especially in humid seasons.
- If moisture-related stringing or surface defects appear, use a filament dryer only after confirming that the spool is rated for the selected drying temperature.
OEM / ODM Services
We support OEM / ODM programs for distributors, wholesalers, importers and private-label brands building a decorative PLA range. Options include neutral packaging, custom product labels, branded retail boxes, carton marks, selected spool presentation and coordinated SKU naming. We lock the approved black-purple color presentation, net-weight format and packaging artwork before production so the bulk order follows the same commercial specification.
MOQ Reference: Neutral packaging starts at 50 rolls. OEM packaging is typically arranged for 500–1,000 rolls, depending on the approved packaging scope. Explore our OEM / ODM filament manufacturing service and private-label filament program.
Quality Control
- Diameter measurement against the stated 1.75mm specification and ±0.03mm tolerance.
- Visual inspection of the black-and-purple color arrangement and co-extruded strand appearance.
- Spool winding inspection for orderly layers and stable filament payout.
- Print-sample review for extrusion consistency, surface appearance and silk highlights.
- Vacuum-seal and desiccant inclusion checks for the packed unit.
- Carton, product label and order-marking review before shipment release.
Compliance & Technical Documents
For this SKU, SSSray supplies TDS and SDS for technical reference and safe handling. Available RoHS / REACH declarations and third-party reports can also be provided when they match the current formulation and destination market.
Send us your destination market and required document checklist with the inquiry, and our sales team will provide the matching technical and compliance files for your order.
Frequently Asked Questions
What makes this black and purple silk PLA different from gradient PLA?
This filament uses a black-and-purple co-extruded strand. The two colors occupy different faces and appear differently as the printed model turns. It is a dual-face color effect rather than a rainbow or lengthwise-gradient color sequence.
Does the dual-color effect require a multi-material printer?
The black-and-purple color construction is built into one filament strand, so the two-tone appearance does not require loading two separate color spools. Confirm the spool dimensions and filament path before using an automatic material system or enclosed feeder.
Which printers can use this 1.75mm filament?
It is intended for most open-material 1.75mm FDM/FFF printers, including common Bambu Lab, Prusa, Creality and Flashforge systems. Check the printer’s supported filament diameter, spool clearance and feed path before production printing.
What nozzle and bed temperatures should I start with?
Start at 210–225°C for the nozzle and 50–60°C for the bed. A practical initial print speed is 40–70 mm/s. Run a short calibration print and slow the outer walls to 30–45 mm/s when the silk surface finish is the priority.
What applications are best suited to this dual-color silk PLA?
It is positioned for decorative vessels, lattice models, figurines, sculptural pieces, awards, desk accessories and display models. It is not positioned as an engineering filament for high-load or high-temperature service.
What is the MOQ for neutral and OEM orders?
Neutral packaging starts at 50 rolls. OEM packaging is typically arranged for 500–1,000 rolls, with the final quantity depending on the approved label, box and packaging requirements.
Can qualified buyers request samples?
Qualified B2B buyers can apply for up to 3 complimentary sample spools for product and printer evaluation. Sample freight is paid by the buyer. Share your printer model, target application and delivery country when requesting samples.
What are the lead time and payment terms?
Standard orders are scheduled for 7–15 days and customized orders for 15–25 days. T/T is accepted for orders with 30% deposit and 70% balance before shipment. PayPal is available for small trial orders; L/C is considered for evaluated large-volume customers.
Source Black & Purple Dual-Color Silk PLA for Your Product Range
Send us your target quantity, destination market and packaging requirements. We will match the sample route, product specification and wholesale or private-label order plan to your market.



Related products
-

Pure White PLA+ Filament by SSSray – Filament PLA+ Biały for Detailed Architectural & Display Models, Low-Sheen 3D Printer Filament
-
Dual Color Silk PLA Filament 1.75mm 1kg – Blue-Green Gradient High-Gloss 3D Printer Material for Decorative Models
-
SSSray PLA Signage Grade 3D Printing Filament – Translucent & Solid 1kg (Custom OEM & Wholesale)
-
SSSray PLA+ in Jet Black: 3D Printer Filament for Electronics Enclosures & Fan Grilles – PLA+ Filament Schwarz