Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

SSSray Silk PLA Series | Lengthwise Tri-Color Gradient | Factory-Direct Wholesale & OEM / ODM
SSSray Onyx Black, Crimson Red & Golden Yellow Tri-Color Silk PLA 3D Printer Filament for Decorative Sculptures – filament PLA jedwabny trójkolorowy
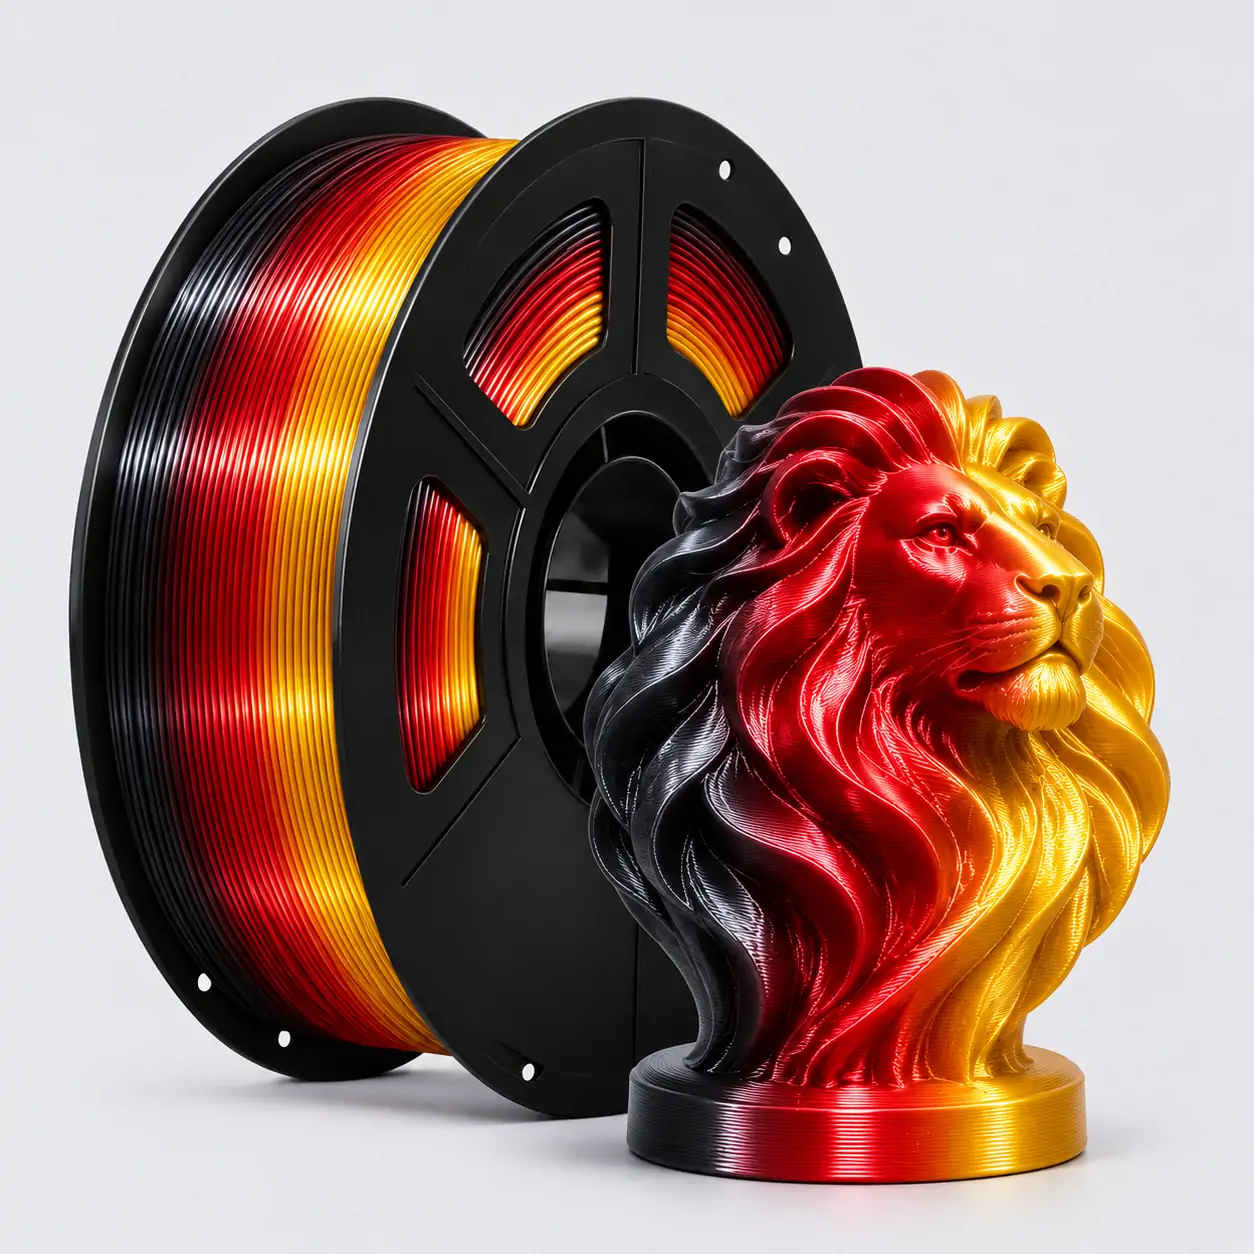
High-gloss Silk PLA with an Onyx Black → Crimson Red → Golden Yellow lengthwise gradient for sculptures, busts, trophies and premium display models.
Print a progressive black-to-red-to-gold color story from one 1.75mm Silk PLA spool. As the filament advances, the gradient moves through Onyx Black, Crimson Red and Golden Yellow, creating successive color bands on suitable print heights without a multi-material color-change system. SSSray manufactures this 1kg plastic-spool SKU in Jinhua, Zhejiang, China for global wholesalers, importers, distributors and private-label brands, with neutral-packaging orders from 50 rolls and OEM packaging programs typically from 500–1,000 rolls.
MaterialSilk PLA
SeriesTri-Color Contrast
Color EffectBlack → Red → Gold Gradient
Diameter1.75mm
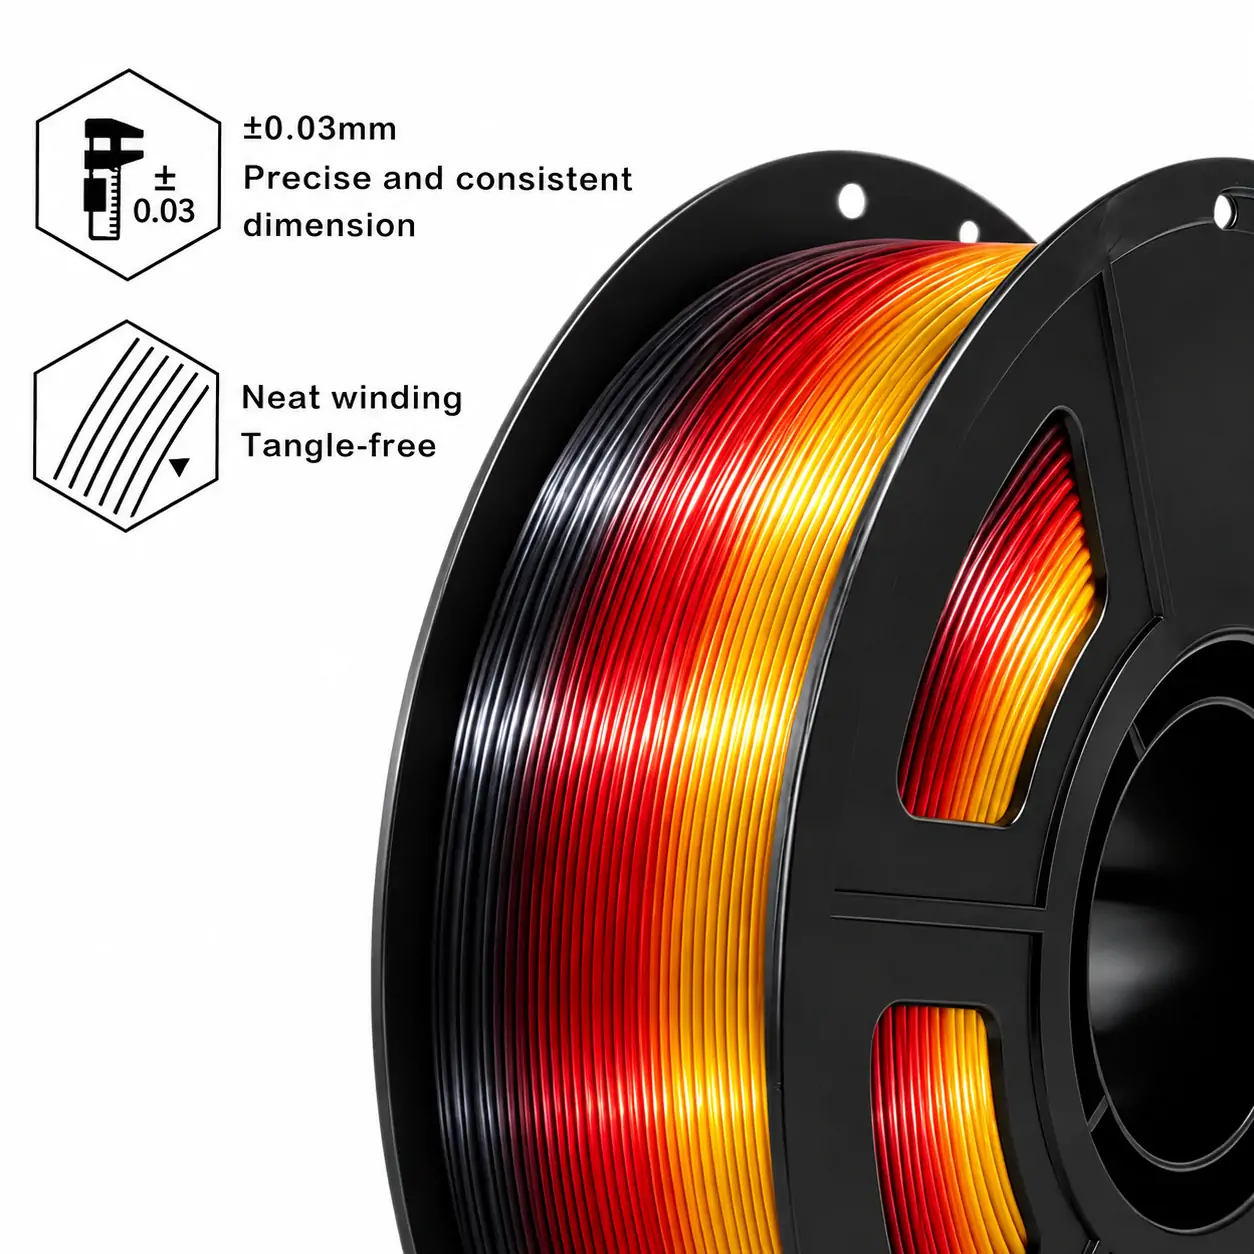
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp.205–215°C standard
Bed Temp.50–60°C
Print Speed50–100mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time: Standard orders 7–15 days; customized orders 15–25 days after specification confirmation.
Product Overview
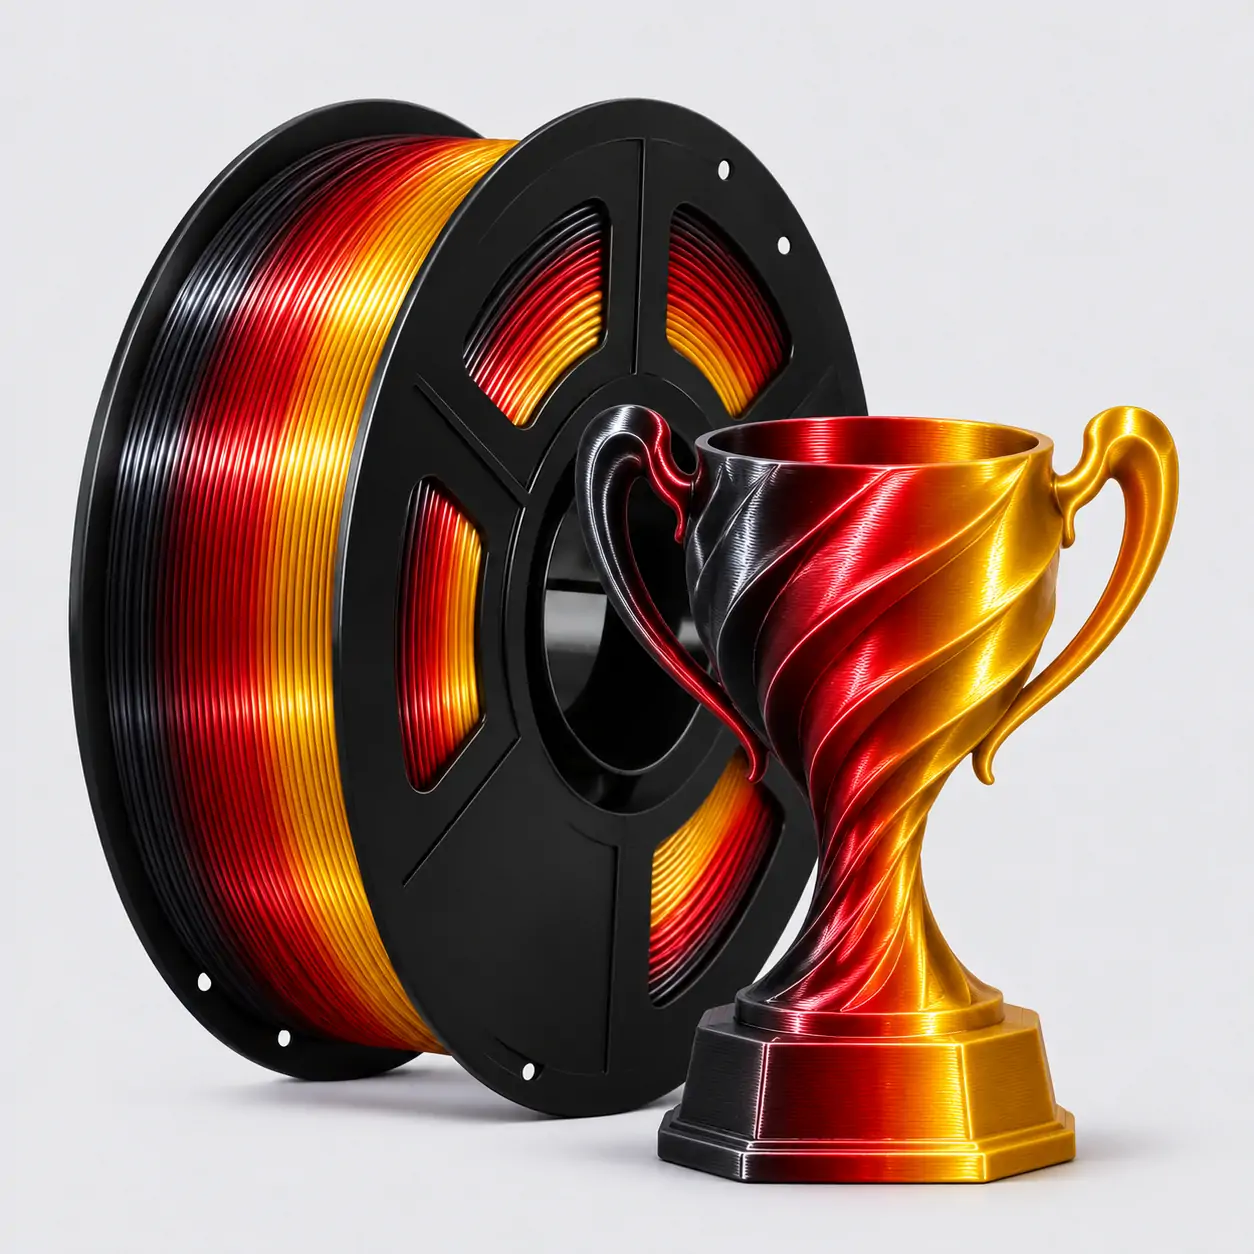
SSSray Onyx Black, Crimson Red & Golden Yellow Tri-Color Silk PLA is an FDM/FFF filament with a continuous, smooth color gradient running along the filament length. The color transitions progressively from Onyx Black through Crimson Red to Golden Yellow as the spool feeds. It is not a three-color side-by-side filament cross-section. On suitable models, the gradual transition appears across successive layers, while the high-gloss Silk PLA finish brings out sculptural contours, relief details and curved surfaces. The colorway is suited to lion busts, trophies, commemorative sculptures, collectible figures and decorative display pieces.
Manufactured by SSSray in Jinhua, Zhejiang, China, this SKU is supplied on a plastic spool with 1.75mm diameter, ±0.03mm stated tolerance, 1kg net filament weight and vacuum-sealed packaging with desiccant. Neutral-packaging orders start from 50 rolls; OEM packaging programs typically start from 500–1,000 rolls. For the intended color placement, select a model with sufficient height and check the slicer’s material-consumption estimate before printing.
Why This Tri-Color Silk PLA Stands Out
The continuous black-to-red-to-gold transition gives a single-spool decorative print a changing appearance without requiring filament swaps or a multi-material unit. Because the gradient follows filament consumption, its position in the finished model depends on the model’s height, geometry and extrusion path. The glossy surface adds reflected highlights to raised details and curved walls, making this colorway particularly effective on display pieces with broad, visible outer surfaces.
Key Selling Points
Lengthwise Black-to-Red-to-Gold Gradient
The continuous gradient follows the filament length and develops progressively across successive layers as the spool feeds.
High-Gloss Silk Surface
The reflective finish highlights raised contours, curved shells and sculptural details on display prints.
Single-Spool Color Progression
One spool delivers the three-stage sequence through a standard single-extruder workflow; no multi-material change system is required for the built-in gradient.
Made for Vertical Display Models
Tall busts, trophy forms, columns and ornaments give the color progression room to develop across print height.
1.75mm / ±0.03mm Supply Specification
The standard 1.75mm format and stated ±0.03mm tolerance support mainstream FDM/FFF product assortments.
Factory-Direct B2B & OEM Supply
Neutral packaging from 50 rolls and OEM packaging programs typically from 500–1,000 rolls support wholesale launches and private-label expansion.
Wholesale Positioning for Distributors & Private-Label Brands
The black-red-gold gradient gives distributors a distinct decorative Silk PLA option for sculpture, trophy and giftware assortments. One spool carries the continuous color transition, so the finished effect can be demonstrated on a single-extruder printer without manual filament changes. Tall models with broad outer surfaces provide the clearest display of the gradual transition.
SSSray supplies this 1kg SKU for wholesale and private-label programs. Neutral packaging starts from 50 rolls, while OEM packaging typically starts from 500–1,000 rolls, subject to the approved artwork and packaging configuration. Quotations are prepared against the requested quantity, packaging plan and FOB Ningbo / EXW shipping terms.
How We Work
1
Requirement Review
Confirm target market, annual volume, color effect, spool and packaging needs.
2
Specification Approval
Confirm diameter, tolerance, net weight, gross weight and document requirements.
3
Sample Evaluation
Review print appearance, color transition, feeding and packaging before bulk approval.
4
Packaging & Artwork
Approve neutral labels or OEM artwork, carton marks and barcode details.
5
Bulk Production
Arrange production against the approved SKU specification and order terms.
6
Final QC & Shipment
Complete agreed inspection and packing checks, then coordinate FOB Ningbo or EXW shipment.
Material Comparison Guide
| Material | Typical Appearance | Typical Nozzle / Bed Range | Material Behavior | Typical Applications |
|---|---|---|---|---|
| SSSray Tri-Color Silk PLA | High-gloss lengthwise gradient: Onyx Black → Crimson Red → Golden Yellow | Nozzle 200–230°C / Bed 50–60°C | PLA-based decorative filament; color progression follows filament consumption, while controlled outer-wall speed preserves a more even silk sheen. | Decorative busts, trophies, commemorative sculptures and display models |
| Standard PLA | Matte to semi-gloss, depending on formulation | Nozzle 190–220°C / Bed 45–60°C | Easy-processing general-purpose material with low shrinkage in typical desktop FDM use. | Prototypes, figures, education and general models |
| PETG | Glossy to translucent, depending on grade | Nozzle 230–250°C / Bed 70–90°C | Generally more ductile than PLA; moisture control and stringing management are important. | Functional parts, brackets, containers and practical components |
| ABS / ASA | Matte to satin, depending on grade | Nozzle 240–260°C / Bed 90–110°C | Higher-temperature processing; enclosure and warping control are commonly important. | Engineering housings, durable parts and outdoor-oriented ASA components |
These are typical material-family processing ranges. Use the selected grade’s print profile and follow the printer and build-plate manufacturer’s operating limits.
Technical Specifications
| Product Name | SSSray Onyx Black, Crimson Red & Golden Yellow Tri-Color Silk PLA 3D Printer Filament for Decorative Sculptures – filament PLA jedwabny trójkolorowy |
|---|---|
| Material | Silk PLA (Polylactic Acid) – FDM / FFF 3D printing filament |
| Product Series | SSSray Silk PLA Series – Tri-Color Contrast Collection |
| Color / Effect | Onyx Black → Crimson Red → Golden Yellow; high-gloss lengthwise gradient |
| Color Structure | Sequential color progression along the filament length; each color feeds in order as the spool advances |
| Filament Diameter | 1.75mm standard; 2.85mm available for selected production programs on request |
| Diameter Tolerance | ±0.03mm |
| Net Weight | 1kg per spool |
| Gross Weight | 1.3kg per spool |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Recommended Nozzle Temperature | 205–215°C at 50–100mm/s; 215–230°C for calibrated high-speed printing |
| Recommended Bed Temperature | 50–60°C |
| Recommended Print Speed | 50–100mm/s standard; 100–200mm/s on calibrated high-speed FDM systems |
| Outer-Wall Speed | 30–50mm/s for a consistent silk gloss |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, subject to hotend, extruder and spool fit |
| Typical Applications | Decorative sculptures, busts, trophies, commemorative models, display figures and gift products |
| MOQ | Neutral packaging: 50 rolls; OEM packaging: typically 500–1,000 rolls |
| Lead Time | Standard: 7–15 days; customized: 15–25 days |
| Trade Terms | FOB Ningbo / EXW |
| Technical Documents | TDS, SDS/MSDS and batch COA support for qualified wholesale / OEM orders; applicable compliance documents confirmed by market and order scope |
Recommended Print Settings
| Parameter | Recommended Value | Usable / Adjustment Range |
|---|---|---|
| Nozzle Temperature | 205–215°C at 50–100mm/s | 200–230°C; use 215–230°C when increasing speed toward 100–200mm/s |
| Build Plate Temperature | 50–60°C | Follow the build-plate manufacturer’s temperature and surface limits |
| Unheated Build Plate | Heated bed preferred | For unheated surfaces, use a suitable adhesion aid and verify first-layer bonding |
| Standard Print Speed | 50–100mm/s | 40–100mm/s for regular desktop profiles |
| High-Speed Printing | 100–200mm/s | Use a high-flow hotend and calibrate temperature, flow rate and cooling before production |
| Outer-Wall Speed | 30–50mm/s | 30–60mm/s; use the lower end for maximum silk gloss and fine sculpture surfaces |
| Retraction – Bowden | 3–5mm | Adjust to Bowden tube length and hotend design |
| Retraction – Direct Drive | 0.8–1.2mm | 0.5–1.5mm; tune in small increments to control stringing |
| Retraction Speed | 30–40mm/s | 30–50mm/s according to extruder response |
| Layer Height | 0.16–0.20mm | 0.12–0.30mm; use 0.12–0.16mm for detailed busts and reliefs |
| Cooling Fan | 80–100% after initial layers | 50–100% according to overhangs, bridges and layer bonding |
| Wall Count | 2–3 walls for decorative models | 2–4 walls according to shell design and part dimensions |
| Infill | 15–20% for decorative models | 40–60% for thicker display parts requiring additional internal support |
| First-Layer Speed | 20–30mm/s | 15–30mm/s according to build surface and first-layer adhesion |
| Bed Adhesion | Clean smooth or textured PEI | Suitable glass surfaces with a compatible adhesive / release layer where required |
| Nozzle Diameter | 0.4mm | 0.4–0.6mm; recalibrate line width and flow for other nozzle sizes |
For a premium Silk finish, keep visible outer walls steady at 30–50mm/s. Raise internal and infill speeds only after flow calibration on the target printer.
Print Optimization Guide
| Print Objective | Printing Guidance |
|---|---|
| Plan the Black → Red → Gold Transition | Choose a model with sufficient Z-height and preview the slicer’s material-consumption estimate so the color sequence develops across the intended display area. |
| Bring Out the Silk Gloss | Keep visible outer walls at a steady 30–50mm/s; avoid abrupt speed changes across prominent surfaces. |
| Print Fine Sculpture Detail | Use a 0.4mm nozzle and 0.12–0.16mm layer height for facial details, reliefs and fine contours. |
| Run at Higher Production Speed | Start at 50–100mm/s; move toward 100–200mm/s only after tuning nozzle temperature, flow rate and cooling for the printer. |
| Reduce Stringing | Keep filament dry, tune retraction in small steps and avoid excessive nozzle temperature during travel moves. |
| Secure the First Layer | Clean the PEI surface, set the bed to 50–60°C and use a 20–30mm/s first-layer speed. |
| Protect the Silk Surface After Printing | Reseal the spool with desiccant or return it to a dry filament storage box between print jobs. |
Printer Brand Starting Settings
| Printer Ecosystem | Nozzle Temperature | Bed Temperature | Outer Wall / General Speed | Setup Notes |
|---|---|---|---|---|
| Bambu Lab | 205–220°C | 50–60°C | 30–40 / 50–100mm/s | Keep outer walls near 40mm/s for silk sheen; calibrate flow and maximum volumetric speed before using the 100–200mm/s high-speed range. |
| Prusa | 205–220°C | 50–60°C | 35–50 / 50–100mm/s | Start with a PLA profile, run a temperature check and use a clean PEI sheet with a tuned first layer. |
| Creality | 200–220°C | 50–60°C | 35–50 / 40–80mm/s | Confirm Bowden or Direct Drive before setting retraction; K1-class high-speed systems require flow and temperature calibration before increasing speed. |
| Anycubic | 205–220°C | 50–60°C | 35–50 / 50–100mm/s | Use a 0.4mm nozzle profile first; tune flow, cooling and first-layer adhesion for the selected build plate. |
| Flashforge | 205–230°C | 50–60°C | 35–50 / 50–150mm/s | For high-speed models, raise temperature within the recommended range and validate extrusion flow before moving toward 200mm/s. |
Use these SSSray starting profiles for common 0.4mm FDM configurations. Set the final speed according to the printer’s hotend capacity, maximum volumetric flow, cooling and slicer preview.
Applications
| Application Focus | Practical Notes |
|---|---|
| Decorative Sculptures & Lion Busts | Taller sculptural forms let the black-to-red-to-gold sequence develop across successive layers while the silk sheen highlights raised facial details and contours. |
| Trophies, Awards & Commemorative Models | Use vertical trophy bodies, award columns and commemorative forms to showcase the progressive color transition in a single print. |
| Collectibles & Figurines | The reflective surface and changing color bands create a distinctive presentation for display figures and collector editions. |
| Giftware & Home Décor | Suitable for statement ornaments, desk décor, seasonal pieces and customized decorative products. |
| Cosplay Accessories & Display Props | Useful for decorative trims, emblems, badges and presentation props where color progression and surface finish are key design features. |
| Education & Creative Workshops | Demonstrates how filament length, material consumption, model height and slicer paths influence gradient placement in FDM printing. |
Storage Guide
- Keep each spool in its original vacuum-sealed bag until it is ready for printing.
- After opening, reseal the bag with the supplied desiccant or transfer the spool to a dry filament storage box.
- Store in a cool, dry area away from direct sunlight, heaters and temperature extremes; keep the storage container sealed between jobs.
- If stringing, popping or surface defects indicate moisture uptake, dry the filament at approximately 50°C for 6–8 hours in a controlled filament dryer, observing the spool’s heat tolerance.
- For repeatable Silk PLA gloss, keep the filament protected from ambient humidity during printing breaks and long-term storage.
OEM / ODM Services
SSSray manufactures 3D printing filament in Jinhua, Zhejiang, China and supports wholesale, OEM and private-label programs from extrusion through finished packaging. For this black-to-red-to-gold lengthwise-gradient Silk PLA, we coordinate the product presentation around one defined color sequence so the spool, retail box, barcode and export carton carry a consistent SKU identity.
Private-Label Identity
Custom logo labels, product names, SKU codes, barcodes and multilingual retail packaging artwork.
Packaging & Spool Presentation
Neutral packaging, branded retail boxes, spool labels, carton marks and project-specific packing plans.
Product & Color Program
Confirm the 1.75mm specification, spool format, approved black-red-gold gradient reference and packaging configuration for repeat orders.
MOQ: Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls, depending on artwork, packaging components and order configuration. SSSray coordinates sample evaluation and packaging approval before bulk production.
Explore our OEM / ODM manufacturing service for private-label project planning.
Quality Control
At SSSray, quality control is built into extrusion, spooling and export packing—not added as a final visual check. Our factory combines inline laser measurement, moisture testing, color-reference verification, print sampling and batch traceability to support repeatable wholesale and OEM supply.
- Inline Dual-Axis Laser Monitoring: Optical micrometers continuously monitor filament diameter and ovality. Out-of-tolerance sections are automatically cut and purged to support the stated ±0.03mm diameter control.
- Moisture Control & Karl Fischer Testing: Material drying and dehumidification are followed by moisture testing before vacuum sealing, helping control moisture-related extrusion and surface defects.
- Color Reference Verification: Spectrophotometer Delta E records compare production lots with approved color references. For this SKU, the approved sequence is Onyx Black → Crimson Red → Golden Yellow.
- Spool Winding & Visual Inspection: Our production checks cover winding condition, spool integrity, filament appearance and batch identification before packing.
- Print-Farm Validation: Representative spools undergo extended printing checks, including continuous 24-hour runs on selected Bambu Lab, Creality and Voron platforms.
- Batch Traceability & COA: Batch coding and spool-level traceability connect production records with final inspection. Batch COA documentation supports qualified wholesale and OEM orders.
Review our Batch QC Data & COA and 3D Printer Filament Test Protocol for the factory quality-control process.
Compliance & Technical Documentation
For wholesale and OEM orders, SSSray provides product technical files and batch documentation matched to the selected material and order. Our team confirms the applicable TDS, SDS/MSDS, COA and destination-market compliance requirements with your quotation.
| Document / Requirement | SSSray Documentation Support |
|---|---|
| TDS – Technical Data Sheet | Technical specifications and recommended processing guidance for the selected material grade. |
| SDS / MSDS | Safety information for the supplied material and destination-market review. |
| COA – Certificate of Analysis | Batch-related quality records and measured production data for qualified wholesale / OEM orders. |
| RoHS / REACH | Applicable declarations or laboratory reports supplied according to the material formulation and destination-market scope. |
| CE | CE marking is assessed against applicable product legislation; it is not a generic certification for 3D printer filament as a material. |
| SGS / Third-Party Reports | Third-party testing can be arranged when a buyer requires a defined test scope and destination-market evidence. |
Tell our sales team your destination country and document requirements at RFQ stage so the correct file set can be aligned with the order.
Frequently Asked Questions
What is the MOQ for this tri-color Silk PLA?
Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls, depending on the approved label, box and packaging configuration.
What are the standard product specifications?
The standard SKU is 1.75mm diameter, ±0.03mm tolerance and 1kg net weight on a plastic spool. Gross weight is 1.3kg per spool.
Which printers can use this filament?
It is designed for most open-material 1.75mm FDM/FFF printers, including Bambu Lab, Prusa, Creality, Anycubic, Elegoo and Flashforge systems. Match the spool fit, extruder path, hotend and slicer profile to the exact printer model.
What print settings should I start with?
Start at 205–215°C nozzle temperature, 50–60°C bed temperature and 50–100mm/s print speed. Keep visible outer walls around 30–50mm/s for silk gloss. Calibrated high-speed systems can be tuned toward 100–200mm/s with 215–230°C nozzle temperature.
How does the black, red and gold gradient work?
The colors run along the filament length in sequence: Onyx Black, then Crimson Red, then Golden Yellow. They feed one after another as the spool advances; the three colors are not arranged side by side across the same filament cross-section.
How can I make the color transition more visible?
Choose a model with sufficient height and continuous material consumption, such as a bust, trophy column or vertical ornament. Preview the slicer’s material-consumption estimate and layer view to plan where the transition is likely to appear; the final placement follows model geometry and extrusion path.
Can I request samples before a bulk order?
Approved B2B qualification customers may receive up to 3 complimentary sample rolls after review. Sample combination and freight arrangements are confirmed during the inquiry.
Can SSSray provide private-label packaging and technical documents?
Yes. OEM/ODM programs cover logo labels, retail boxes, carton marks, SKU and barcode information, multilingual artwork and spool presentation. TDS, SDS/MSDS and batch COA support is available for qualified wholesale/OEM orders; applicable compliance documents are confirmed by material and destination market.
Source Black-to-Red-to-Gold Silk PLA Direct from SSSray
Add a lengthwise-gradient Silk PLA SKU to your decorative filament range. SSSray supplies the Onyx Black → Crimson Red → Golden Yellow 1.75mm / 1kg format for wholesale and private-label programs, with sample qualification, factory batch-quality support and OEM packaging. Send us your target quantity, destination and packaging requirements for a factory-direct quotation.



Related products
-

Dual Color Gradient Crystal PLA Filament 1.75mm 1kg – Translucent Two-Tone Finish for FDM 3D Printing, Ideal for Artistic Decor & Jewelry Prototypes
-
Pastel Rainbow PLA Filament 1.75mm 1kg – Smooth Color Transition Multicolor PLA for FDM 3D Printing, Ideal for Creative Decor & Designer Toys
-
Pure White PLA+ Filament by SSSray – Filament PLA+ Biały for Detailed Architectural & Display Models, Low-Sheen 3D Printer Filament
-
SSSray PLA+ Filament in Lagoon Teal for Decorative Vases & Desk Organizers – Sợi in 3D PLA+ Xanh Ngọc, Satin-Finish 3D Printer Filament