Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

ABS Standard Series | Electronics Components | OEM / ODM Supply
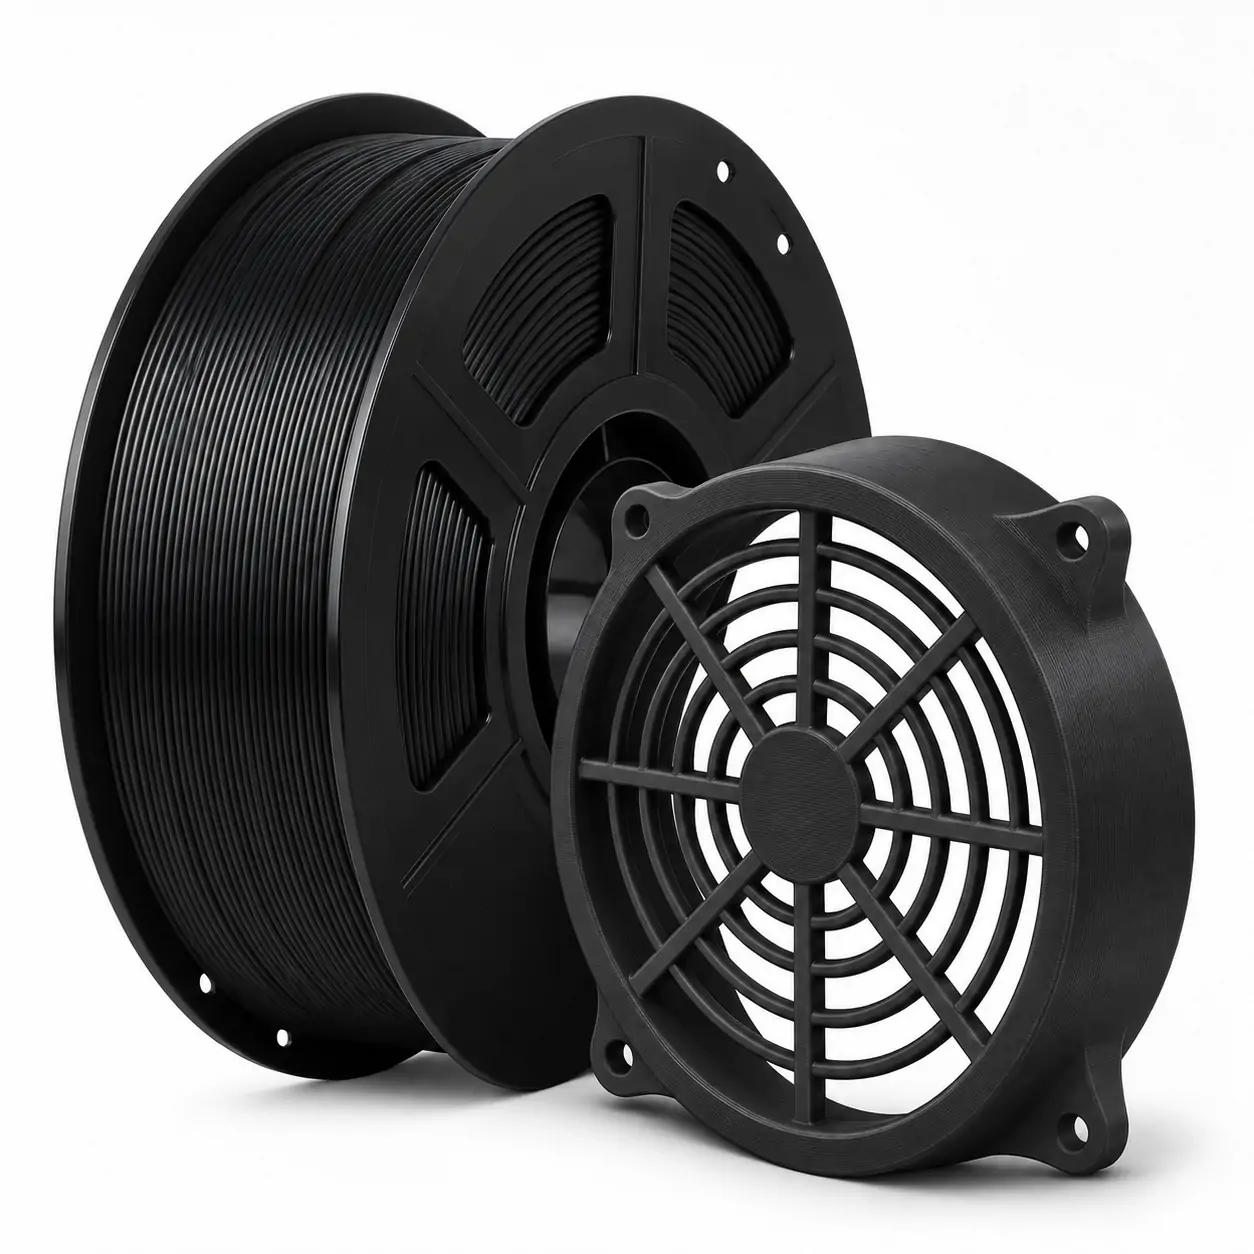
SSSray Deep Black ABS 3D Printer Filament for Fan Guards & Electronics Housings – Filamen ABS Hitam
We manufacture Deep Black ABS for ventilated fan guards, precise electronics housings and repeatable B2B engineering-filament supply.
Specify a uniform low-sheen black finish with 1.75mm ±0.03mm diameter control, typical 40 ± 2 MPa XY tensile strength and up to 250 mm/s within our ABS process window. We handle samples, private-label packaging and export replenishment from the same supply team.
Get Bulk QuoteMaterialABS
SeriesABS Standard
Color EffectDeep Black · Satin
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp220–240°C
Bed Temp90–100°C
Print Speed60–150 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 days; customized orders typically 15–25 days.
Product Overview
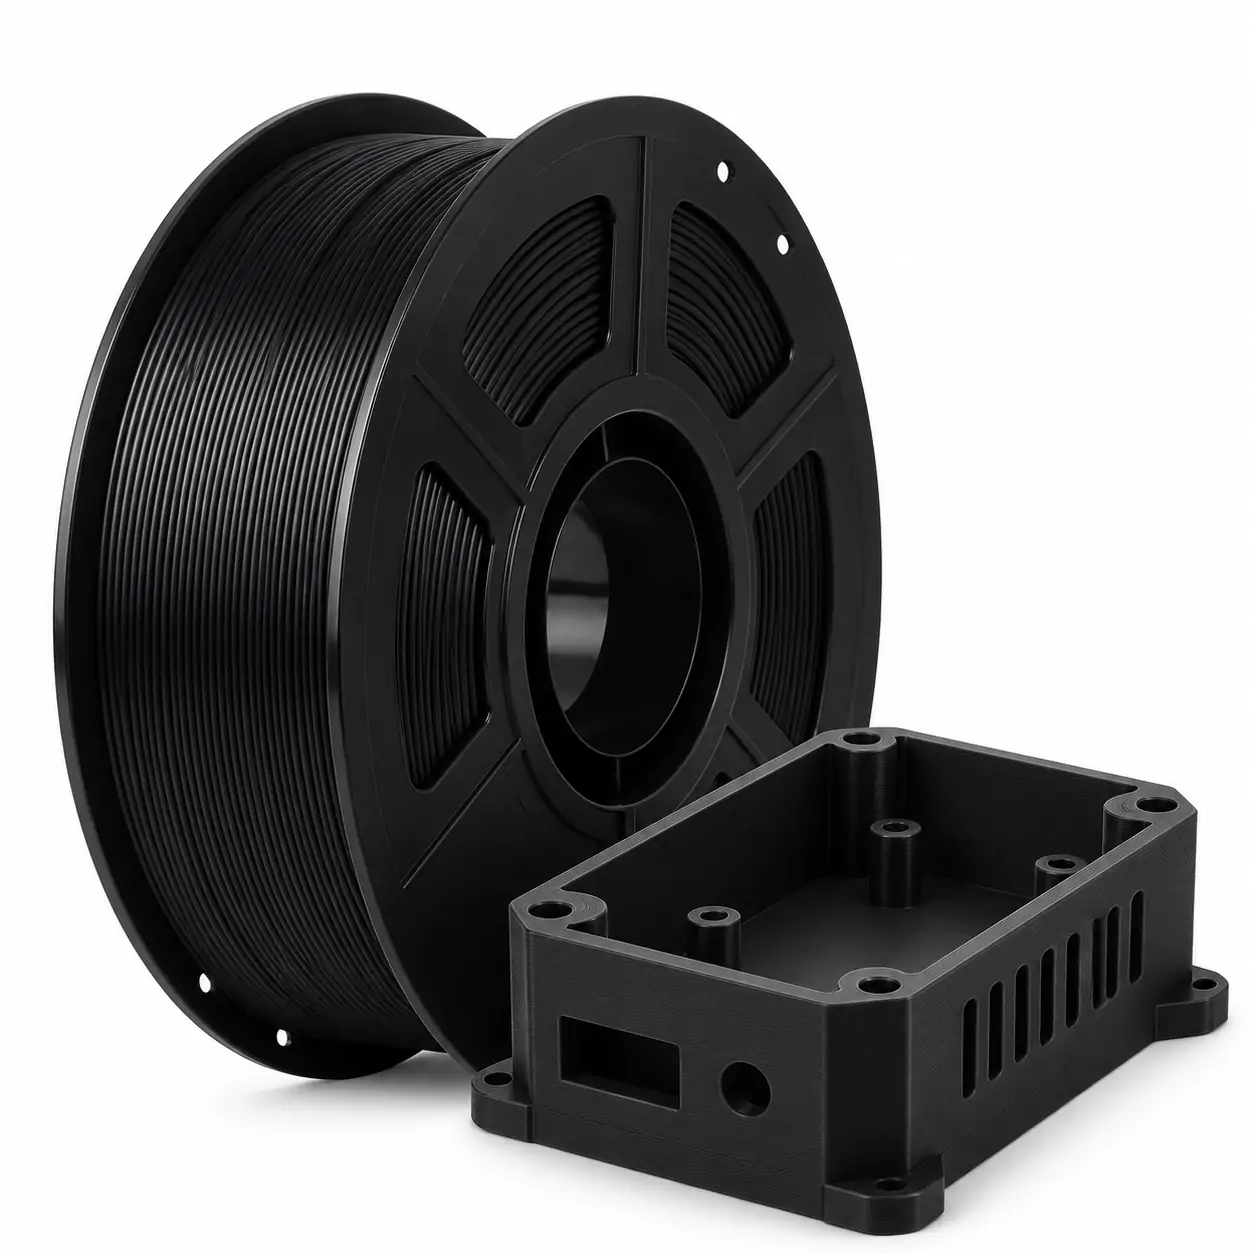
We manufacture SSSray Deep Black ABS for ventilation grilles, fan guard frames, indoor electronics housings and functional FDM/FFF components. Its uniform neutral black pigment and smooth satin finish give airflow slots, screw bosses, ribbing and mating enclosure edges a coherent technical appearance. Standard ABS offers higher heat resistance than PLA and responds well to drilling, sanding, machining and controlled solvent finishing. This makes Deep Black a practical indoor engineering grade for distributors and OEM teams serving maintenance, workshop and electronics-accessory buyers.
Our 1.75mm ±0.03mm filament comes on a 1kg plastic spool, vacuum sealed with desiccant. For everyday enclosed-printer production, we recommend 60–150 mm/s; the broader 40–250 mm/s process window supports further tuning on suitable equipment and geometries. Typical printed-specimen data include XY tensile strength of 40 ± 2 MPa and heat deflection temperature of 98°C at 0.455 MPa. We help you qualify fine vents, fastener locations and heat-set inserts, then move into neutral packaging from 50 spools or private-label production with approved artwork. Our export team handles repeat-order planning and FOB Ningbo or EXW shipment.
Why This Product Stands Out
Built for deep-black vented hardware: We match a low-sheen neutral black appearance with the heat capability and post-processing freedom of standard ABS. Your customers can print airflow openings, removable guards, controller-case shells and fitted fastener features in a single consistent finish. Our documented 40–250 mm/s process window, published XY mechanical values and 50-spool neutral MOQ give purchasing teams the parameters to plan material qualification and repeat orders.
Key Selling Points
Uniform Deep Black Satin
We target a neutral low-sheen finish on vent ribs, curved guard rings and case walls, without metallic or colour-shift effects.
Productive ABS Print Window
Our 60–150 mm/s everyday profile balances enclosure detail and throughput; suitable enclosed systems can tune within 40–250 mm/s.
Heat & Mechanical Capability
Our typical printed-specimen data show XY tensile strength of 40 ± 2 MPa and HDT of 98°C at 0.455 MPa.
Made for Vented Geometry
Print fan-guard lattices, removable access panels and precision screw-boss areas, then drill or finish the ABS shell as required.
Controlled Feed & Packing
We supply 1.75mm ±0.03mm filament on 1kg plastic spools with neat winding, vacuum sealing and desiccant for export handling.
Factory OEM / ODM Supply
Start with 50 neutral spools or plan 500–1,000-spool private-label packaging with our artwork, sampling and Ningbo export team.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| Low-Sheen Deep Black Pigmentation | Coordinate vented faces, fan-guard rings and fastening details across one hardware assortment |
| 40 ± 2 MPa XY Tensile Strength | Numerical material benchmark for printed enclosure and mechanical-prototype qualification |
| 98°C HDT at 0.455 MPa | Practical heat-deflection reference for selecting indoor equipment grades |
| 0.16–0.24mm Functional Layer Height | Refine narrow grille openings, controlled outer walls and heat-set insert pilot geometry |
| 1.75mm ±0.03mm Filament | Defined procurement and incoming-diameter tolerance for repeat-order consistency |
| 1kg Vacuum-Sealed Spool | Dry-packing format for wholesale stocking, print farms and private-label retail units |
| Neutral 50-Spool MOQ / Custom Packaging | Qualify the market first, then scale labels, boxes and barcodes with our OEM team |
Balanced Quality and Cost Efficiency
We help distributors sell a repeatable black ABS SKU across fan-guard, controller-housing and equipment-spare-part programs without splitting inventory into several appearance variants. Neutral supply starts at 50 spools; approved private-label programs normally run 500–1,000 spools. Our standard export carton holds 10 individually protected 1kg units, with an approximately 14 kg carton reference for logistics planning. Buyers can qualify one spool profile, align the Deep Black finish with their hardware range and reorder through our established carton and Ningbo shipping arrangements.
How We Work
1
Usage & Volume Review2
ABS Specification Confirmation3
Sample & Printer Qualification4
Packaging & Artwork Approval5
Order Scheduling & QC6
Inspection & Export DispatchMaterial Comparison Guide
| Material | Material Behaviour | Printing Conditions | Typical Application | Selection Note |
|---|---|---|---|---|
| SSSray Deep Black ABS Standard | Typical XY tensile strength 40 ± 2 MPa; HDT 98°C at 0.455 MPa; workable post-processing | Enclosed FDM; 90–100°C bed; low cooling | Indoor fan guards, ventilated controller housings, screw-boss parts | Choose for heat-capable indoor hardware with a uniform satin-black finish |
| SSSray Jet Black PLA+ | Lower thermal resistance; simpler dimensional and first-layer control | Lower nozzle/bed temperatures; open printers commonly used | Display enclosures, fit checks, general-purpose grilles | Choose for easy production when elevated heat performance is unnecessary |
| SSSray Jet Black ABS-FR | Separate flame-retardant formulation; specify required test class and thickness | Enclosed ABS-capable printer; grade-specific profile | Housing projects with defined flame-performance requirements | Ask us for the matching ABS-FR grade and its project documents |
| ASA | ABS-family mechanical behaviour with better UV/weathering resistance | Enclosed FDM; heated bed and controlled cooling | Exterior covers, outdoor brackets and weather-exposed parts | Choose for sustained sunlight and outdoor service |
| PETG | Lower shrinkage and warp tendency than ABS; softer thermal response | Heated bed; enclosure commonly optional | General workshop covers, fixtures and low-heat housings | Choose when bed adhesion and dimensional ease take priority |
Technical Specifications
| Product Name | SSSray Deep Black ABS 3D Printer Filament for Fan Guards & Electronics Housings – Filamen ABS Hitam |
|---|---|
| Material | Acrylonitrile Butadiene Styrene (ABS) – FDM/FFF filament |
| Series | SSSray ABS Standard Series – Electronics Housings & Mechanical Components |
| Color / Finish | Deep Black – uniform neutral black; smooth, low-sheen satin finish |
| Filament Diameter | 1.75mm standard; 2.85mm upon project confirmation |
| Diameter Tolerance | ±0.03mm (specified) |
| Roundness Deviation | ≤0.02mm |
| Net Filament Weight | 1kg per standard spool; 3kg / 5kg project options |
| Gross Weight | 1.3kg per packed 1kg unit |
| Spool Type | Plastic spool; alternative spool solutions by project |
| Packaging | Vacuum-sealed bag with desiccant; individual box |
| Surface Appearance | Satin to low-sheen black; appearance depends on part geometry and toolpath |
| Processing Requirement | ABS-capable enclosed printer, heated bed, low part cooling and suitable ventilation |
| Printer Compatibility | Most 1.75mm open-material FDM/FFF printers equipped for ABS temperatures and enclosure printing |
| Primary Applications | Fan guards, ventilated electronics housings, indoor covers, equipment brackets, functional prototypes |
| OEM / ODM | Private-label labels, cartons, colour matching and spool-format discussions |
| Typical XY Tensile Strength | 40 ± 2 MPa (ISO 527-2 / ASTM D638) |
| Typical XY Tensile Modulus | 2,300 MPa (ISO 527-2 / ASTM D638) |
| Typical XY Flexural Strength | 60–70 MPa (ISO 178 / ASTM D790) |
| Typical Notched Izod Impact | 18–28 kJ/m² (ISO 180) |
| Heat Deflection Temperature | 98°C at 0.455 MPa; 88°C at 1.82 MPa (ISO 75-2 / ASTM D648) |
| Glass Transition Temperature | 105.3°C (ISO 11357-2 / ASTM D3418) |
| Typical Test Specimen Setup | XY printed specimens; 0.2mm layer height; 100% infill |
Recommended Print Settings
| Parameter | Recommended Production Profile | Additional Usable / Tunable Range |
|---|---|---|
| Nozzle Temperature | 220–240°C; 230°C routine starting point | 220–260°C; 245–255°C for higher-flow tuning after extrusion and layer-bond checks |
| Heated Bed | 90–100°C; 95°C routine starting point | 90–110°C on rated equipment; use the higher end for large footprints and corner adhesion |
| Print Speed | 60–150 mm/s for routine enclosed-printer production | 40–250 mm/s; use 150–250 mm/s on qualified high-flow paths with controlled cooling |
| Layer Height (0.4mm Nozzle) | 0.16–0.24mm | 0.12–0.30mm; tune for vent-edge detail and wall strength |
| Part Cooling Fan | 0–20% for functional walls; off during first 3 layers | 0–50% for bridges and small features when layer adhesion permits |
| Direct Drive Retraction | 0.8–1.2mm at 25–35 mm/s | Start low and tune for stringing; do not use Bowden distances |
| Bowden Retraction | 2.0–3.0mm at 20–30 mm/s | Tune for path length and hot-end design |
| Perimeter / Wall Count | 3–4 walls | 2 for visual prototypes; 4–5 for thicker mechanical shells |
| Infill | 15–25% for shape trials | 35–60% for higher structural demand after part validation |
| First-Layer Speed | 15–25 mm/s | 15–30 mm/s; tune for plate preparation and first-layer adhesion |
| Build Surface | Smooth/textured PEI with suitable adhesive | Prepared glass or engineering plate with a compatible release layer |
| Brim | 5–10mm on large or corner-heavy parts | Increase only where edge lifting persists |
| Enclosure | Closed chamber; preheat for stable wall adhesion | 50–60°C in rated actively heated chambers; use passive enclosures for compact parts and respect hardware limits |
| Drying if Moisture Affected | 80°C for 4–6h using rated equipment | Remove the spool from heat-sensitive holders; dry only where the equipment is rated for 80°C |
| Ventilation | Use appropriate extraction/filtration | Keep airflow away from the print itself to avoid drafts |
Print Optimization Guide
| Printing Situation | Factory Guidance |
|---|---|
| Vented Fan Guards | We recommend 0.16–0.20mm layers, reinforced mounting rings and strut orientation that keeps airflow openings clean. |
| Electronics Housing Fit | Use a fit coupon for screw bosses, snap features, heat-set inserts and mating edges; allow for standard ABS shrinkage. |
| Deep Black Surface Uniformity | Hold outer-wall speed and nozzle temperature steady across broad case faces; reduce sudden changes that produce uneven gloss. |
| Corner Lifting | Preheat the enclosed build area, clean the plate and use a 5–10mm brim on wide footprints. |
| Layer Splitting | Reduce drafts and part cooling; check bed/chamber thermal stability and, where appropriate, raise nozzle temperature slightly. |
| Holes and Clearances | We use dimensionally representative test coupons to set insert pilots and fan-guard mounting clearances before repeat production. |
| Bridges / Thin Grilles | Use local cooling only where required for geometry; avoid high fan speeds across the entire part. |
| Health & Workspace | Print ABS in an enclosed machine with proper ventilation; keep operators away from unnecessary fume exposure. |
Printer Brand Starting Settings
| ABS-Capable Printer | Nozzle | Bed | Speed | Commissioning Notes |
|---|---|---|---|---|
| Bambu Lab X1 / P1S | 230–245°C | 95–100°C | 60–150 mm/s | Start with an enclosed ABS preset; use 150–250 mm/s only after melt-flow and vent-detail checks |
| Prusa with Enclosure | 230–245°C | 95–100°C | 50–100 mm/s | Use the ABS-compatible PEI surface, preheat enclosure and tune first-layer brim |
| Creality K1 / K1 Max | 230–250°C | 95–100°C | 60–150 mm/s | Keep the bed within the 100°C limit; close the enclosure and check bridge cooling |
| Flashforge ABS-Capable Enclosed Models | 230–245°C | 95–100°C | 60–150 mm/s | Use an ABS-capable enclosed model; extend speed only where hot-end flow and geometry permit |
| Other Enclosed 1.75mm FDM Printers | 225–240°C | 90–100°C | 40–100 mm/s | Check machine hot-end and bed ratings before moving toward the wider print window |
Start with a 0.4mm nozzle and a small qualification part. Adjust the profile to your exact printer, plate, ventilation, geometry and mechanical targets; machine limits always apply.
Performance Characteristics
| Characteristic | Engineering / Material Behaviour | Procurement or Design Note |
|---|---|---|
| Deep Black Finish | Uniform neutral black with a smooth, low-sheen satin appearance | Use stable outer-wall speed for matching fans, frames and controller faces |
| Diameter & Roundness | 1.75mm ±0.03mm; roundness deviation ≤0.02mm | Defined incoming dimensions support consistent feeding and lot qualification |
| XY Tensile Strength / Modulus | 40 ± 2 MPa / 2,300 MPa (ISO 527-2 / ASTM D638) | Typical printed-specimen data for bracket and housing material selection |
| XY Flexural Strength | 60–70 MPa (ISO 178 / ASTM D790) | Useful bend-performance reference for enclosure ribs and mounting features |
| Notched Izod Impact Strength | 18–28 kJ/m² (ISO 180) | Impact-response reference for practical guard and cover prototypes |
| Heat Deflection / Glass Transition | 98°C HDT at 0.455 MPa; 88°C at 1.82 MPa; Tg 105.3°C | Use the specified loading level when comparing heat-performance requirements |
| Post-Processing | Standard ABS supports drilling, sanding, machining and controlled solvent finishing | Refine visible housing edges and heat-set insert openings after printing |
| Printed-Specimen Conditions | XY orientation, 0.2mm layers and 100% infill | Clear test geometry makes our typical engineering values useful for comparison |
Applications
| Application Focus | Practical Notes |
|---|---|
| Fan Guards & Ventilation Grilles | We recommend consistent 0.16–0.20mm layers for thin spokes, accurate fan clearance and a matching satin-black outer ring. |
| Vented Electronics Housings | Print controller shells with cable exits, airflow slots and screw bosses; our ABS profile supports enclosed-machine repeatability. |
| Equipment Covers & Faceplates | Produce neutral black access covers, instrument bezels and replaceable indoor equipment panels with a coordinated finish. |
| Mechanical Brackets & Mounts | Prototype heat-set insert seats, mounting ears and load-bearing geometry using the listed XY mechanical reference values. |
| Maintenance / Spare-Part Prototypes | Check fit, drilled openings and enclosure-temperature conditions before moving from printed trial parts to repeat supply. |
| Wholesale & Private-Label ABS | Stock a defined standard ABS grade for OEM accessory lines, technical retailers, distributor replenishment and print farms. |
Storage Guide
- Keep unopened units in their vacuum-sealed bags with desiccant until needed for production.
- After opening, store the spool with desiccant in a dry box; we recommend a storage area below 50% RH.
- Avoid direct sunlight, sources of heat and prolonged uncontrolled warehouse humidity.
- When moisture affects extrusion, dry at 80°C for 4–6h in a rated dryer or oven, with a heat-safe spool arrangement.
- Retain the product label and delivery batch reference for incoming inspection and repeat-order traceability.
OEM / ODM Services
We supply Deep Black standard ABS to distributors and private-label partners with custom logos, retail box artwork, barcode labels, carton markings and approved packaging layouts. Our commercial team coordinates the black finish sample, package artwork approval, production schedule and carton documents before shipment. We offer 1kg plastic spools as standard, plus project-based 3kg/5kg spool formats and selected 2.85mm production.
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools. Explore private-label filament programs or send us your OEM requirements.
Quality Control
- We control the 1.75mm ±0.03mm diameter specification and ≤0.02mm roundness deviation during production checks.
- We inspect neat winding, spool integrity and filament feed presentation before packing.
- We compare the neutral Deep Black satin appearance against the approved product colour reference.
- We seal individual retail units with desiccant and check the vacuum pack before export-carton loading.
- We coordinate batch identification with purchase-order records for distributor replenishment.
- We check standard carton counts, customer labels and dispatch documents before FOB Ningbo or EXW release.
Compliance & Technical Documents
- We supply technical information for our standard ABS formulation, including mechanical and thermal property references.
- Our team supports SDS/MSDS document requests for importer records and safe material handling.
- Send us your market and required RoHS or REACH documentation list so we can coordinate the matching available evidence.
- For projects specifying a UL94 V-0/V-1/V-2 flame class, ask us about our separate SSSray ABS-FR material options and applicable reports.
- For electrical equipment projects, we can discuss material-grade selection and the test documentation needed for your assembly plan.
Frequently Asked Questions
Why choose Deep Black ABS for fan guards and electronics housings?
We designed this standard ABS offering around precise vent openings, screw-boss geometry and a consistent low-sheen black finish. You gain the heat and post-processing capability of ABS together with our 1kg distributor format and OEM supply service.
Does this ABS need an enclosed 3D printer?
Yes. We recommend an ABS-capable enclosure, a 90–100°C bed and low cooling for repeatable housings and grilles. Ventilate the workspace while keeping cold drafts away from the build.
What nozzle temperature and speed should we start with?
Start near 230°C with a 90–100°C bed and a 0.4mm nozzle. We recommend 60–150 mm/s for everyday production; suitable enclosed systems can tune within our 40–250 mm/s process window. Check melt flow and wall bonding before raising speed.
Which SSSray black grade should we specify for flame-class projects?
Choose this Deep Black standard ABS for general indoor fan guards and vented components. For a specified flame class, we can introduce our separate SSSray ABS-FR range and coordinate the applicable material documentation with your team.
What is the MOQ for bulk and private-label orders?
Neutral packaging starts from 50 spools. OEM packaging typically requires 500–1,000 spools depending on custom labels, artwork and box requirements.
Can we evaluate samples before a wholesale purchase?
Yes. We offer verified B2B buyers up to three complimentary sample spools; the buyer pays freight. Our team can help you review the Deep Black finish, fan-guard detail and printer profile before the wholesale order.
Which diameters and spool sizes do you support?
Standard supply is 1.75mm on a 1kg plastic spool. Selected 2.85mm filament and 3kg/5kg packages are available for discussion against project demand.
What are the export terms, payment method and lead time?
We support FOB Ningbo and EXW. Standard lead time is 7–15 days and customized production is 15–25 days. Our standard T/T terms are 30% deposit and 70% before shipment; PayPal is available for small trial orders.
Looking for a Reliable Deep Black ABS Supplier?
Tell us your destination, spool quantity and enclosure model. We’ll quote our Deep Black ABS, arrange sample qualification and prepare neutral or private-label export packaging for your order.



Related products
-

Engineering Grade PA6/66 Carbon Fiber Reinforced 3D Printing Filament 1.75mm 1kg – High Stiffness Wear Resistant Low Warpage for Metal Replacement Parts
-
PA12-GF Glass Fiber Reinforced Nylon Filament 1.75mm 1kg – Industrial Grade Engineering Polyamide for Structural Manufacturing & Functional Prototyping
-
SSSray PC-ABS 3D Printer Filament Black 1.75mm 1kg
-
Wholesale PC-ABS-FR UL94 V-0 Filament 1kg (1.75mm / 2.85mm) – High-Heat PETG-FR Alternative 3D Printer Filament for Electrical Enclosures & Junction Boxes | OEM Manufacturer