Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM


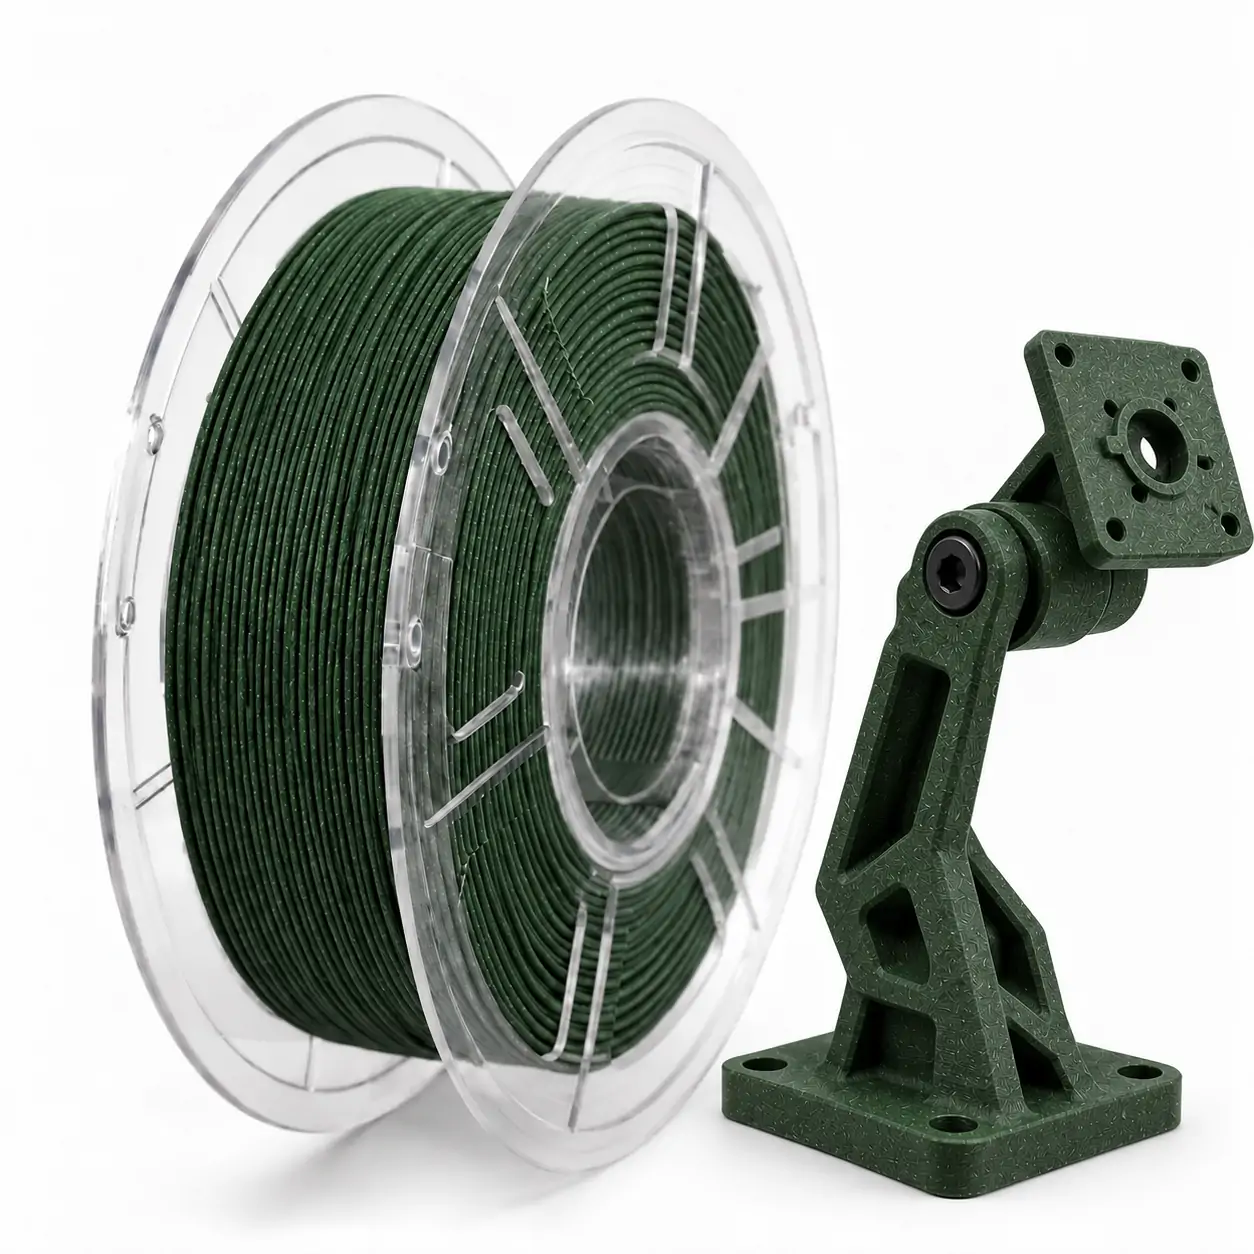

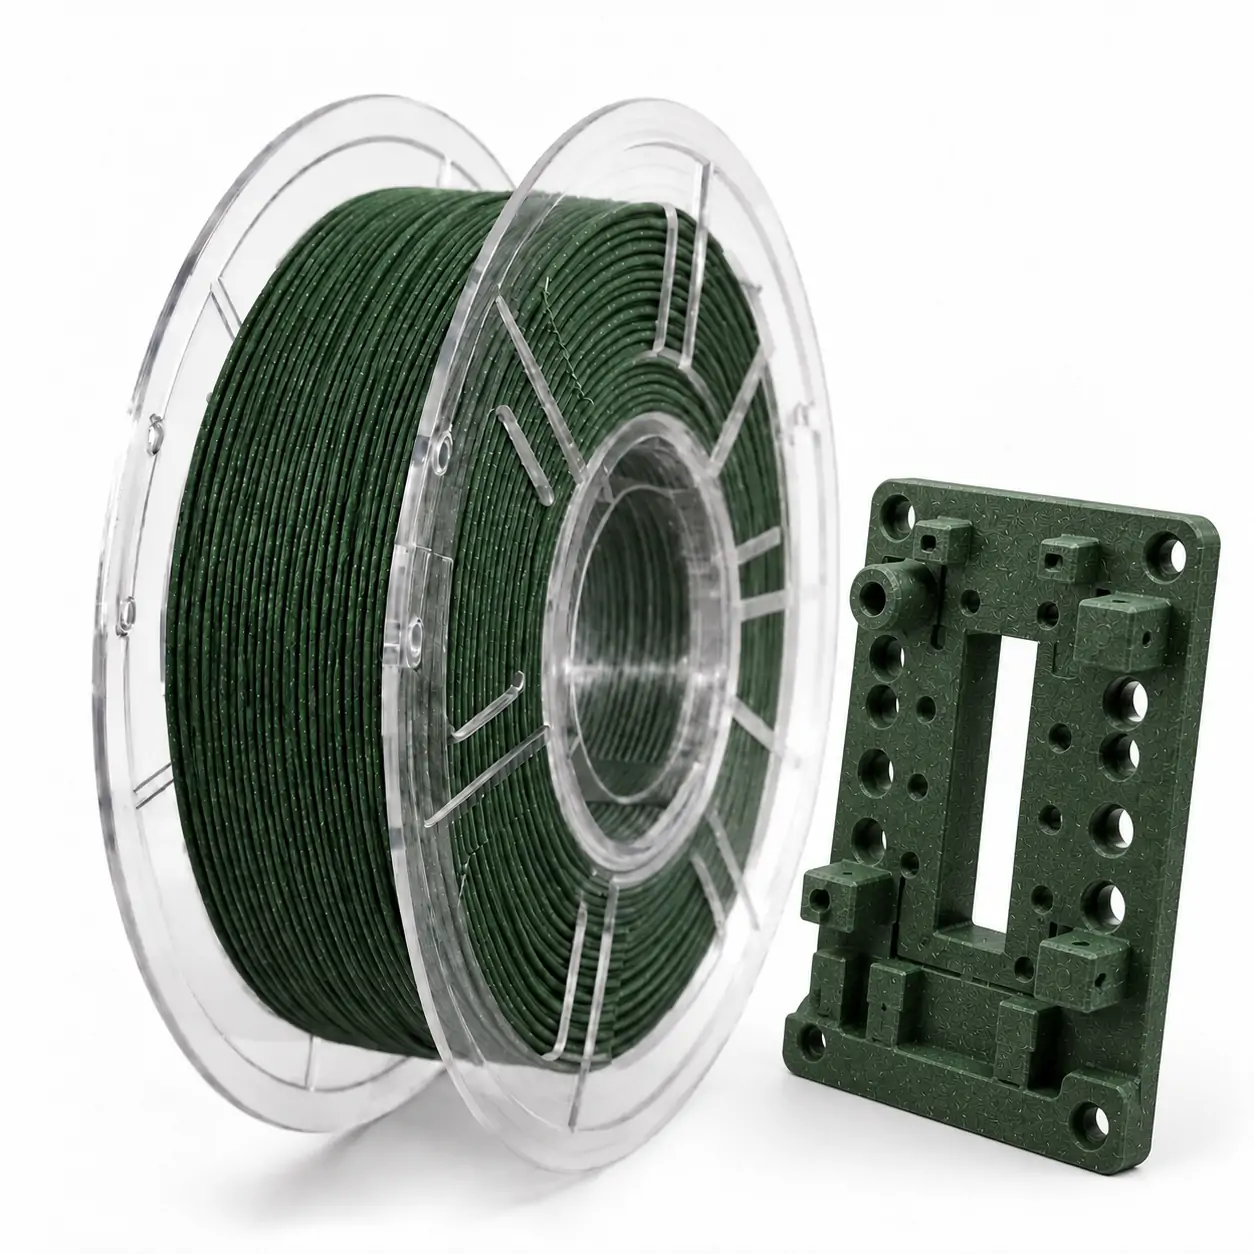
Deep Forest Green PLA-CF | Wholesale Supply | OEM / ODM
SSSray PLA-CF Matte Carbon Fiber PLA 3D Printer Filament 1.75mm, Deep Forest Green – Karbon Fiber PLA Filament Yeşil for Functional Parts & Jigs
B2B PLA-CF supply for distributors, print farms and industrial sourcing programs.
The Deep Forest Green finish is dark and olive-toned, with a low-sheen surface and subtle carbon-fiber flecks that give printed parts a restrained, industrial appearance.
MaterialPLA-CF
SeriesSSSray PLA-CF Carbon Fiber Series
Color EffectDeep Forest Green Matte
Diameter1.75mm
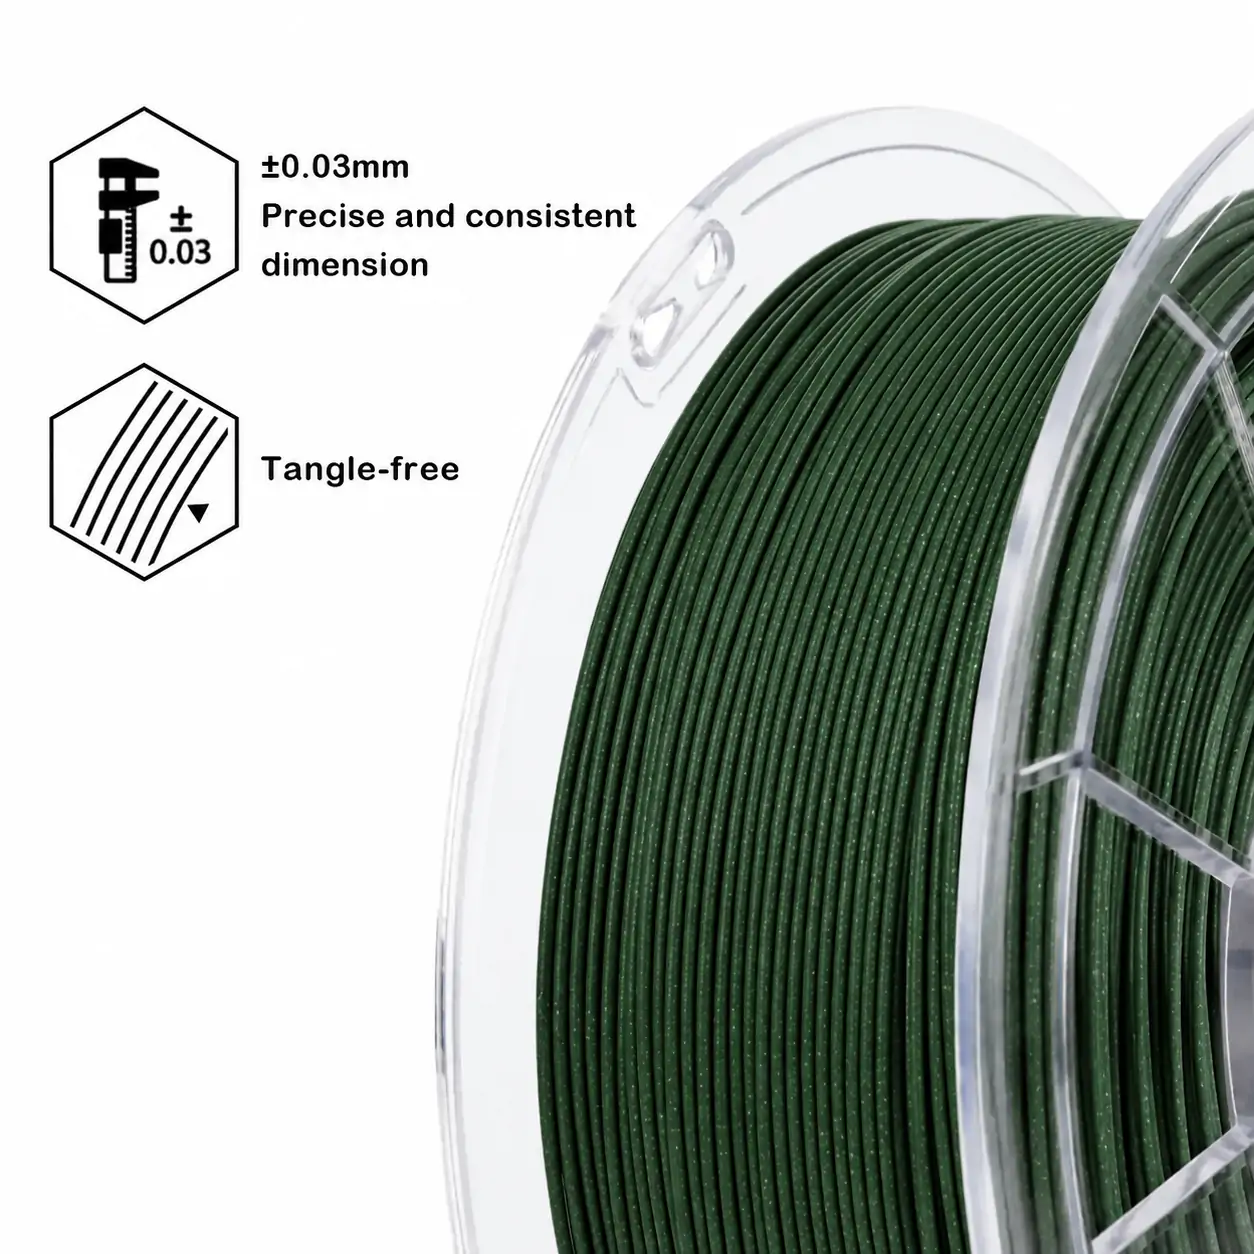
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp210–225°C
Bed Temp50–60°C
Usable Speed40–250 mm/s
Nozzle0.6mm Hardened Preferred
PackagingVacuum + Desiccant
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 days; customized orders typically 15–25 days.
Product Overview
We compound chopped carbon fiber into a PLA matrix to produce a rigid-feeling composite for jigs, fixture plates, brackets, mounting aids, prototype housings and workshop components. The PLA base keeps this grade within a familiar FDM processing range; it is intended for room-temperature functional parts rather than sustained high-heat service.
A Carbon Fiber Color Built for Functional Product Lines
For distributors and private-label brands already carrying PLA-CF, this grade adds a differentiated catalog option without introducing a new polymer family or a separate high-temperature print workflow. Buyers can qualify it alongside existing PLA-CF SKUs using the same nozzle-wear, extrusion-flow and first-layer checks.
Key Selling Points
Deep Forest Green CF Finish
Dark olive-toned green creates a recognizable functional SKU while keeping the restrained matte appearance expected from carbon-fiber materials.
Rigid Functional Printing
Well matched to jigs, fixtures, brackets, mounting aids, prototype housings, and workshop components where stiffness and shape retention matter.
Production-Friendly Speed
Designed for production planning across different FDM systems, this grade can be tuned to the hotend’s flow capacity, cooling setup and layer-bond requirements of each printer.
±0.03mm Diameter Control
Controlled filament diameter supports stable feeding across repeat batches and multi-printer production workflows.
Practical CF Hardware Setup
0.4mm hardened nozzles are usable, while 0.6mm wear-resistant nozzles provide a wider flow path for longer production runs.
Wholesale & Private Label Ready
We support neutral supply, branded labels, retail boxes, color programs, and OEM / ODM packaging for international B2B buyers.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| Material Formulation | PLA matrix compounded with chopped carbon fiber; gives buyers a clear material-family reference for product selection |
| Standard Filament Diameter | 1.75mm standard; 2.85mm available on request for project-specific printer fleets |
| Spool Format | 1kg standard; 3kg and 5kg formats available on request for different order and production requirements |
| Build Environment | A heated chamber is normally unnecessary for PLA-CF; stable bed temperature and first-layer adhesion remain important |
| Gross Weight | 1.3kg for the standard 1kg spool, providing a reference for freight quotation and warehouse handling |
| Drying Guidance | 50–55°C for 6–8 hours after humid storage or moisture symptoms; return the spool to dry, sealed storage after drying |
Where Deep Forest Green PLA-CF Fits in a Carbon Fiber Filament Line
For distributors already carrying black PLA-CF, Deep Forest Green creates a second functional SKU without forcing customers into a different material system. It uses familiar PLA-class temperatures, does not normally require a heated chamber, and keeps the matte carbon-fiber appearance that buyers associate with jigs, fixtures and technical prototypes. This makes it especially useful for brands that want to expand a carbon-fiber range by color while keeping printer requirements and end-user onboarding straightforward.
For applications requiring greater toughness, heat resistance, or environmental durability, buyers can move upward within our carbon fiber filament range to PETG-CF or PA-CF rather than asking one PLA-CF grade to cover every engineering requirement.
How We Work
1
Application & Volume Review
2
Color & Specification Confirmation
3
Sample & Print Test
4
Label & Packaging Approval
5
Batch Production & QC
6
Export Packing & Shipment
Material Comparison Guide
| Material | Surface / Material Behavior | Typical Print Conditions | Hardware Consideration | Typical Use |
|---|---|---|---|---|
| Deep Forest Green PLA-CF | Matte, rigid PLA-based carbon-fiber composite with low-gloss technical surface | 210–225°C nozzle / 50–60°C bed | Wear-resistant nozzle; enclosure normally unnecessary | Jigs, fixtures, brackets, workshop parts, prototype housings |
| Standard PLA | Smooth or satin unfilled PLA with easier nozzle requirements | 190–230°C nozzle / 45–60°C bed | Standard nozzle suitable for most grades | General models, prototypes, displays, everyday prints |
| PETG-CF | Matte CF composite with greater toughness and temperature margin than PLA-CF | Approx. 235–260°C nozzle / 70–85°C bed | Wear-resistant nozzle and good moisture control | Functional housings, machine parts, brackets, durable fixtures |
| PA-CF | Engineering nylon composite with higher thermal and mechanical capability | Higher nozzle temperature with controlled drying | Wear-resistant nozzle and strict moisture management | Engineering tooling, demanding fixtures, structural functional parts |
Technical Specifications
| Product Name | SSSray PLA-CF Matte Carbon Fiber PLA 3D Printer Filament 1.75mm, Deep Forest Green – Karbon Fiber PLA Filament Yeşil for Functional Parts & Jigs |
|---|---|
| Material | PLA-CF – polylactic acid compounded with chopped carbon fiber |
| Series | SSSray PLA-CF Carbon Fiber Series – Matte Functional Parts & Workshop Fixtures |
| Color / Effect | Deep Forest Green; dark olive-toned matte green with subtle carbon-fiber texture |
| Filament Diameter | 1.75mm standard; 2.85mm available on request |
| Tolerance | ±0.03mm |
| Net Weight | 1kg standard; 3kg and 5kg available on request |
| Gross Weight | 1.3kg for standard 1kg unit |
| Spool Type | Plastic spool |
| Packaging | Vacuum sealed with desiccant |
| Preferred Nozzle | 0.6mm hardened steel or other wear-resistant nozzle |
| Usable Nozzle Size | 0.4mm or larger wear-resistant nozzle |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers that can use a wear-resistant nozzle, including Bambu Lab, Prusa, Creality, Flashforge, Anycubic and Elegoo platforms |
| Typical Applications | Jigs, fixtures, brackets, mounting aids, prototype housings, workshop components, robotics and drone prototypes |
| OEM / ODM | Supported |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | 210–225°C |
| Usable Nozzle Range | 190–230°C; increase temperature only as required by flow rate and print speed |
| High-Speed Temperature Guidance | 225–230°C when higher flow requires it; remain within the usable nozzle range and verify layer bonding |
| Recommended Bed Temperature | 50–60°C |
| Usable Bed Range | 45–60°C; selected build surfaces can also run unheated after first-layer tuning |
| Recommended Print Speed | 60–150 mm/s |
| Usable Speed Range | 40–250 mm/s on capable high-flow systems after volumetric-flow, temperature and layer-bond calibration; not a universal setting for every printer |
| Nozzle Diameter | 0.6mm wear-resistant preferred; 0.4mm hardened nozzle usable |
| Layer Height | 0.20–0.28mm with a 0.4mm nozzle; validate finer layers before production |
| Cooling Fan | 50–100% after the first layers; tune lower for layer bonding and higher for small features |
| Direct Drive Retraction | 0.5–1.0mm at 30–40 mm/s; fine-tune for the hotend and nozzle |
| Bowden Retraction | 2–5mm at 30–45 mm/s; fine-tune to tube length and extruder response |
| Wall Count | 3–5 perimeters for functional parts |
| Infill | 20–30% general functional parts / 40–60% higher-demand jigs and fixtures |
| First Layer Speed | 20–30 mm/s |
| Bed Adhesion | Clean PEI, textured PEI or suitable coated/glass surface; use adhesive where the build surface requires it |
| Enclosure | Normally not required for PLA-CF |
| Drying | 50–55°C for 6–8 hours after humid storage or when moisture symptoms appear; keep sealed with desiccant after drying |
Print Optimization Guide
| Item | Practical Guidance |
|---|---|
| Nozzle Selection | Use a hardened or other wear-resistant nozzle because carbon-fiber-filled filament accelerates wear on ordinary brass nozzles |
| Production Nozzle Size | Use 0.6mm for longer production runs and higher flow; 0.4mm remains useful where smaller features are important |
| Matte Surface Quality | Keep outer-wall speed below the maximum production speed when the most uniform matte finish is the priority |
| Fixture Stiffness | Increase wall count before relying only on high infill; perimeter structure contributes strongly to the rigidity of jigs and brackets |
| First Layer | Use a clean build plate, 50–60°C bed and controlled first-layer speed before increasing throughput on later layers |
| Moisture Control | Dry the spool if popping, rough extrusion or abnormal stringing appears, then return it to sealed storage with desiccant |
| High-Speed Printing | For operation within the 40–250 mm/s usable range, increase nozzle temperature only within the 190–230°C usable range and confirm that the hot end can maintain the required volumetric flow, cooling and layer bonding; 250 mm/s is not a universal setting for every printer |
| Deep Forest Green Finish | Larger faces, brackets and fixture plates show the dark olive-green matte CF texture particularly well under neutral workshop lighting |
Printer Brand Starting Settings
| Printer Brand / Family | Nozzle | Bed | Speed | Starting Notes |
|---|---|---|---|---|
| Bambu Lab X1-Carbon | 215–225°C | 50–60°C | 60–150 mm/s | Factory hardened-steel 0.4mm nozzle is suitable; a hardened 0.6mm nozzle gives more flow margin for sustained PLA-CF printing |
| Bambu Lab X1 / P1 Series | 215–225°C | 50–60°C | 60–150 mm/s | Use a hardened-steel nozzle; 0.6mm is preferred for regular abrasive PLA-CF production |
| Bambu Lab A1 | 215–225°C | 50–60°C | 60–120 mm/s | Replace the stock stainless-steel nozzle with a hardened-steel nozzle before regular PLA-CF use; 0.6mm gives more flow margin |
| Prusa MK4 / CORE One Families | 210–225°C | 55–60°C | 50–100 mm/s | The standard brass nozzle wears quickly with abrasive filament; fit a hardened or other abrasion-resistant nozzle and start at 0.20mm layer height or above |
| Creality K1 | 210–225°C | 50–60°C | 60–120 mm/s | Nozzle hardware varies by production revision; use a fitted hardened or other wear-resistant nozzle for regular PLA-CF printing |
| Creality K1 Max | 210–225°C | 50–60°C | 60–150 mm/s | The factory hardened-steel nozzle is suitable; increase speed only after flow and first-layer behavior are stable |
| Flashforge Adventurer 5M Series | 210–225°C | 50–60°C | 50–100 mm/s | Flashforge specifies PLA-CF with 0.6mm / 0.8mm nozzle options; use a wear-resistant nozzle and validate flow before increasing speed |
| Anycubic Open-Material 1.75mm Models | 210–225°C | 50–60°C | 50–100 mm/s | Use an abrasion-resistant nozzle and increase speed only after first-layer and flow calibration |
| Elegoo Open-Material 1.75mm Models | 210–225°C | 50–60°C | 50–100 mm/s | Use an abrasion-resistant nozzle for repeat PLA-CF production and tune retraction by extruder type |
These are SSSray starting parameters, not printer-manufacturer PLA-CF profiles. The 60–150 mm/s range is the typical production starting window; the broader 40–250 mm/s usable range applies only to capable high-flow setups after volumetric-flow, first-layer, cooling and layer-bond validation.
Performance Characteristics
| Characteristic | What You Can Expect in Printing | Recommended Use |
|---|---|---|
| Warping Behavior | PLA-based processing keeps warping manageable under a stable first layer and recommended bed temperature | Medium-size brackets, plates and functional components |
| Temperature Capability | Retains PLA-matrix temperature behavior rather than high-temperature nylon or PC performance | Room-temperature functional parts, tooling aids and prototypes |
Applications
| Application Focus | Practical Notes |
|---|---|
| Assembly Jigs & Fixtures | Suitable for alignment aids, fixture plates, drill guides and workshop tooling where a rigid body and matte surface are useful |
| Mounting Brackets | Works well for equipment mounts, sensor holders and non-safety-critical brackets that need stable geometry |
| Robotics & Drone Prototypes | Useful for prototype mounts, covers, structural mockups and iterative development parts |
| Prototype Housings | Deep Forest Green gives prototype enclosures and machine-side housings a distinctive engineering appearance |
| Workshop Components | Suitable for tool holders, gauges, clamps, organizers and machine-side accessories |
| Technical Display Models | The matte CF texture gives demonstration parts a more functional appearance than conventional glossy PLA |
Storage Guide
- Keep unopened spools vacuum sealed with desiccant until use
- Return opened spools to a sealed bag or dry box in humid environments
- Dry at 50–55°C for 6–8 hours if moisture-related extrusion symptoms appear
- Keep spools away from direct sunlight and unnecessary heat during storage
- Secure the filament end before storage to protect the winding for the next print run
OEM / ODM Services
We supply PLA-CF programs for distributors, wholesalers, private-label brands, importers, industrial sourcing teams, education suppliers, and print farms. Available options include neutral packaging, private labels, branded retail boxes, barcode and SKU labels, carton marks, color assortment planning, standard or customized spool formats, and project-specific packaging.
MOQ Reference: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools. Standard production is typically 7–15 days, while customized programs are typically 15–25 days.
Quality Control
- Diameter and tolerance checks against the confirmed ±0.03mm specification
- Winding appearance and spool condition inspection before packing
- Deep Forest Green color and matte surface consistency checks during production
- Vacuum seal and desiccant inclusion inspection
- OEM label, barcode, retail box and carton-mark verification
- Final order check covering SKU, quantity, packaging and shipment preparation
Technical Documents & Compliance
| Document / Requirement | Supply Information |
|---|---|
| TDS | Technical Data Sheet available for product and project documentation |
| SDS / MSDS | Safety Data Sheet available for shipping and customer documentation |
| RoHS / REACH | Supporting compliance documents can be matched to the ordered product and market requirement |
| SGS / Third-Party Reports | Applicable third-party reports can be supplied for relevant products and project requirements |
| B2B Documentation | Contact our team with your required document list so the correct technical and commercial files can be prepared with the order |
Frequently Asked Questions
What is the MOQ for Deep Forest Green PLA-CF?
Neutral packaging starts from 50 spools. OEM packaging normally starts from 500–1,000 spools depending on the label, box, spool, and customization requirements.
How fast can this PLA-CF be printed?
For routine production, 60–150 mm/s provides a practical balance of throughput and surface finish. High-flow printers can work within a broader 40–250 mm/s range after nozzle temperature, volumetric flow, cooling and layer bonding are calibrated.
What nozzle should I use for PLA-CF?
Use a hardened steel or other wear-resistant nozzle because carbon-fiber-filled filament is abrasive. A 0.4mm hardened nozzle can be used, while 0.6mm is preferred for longer production runs and a more forgiving material flow path.
Does Deep Forest Green PLA-CF need a heated enclosure?
A heated enclosure is normally unnecessary. A clean build surface, stable first layer, 50–60°C bed temperature and controlled cooling are more important for routine PLA-CF printing.
What parts is this color best suited for?
The dark olive-green matte finish works particularly well for jigs, fixture plates, brackets, sensor mounts, prototype housings, robotics parts, workshop accessories and other functional prints where a technical color is preferred over standard black.
Can I request samples before placing a bulk order?
Verified B2B buyers can apply for up to 3 complimentary sample spools. Use our B2B sample program for sample requests or our filament qualification program for structured product testing.
Can SSSray supply private-label PLA-CF?
Yes. We support custom labels, branded retail boxes, barcode and SKU labels, carton marks, spool options, color programs, and OEM / ODM packaging for B2B projects.
What is the normal lead time?
Standard orders are typically produced in 7–15 days. Customized OEM / ODM orders are typically 15–25 days after product specifications and packaging details are confirmed.
Add Deep Forest Green to Your PLA-CF Product Line
Contact our team for bulk pricing, sample testing, private-label packaging, or a multi-color PLA-CF supply program. Buyers building a broader composite range can also explore our Wholesale Carbon Fiber Filament program.



Related products
-

SSSray PLA-CF in Dusty Rose: 1.75mm Carbon Fiber PLA 3D Printer Filament – filament PLA fibre de carbone rose – for Motor Mounts & Finned Housings
-
High-Strength ABS-GF Filament 1.75mm 1kg – Glass Fiber Reinforced Engineering Grade for Industrial Functional Parts| OEM/ODM Bulk Supply
-
SSSray 1.75mm PLA-CF 3D Printing Filament, Midnight Navy Carbon Fiber PLA – カーボンファイバー入りPLAフィラメント – for Tooling Clamps & Pulley Brackets
-
SSSray Charcoal Black PETG-CF 3D Printer Filament, Matte Carbon Fiber PETG – siyah karbon fiber PETG filament for Drone Gimbal Mounts & Support Brackets