Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

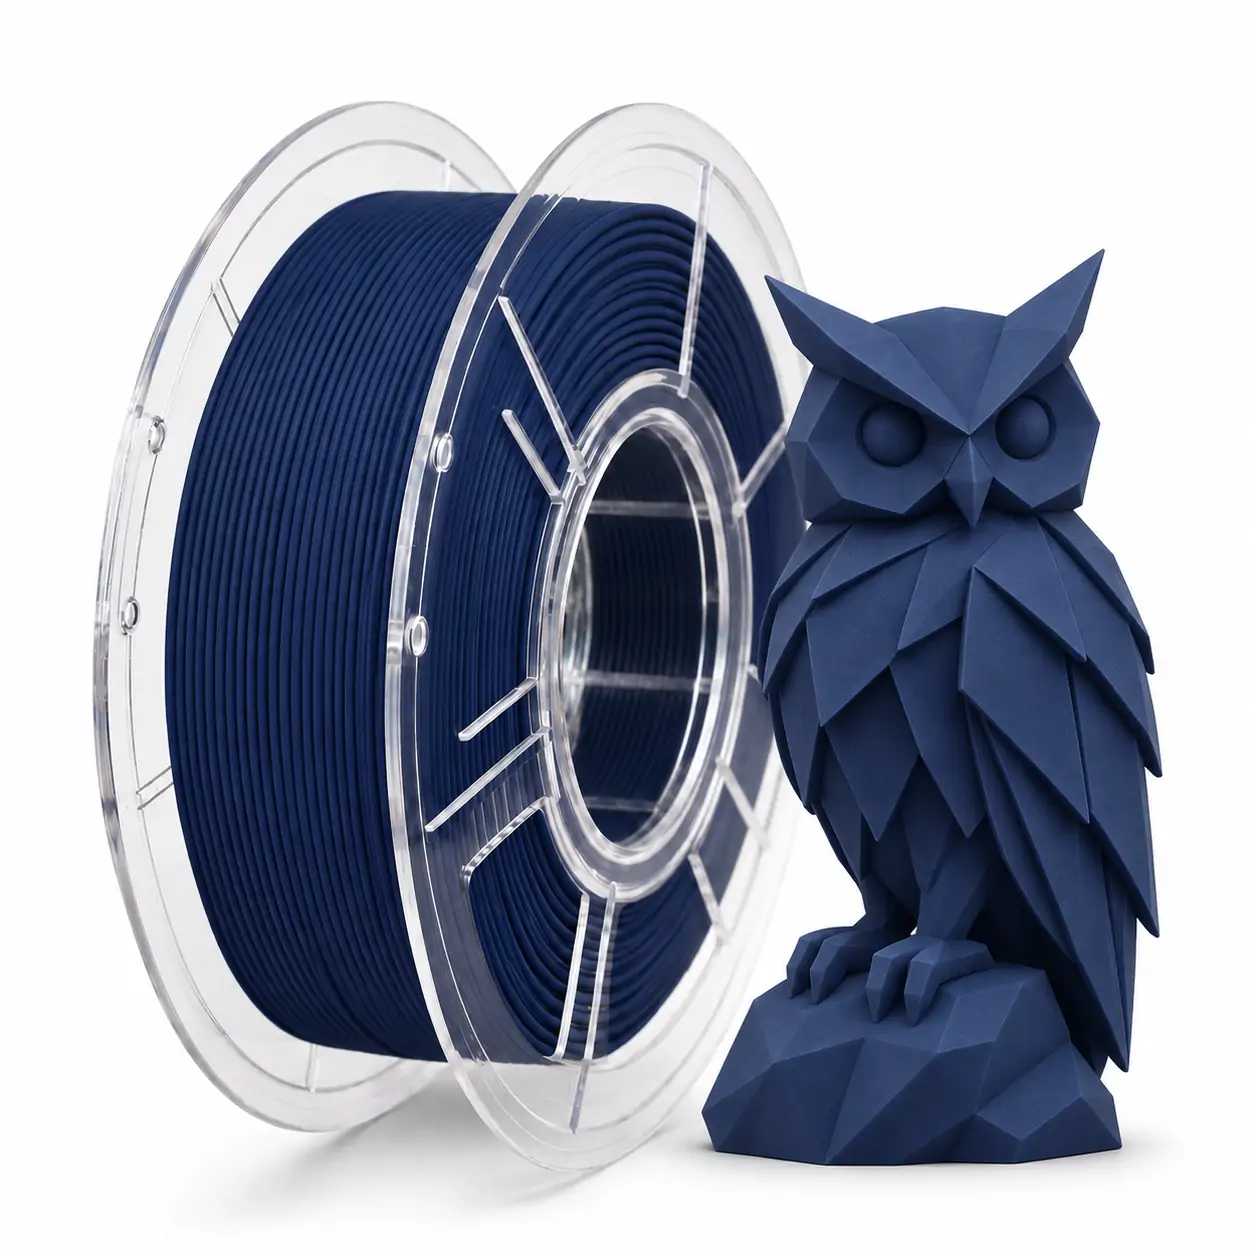


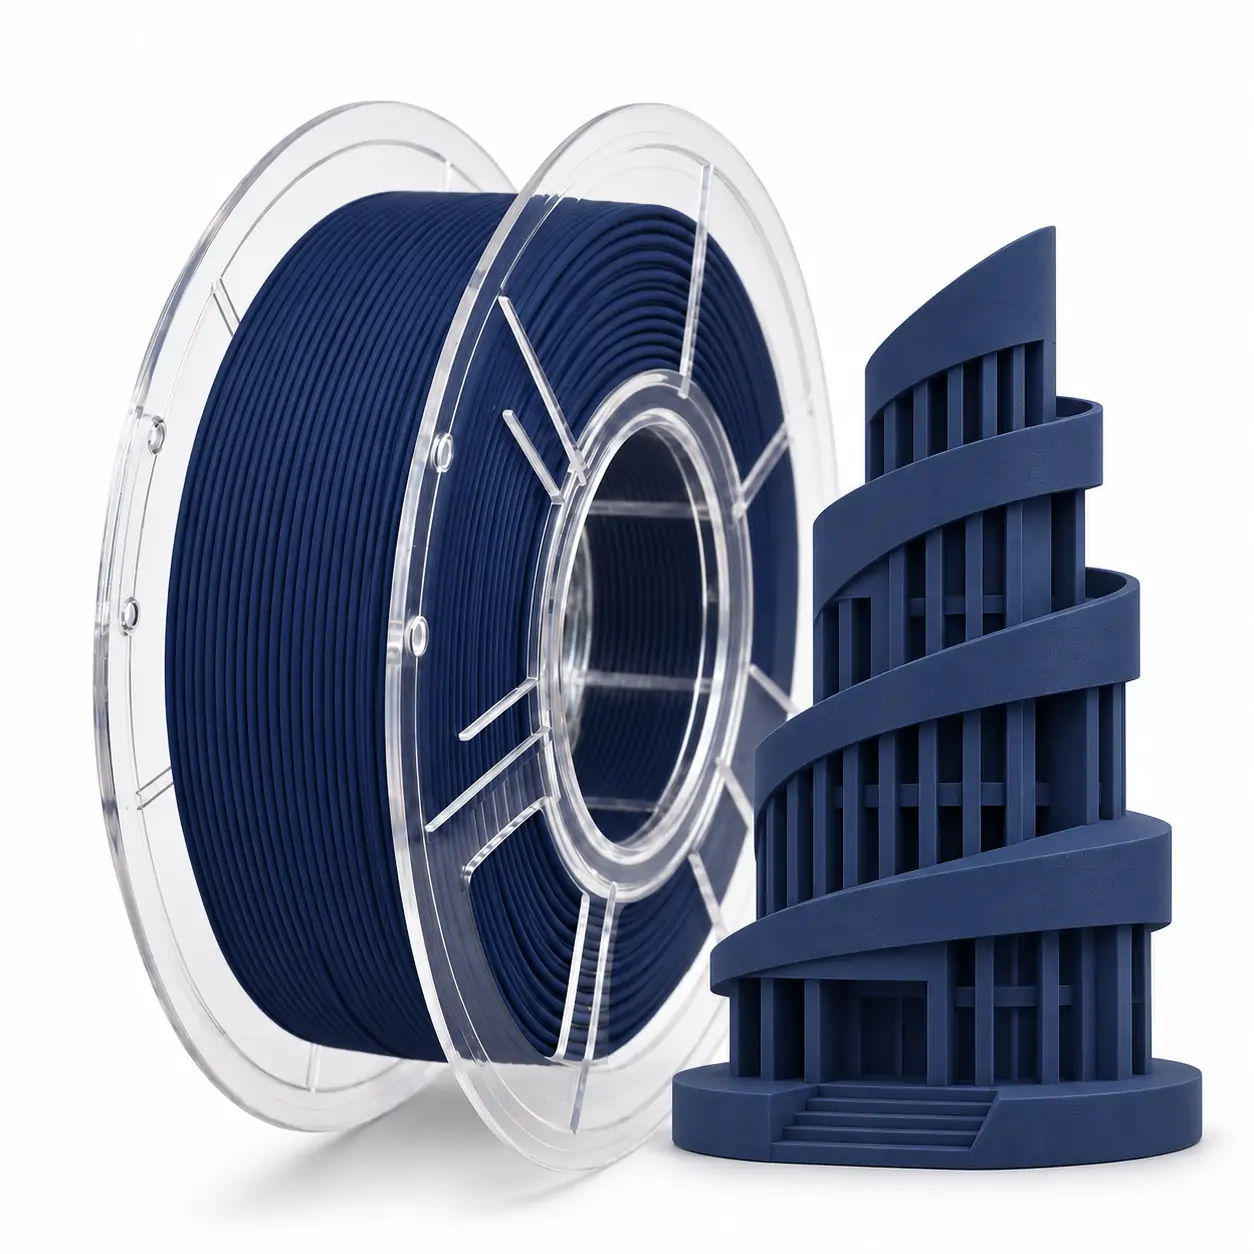
SSSray PLA Matte Series | High-Speed Deep Navy Blue | Factory Direct
SSSray Navy Blue PLA Matte Filament 1.75mm – High-Speed Matte PLA for FDM 3D Printing
Factory-direct 1.75mm navy blue PLA matte filament for FDM/FFF printing, architectural presentation models, geometric displays, low-poly figures and B2B wholesale supply.
We manufacture SSSray Navy Blue PLA Matte for FDM/FFF buyers who need a solid, opaque deep-navy colour, a soft low-glare finish and a defined high-speed print profile up to 250mm/s. Its muted indigo-grey undertone helps faceted planes, columns, spiral ramps and stair details remain visually clear on architectural and geometric prints.
MaterialPLA Matte
SeriesSSSray PLA Matte Series
Color EffectSolid Navy Blue / Soft Matte
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp210–230°C
Bed Temp45–60°C
Print Speed100–250 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time: Standard 7–15 working days; customized orders typically 15–25 working days.
Product Overview
SSSray Navy Blue PLA Matte Filament is a 1.75mm PLA Matte material for FDM/FFF printers, supplied on a 1kg plastic spool with a stated ±0.03mm diameter tolerance. We manufacture it in a solid, opaque deep-navy shade with a muted indigo-grey undertone. Its soft matte surface diffuses reflected light rather than creating a glossy highlight, helping the planes of low-poly figures and the edges of architectural models remain visually legible. It is suited to scale buildings, façade studies, tower forms, columns, spiral ramps, stair details, low-poly figures and other geometric presentation models.
We vacuum-seal each 1kg spool with desiccant. For this SKU, our starting profile is 210–230°C nozzle temperature, 45–60°C bed temperature and 100–250mm/s print speed. Tune hotend flow, cooling and acceleration to the actual printer and model while keeping the print profile within the 250mm/s maximum. Neutral packaging starts at 50 spools; OEM packaging typically starts at 500–1,000 spools. This deep-navy high-speed matte SKU is distinct from our existing Matte Blue PLA and Navy Blue PLA Basic.
Why This Product Stands Out
We developed this SKU for buyers who need a deep, opaque navy shade, a soft low-glare matte surface and higher-throughput PLA processing. It is a single-color material, not a silk, metallic or gradient filament. The combination gives architectural geometry and faceted display models a restrained finish while adding a distinct high-speed option to a PLA Matte assortment.
Key Selling Points
Factory-Controlled Diameter
Our inline dual-axis laser monitoring tracks filament diameter during extrusion against the PLA-family production standard of 1.75mm ±0.03mm. The published maximum ovality benchmark is ≤0.020mm, giving buyers measurable dimensional criteria for batch qualification and incoming inspection.
High-Speed PLA Matte Output
Use 100–250mm/s for this SKU’s high-speed production profile. Calibrate hotend flow, cooling and slicer settings on the actual printer, and keep the selected print speed at or below 250mm/s.
Navy Blue Matte Finish
Solid, opaque deep navy with a muted indigo-grey undertone; no gradient, silk or metallic effect.
Vacuum-Sealed 1kg Spool
Each 1kg plastic spool is vacuum-sealed with silica desiccant; our published PLA-family vacuum-protection benchmark is −0.09MPa.
Factory-Direct Export Supply
Neutral packaging starts at 50 spools; OEM packaging typically starts at 500–1,000 spools, with export supply from Ningbo, China.
OEM / ODM & Private Label
As the manufacturer, we coordinate custom labels, branded boxes, barcodes, carton marks and selected spool options directly with qualified buyers.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| Colour Specification | Solid, opaque deep navy with muted indigo-grey undertone; single-colour matte, not silk, metallic or gradient |
| Print Profile | 100–250mm/s on suitable FDM/FFF systems after printer-specific calibration; maximum 250mm/s |
| Dimensional QC | 1.75mm ±0.03mm; PLA-family maximum ovality benchmark ≤0.020mm |
| Moisture & Packaging | PLA-family moisture benchmark ≤0.02%; vacuum reference −0.09MPa with silica desiccant |
| Lot Evidence | Batch COA records measured lot values; factory checks include laser diameter, moisture and colour control |
| Unit Configuration | 1kg net filament on a plastic spool; 1.3kg gross packaged reference |
| B2B Order Format | Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools |
Factory-Direct Supply for High-Speed B2B Programs
We manufacture filament at our Jinhua, Zhejiang facility and operate 50+ extrusion lines, with published monthly production capacity above 1,000 tons. For this Navy Blue PLA Matte SKU, we combine a distinctive deep-navy finish, a print profile up to 250mm/s, batch-linked quality records, neutral packaging from 50 spools and OEM packaging typically from 500–1,000 spools. We work with buyers to qualify samples, confirm print performance on the target printer and agree on colour, packaging and batch acceptance requirements for repeat orders. Review our factory batch QC data and COA process or our wholesale high-speed filament program.
For buyers comparing blue PLA options, this new SKU remains separate from our Matte Blue PLA and Navy Blue PLA Basic. Choose this page when the requirement is specifically deep navy, matte appearance and high-speed processing.
B2B Cooperation Process
1
Project & Market Requirement Review
2
Colour, Diameter & Packaging Confirmation
3
Sample Printing & Approval
4
Label, Spool & Carton Planning
5
Batch Production Scheduling
6
Final QC, Packing & Shipment
Material Comparison Guide
| Material | Surface / Appearance | Print Speed Positioning | Typical Nozzle / Bed | Best-Fit Applications |
|---|---|---|---|---|
| Navy Blue PLA Matte (this SKU) | Solid, opaque deep navy; diffuse low-glare matte | 100–250mm/s after printer-specific calibration; maximum 250mm/s | 210–230°C / 45–60°C; 230–260°C for advanced high-flow tuning | Architectural models, low-poly figures, geometric display pieces |
| Standard PLA | Usually smoother with more visible surface reflection | Conventional profile; depends on formulation, hotend and cooling | 185–235°C / 50–60°C | Prototypes, education, everyday models |
| PETG | Often glossier; more ductile than PLA | Grade- and hotend-dependent; tune cooling and flow | 215–270°C / 70–90°C | Utility parts, brackets, covers and functional models |
| ABS / ASA | Satin to matte depending on grade; higher-temperature material family | Enclosure, thermal control and machine capability are key limits | ABS: 230–255°C / 95–110°C; ASA: 220–275°C / 90–110°C | Engineering housings; ASA for outdoor-oriented parts |
Speed and temperature values are starting references, not universal presets. Confirm the material TDS and qualify the profile on the actual printer, hotend and model geometry.
Technical Specifications
| Product Name | SSSray Navy Blue PLA Matte Filament 1.75mm – High-Speed Matte PLA for FDM 3D Printing |
|---|---|
| Material | PLA Matte (polylactic acid with a matte surface finish) |
| Product Series | SSSray PLA Matte Series – Deep Tones for Architectural & Geometric Models |
| Colour | Navy Blue; medium-dark navy with a muted indigo-grey undertone |
| Colour / Surface Effect | Solid, opaque, soft matte; no gloss, silk, metallic or gradient effect |
| Filament Diameter | 1.75mm standard for this SKU |
| Diameter Tolerance | ±0.03mm |
| Recommended Nozzle Temperature | 210–230°C for routine high-speed printing; 230–260°C for advanced high-flow tuning |
| Recommended Bed Temperature | 45–60°C |
| Print Speed | 100–250mm/s; maximum 250mm/s on suitable systems after printer-specific calibration |
| Net Filament Weight | 1kg per spool |
| Gross Weight | 1.3kg per packaged spool |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, including Bambu Lab, Prusa, Creality, Flashforge, Anycubic and Elegoo models; confirm spool clearance and material profile |
| Typical Applications | Architectural presentation models, low-poly figures, geometric display models, scale towers, columns and educational models |
| OEM / ODM | Supported: private label, labels, packaging, selected spool options and project-based colour discussions |
| Compliance | RoHS compliant; current product compliance documentation is available for buyer review |
| Technical Documents | SKU-specific TDS and SDS / MSDS are available; batch COA and lot QC records are available through our factory QC process |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Nozzle Temperature | 210–230°C for routine high-speed printing; 230–260°C only when required by a tuned profile approaching 250mm/s |
| Bed Temperature | 45–60°C; tune within this range for the build plate, model footprint and room conditions |
| Print Speed | 100–250mm/s; increase only after confirming stable extrusion, cooling and layer bonding |
| Usable Speed Window | 50–250mm/s depending on hotend flow, nozzle, layer dimensions, acceleration, cooling and model geometry |
| Maximum Volumetric Flow | Set the slicer limit to the tested capability of the actual hotend and filament profile; do not use motion speed alone as the flow limit |
| Retraction – Direct Drive | 0.4–1.2mm at 25–40mm/s; tune to the extruder and hotend |
| Retraction – Bowden | 3–5mm at 25–45mm/s; tune to the actual filament path |
| Layer Height | 0.16–0.28mm recommended with a 0.4mm nozzle; 0.12–0.32mm usable after profile tuning |
| Cooling Fan | 100% after the first 2–3 layers for high-speed cooling; reduce only if layer adhesion or surface finish requires tuning |
| Wall Count | 2–4 perimeters; use 3–4 for larger display parts that need additional rigidity |
| Infill | 15–20% for decorative models; 25–40% for prototypes; 40–60% for denser display parts |
| First-Layer Speed | 20–40mm/s to establish bed contact before ramping to the production profile |
| Bed Adhesion | Clean smooth PEI, textured PEI or glass; follow the build-plate maker’s recommended cleaning or adhesion method |
| Drying, if Moisture Is Suspected | 50°C for approximately 8 hours in a controlled filament dryer; cool and reseal with desiccant |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Speed Ramp | Qualify at 150–200mm/s, then increase only as needed up to 250mm/s while checking extrusion continuity, layer bonding and surface quality |
| Volumetric Flow | Set maximum volumetric flow from a test on the actual hotend, nozzle, line width and layer height; a motion-speed value alone does not prove throughput |
| Temperature Scaling | Use 210–230°C for routine high-speed work; increase progressively toward 230–260°C only when higher flow demand requires it |
| Architectural Edges | Use 0.12–0.16mm layers for fine façade details; keep outer-wall speed consistent and reduce it only where detail requires |
| Low-Poly Facets | Keep model orientation and external-wall settings consistent so the matte surface reads evenly across facet transitions |
| Outer-Wall Finish | Use a stable outer-wall speed and avoid abrupt speed or temperature changes across visible faces; prioritize uniformity over peak motion speed on display surfaces |
| Cooling | Use strong part cooling after the first layers; confirm bridges and short layer times remain clean at the selected production speed |
| Seam Placement | Align the Z seam to a rear edge or less visible corner; avoid random seam placement on a main display face |
| First-Layer Adhesion | Run the first layer at 20–40mm/s, confirm Z offset and plate cleanliness, then ramp to the production profile |
| Nozzle Choice | A standard 0.4mm nozzle suits routine use; a high-flow 0.4mm or 0.6mm setup is preferred when targeting the upper speed range |
| Moisture Management | Keep the spool sealed with desiccant between jobs; dry it if popping, bubbles or inconsistent extrusion appear |
| Large Flat Models | Use a stable bed temperature and avoid cold drafts; add a brim when the footprint or room conditions call for it |
Printer Brand Starting Settings
| Printer Platform | Nozzle | Bed | Starting / Qualified Speed | SSSray Setup Note |
|---|---|---|---|---|
| Bambu Lab | 220–230°C | 55–60°C | 200–250mm/s | Start from a Generic / PLA profile; calibrate flow ratio and maximum volumetric speed before increasing throughput |
| Prusa | 210–230°C | 50–60°C | 150–250mm/s | Use a high-flow nozzle where supported; confirm stable extrusion before raising speed |
| Creality | 220–230°C | 45–60°C | Up to 250mm/s | For K1 / Ender high-speed platforms; use strong cooling and tune maximum flow before approaching the upper range |
| Anycubic | 210–230°C | 55–65°C | 150–250mm/s | Confirm hotend throughput, build-plate profile and surface finish before moving toward higher flow |
| Elegoo | 210–230°C | 40–60°C | 200–250mm/s | Use full part cooling after the early layers and confirm finish quality at the selected speed |
These are first-print references for supported high-speed platforms, not universal machine presets. Calibrate flow ratio, maximum volumetric speed, cooling and pressure advance on the actual printer. Keep this SKU at or below 250mm/s; reduce outer-wall speed when fine architectural detail or surface uniformity takes priority.
Performance Characteristics
| Characteristic | Product Specification / Behaviour | Production or Use Reference |
|---|---|---|
| Colour | Solid, opaque navy blue with a muted indigo-grey undertone | Single-colour appearance; no gradient, silk or metallic effect |
| Surface Reflection | Soft matte, diffuse reflection | Reduces specular glare on visible planes and edges |
| Filament Diameter | 1.75mm with ±0.03mm stated tolerance | Use the stated tolerance as the incoming inspection reference for batch qualification |
| Extrusion Behaviour | High-speed PLA Matte extrusion under a tuned profile | 100–250mm/s profiles after hotend-flow and cooling calibration; maximum 250mm/s for this SKU |
| Dimensional Behaviour | PLA-based material with a low warping tendency under suitable setup | Bed preparation, part footprint and ambient drafts affect results |
| Factory High-Speed Validation | SSSray sampled-spool print-farm testing for this SKU covers speeds up to 250mm/s | Factory print-farm runs use Bambu Lab, Creality and Voron systems; qualify the final profile on the buyer’s printer and hotend |
| Packaging Format | 1kg net spool; 1.3kg gross packaged weight | Vacuum-sealed bag with desiccant; plastic spool |
| Application Positioning | Display and general-purpose models | Not positioned as a high-temperature engineering material |
Applications
| Application Focus | Practical Notes |
|---|---|
| Architectural Presentation Models | Deep navy provides a restrained display tone for massing studies, façade blocks and scale-building models |
| Columns, Towers & Spiral Structures | The matte surface keeps vertical lines, spiral ramps, stair geometry and structural layers visually readable |
| Low-Poly Figures & Animals | Opaque colour and diffuse reflection help polygon planes remain distinct under indoor lighting |
| Urban Planning & Educational Models | Useful for physical study models, teaching aids and presentation pieces where a consistent solid colour is preferred |
| Geometric Display Objects | Suitable for faceted sculptures, desk displays and decorative models with defined edges |
| Concept & Product Mock-ups | Use for visual form reviews and non-load-bearing prototypes; select another material where heat or impact resistance is required |
Storage Guide
- Keep unopened spools in the original vacuum-sealed bag with the supplied desiccant
- After opening, return the spool to a sealed dry box or resealable moisture-barrier bag
- Store in a cool, dry place away from direct sunlight and heat sources
- For humid storage environments, maintain a dry-box humidity target below 20% RH where practical
- If moisture symptoms appear during printing, dry at 50°C for approximately 8 hours in a controlled filament dryer before resealing
OEM / ODM Services
We manufacture and supply PLA Matte filament for distributors, wholesalers, importers and private-label brands. OEM discussions can cover neutral or branded labels, retail-box artwork, barcode and carton marking, selected spool options, colour-range planning and private-label product-line development. Send us your target market, annual volume, packaging format and colour reference for quotation and feasibility review.
MOQ Reference: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls. Final packaging scope and lead time are confirmed with the order specification.
Factory Quality Control & Batch COA
- Our inline dual-axis laser monitoring tracks filament diameter during extrusion against the PLA-family production standard of 1.75mm ±0.03mm. The published maximum ovality benchmark is ≤0.020mm, giving buyers measurable dimensional criteria for batch qualification and incoming inspection.
- After drying, our moisture analysis checks the PLA / PLA+ / High-Speed PLA family benchmark of ≤0.02% before vacuum sealing, supporting consistent material handling and storage protection.
- During production, we check colour against the approved master reference. Our published PLA-family colour-difference benchmark is ΔE < 0.8, supporting shade control across production batches and repeat orders.
- We put sampled spools through 24-hour print-farm runs on Bambu Lab, Creality and Voron systems, with the validated print-speed ceiling for this SKU set at 250mm/s. These extended print trials help us assess extrusion stability and print consistency over sustained operation.
- Our factory QC program also covers melt-flow and tensile testing, precision weighing, print trials, winding inspection and package-integrity checks.
- We issue a batch Certificate of Analysis (COA) with measured lot values for each shipment and use batch identification to support production traceability and repeat-order follow-up.
See the SSSray Batch QC Data & Factory COA page for the published PLA-family release benchmarks and factory inspection process. SKU- and lot-specific records are confirmed against the order and shipment batch.
Compliance & Technical Documents
- We supply this SKU with current RoHS compliance documentation for buyer review and product qualification.
- We maintain current SKU-specific TDS and SDS / MSDS files for technical qualification, purchasing and import-documentation checks.
- We can match batch COA records and applicable lot QC data to the shipment; additional market-specific declarations are confirmed against the destination-market requirements.
Frequently Asked Questions
What shade and surface effect does this Navy Blue PLA Matte have?
It is a solid, opaque medium-dark navy blue with a slightly muted indigo-grey undertone. The finish is soft matte, without a silk, metallic or gradient effect.
Which printers can use this 1.75mm filament?
It is suitable for most open-material FDM/FFF printers designed for 1.75mm filament, including many Bambu Lab, Prusa, Creality, Flashforge, Anycubic and Elegoo models. Check the spool holder, filament path and slicer profile for the specific machine.
What print settings should I start with?
Start at 210–230°C nozzle temperature, 45–60°C bed temperature and 100–250mm/s for high-speed printing. When approaching the 250mm/s upper range, use a suitable high-flow system and tune nozzle temperature toward 230–260°C while matching maximum volumetric flow and cooling to the hotend.
What high-speed print range can this Navy Blue PLA Matte support?
Use 100–250mm/s as the high-speed production window for this Navy Blue PLA Matte Filament. A suitable high-flow system can approach the 250mm/s upper limit when hotend flow, nozzle temperature, cooling, acceleration and model geometry are properly matched. Our factory print-farm testing includes 24-hour sampled-spool runs on Bambu Lab, Creality and Voron systems at speeds up to 250mm/s.
Is the matte finish suitable for architectural and low-poly models?
Yes. The opaque navy colour and diffuse matte surface are intended for display models where reduced glare helps planes, edges, columns and geometric features remain easy to read.
Can this PLA Matte be used for functional or outdoor parts?
This product is positioned for display and general-purpose models. PLA has limited heat resistance compared with PETG, ABS and ASA, so choose a material designed for the required heat, impact or outdoor exposure when the part has demanding service conditions.
What is the minimum order quantity?
Neutral packaging starts from 50 rolls. OEM packaging typically starts at 500–1,000 rolls, depending on the agreed label, box and spool requirements.
Can qualified buyers receive samples?
Verified B2B buyers can apply for up to 3 complimentary 1kg sample spools for evaluation after review. Sample freight is paid by the buyer; preparation and dispatch timing are confirmed by sales.
What OEM options, lead times and documents can SSSray support?
OEM options include private labels, branded boxes, carton markings, selected spool options and project-based colour planning. Standard orders are typically 7–15 working days; customized orders are typically 15–25 working days. We can provide the current SKU-specific TDS, SDS / MSDS and RoHS compliance documentation for buyer review.
Source High-Speed Navy Blue PLA Matte Direct from SSSray
We supply this 1.75mm deep-navy matte SKU for high-speed FDM printing, wholesale distribution and OEM / private-label programs. Contact our factory team for pricing, sample qualification, batch QC records and export planning.



Related products
-

SSSray PLA Signage Grade 3D Printing Filament – Translucent & Solid 1kg (Custom OEM & Wholesale)
-
Pink Crystal PLA Filament 1.75mm 1kg – High Translucency Glossy Finish for FDM 3D Printing, Ideal for Decorative Models & Jewelry Prototypes
-
Rainbow Glow-in-the-Dark PLA Filament 1.75mm 1kg – Multi-Color Luminous Gradient for FDM Printers, Ideal for Novelty Toys & Display Models
-
Dual Color Gradient Crystal PLA Filament 1.75mm 1kg – Translucent Two-Tone Finish for FDM 3D Printing, Ideal for Artistic Decor & Jewelry Prototypes