Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

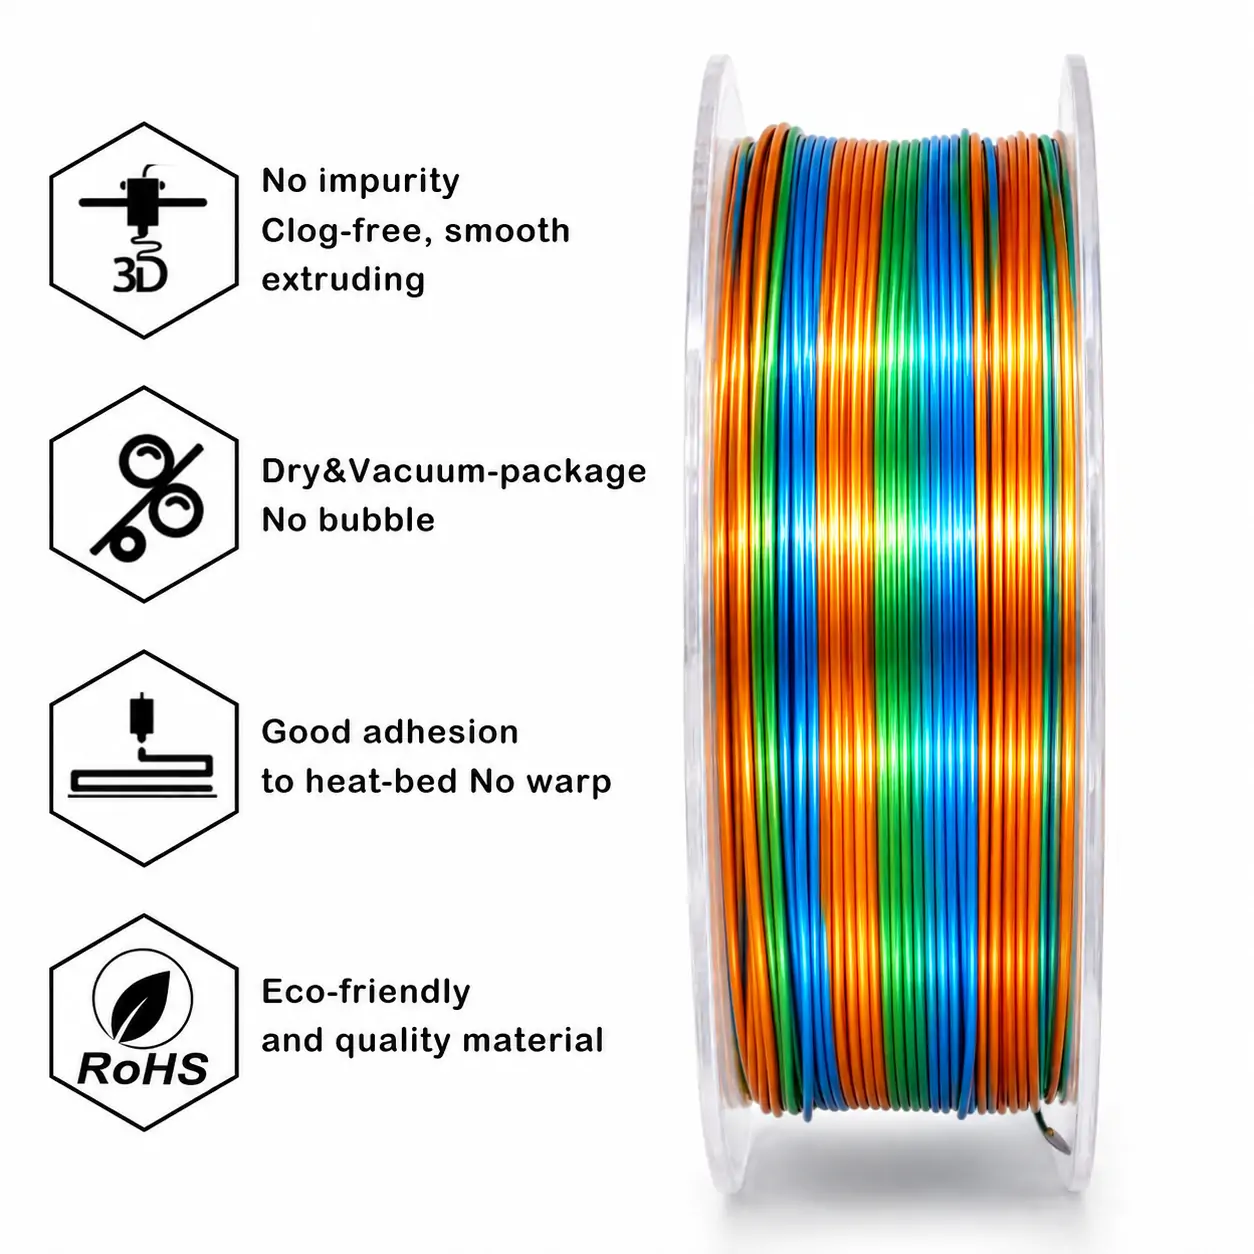
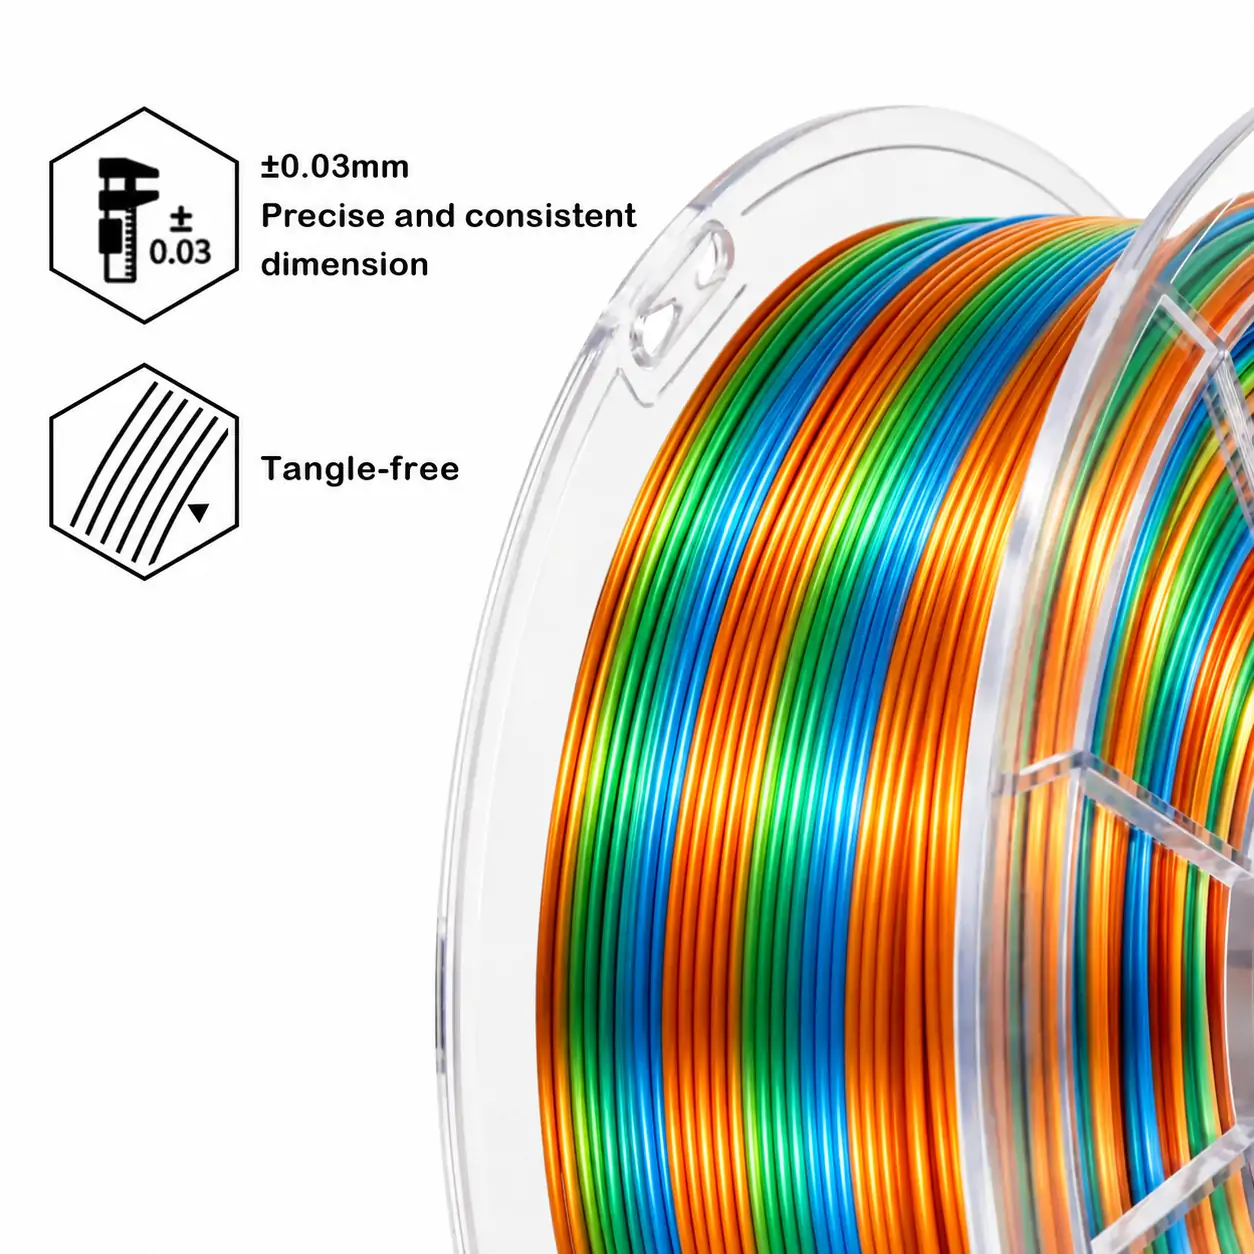
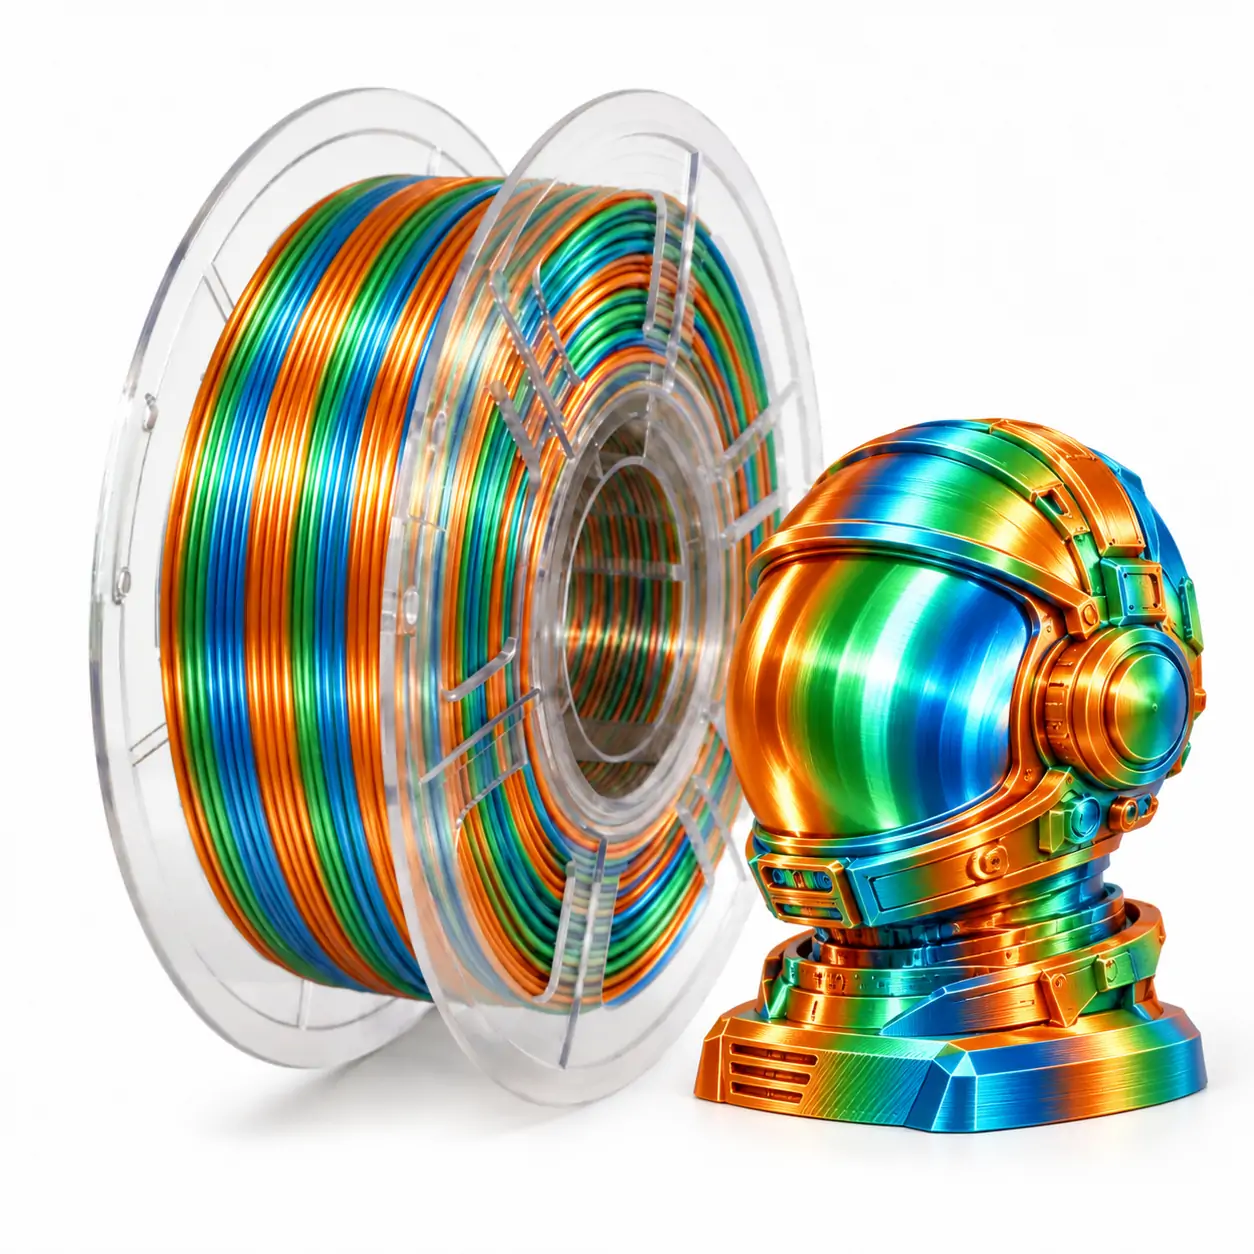
SSSRAY PLA SILK SERIES | TROPIC TRICOLOR | FACTORY-DIRECT WHOLESALE & OEM / ODM
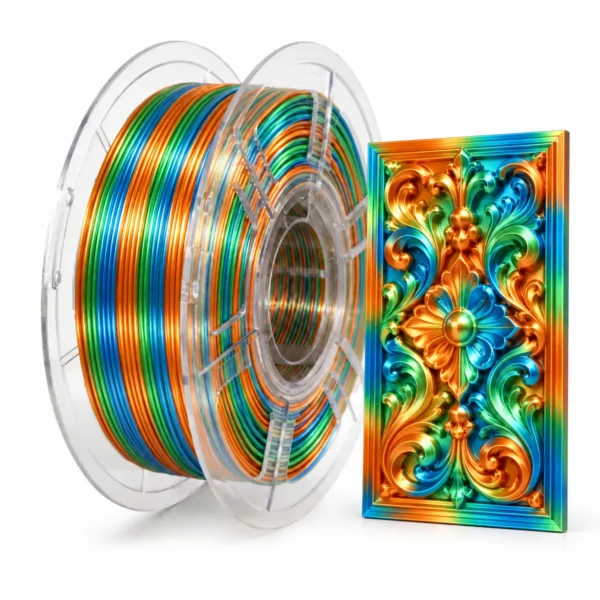
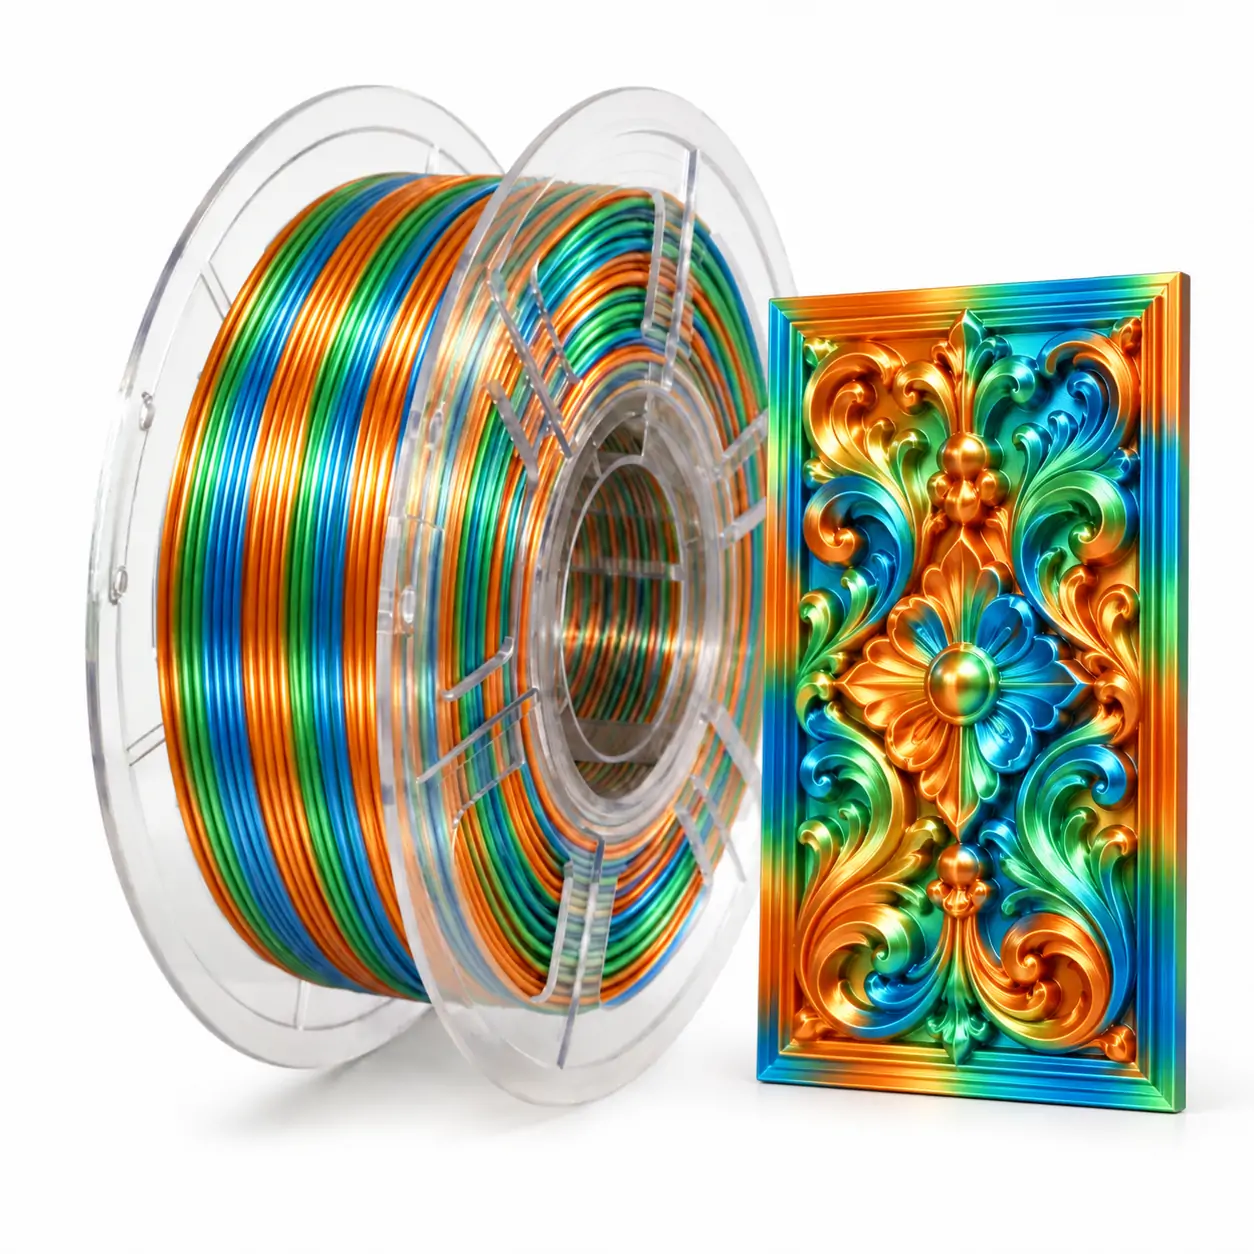
3D Printer Filament 1.75mm, SSSray Silk PLA Multicolor in Orange, Green & Blue – Многоцветный шелковый PLA-пластик for Sci-Fi Helmet Busts & Carved Wall Plaques
Factory-direct tricolor Silk PLA for distributors, private-label brands, décor studios, retailers, and decorative FDM filament ranges.
Bring a stronger visual identity to your decorative filament range with SSSray Tropic Tricolor Silk PLA. Copper-orange moves through leaf-green into azure-blue, with yellow-green and teal transition zones that add depth to sci-fi helmet busts, carved wall plaques, and ornamental reliefs. Our 1.75mm, 1kg spool format is built for established FDM/FFF workflows, with ±0.03mm diameter control and a high-speed tuning window reaching 250mm/s on capable systems.
MaterialPLA Silk
SeriesSSSray PLA Silk
Color EffectTropic Tricolor Gradient
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp210–230°C
Bed Temp45–60°C
Print Speed60–150mm/s · up to 250mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time: Standard orders 7–15 working days; customized orders 15–25 working days.
Print Performance: 60–150mm/s standard tuning window; up to 250mm/s on capable high-speed systems after flow and cooling calibration.
Product Overview
SSSray Tropic Tricolor Silk PLA brings three coordinated colors into one continuous filament: warm copper-orange, bright leaf-green, and clear azure-blue, repeating orange → green → blue along the spool. Yellow-green and teal transition zones create a richer color rhythm across larger prints. The silk-finish surface reflects light across raised edges, helmet curves, carved recesses, and ornamental scrollwork—making this grade a strong choice for display pieces where finish and visual differentiation influence the final product value. Browse the SSSray PLA Silk Series for complementary solid, dual-color, and multicolor finishes.
For distributors, wholesalers, and private-label brands, SSSray supplies this specialty colorway in a standard 1.75mm format, wound on a plastic spool with 1kg net filament weight and vacuum-sealed packaging with desiccant. The stated ±0.03mm diameter tolerance supports consistent feeding on a correctly calibrated printer. Neutral-packaging orders start at 50 rolls; OEM packaging programs typically start at 500–1,000 rolls. At our Jinhua, Zhejiang factory, extrusion, winding, diameter monitoring, color inspection, and packaging are coordinated within the production workflow. Before bulk production, we confirm the approved color reference, spool and packaging configuration, and inspection requirements against your order.
Why This Product Stands Out
Each spool combines a repeating copper-orange, leaf-green, and azure-blue color sequence with a reflective silk finish. On curved busts, raised details, and carved relief panels, the silk surface catches light across changing angles, making contours and color transitions easier to see. Retailers can position this SKU as a decorative Silk PLA option for sculptural décor, sci-fi busts, and relief panels; distributors can add it to an existing PLA Silk assortment.
Key Selling Points
Signature Three-Color Cycle
Copper-orange, leaf-green, and azure-blue repeat along one spool, with yellow-green and teal transitions for distinctive finished prints.
High-Gloss Silk Appearance
Reflective highlights bring out helmet curves, raised lettering, carved recesses, and ornamental details.
Precision Diameter Control
1.75mm filament with ±0.03mm stated tolerance supports stable feeding and consistent extrusion setup.
High-Speed Profile Potential
Designed for a practical 60–120mm/s production window, with tuning headroom up to 250mm/s on capable high-speed systems after flow and cooling calibration.
Factory-Direct Production
SSSray operates 50+ extrusion lines and publishes monthly production capacity above 1,000 tons for global B2B supply.
OEM / ODM Brand Programs
Build your own retail identity with custom labels, branded cartons, spool options, and coordinated product-line presentation.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| Repeating Orange–Green–Blue Sequence | Creates a recognizable signature colorway that stands apart from solid-color and standard rainbow PLA assortments. |
| Yellow-Green and Teal Transition Zones | Adds intermediate tones between the three main colors for a more continuous visual change across larger models. |
| Silk-Finish Surface Formulation | Reflective highlights emphasize relief depth, rounded geometry, raised details, and decorative edges. |
| 1.75mm FDM / FFF Format | Fits the most widely used open-material desktop FDM printer format and supports broad retail compatibility. |
| ±0.03mm Diameter Tolerance | Supports consistent feeding and extrusion when paired with a calibrated printer and suitable slicer profile. |
| 1kg Net Spool, Vacuum-Sealed with Desiccant | Provides a familiar retail unit with moisture-conscious packaging for warehousing and export handling. |
| Factory-Direct OEM / ODM Supply | Supports private-label branding, branded cartons, product-line planning, and volume purchasing programs. |
Commercial Value for Wholesale Buyers
Retailers can merchandise this SKU as a decorative Silk PLA option for sci-fi busts, sculptural décor, relief panels, figurines, and giftable display pieces. Distributors can add it beside standard PLA, PLA+, and other Silk PLA colors while keeping the familiar PLA material category for their customers.
SSSray supports this range with 1kg retail-ready spools, a stated ±0.03mm diameter tolerance, vacuum-sealed packaging with desiccant, neutral-packaging MOQ from 50 rolls, and OEM packaging programs typically from 500–1,000 rolls. Our 50+ extrusion lines, published monthly capacity above 1,000 tons, and export experience across 50+ countries support wholesale and private-label supply planning. For an accurate quotation, send us your required quantity, packaging artwork, destination port, and preferred Incoterm. Explore the SSSray PLA Silk range or compare our wholesale PLA supply program.
How We Work
1
Requirement & Market Review2
Color, Diameter & Packaging Confirmation3
Sample Evaluation & Print Feedback4
Label, Carton & OEM Approval5
Production Scheduling & QC6
Final Inspection & ShipmentMaterial Comparison Guide
| Material | Surface & Appearance | Typical Functional Profile | Typical Print Conditions | Typical Use |
|---|---|---|---|---|
| SSSray Tricolor Silk PLA | Silk sheen with repeating orange, green, and blue transitions. | PLA-based decorative material; not positioned as an engineering-grade load-bearing material. | PLA-family nozzle and bed temperatures; moderate outer-wall speed is useful for surface finish. | Sci-fi busts, carved plaques, relief panels, figurines, display décor. |
| PLA+ / PLA Pro | Appearance depends on grade and pigment; commonly supplied in solid colors and varied finishes. | Formulation-dependent impact and toughness modifications compared with standard PLA. | Generally similar to PLA, with settings dependent on the specific blend. | General-purpose models, prototypes, everyday printed parts. |
| PETG | Often glossy or semi-gloss; surface behavior varies by grade. | Typically more ductile and impact-tolerant than standard PLA; can show stringing. | Usually requires higher nozzle temperatures than PLA and careful cooling/adhesion tuning. | Functional housings, brackets, containers, and utility parts. |
| ABS / ASA | Commonly supplied in matte or satin finishes; ASA is selected for outdoor exposure. | Higher temperature capability than PLA; ABS/ASA shrinkage and warping require process control. | Higher nozzle and bed temperatures; an enclosure is commonly used. | Functional enclosures, automotive-style parts, and outdoor components (ASA). |
Material behavior varies by resin grade, formulation, printer, and processing conditions. Select the material against the end-use requirements rather than appearance alone.
Technical Specifications
| Product Name | 3D Printer Filament 1.75mm, SSSray Silk PLA Multicolor in Orange, Green & Blue – Многоцветный шелковый PLA-пластик for Sci-Fi Helmet Busts & Carved Wall Plaques |
|---|---|
| Material | PLA Silk (Polylactic Acid) with a silk-finish formulation |
| Product Series | SSSray PLA Silk Series – Tricolor Gradient Line for Sci-Fi Busts & Relief Décor |
| Color Effect | Tropic Tricolor Silk Gradient |
| Color Sequence | Orange → Green → Blue → Orange, repeating along the filament length |
| Transition Colors | Yellow-green between orange and green; teal between green and blue |
| Filament Diameter | 1.75mm standard; 2.85mm available for selected grades and qualified production projects |
| Diameter Tolerance | ±0.03mm |
| Roundness Deviation | ≤0.02mm |
| Net Filament Weight | 1kg per spool |
| Gross Weight | 1.3kg per packaged unit |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Printing Technology | FDM / FFF |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, subject to spool fit, hotend, and slicer settings (e.g. Bambu Lab, Prusa, Creality, Anycubic, and Elegoo) |
| Typical Applications | Sci-fi helmet busts, astronaut models, carved wall plaques, acanthus relief panels, figurines, and decorative display models |
| OEM / ODM | Supported; packaging, labels, and private-label project details are subject to order review |
| Technical Documents | Current controlled PLA Silk Series TDS and applicable SDS available for buyer qualification; product-specific acceptance limits are confirmed against the approved order specification. |
PLA Silk Series Reference Properties
| Property | Typical Value | Test Condition / Reference |
|---|---|---|
| Melt Flow Rate (MFR) | 6–9 g/10min | 190°C / 2.16kg; ISO 1133 |
| Tensile Strength (XY) | 45 ± 2 MPa | ISO 527-2 / ASTM D638 |
| Tensile Modulus (XY) | 2,448 MPa | ISO 527-2 / ASTM D638 |
| Elongation at Break (XY) | 10–15% | ISO 527-2 / ASTM D638 |
| Flexural Strength (XY) | 75 MPa | ISO 178 / ASTM D790 |
| Flexural Modulus (XY) | 2,580 MPa | ISO 178 / ASTM D790 |
| Notched Izod Impact Strength | 5–6 kJ/m² | ISO 180 / ASTM D256 |
| Notched Charpy Impact Strength | 5–7 kJ/m² | ISO 179-1 |
| Shore Hardness | 84 Shore D | ISO 868 / ASTM D2240 |
| Glass Transition Temperature (Tg) | 56.8°C | ISO 11357-2 / ASTM D3418 |
| Heat Deflection Temperature (HDT) | 57°C @ 0.455MPa / 52°C @ 1.82MPa | ISO 75-2 / ASTM D648 |
| Vicat Softening Temperature | 63°C | ISO 306 / ASTM D1525 |
| Melting Temperature | 150–165°C | ISO 11357-2 / ASTM D3418 |
| Water Absorption (24h) | 0.3–0.4% | ISO 62 |
These are typical PLA Silk Series reference values, not guaranteed acceptance limits for every colorway or production lot. For supplier qualification, request the current controlled TDS and confirm the applicable test method, specimen preparation, conditioning, and acceptance limits in the purchase specification. The agreed product specification governs the supplied grade and order.
Recommended Print Settings
| Parameter | Recommended Starting Guidance |
|---|---|
| Nozzle Temperature | 210–230°C recommended; 220°C is a strong starting point for balanced flow and silk sheen. |
| Bed Temperature | 45–60°C general range; start at 50–55°C on PEI. Bambu Lab profiles may use 35–45°C on supported plates. |
| Standard Print Speed | 60–150mm/s for everyday production and decorative models; tune against the printer’s hotend flow capacity. |
| High-Speed Operating Window | 120–250mm/s on capable high-speed systems after flow, cooling, and extrusion calibration. |
| Outer-Wall Speed | 30–60mm/s for a brighter, more even silk surface and clean visible contours. |
| Inner Wall / Infill Speed | 80–150mm/s starting range; increase toward 250mm/s only when the hotend maintains stable flow. |
| Layer Height | 0.12–0.24mm with a 0.4mm nozzle; 0.16–0.20mm balances surface detail and print productivity. |
| Cooling Fan | 80–100% after the first 2–3 layers; use full cooling for bridges and overhangs where needed. |
| Retraction – Bowden | 3–5mm at 25–40mm/s as a starting range; tune to the extruder path. |
| Retraction – Direct Drive | 0.5–1.2mm at 25–40mm/s as a starting range. |
| Wall Count | 2–3 perimeters for decorative models; 3 walls for larger display pieces and raised relief structures. |
| Infill | 10–20% for lightweight décor; 30–50% for heavier display pieces where added internal support is useful. |
| First-Layer Speed | 20–30mm/s for controlled first-layer bonding and repeatable bed adhesion. |
| Build Plate | Smooth or textured PEI is a practical first choice. On glass, use a compatible adhesive and follow the plate manufacturer’s guidance. |
| Drying / Moisture Recovery | 50–55°C for 4–6 hours in a controlled filament dryer when moisture-related popping, stringing, or surface defects appear. |
For production speed, tune the outer wall separately from inner walls and infill. The 250mm/s upper window is intended for high-speed machines with sufficient hotend flow—not a universal setting for every printer or model.
Print Optimization Guide
| Optimization Item | Practical Guidance |
|---|---|
| Show the Color Sequence | Use taller or larger models when the design needs room to display more of the repeating orange-green-blue transition. |
| Choose Model Geometry | Raised relief, curved helmet shells, rounded busts, and broad decorative surfaces make color changes easier to see. |
| Preserve Silk Sheen | Use a moderate outer-wall speed and avoid unnecessary speed changes across visible surfaces. |
| Refine Fine Details | Use a 0.12–0.16mm layer height for fine ornamental details with a 0.4mm nozzle, then verify cooling and extrusion. |
| Control First-Layer Adhesion | Clean the build plate, level it correctly, and keep the first layer speed conservative. |
| Manage Moisture | Keep the spool sealed with desiccant between jobs; if moisture-related defects appear, dry at 50–55°C for 4–6 hours in a controlled filament dryer. |
| Reduce Stringing | Calibrate retraction and travel behavior in small steps; excessive retraction can create inconsistent feeding. |
Printer Brand Starting Settings
| Printer Brand / Family | Nozzle | Bed | Outer Wall | Inner Wall / Infill | Setup Note |
|---|---|---|---|---|---|
| Bambu Lab (A / P / X series) | 210–240°C | 35–45°C | 30–60mm/s | 80–150mm/s; tune toward 200–250mm/s only when the hotend flow limit and surface quality remain stable | Use the plate-specific PLA Silk profile; keep visible outer walls slower to preserve gloss. |
| Prusa (MK / CORE series) | 210–230°C | 50–60°C | 30–60mm/s | 60–120mm/s | Start with a clean PEI sheet and tune cooling for bridges and fine relief. |
| Creality (Ender / K series) | 210–230°C | 50–60°C | 30–50mm/s | 50–100mm/s | Set retraction for Bowden or direct drive; verify first-layer adhesion. |
| Anycubic (Kobra series) | 210–230°C | 45–55°C | 30–50mm/s | 50–100mm/s | Calibrate flow and cooling before raising acceleration or infill speed. |
| Elegoo (Neptune series) | 210–230°C | 45–55°C | 30–50mm/s | 50–100mm/s | Use a PLA profile as the base and tune the outer wall for the required sheen. |
These brand-family values are production starting points, not locked presets. Use the temperature range suited to the specific build plate and printer profile. Actual sustainable speed depends on hotend volumetric flow, nozzle size, cooling, acceleration, and model geometry; validate the selected profile on the target printer before production.
Performance Characteristics
| Characteristic | PLA Silk Performance | What It Means in Finished Prints |
|---|---|---|
| Silk Surface Reflection | High-gloss, light-reflective finish | Highlights raised edges, curved helmet shells, carved recesses, and ornamental relief surfaces. |
| Three-Color Transition | Repeating copper-orange → leaf-green → azure-blue sequence | Color placement changes with extrusion length, model height, and the spool’s position in its repeating cycle. |
| Transition Blending | Yellow-green and teal intermediate tones | Creates a more continuous color story than a simple two-color switch. |
| Relief and Contour Definition | Reflective highlights across raised and recessed geometry | Well suited to acanthus scrolls, sculpted busts, carved plaques, and display surfaces with changing angles. |
| Layer-Line Appearance | Silk sheen can soften the visual prominence of layer lines | Use 0.16–0.20mm layers and a controlled outer-wall speed; the finish does not eliminate layer lines. |
| Print Process Behavior | Familiar PLA-family processing window | Generally easier to manage on open-frame printers than ABS/ASA; clean bed preparation and first-layer control remain important. |
| Thermal Use Profile | Tg 56.8°C; HDT 57°C @ 0.455MPa / 52°C @ 1.82MPa | Designed for decorative and indoor display use, not sustained high-temperature service. |
Surface results vary with color-cycle position, model geometry, nozzle size, temperature, cooling, and wall speed. This grade is positioned for decorative and display prints rather than sustained high-temperature engineering service.
Applications
| Application Focus | Practical Notes |
|---|---|
| Sci-Fi Helmet Busts | Curved shells and raised details can show the changing copper-orange, green, and blue tones across the model. |
| Retro Astronaut & Character Busts | Use moderate outer-wall speeds to retain visible contours and a consistent silk surface character. |
| Carved Wall Plaques | Broad relief surfaces and recessed carving can catch highlights from the silk finish. |
| Acanthus Scroll Relief Panels | Ornamental leaves and raised scrollwork provide multiple surfaces for the gradient to read across. |
| Decorative Figurines | Suitable for display-oriented figures, collectibles, and giftable printed objects. |
| Interior Display Décor | Consider larger formats when the design needs a more visible color transition; avoid positioning as outdoor or high-heat material. |
| Retail Demonstration Models | Useful for sample displays that communicate color, finish, and decorative application to end customers. |
Storage Guide
- Keep each spool in its original vacuum-sealed moisture-barrier bag with the supplied desiccant until loading.
- After opening, return the spool to a dry box or resealable moisture-barrier bag with fresh desiccant between print jobs.
- Store at 15–25°C in a dry, shaded area; keep the spool away from direct sunlight, heat sources, and dust.
- Keep storage humidity below 50% RH where practical and minimize open-air exposure during production shifts.
- If popping, stringing, or surface defects indicate moisture uptake, dry at 50–55°C for 4–6 hours in a controlled filament dryer, then store in a dry box.
OEM / ODM Services
SSSray manufactures and supplies filament for distributors, importers, retailers, and private-label brands. Our factory in Jinhua, Zhejiang, China operates 50+ extrusion lines, publishes monthly capacity above 1,000 tons, and serves buyers in 50+ countries. For this tricolor Silk PLA, we coordinate filament production with custom labels, branded cartons, spool presentation, barcode and language-label requirements, and a consistent look across your decorative filament range. Our in-house color laboratory supports Pantone/RAL color matching and custom color development for OEM programs.
MOQ Reference: Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls, depending on the approved packaging scope and production plan.
Color & Specification Review: The standard color sequence is orange → green → blue. Custom color directions, diameter options, and spool requirements are subject to technical and production confirmation before quotation.
Project Support: Share your target market, annual demand, packaging artwork, printer requirements, and document needs. Our sales and production teams coordinate specification review, sample evaluation, packaging approval, production scheduling, and export dispatch. For a complete factory overview, visit our 3D printer filament manufacturing facility.
Quality Control
| Control Point | Inspection Focus | Buyer-Relevant Record |
|---|---|---|
| 1. Raw Material & Lot Traceability | Incoming resin grade, batch identity, material preparation, and production-lot tracking. | Lot identification and approved material specification. |
| 2. Inline Diameter Monitoring | Laser measurement during extrusion to control the 1.75mm filament diameter against the stated ±0.03mm tolerance. | Diameter readings and lot-level inspection records under the agreed QC plan. |
| 3. Moisture & Melt-Flow Control | Moisture analysis and melt-flow testing to monitor material condition and extrusion consistency. | Applicable test records and agreed acceptance criteria. |
| 4. Color & Surface Inspection | Color reference checks across copper-orange, leaf-green, azure-blue, and transition zones; surface inspection for visible defects. | Approved color sample and appearance reference for repeat orders. |
| 5. Winding, Weight & Packaging | Spool condition, winding alignment, 1kg net weight, vacuum seal, and desiccant inclusion. | Weight and pack inspection records against the order specification. |
| 6. Print Validation & Pre-Shipment Review | Print trials appropriate to the material, final appearance sampling, carton marks, and shipment preparation. | COA supplied with every shipment, documenting measured lot values; additional inspection records follow the agreed order plan. |
Before shipment, our QC team checks the batch against the approved order specification: inline diameter readings, moisture and melt-flow results, color and surface appearance, 1kg net spool weight, winding, vacuum seal, and desiccant inclusion, together with print-validation samples. The COA supplied with each shipment records measured lot values; any additional inspection records follow the QC plan agreed for the order.
Technical Documents & Compliance Support
SSSray supplies technical documents for supplier qualification and export review. The PLA Silk Series TDS provides series-level material reference properties and starting print guidance; the applicable SDS provides material safety information. For each inquiry, share the destination market and buyer requirements so our team can confirm the current document revisions, applicable RoHS/REACH declarations or test reports, and batch records for the selected grade.
| Document / Factory Standard | Buyer Support |
|---|---|
| PLA Silk Series TDS | Request the current controlled revision for series-level reference properties and starting print guidance. Confirm grade applicability and any buyer-specific acceptance limits before qualification. |
| SDS / MSDS | Request the applicable SDS revision for the selected PLA Silk material and destination-market review. |
| ISO 9001 | SSSray factory quality-management certification supports supplier qualification; certificate scope and current revision are available on request. |
| RoHS / REACH | Applicable declarations or test reports are confirmed against the selected material, destination market, and buyer’s requested scope before order approval. |
| COA / Batch Records | Each shipment includes a batch COA documenting measured lot values. The COA can be matched to the Batch ID shown on the master carton and individual spool labels. |
| Third-Party Testing | Independent laboratory testing, including SGS testing, can be arranged when the buyer specifies the required test method and scope. |
To prepare the right document pack, send us the product grade, destination country, intended application, and any buyer-required standards or acceptance limits. Our team will confirm the applicable document revisions and batch records for your sample or bulk order.
Frequently Asked Questions
What is the color sequence of this tricolor Silk PLA?
The filament follows a repeating orange → green → blue → orange sequence. The main colors are warm copper-orange, bright leaf-green, and clear azure-blue, with yellow-green and teal transition areas.
Will every printed model show all three colors?
The visible color distribution depends on the model size, print height, wall count, extrusion length, and where the spool is in its color cycle. Larger or taller models generally provide more room for the transitions to appear, but every model will not display the same color layout.
What kind of surface finish does the filament provide?
The silk-finish formulation is intended to create a reflective decorative surface. For relief panels and sculpted busts, use a moderate outer-wall speed and tune temperature and cooling on a sample print to balance sheen and detail.
What nozzle and bed temperatures should I start with?
Start at 220°C nozzle and 50–55°C bed temperature. Use 30–60mm/s for outer walls to protect the silk sheen, then run inner walls and infill at 80–150mm/s. Capable high-speed systems can be tuned toward 250mm/s after flow and cooling calibration.
Which 3D printers are compatible with this filament?
It is designed for most open-material 1.75mm FDM/FFF printers, including common Bambu Lab, Prusa, Creality, Anycubic, and Elegoo systems. Confirm spool fit, hotend capability, and slicer settings for your specific printer before production use.
Is this material intended for structural or high-temperature parts?
No. This is a decorative PLA-based Silk filament intended for display models and general-purpose prints. For parts requiring higher heat resistance, impact performance, or engineering specifications, select a material designed and qualified for that end use.
What are the MOQ and lead-time arrangements?
Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls. Standard orders are generally scheduled for 7–15 working days, while customized orders are generally 15–25 working days, subject to order details and production confirmation.
Can I request samples and technical documents?
Qualified B2B buyers may apply for up to 3 full-size 1kg sample spools free of charge. Standard sample preparation is typically 3–5 working days; freight is arranged separately, with the payer and route confirmed before dispatch. The latest PLA Silk Series TDS and applicable SDS are available for technical review.
Source Tricolor Silk PLA for Your Decorative Filament Range
Source this signature tricolor Silk PLA directly from SSSray. Request bulk pricing, apply for sample rolls, or build a private-label program with your target colors, packaging artwork, and annual volume.



Related products
-

SSSray PLA+ in Jet Black: 3D Printer Filament for Electronics Enclosures & Fan Grilles – PLA+ Filament Schwarz
-
SSSray Red PLA+ Filament for Sculpted Décor & Utility Hooks – Signal Red 3D Printer Filament, Filamento PLA+ Vermelho
-
Rainbow Glow-in-the-Dark PLA Filament 1.75mm 1kg – Multi-Color Luminous Gradient for FDM Printers, Ideal for Novelty Toys & Display Models
-
Pink Crystal PLA Filament 1.75mm 1kg – High Translucency Glossy Finish for FDM 3D Printing, Ideal for Decorative Models & Jewelry Prototypes