Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

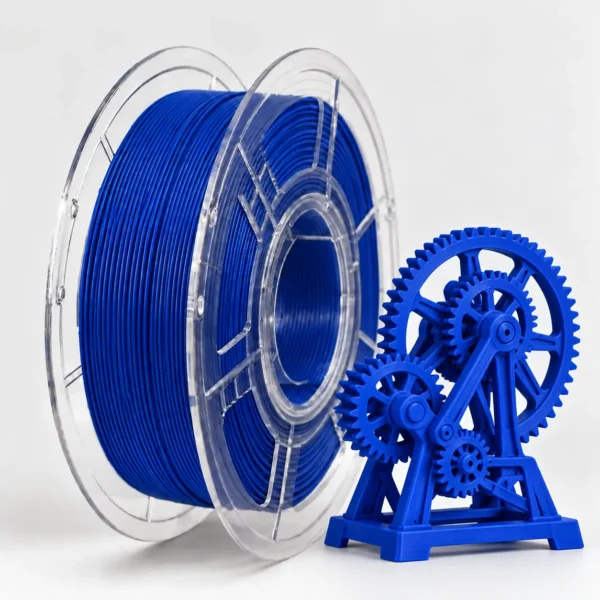
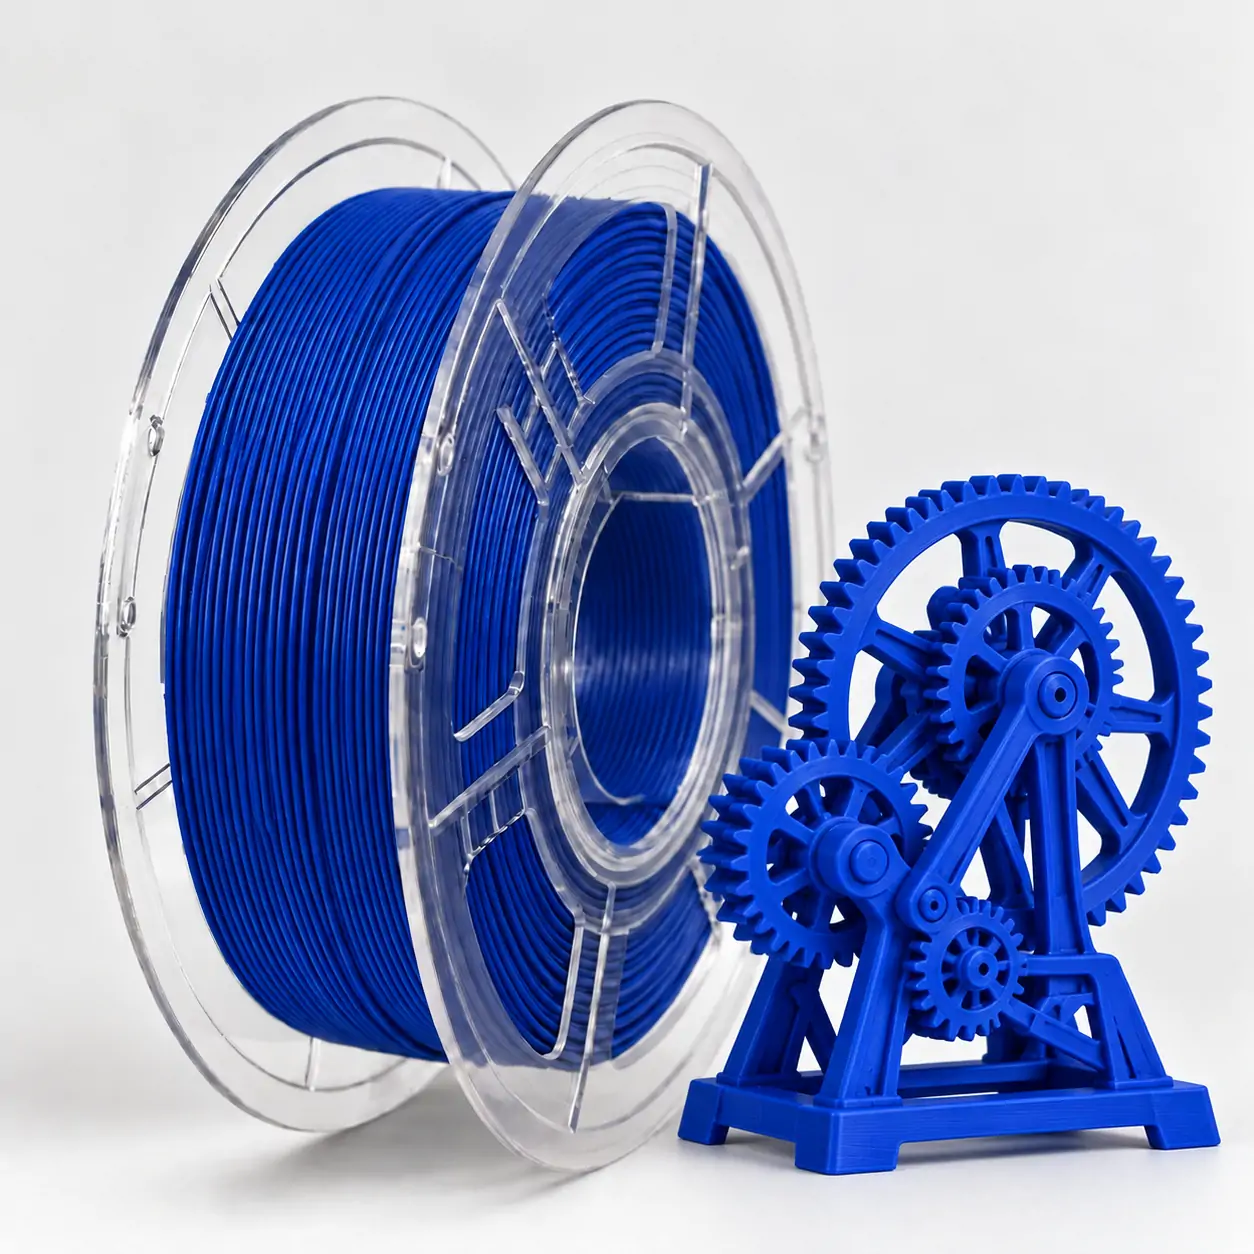
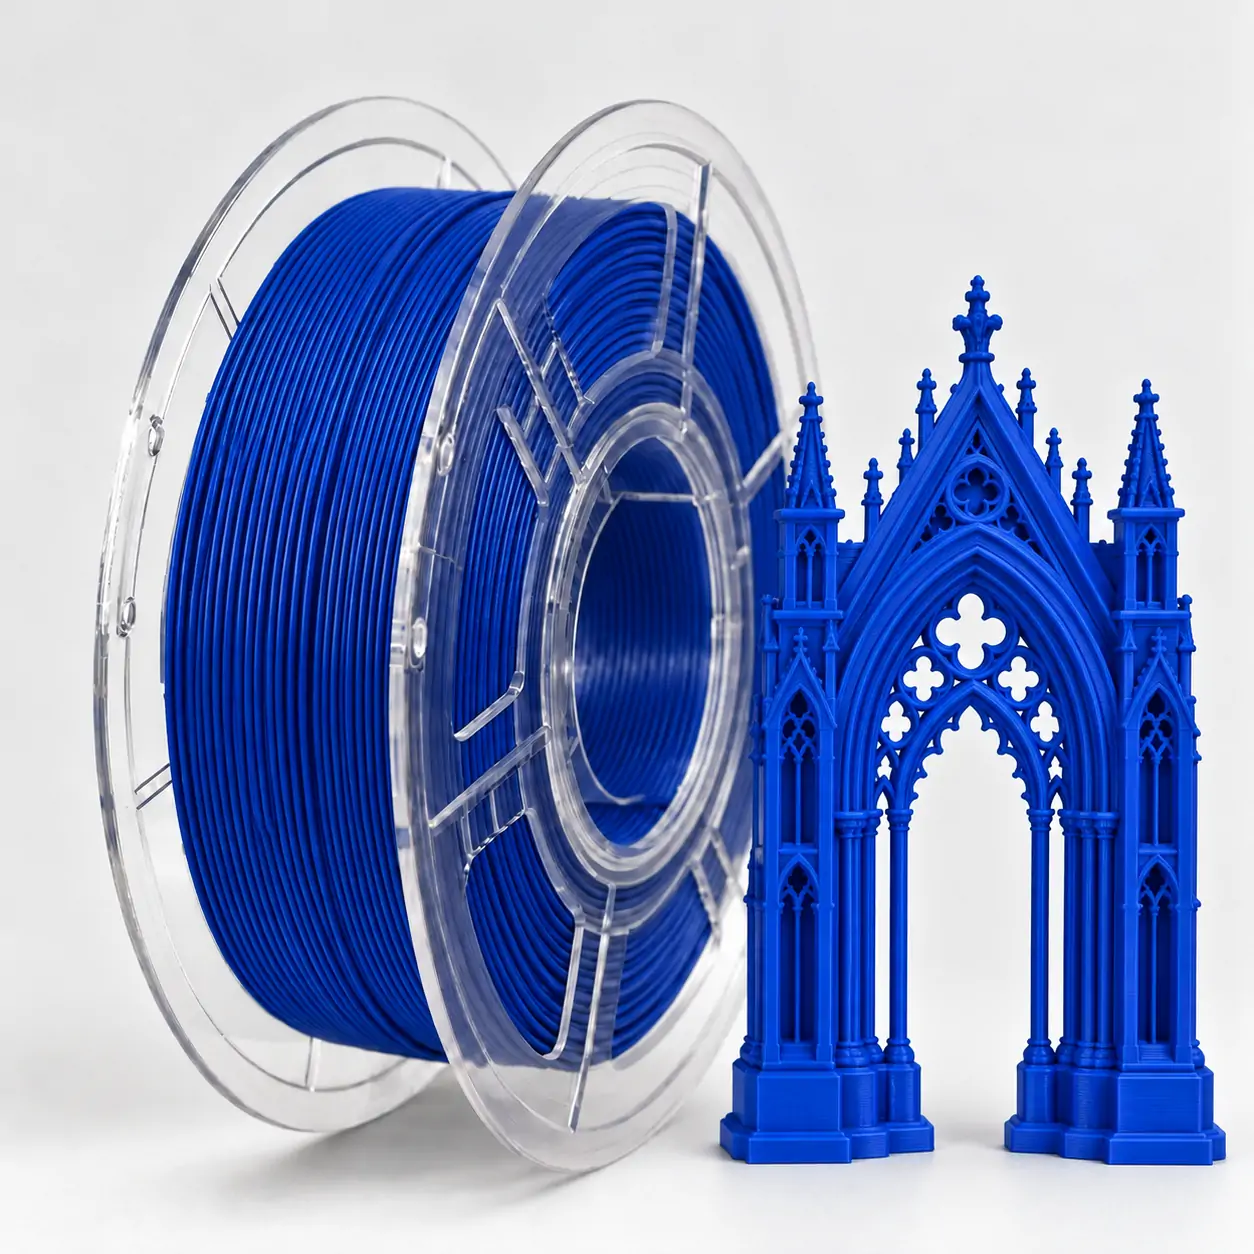
PLA Basic Series | Royal Blue | Wholesale & OEM / ODM
SSSray PLA Basic in Royal Blue — 파란색 PLA 필라멘트 | 1.75mm 3D Printer Filament for Fine-Detail Miniatures & Gear Mechanisms
Royal Blue PLA Basic for distributors and private-label programs that need saturated color, clean fine-detail reproduction, and dependable day-to-day FDM printability.
We produce this deep, opaque Royal Blue with an even satin sheen and a slight cobalt tone for miniatures, gear mechanisms, architectural models, educational parts, and broad retail filament programs.
MaterialPLA Basic
SeriesSSSray PLA Basic Series
Color EffectRoyal Blue / Even Satin
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp200–230°C
Bed Temp45–60°C
Print Speed60–150 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 working days; customized orders typically 15–25 working days.
Product Overview
SSSray PLA Basic in Royal Blue is our standard-grade PLA option for buyers who want dependable everyday printability with a strong, saturated core color. The deep medium-dark blue carries a slight cobalt tone and an even satin sheen, helping miniature edges, gear teeth, arches, lettering, and recessed features stay visually clear. We hold the 1.75mm filament to ±0.03mm, wind it on a plastic spool, and vacuum seal each standard retail unit with desiccant for export storage and channel distribution.
For distributors, 3D-printing stores, education suppliers, and private-label programs, this Royal Blue SKU combines a familiar PLA workflow with a finish that works well in product photography and printed samples. Standard 1kg spools fit mainstream retail programs; 2.85mm diameter, 3kg/5kg formats, custom color matching, labels, boxes, and spool options can be discussed for qualified B2B projects.
Why This Product Stands Out
Royal Blue is a practical core SKU when your customers print small geometry, display mechanisms, architectural parts, and detailed models. The satin surface reduces mirror-like glare while the cobalt-leaning blue keeps edges and relief visible. We combine that color presentation with ±0.03mm diameter control, vacuum-sealed packaging, low-warp PLA processing, and flexible private-label support so buyers can qualify one SKU and expand the same PLA Basic program across additional colors.
Key Selling Points
Stable Diameter Control
±0.03mm diameter control supports steady feeding and repeatable extrusion across routine PLA production runs.
Fine-Detail Definition
Royal Blue satin surfaces keep miniature edges, gear teeth, recesses, and architectural geometry visually clear.
Royal Blue Shelf Appeal
Deep, opaque medium-dark blue with a slight cobalt tone gives distributors a distinct core-color option without a specialty-material learning curve.
Low-Warp PLA Workflow
Standard PLA behavior supports straightforward first-layer setup and low warping under recommended print conditions.
Export-Oriented Supply
1kg retail-ready format, vacuum packaging, 50-spool neutral MOQ, and 7–15 day standard lead time support wholesale purchasing.
OEM / ODM Ready
We support custom labels, branded boxes, color programs, spool options, and private-label development for qualified projects.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| Royal Blue, Even Satin Sheen | Gives miniatures, gears, architecture, and display models a saturated blue finish with readable surface detail |
| 1.75mm ±0.03mm Diameter | Supports consistent feeding across mainstream open-material 1.75mm FDM printer ecosystems |
| Low-Warp PLA Printability | Supports an accessible workflow for retail, education, and everyday prototyping |
| Vacuum Sealed with Desiccant | Helps protect filament condition through storage, export handling, and downstream distribution |
| 1kg Plastic Spool Format | Fits a familiar retail format, with 3kg/5kg options available for qualified project orders |
| OEM / ODM Support | Supports private label, custom packaging, spool presentation, and coordinated color-line development |
Royal Blue PLA Basic for Distributor & Private-Label Programs
We supply Royal Blue as a core opaque-blue option for miniature, education, architectural, mechanical-demo, and general-purpose PLA demand. The satin finish keeps geometry readable in printed samples and product photography, while the standard PLA workflow remains familiar to end users. Procurement teams can start with 50-spool neutral orders for qualification, move to 500–1,000-spool OEM packaging for branded programs, and extend the same PLA Basic specification into coordinated color ranges as demand grows.
How We Work
1
Requirement Review
2
Specification Confirmation
3
Sample Evaluation
4
Packaging Discussion
5
Production Arrangement
6
Inspection & Shipment
Material Comparison Guide
| Material | Typical Nozzle | Typical Bed | Material Behavior | Typical Use |
|---|---|---|---|---|
| PLA Basic | 190–240°C | 40–60°C | Low warping, stiff feel, strong detail reproduction, high cooling demand for sharp features | Miniatures, visual prototypes, education, architectural and general-purpose models |
| PLA+ / PLA Pro | 205–235°C | 45–65°C | PLA-based printability with formulation-dependent toughness improvement | General-purpose parts, housings, light-duty functional prototypes |
| PETG | 220–250°C | 60–80°C | More ductile than standard PLA; higher temperature demand and greater stringing sensitivity | Enclosures, brackets, fixtures, practical functional parts |
| ABS / ASA | 240–260°C | 90–110°C | Higher heat capability than PLA; stronger warping control and enclosure management usually required | Functional parts; ASA is preferred where outdoor weathering matters |
Technical Specifications
| Product Name | SSSray PLA Basic in Royal Blue — 파란색 PLA 필라멘트 | 1.75mm 3D Printer Filament for Fine-Detail Miniatures & Gear Mechanisms |
|---|---|
| Material | PLA Basic (Polylactic Acid), standard grade for FDM / FFF printing |
| Series | SSSray PLA Basic Series – Saturated-Color Printing for Intricate Miniatures & Mechanical Models |
| Color / Effect | Royal Blue, even satin sheen; deep saturated medium-dark blue with a slight cobalt tone; solid and opaque |
| Filament Diameter | 1.75mm standard; 2.85mm available on request |
| Tolerance | ±0.03mm |
| Net Weight | 1kg standard; 3kg and 5kg options available on request |
| Gross Weight | 1.3kg |
| Spool Type | Plastic spool; custom spool options available for qualified OEM projects |
| Packaging | Vacuum sealed with desiccant |
| Printer Compatibility | Most open-material 1.75mm FDM / FFF printers, including Bambu Lab, Prusa, Creality, Flashforge, Anycubic, and Elegoo platforms |
| Typical Applications | Fine-detail miniatures, gear mechanisms, architectural models, educational demonstrators, display parts, and general-purpose prototypes |
| Compliance | RoHS compliant |
| OEM / ODM | Supported: private label, labels, boxes, color matching, spool options, and project packaging |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | 200–230°C |
| Usable Nozzle Range | 190–240°C |
| Recommended Bed Temperature | 45–60°C |
| Optional Bed Condition | 25–45°C can work on selected high-adhesion PLA build surfaces after first-layer tuning |
| Recommended Print Speed | 60–150 mm/s |
| Tunable Speed Range | 40–250 mm/s on suitable hardware; raise nozzle temperature as volumetric flow demand increases |
| Layer Height | 0.12–0.28mm; 0.12–0.16mm preferred for miniature detail |
| Cooling Fan | 80–100% after the first 2–3 layers; reduce cooling on the first layer for adhesion |
| Retraction | Direct drive: 0.8–1.5mm at 30–45 mm/s; Bowden: 3–5mm at 30–45 mm/s as starting references |
| Wall Count | 2–4 perimeters; use 3–4 where gear teeth or thin mechanical features need more shell support |
| Infill | 15–20% for decorative models; 30–50% for general-purpose prototypes where extra internal support is useful |
| First Layer Speed | 20–30 mm/s |
| Bed Adhesion | Smooth PEI, textured PEI, or glass; use adhesive or release layer only where the selected plate requires it |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Miniature Detail | Use 0.12–0.16mm layers, controlled outer-wall speed, and strong part cooling to keep faces, recesses, and edges crisp |
| Gear Tooth Definition | Use 0.16–0.20mm layers, 3–4 walls, and calibrated flow / dimensional compensation before evaluating fit |
| Satin Surface Consistency | Keep outer-wall speed and nozzle temperature stable across visible surfaces to reduce gloss variation |
| First-Layer Reliability | Clean the build surface, use 20–30 mm/s first-layer speed, and tune Z-offset / first-layer flow for the selected plate |
| Moisture Recovery | If stored filament shows popping, stringing, or rough extrusion, dry at 50–55°C for about 8 hours, then reseal with desiccant |
| Higher-Throughput Printing | Increase temperature gradually with flow demand and verify layer bonding before using the upper end of the tunable speed range |
Printer Brand Starting Settings
| Printer Brand | Nozzle | Bed | Speed | Starting Notes |
|---|---|---|---|---|
| Bambu Lab | 200–230°C | 35–55°C | 80–180 mm/s | Start from a PLA profile; reduce outer-wall speed when miniature surface detail is the priority |
| Prusa | 200–225°C | 40–60°C | 60–120 mm/s | Use full part cooling after initial layers and tune first layer to the selected PEI sheet |
| Creality | 200–230°C | 50–60°C | 60–150 mm/s | Use a standard PLA profile, then calibrate flow and pressure / linear advance for gear detail |
| Flashforge | 200–230°C | 45–60°C | 60–150 mm/s | Use 0.12–0.20mm layers when fine miniature definition matters more than throughput |
| Anycubic / Elegoo | 200–230°C | 50–60°C | 60–150 mm/s | Confirm plate adhesion and cooling behavior before increasing speed on high-flow machines |
Use these as SSSray starting values. Final settings should be tuned to printer model, nozzle size, build surface, slicer, and model geometry.
Performance Characteristics
| Characteristic | Production Reference | Buyer Implication |
|---|---|---|
| Diameter Control | 1.75mm ±0.03mm | Supports predictable feeding for retail, education, and print-farm qualification workflows |
| Color Presentation | Royal Blue, opaque, even satin sheen | Maintains a clear cobalt-leaning blue identity across miniatures, gears, and architectural surfaces |
| Warping Behavior | Low under recommended PLA settings | Reduces setup burden for open-frame and enclosed FDM printers compared with higher-shrink materials |
| Detail Response | Compatible with 0.12–0.16mm fine-detail layer heights | Useful for miniature edges, small gear features, texturing, and ornamental geometry |
| Cooling Response | 80–100% part cooling after initial layers | Helps preserve bridges, overhang edges, and small features during detailed PLA printing |
| Service Positioning | Standard PLA; stiff and easy to print, with limited heat tolerance versus engineering polymers | Best for visual, educational, prototype, and general-purpose parts rather than high-heat service |
Applications
| Application Focus | Practical Notes |
|---|---|
| Fine-Detail Miniatures | The satin Royal Blue surface keeps panel lines, armor edges, facial forms, and recessed detail visible without strong silk-like glare |
| Gear Mechanisms & Demonstrators | Useful for educational gear trains, motion demonstrators, fit checks, and display mechanisms; not positioned for high-load drivetrain service |
| Architectural Models | Deep blue creates clear contrast on arches, ribs, lattice structures, facades, and ornamental geometry |
| Education & Classroom Models | Easy PLA workflow suits repeatable teaching prints, mechanical demonstrations, geometry models, and project kits |
| Retail Decorative Models | A saturated core color supports tabletop pieces, desk models, organizers, display objects, and consumer craft projects |
| General-Purpose Prototypes | Suitable for visual prototypes, housings, light-handling jigs, and form / fit checks where high heat is not expected |
Storage Guide
- Keep unopened spools in their original vacuum-sealed packaging until use
- After opening, return the spool to a sealed bag or dry box with fresh desiccant
- Store away from direct sunlight, heat sources, and prolonged high-humidity exposure
- If moisture symptoms appear, dry at 50–55°C for about 8 hours before reprinting
- Secure the filament end in the spool holes before storage to prevent loose coils and cross-winding
OEM / ODM Services
We support distributors, wholesalers, importers, private-label brands, education suppliers, and project buyers with flexible PLA Basic programs. Available options include neutral packaging, custom labels, branded retail boxes, barcode / SKU labeling, color matching, custom spool presentation, mixed-color purchasing plans, and 3kg / 5kg spool discussions for qualified projects.
MOQ Reference: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools. Standard production lead time is 7–15 working days, while customized programs are typically 15–25 working days after artwork and specification confirmation.
Quality Control
- Diameter and ovality checks against the ±0.03mm production specification
- Royal Blue color and surface-appearance comparison during batch release
- Winding appearance and filament-end security inspection before packing
- Vacuum-seal and desiccant inclusion check for each standard retail unit
- Spool, label, SKU, and outer-carton identification check against the order specification
- Pre-shipment quantity, packaging condition, and batch traceability review
Compliance & Technical Documentation
- RoHS compliance is specified for this Royal Blue PLA Basic SKU
- We provide compliance documentation matched to the applicable SKU and production batch
- TDS / SDS resources are available through the SSSray technical-document download center
- Applicable third-party reports can be provided when they match the requested SKU or order scope
Frequently Asked Questions
What is the MOQ for Royal Blue PLA Basic?
Neutral packaging starts from 50 spools. OEM or customized packaging programs typically start from 500–1,000 spools depending on artwork, packaging structure, and customization scope.
What print settings should I start with?
Start around 200–230°C nozzle, 45–60°C bed, and 60–150 mm/s. On suitable high-flow hardware, tune within 40–250 mm/s after checking extrusion flow, cooling, and layer bonding.
Is the Royal Blue finish glossy or matte?
It is an opaque Royal Blue with an even satin sheen: less reflective than silk PLA while still giving miniatures, gears, and architectural models a clean finished appearance.
Is it suitable for miniature and gear printing?
Yes. Use 0.12–0.16mm layers for fine miniature detail and 0.16–0.20mm with 3–4 walls for gear demonstrators or fit-check parts. For load-bearing gears, select material to match the required heat, fatigue, and wear performance.
Can SSSray provide private-label packaging?
Yes. We support custom labels, branded boxes, barcode / SKU labeling, color-line development, spool presentation, and project packaging for qualified OEM / ODM orders.
Are free samples available for B2B qualification?
Approved B2B buyers can receive up to 3 complimentary sample spools for qualification before a bulk purchasing decision.
Does PLA Basic need drying before printing?
If the vacuum seal is intact and the filament prints cleanly, additional drying is not normally necessary for initial use. If stored filament shows popping, rough extrusion, or excess stringing, dry it at 50–55°C for about 8 hours.
What is the production lead time?
Standard orders are typically 7–15 working days. Customized OEM / ODM orders are typically 15–25 working days after specifications and artwork are confirmed.
Build Your Royal Blue PLA Basic Supply Program
Request bulk pricing, qualification samples, or an OEM / private-label plan for Royal Blue PLA Basic with saturated color, fine-detail printability, and export-ready supply terms.



Related products
-

SSSray PLA+ Filament in Lagoon Teal for Decorative Vases & Desk Organizers – Sợi in 3D PLA+ Xanh Ngọc, Satin-Finish 3D Printer Filament
-
Pure White PLA+ Filament by SSSray – Filament PLA+ Biały for Detailed Architectural & Display Models, Low-Sheen 3D Printer Filament
-
SSSray Red PLA+ Filament for Sculpted Décor & Utility Hooks – Signal Red 3D Printer Filament, Filamento PLA+ Vermelho
-
Dual Color Gradient Crystal PLA Filament 1.75mm 1kg – Translucent Two-Tone Finish for FDM 3D Printing, Ideal for Artistic Decor & Jewelry Prototypes