Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

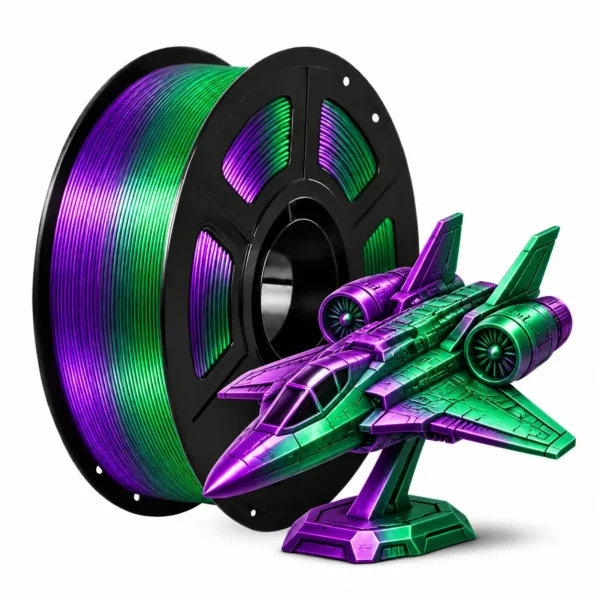
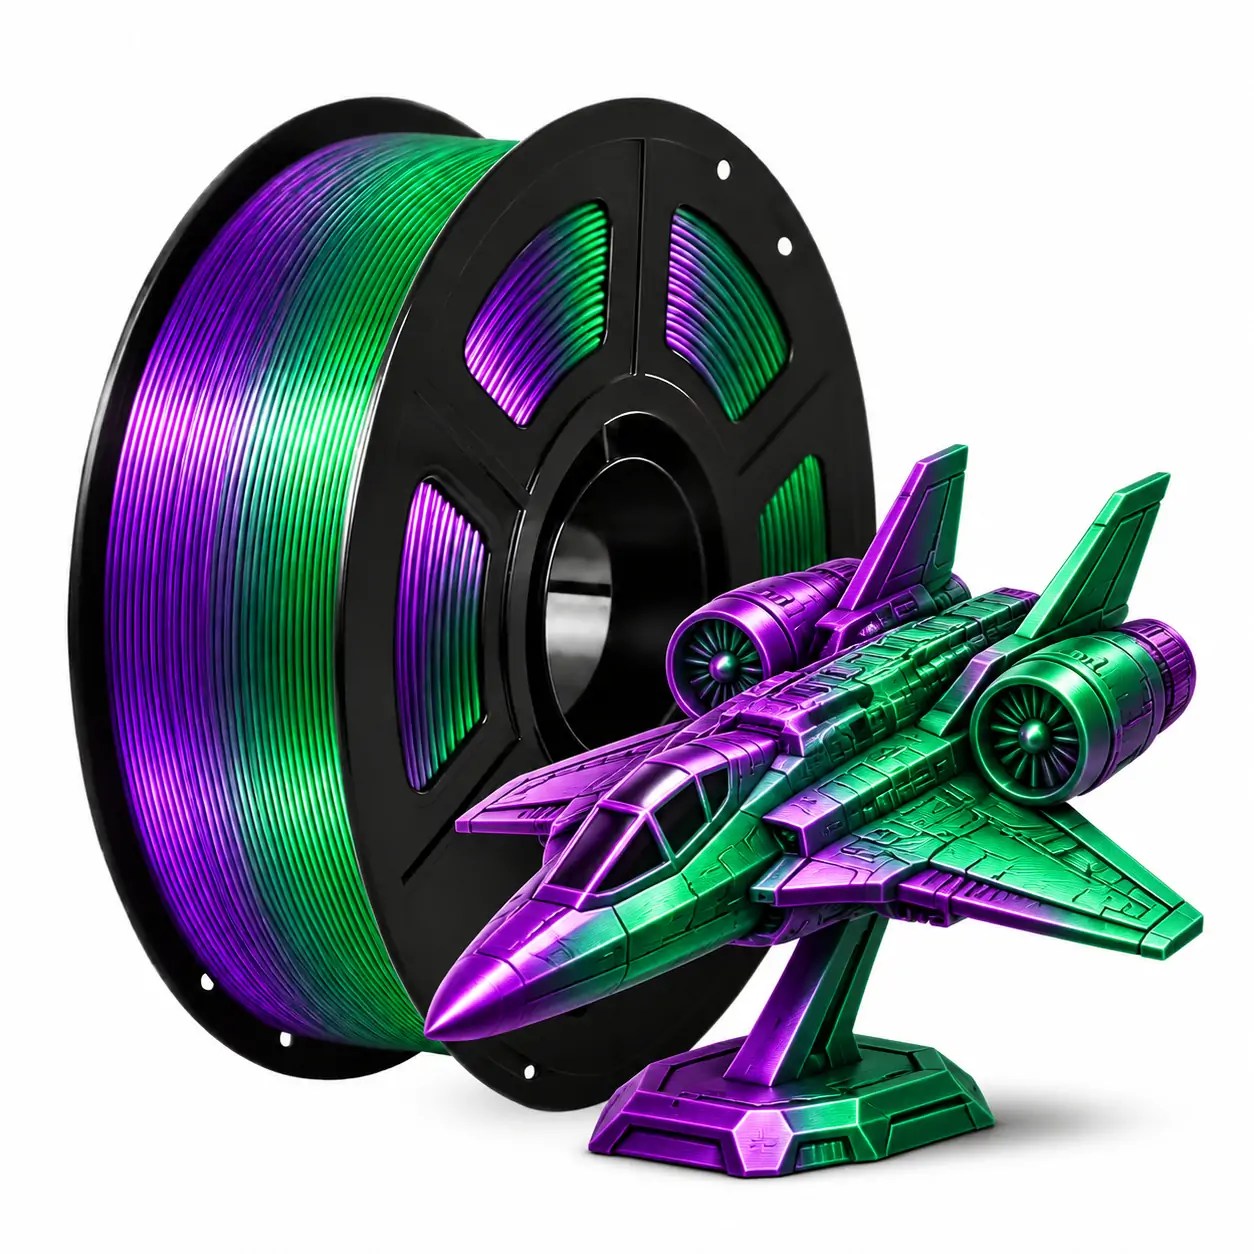
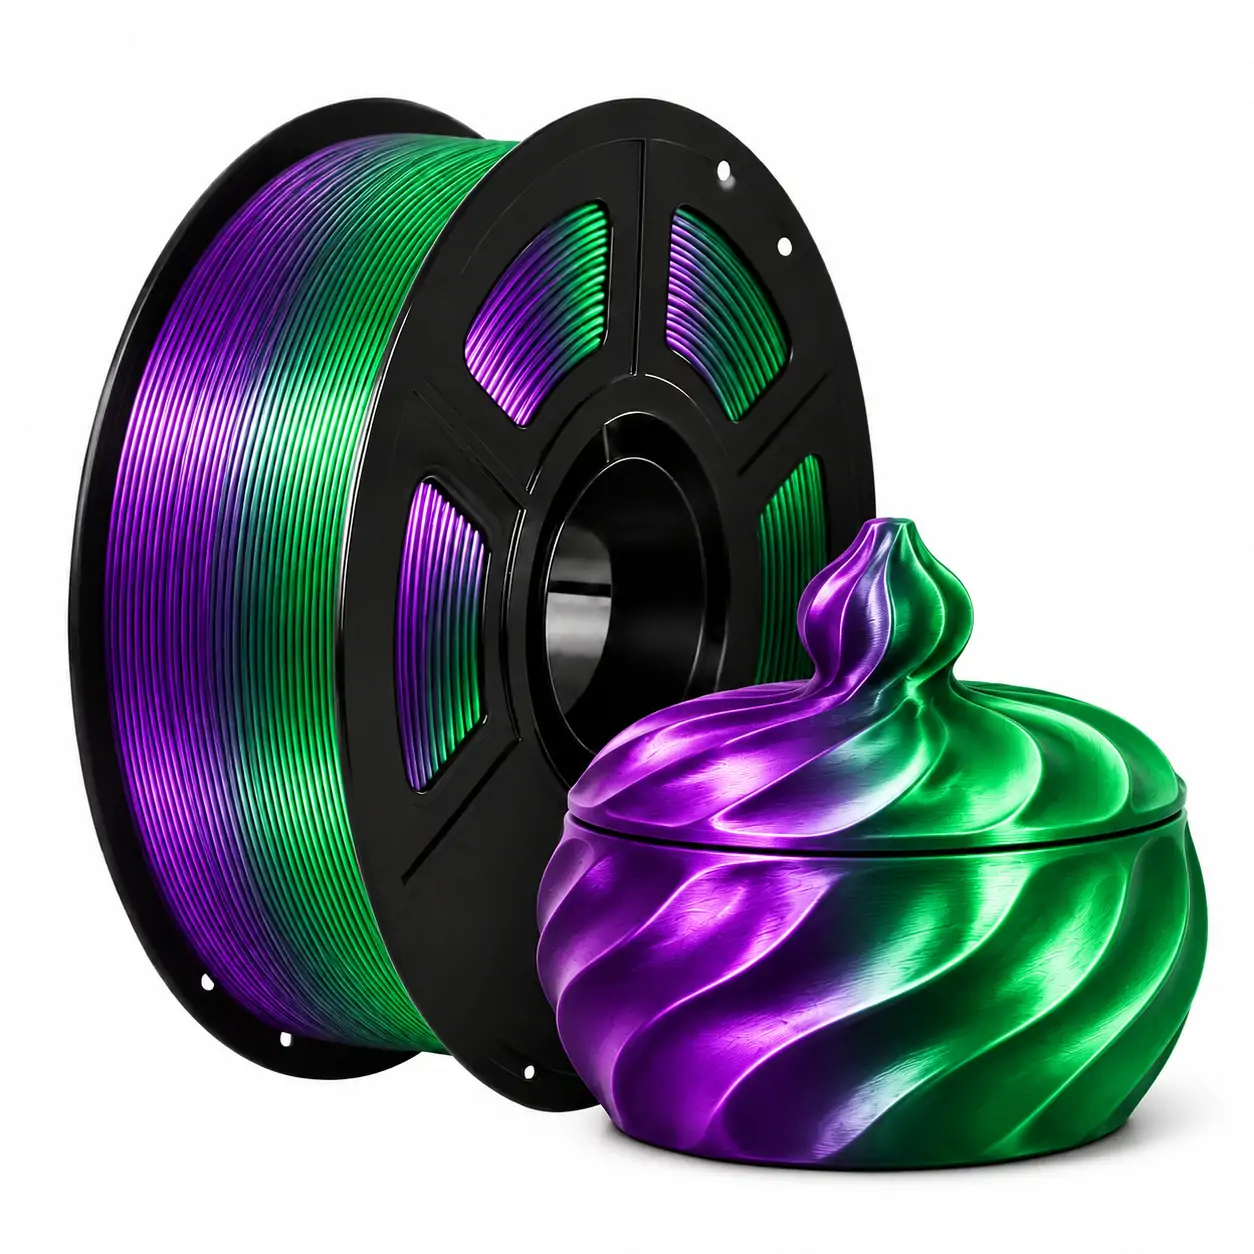
SSSRAY PLA SILK SERIES | SEQUENTIAL-SECTION DUAL-COLOR PLA | WHOLESALE & OEM / ODM
SSSray Violet & Emerald Green Dual-Color Silk PLA 3D Printer Filament – filament PLA bicolore for Sculptural Display Prints
Sequential-section Violet & Emerald Green Silk PLA for sci-fi models, sculptural displays, distributors, and private-label filament ranges.
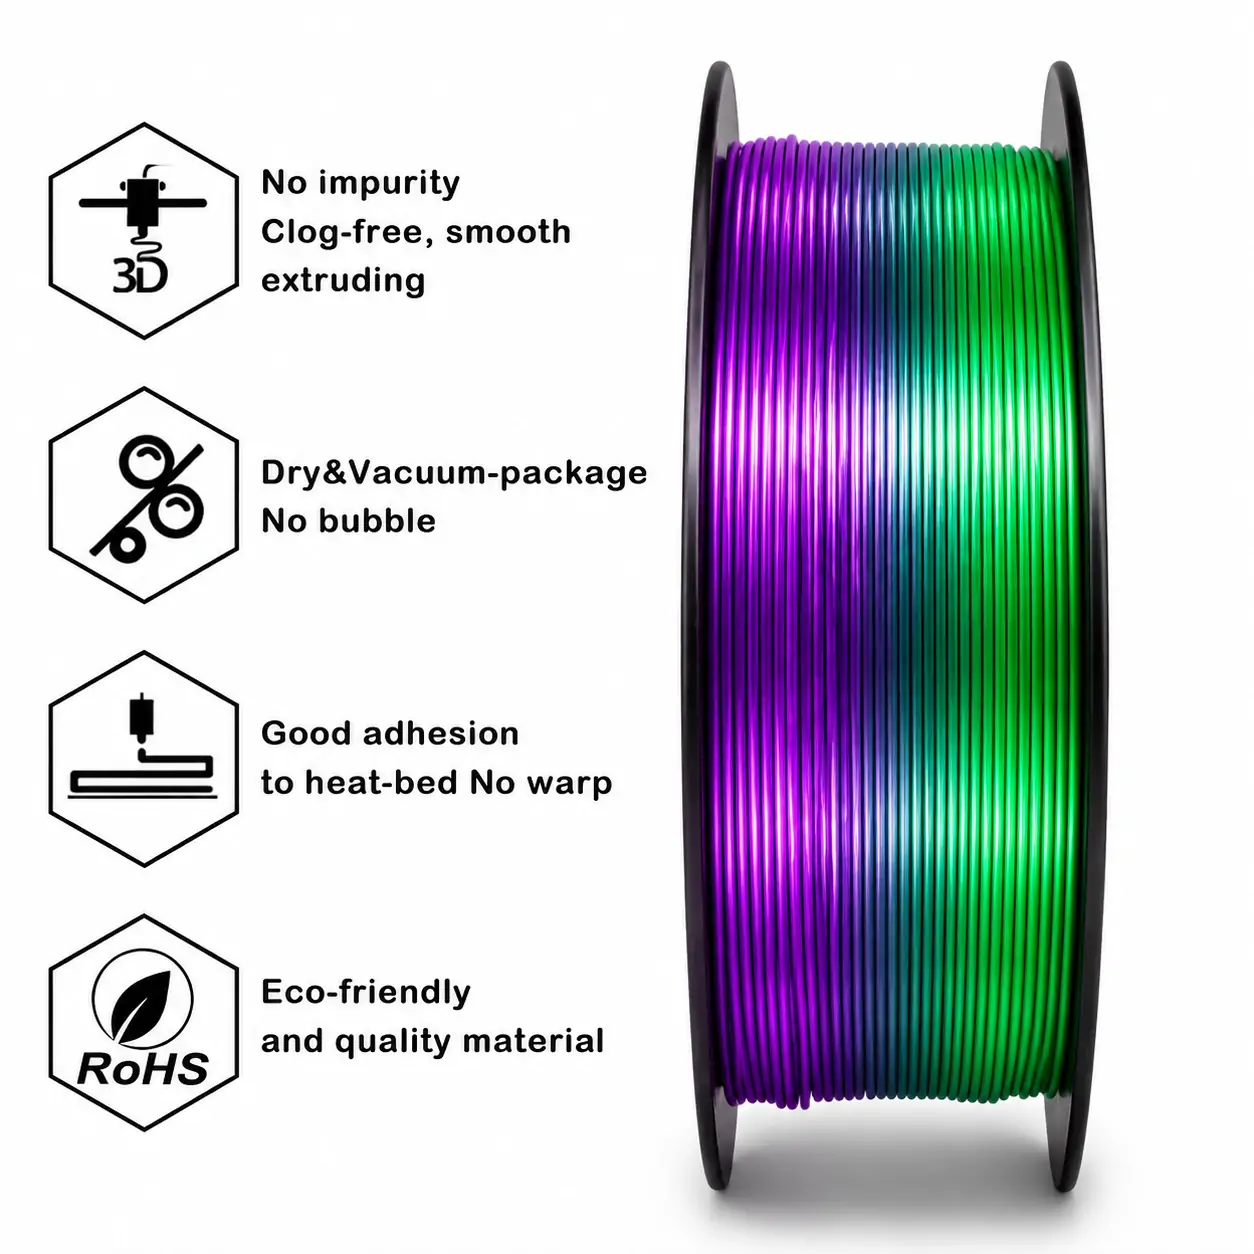
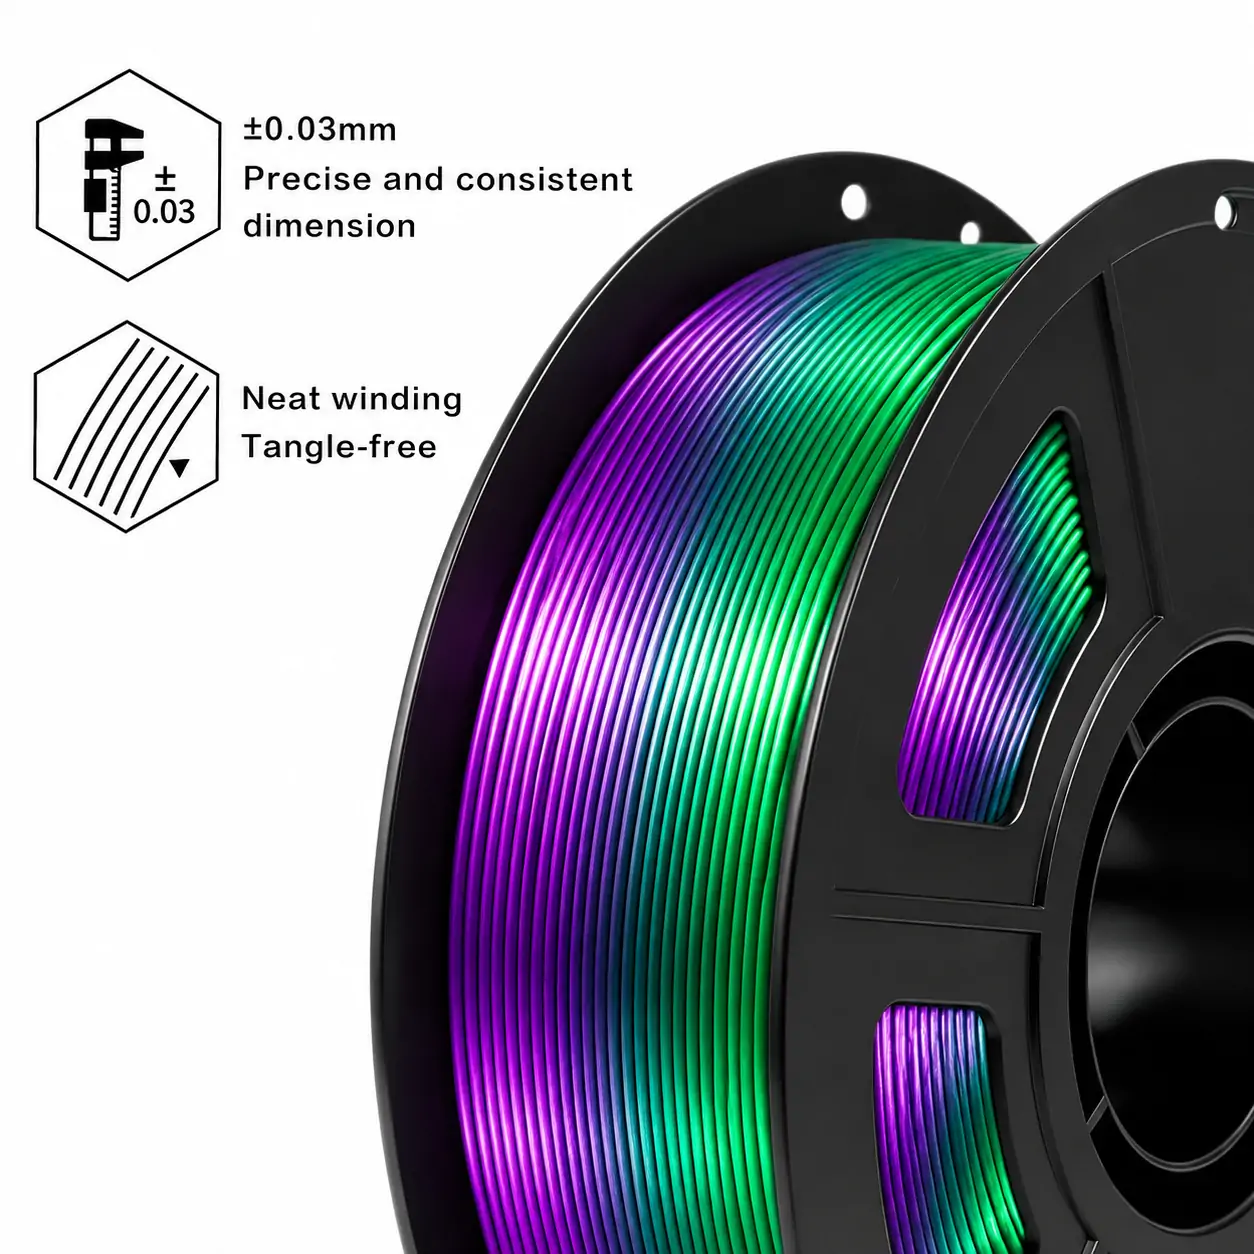
Violet-purple and emerald-green color sections run one after another along the filament length. The printer feeds each section through a standard single-nozzle FDM / FFF setup, so the finished model changes color when the next section reaches the hot end. This is a sequential color-change filament, not a side-by-side co-extruded strand or a continuous rainbow gradient. The 1kg plastic spool is supplied with a stated 1.75mm diameter, ±0.03mm tolerance, vacuum sealing, and desiccant protection.
MaterialDual-Color Silk PLA
Color StructureSequential sections along filament length
Color PairingViolet Purple + Emerald Green
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp210–230°C
Bed Temp50–60°C
Print Speed50–120mm/s recommended
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 rolls; OEM packaging typically 500–1,000 rolls.
Lead Time: Standard orders 7–15 days; customized orders 15–25 days.
Product Overview
SSSray Violet & Emerald Green Dual-Color Silk PLA is a 1.75mm FDM / FFF filament built around two sequential color sections arranged along the filament length. The strand feeds through a standard single-nozzle setup: one color section runs through the hot end before the next section reaches it, creating a visible color change as the print consumes the spool. This is not a side-by-side co-extruded filament or a continuous rainbow gradient. The transition appears where the filament boundary is extruded, so its position on the finished model depends on total filament consumption, model geometry and toolpath. We recommend this SKU for sci-fi spacecraft, armor shells, character busts, tabletop display pieces and sculptural objects with enough surface area to show the color change. Its silk-gloss surface brings reflective highlights to curved panels and raised details. Each spool carries 1kg net filament, a 1.75mm nominal diameter and ±0.03mm tolerance, with vacuum-sealed packaging and desiccant protection. SSSray supplies this display-focused PLA for wholesale orders, neutral packaging from 50 rolls and OEM packaging programs typically from 500–1,000 rolls. Qualified B2B buyers can request sample spools for printer and market evaluation.
For related finishes, browse our SSSray PLA Silk filament range. For bulk purchasing and brand development, see our wholesale PLA filament and private-label 3D printer filament programs.
Color Structure & Sample Approval
Violet-purple and emerald-green sections are joined end-to-end along the filament length. The transition appears when the next section reaches the hot end, so its position on a printed part depends on filament consumption and the model’s toolpath. Before a wholesale or private-label order, we recommend printing a sample spool on the intended printer and reviewing the transition on the target model.
Key Selling Points
Sequential Color Construction
Violet-purple and emerald-green sections follow one another along a single filament strand and pass through a standard single-nozzle setup.
Silk Gloss for Display Prints
The reflective surface brings out curved shells, armor contours and raised details on decorative and sculptural models.
Wholesale & Private-Label Supply
Neutral packaging starts at 50 rolls; OEM packaging typically starts at 500–1,000 rolls for approved label and retail-pack projects.
Sample & Order Approval Checks
| Check Point | How We Check It |
|---|---|
| Color Transition | We print a sample using the intended model size and orientation, then review where the violet-to-emerald boundary appears on the finished part. |
| Filament Diameter | We check the 1.75mm nominal diameter against the stated ±0.03mm tolerance using the inspection method agreed for the order. |
| Silk Surface Finish | We review gloss consistency on curved and flat surfaces against the approved sample profile. |
| Spool and Packaging | We confirm 1kg net filament per spool and the vacuum-sealed bag with desiccant before dispatch. |
| Bulk-Order Release | We align the approved sample appearance, label artwork and packing specification before production release. |
Wholesale Fit for Your PLA Range
We support distributors adding a distinctive sequential-color Silk PLA option to their existing ranges. Private-label buyers can align spool labels, retail-box artwork and carton marks with the approved sample. Neutral packaging starts at 50 rolls; OEM packaging typically starts at 500–1,000 rolls, depending on the approved customization scope.
How We Work
1
Market, Model & Order Brief2
Color Sequence & SKU Confirmation3
Sample Print & Transition Review4
Label & Retail-Pack Approval5
Production & Six-Point QC6
Export Packing & ShipmentPLA Material Comparison
| PLA Type | Surface / Color Effect | Typical Buyer Use |
|---|---|---|
| Violet & Emerald Sequential Silk PLA | High-gloss Silk finish with violet-purple and emerald-green sections arranged one after another along the filament length. | Distinctive display prints, sci-fi models, figures and decorative retail products. |
| Standard PLA | Usually supplied as a single-color material; surface finish varies from matte to semi-gloss by grade and pigment. | General prototypes, concept models, classroom projects and decorative prints. |
| PLA+ / PLA Pro | Modified PLA formulations; stiffness, impact response and print behaviour vary by supplier. | General-purpose parts where the selected formulation’s mechanical profile is preferred. |
Select the PLA grade according to the required surface appearance and part performance; use the print profile specified for the exact material.
Technical Specifications
| Product Name | SSSray Violet & Emerald Green Dual-Color Silk PLA 3D Printer Filament – filament PLA bicolore for Sculptural Display Prints |
|---|---|
| Material | Dual-Color Silk PLA (Polylactic Acid), FDM / FFF 3D printing material |
| Product Series | SSSray PLA Silk Series – Dual-Color Creative & Display Collection |
| Color / Effect | Violet Purple & Emerald Green – high-gloss Silk finish with sequential color sections |
| Filament Construction | Sequential color sections arranged along the filament length; not side-by-side co-extrusion |
| Color Transition | One color section follows the next as filament feeds through a single nozzle; transition position depends on filament consumption and toolpath |
| Filament Diameter | 1.75mm standard for this SKU |
| Diameter Tolerance | ±0.03mm |
| Net Filament Weight | 1kg per spool |
| Gross Weight | 1.3kg per packaged spool |
| Spool Type | Plastic spool |
| Packaging | Vacuum-sealed bag with desiccant |
| Printing Technology | FDM / FFF |
| Recommended Nozzle Temperature | 210–230°C; start at 215°C and tune for the printer and desired silk finish |
| Recommended Bed Temperature | 50–60°C |
| Recommended Print Speed | 50–120mm/s recommended; 40–200mm/s usable after flow and temperature calibration |
| Recommended Layer Height | 0.16–0.20mm for a 0.4mm nozzle |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers, subject to the printer’s material and temperature limits |
| Typical Applications | Sculptural display prints, figurines, sci-fi models, decorative vessels, props, and creative retail products |
| OEM / ODM | Available for qualified B2B projects |
| Technical / Compliance Documents | Request the applicable TDS and SDS/MSDS for the confirmed SKU; compliance documents are supplied where they apply to the product and destination market |
Recommended Print Settings
| Parameter | Recommended Starting Value | Practical Adjustment Range |
|---|---|---|
| Nozzle Temperature | 210–230°C; begin at 215°C | 200–240°C after temperature-tower and extrusion checks. |
| Bed Temperature | 50–60°C | 45–60°C; match the surface and first-layer requirements. |
| Print Speed | 50–120mm/s overall | 40–200mm/s after flow and temperature calibration; use lower speeds for visible outer walls. |
| Outer-Wall Speed | 30–50mm/s | 30–60mm/s; keep the speed steady across visible panels and curved surfaces. |
| Layer Height | 0.16–0.20mm with a 0.4mm nozzle | 0.12–0.28mm according to detail and nozzle diameter. |
| Part Cooling Fan | 80–100% after the first 2–3 layers | 50–100%; tune for overhangs, layer bonding, and small features. |
| Retraction – Direct Drive | 0.8–1.2mm at 25–40mm/s | 0.5–1.5mm; tune to the extruder and hotend. |
| Retraction – Bowden | 3–5mm at 25–40mm/s | 2–6mm; tune to the Bowden path and hotend. |
| Wall Count | 3 perimeters | 2–4 perimeters according to shell strength and appearance. |
| Infill | 15–20% for decorative models | 40–60% for thicker display parts where additional internal support is needed. |
| First-Layer Speed | 20–30mm/s | 15–35mm/s; prioritize a stable, continuous first layer. |
| Bed Adhesion | Clean PEI, satin PEI, or suitable glass surface | Use a compatible adhesive/release aid only when required by the build plate. |
| Pre-Print Drying | 50–55°C for 6–8 hours when moisture symptoms appear | Use a temperature-controlled filament dryer and verify spool heat limits. |
For a clean production setup, run a temperature tower, flow check, and small appearance sample on the target printer before saving the material profile.
Print Optimization Guide
| Optimization Focus | Practical Guidance |
|---|---|
| Sequential Color Transition | The color sections run one after another along the filament length. The transition prints when the next section reaches the hot end; its position on the model follows cumulative filament use and the toolpath. Test the intended model size before preparing retail samples. |
| Show the Violet / Emerald Contrast | Choose a model with broad visible surfaces—such as a spacecraft fuselage, armor shell or display bust—so the color change is easy to see. Small prints may finish before the transition reaches a prominent area. |
| Silk Gloss | Keep outer-wall speed steady at 30–50mm/s for visible surfaces. Avoid abrupt speed changes that can create uneven sheen across curved panels. |
| Temperature Tuning | Begin at 215°C and adjust in 5°C steps within the recommended range. Keep the temperature high enough for consistent extrusion without sacrificing surface definition. |
| Cooling Balance | Use moderate-to-high part cooling after the first layers for overhangs and fine details. Reduce fan output if small features or layer bonding require adjustment. |
| Stringing Control | Keep the filament dry, clean the nozzle and tune retraction for the actual extruder. Direct-drive and Bowden retraction values are not interchangeable. |
| Bed Adhesion | Clean the PEI or other compatible build surface, slow the first layer and verify Z-offset before increasing bed temperature. |
| Large Display Models | Use a brim for narrow contact areas or tall, slim models. Keep the printer away from drafts to reduce first-layer and cooling variation. |
Printer Brand Starting Settings
| Printer Ecosystem | Nozzle Start | Bed Start | Outer-Wall Start | Profile / Setup Notes |
|---|---|---|---|---|
| Bambu Lab A1 / P1 / X1 | 215–225°C | 55–65°C on Smooth PEI; 65–85°C on Textured PEI (Bambu PLA reference) | 35–50mm/s | Bambu Lab’s current PLA guide lists 55–65°C for Smooth PEI and 65–85°C for Textured PEI. Start with a Generic PLA or Silk PLA profile, then verify first-layer adhesion with this Silk PLA and the selected plate. |
| Prusa MK4 / MK4S / MINI+ | 215°C first layer; 210–220°C after | 60°C | 30–45mm/s | Begin with the PLA profile, then tune for Silk gloss. Smooth or satin PEI provides a practical starting surface. |
| Creality K1 Series / K2 Plus | 220–230°C | 45–50°C | 40–60mm/s | Use the Generic Silk PLA profile where available. On K1-family Silk profiles, retain the material’s temperature and flow limits while slowing visible walls for finish. |
| Flashforge Adventurer 5M / 5M Pro | 210–230°C | 45–60°C | 40–60mm/s | Select Silk PLA or Generic PLA as the base profile; do not transfer a high-speed preset without checking flow and outer-wall quality. |
Select the closest PLA / Silk PLA profile, then confirm first-layer adhesion, extrusion flow and outer-wall finish on the exact printer model before running the full display piece.
Performance Characteristics
| Characteristic | Product Behaviour | Practical Reference |
|---|---|---|
| Silk Surface Appearance | High-gloss finish creates reflective highlights on curved panels and raised details. | Keep outer-wall speed steady at 30–50mm/s and tune temperature and cooling on the target printer. |
| Print Setup | PLA-based FDM / FFF filament for standard 1.75mm feed paths. | Start within the stated 210–230°C nozzle and 50–60°C bed ranges; qualify the profile with a sample print. |
| Application Position | Designed for decorative, sculptural and general-purpose PLA display prints. | Choose another material family for sustained high-temperature, outdoor or heavy-load engineering service. |
Applications
| Application Focus | Practical Notes |
|---|---|
| Sci-Fi Starfighters & Spacecraft Shells | Broad fuselage and wing surfaces give the violet / emerald sequence room to appear across a recognizable display model. |
| Mecha Armor & Fantasy Creatures | Layered armor plates, curved shells and larger body sections provide visible areas for the sequential color transition. |
| Character Busts & Collectible Figures | Use a representative bust or larger figure when you want the color boundary to show across a prominent surface rather than a small detail. |
| Tabletop Terrain & Diorama Features | Futuristic structures, display bases and terrain pieces can use the two-color sequence to separate large visual zones within one filament feed. |
| Sculptural Vessels & Desk Objects | Curved walls and taller forms can reveal the color change as the print consumes more filament; test the intended height and wall geometry. |
| Retail Display & Gift Collections | A violet-and-emerald sequential Silk PLA SKU adds a clear color-story option to themed model, collectible and decorative product ranges. |
Storage Guide
- Keep unused filament in its vacuum-sealed bag with the supplied desiccant; reseal promptly after opening.
- Store in a cool, dry location away from direct sunlight, heat sources, and rapid temperature changes.
- For opened spools, use a sealed storage box with fresh desiccant; an internal humidity target of 20% RH or lower is a practical storage reference.
- If stringing, popping, or inconsistent extrusion indicates moisture exposure, dry at a controlled 50–55°C for 6–8 hours, subject to the spool’s heat limit.
- Keep the filament path clean and avoid letting the free end unwind or cross over adjacent turns during storage.
OEM / ODM Services
SSSray supports distributors, wholesalers, importers and private-label brands that want a Silk PLA SKU with a clear visual identity. For this Violet & Emerald Green product, we can coordinate the product name, color-sequence description, spool label, retail-box artwork, barcode, outer-carton marks and export packing details as one order specification. Buyers can also discuss custom color combinations, spool presentation and packaging formats for a wider branded range.
As a factory-direct 3D printer filament manufacturer in Jinhua, China, SSSray aligns the material specification, sample appearance and packaging artwork with your purchasing team before bulk production. Neutral packaging starts from 50 rolls; OEM packaging typically starts from 500–1,000 rolls, depending on the approved customization scope. We recommend approving a physical sample and final artwork before production release.
Quality Control
- We identify incoming raw materials and color batches before production release.
- We monitor filament diameter during extrusion against the 1.75mm ±0.03mm specification.
- We inspect the filament surface and violet / emerald color sequence for visible contamination, streaking and finish consistency.
- We check spool winding alignment, tension, cross-over risk and filament-end retention before packing.
- We carry out sample extrusion and print verification against the approved reference profile and appearance sample.
- We check vacuum sealing, desiccant, product labels and export-carton marks before shipment.
Certifications & Technical Documentation
- Technical Data Sheet (TDS): Request the applicable technical specification for the confirmed Violet & Emerald Green Silk PLA SKU.
- Safety Data Sheet (SDS / MSDS): Our team confirms the applicable safety document for the selected material and shipment file.
- RoHS / REACH: Compliance documents are supplied when they cover the confirmed formulation and product scope.
- CE: We do not present CE as a filament certification for this SKU.
- SGS / Third-Party Testing: Any report shared for buyer review identifies its tested product scope and issuing laboratory.
For wholesale and OEM orders, tell our sales team which technical or compliance files your purchasing process requires. We will confirm the documents applicable to the selected product and destination market.
Frequently Asked Questions
How is the violet and emerald color effect arranged in this filament?
The two colors are arranged in sequential sections along the filament length. One section feeds through the nozzle before the next section arrives, so the printed color changes as the spool is consumed. The colors are not side-by-side in the same cross-section and do not require a second filament feed.
Where will the color transition appear on my printed model?
The transition appears when the filament boundary reaches the hot end. Its position on the model depends on the amount of filament consumed, the model geometry and the slicer’s toolpath. For a retail demonstration, test the intended model size and print orientation with a sample spool first.
What is the MOQ for this dual-color Silk PLA?
Neutral packaging starts from 50 rolls. OEM packaging typically starts from 500–1,000 rolls, depending on the custom label, retail box and packaging scope.
Can I request samples before placing a wholesale order?
Qualified B2B buyers can apply for up to 3 free full-size 1kg sample spools after project review. We confirm the sample combination and dispatch arrangements before shipment.
Which printers can use this 1.75mm filament?
It is designed for most open-material 1.75mm FDM / FFF printers, including common Bambu Lab, Prusa, Creality and Flashforge systems. Confirm the printer’s filament path, material profile, extruder setup and temperature limits before printing.
What nozzle and bed temperatures should I start with?
Start at 215°C nozzle temperature and 50–60°C bed temperature. The recommended nozzle range is 210–230°C. Tune in small increments for the printer, build plate, model geometry and desired Silk gloss.
Can SSSray customize the label, packaging or color combination?
Yes. OEM / ODM options include private-label spool labels, retail-box artwork, barcodes, outer-carton marks and project-based color development. Custom projects are reviewed against the required specification, MOQ and production schedule.
What are the lead time and shipping terms?
Standard orders are scheduled for 7–15 days; customized orders for 15–25 days. We support FOB Ningbo, China and EXW SSSray Factory, Jinhua, Zhejiang, China, under Incoterms® 2020. Ningbo, China is the stated port of loading for FOB shipments.
Add Violet & Emerald Sequential Silk PLA to Your Display Filament Range
Bring a sequential violet-and-emerald color story into your PLA range with a single-nozzle Silk PLA spool. Contact SSSray for bulk pricing, sample qualification, private-label packaging and an export quotation matched to your order quantity and destination market.



Related products
-

SSSray PLA Signage Grade 3D Printing Filament – Translucent & Solid 1kg (Custom OEM & Wholesale)
-
Dual Color Gradient Crystal PLA Filament 1.75mm 1kg – Translucent Two-Tone Finish for FDM 3D Printing, Ideal for Artistic Decor & Jewelry Prototypes
-
Aurora Rainbow PLA Filament 1.75mm 1kg – Rich Magenta-Purple Gradient for FDM 3D Printing, Optimized for Character & Organic Modeling (Wholesale OEM/ODM)
-
SSSray Red PLA+ Filament for Sculpted Décor & Utility Hooks – Signal Red 3D Printer Filament, Filamento PLA+ Vermelho