Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

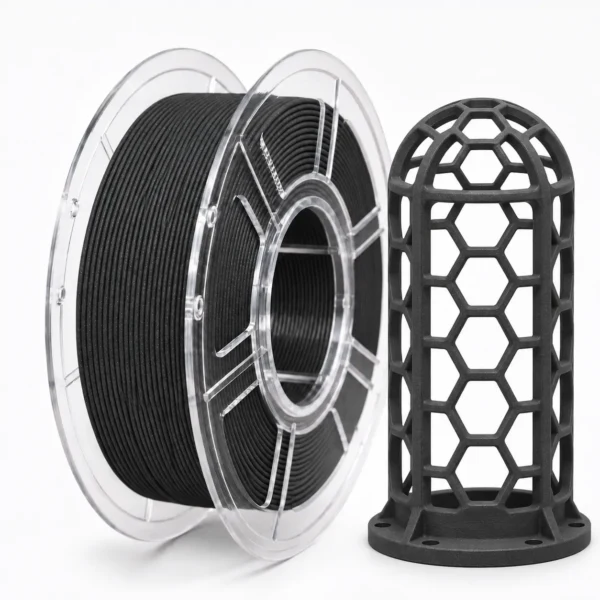
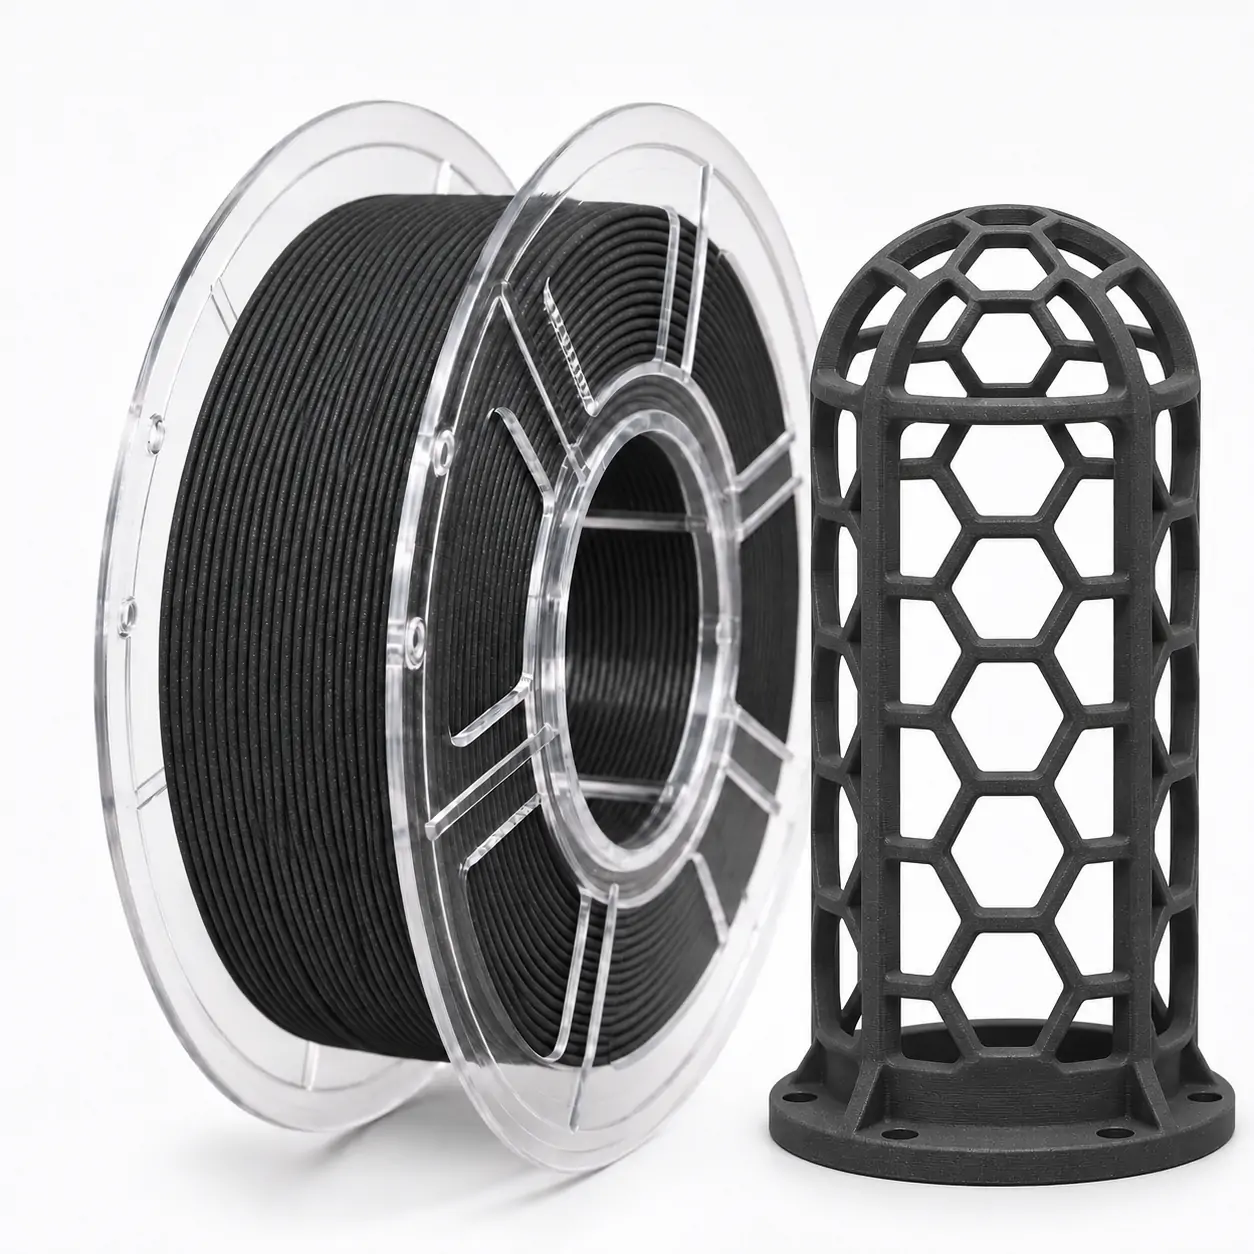
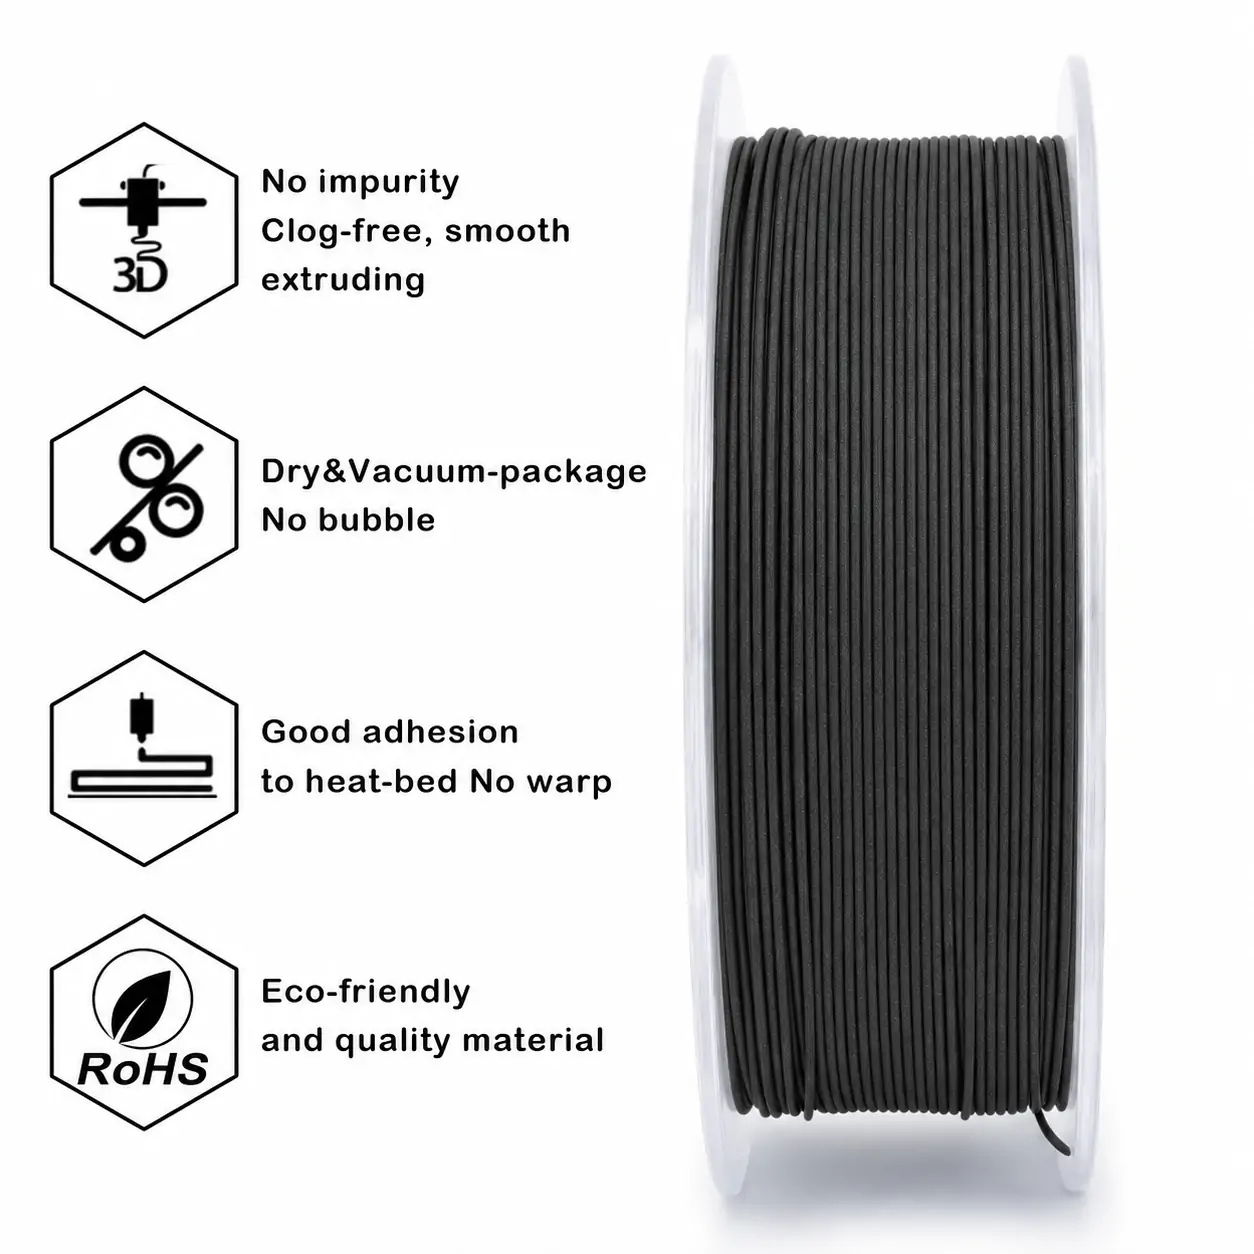
PA12-CF Functional Parts Series | 15% Carbon Fiber | Wholesale & OEM
SSSray Industrial Black PA12-CF 1.75mm 3D Printer Filament – 15% Carbon Fiber Nylon (เส้นไนลอนผสมคาร์บอนไฟเบอร์) for Lattice Guards & Support Frames
Our custom 15% carbon fiber PA12 nylon delivers a refined industrial-black finish for lattice guards, rigid fixtures and support-frame production.
We manufacture Industrial Black PA12-CF15 for engineering buyers who need a stiff, lightweight nylon composite with a uniform charcoal-black, soft-matte appearance. From open-cell honeycomb guards to four-column mounting frames, we help you match print geometry, material handling and dependable factory-direct supply. Choose our standard 1kg export spool or build your own private-label program.
MaterialPA12 + 15% CF
SeriesPA12-CF Functional Parts
Color EffectIndustrial Black / Soft Matte
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp260–280°C
Bed Temp90–100°C
Print Speed40–80 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 days; customized orders typically 15–25 days.
Product Overview
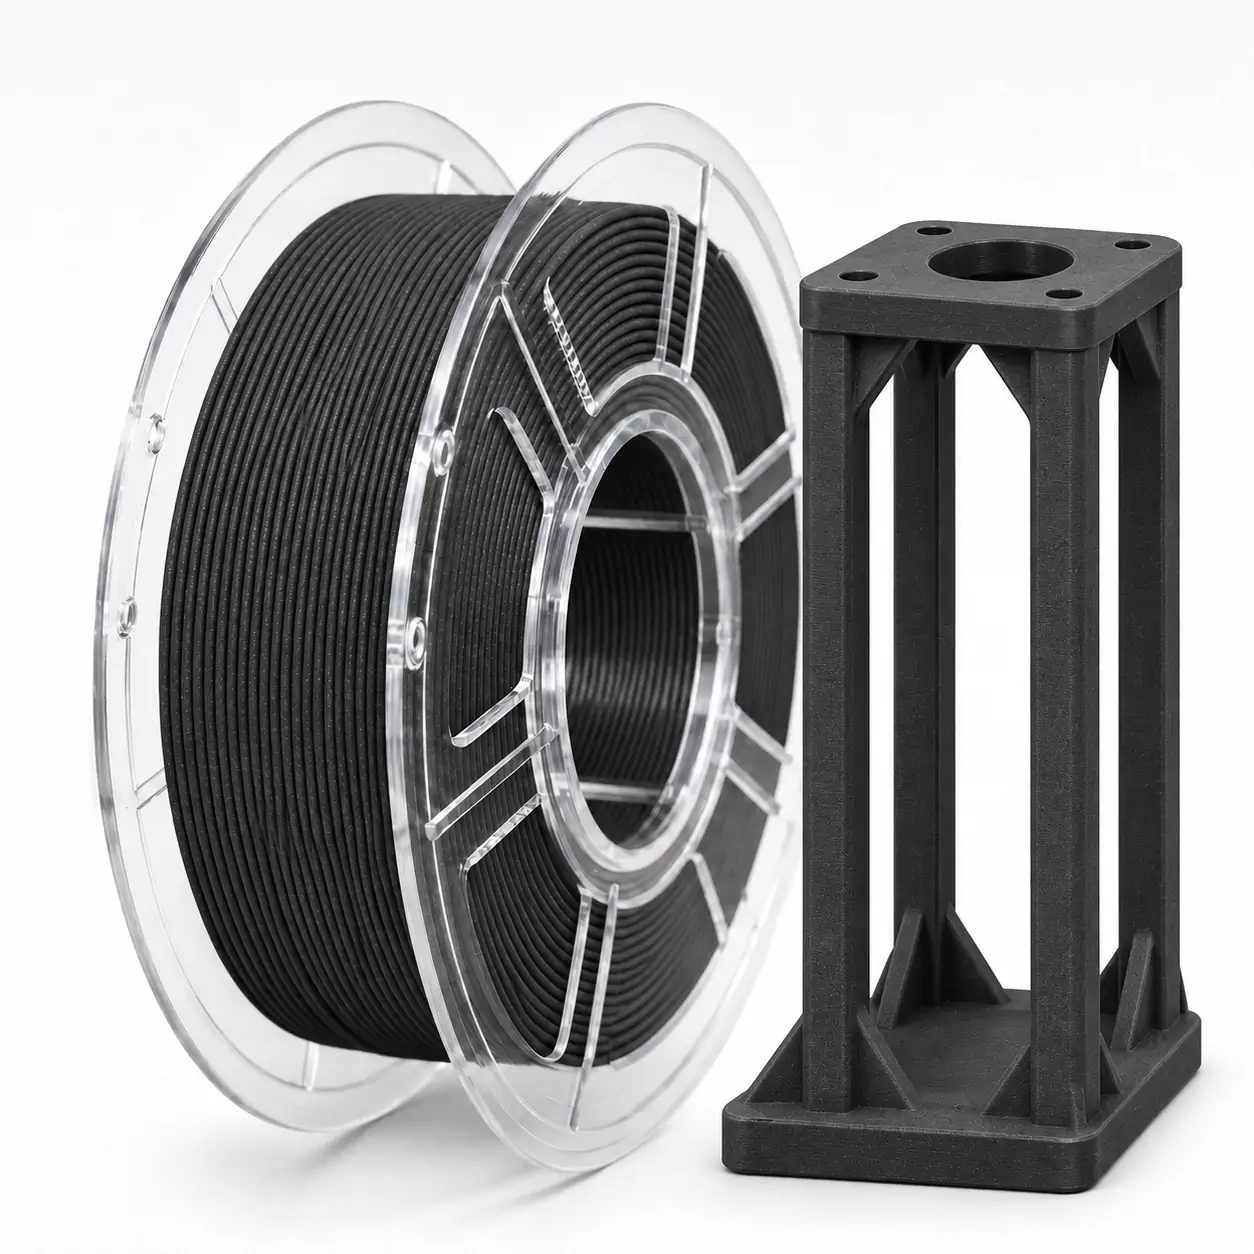
Our Industrial Black PA12-CF15 combines Nylon 12 with 15% carbon fiber for rigid functional components that need a clean, professional finish. Its deep charcoal-black, opaque surface develops a distinctive fine-textured matte appearance on printed honeycomb ribs, guard panels and four-column support frames. The reinforced PA12 formulation is a practical choice for equipment brackets, workholding fixtures and lightweight assemblies where part orientation, continuous perimeter paths and dimensional consistency matter. We make this custom grade for customers who want engineering function and a consistent industrial-black presentation in one filament.
We supply 1.75mm filament with ±0.03mm diameter tolerance, vacuum sealing and desiccant protection on a 1kg plastic spool. For clean extrusion and reliable matte surfaces, dry before printing, feed from a dry box and use a 0.6mm wear-resistant nozzle with a heated bed. Send us your lattice rib dimensions, frame load direction, printer models and expected order quantity. Our team will recommend a practical sample setup and quote neutral-packed or private-label supply directly from our export program.
Industrial Black PA12-CF15 for Lattice Guards & Frames
Purpose-built for matte-black guards and structural frame prototypes. Our 15% carbon fiber PA12 combines the design freedom of open-cell lattice printing with the understated look of charcoal-black industrial hardware. The fine surface texture helps printed ribs and mounting bosses look cohesive beside metal machine assemblies. With a 0.6mm hardened nozzle, dry-filament feed and our 260–280°C recommended nozzle range, you can build repeatable profiles for complex guards and fixture bodies. We back the product with 1kg vacuum-packed export units, direct technical discussions and wholesale/private-label options.
Key Selling Points
Precision 1.75mm Feed
We manufacture to a 1.75 ±0.03mm diameter specification and check production-batch diameter records to support predictable feeding, sample approvals and repeat orders.
Efficient PA12-CF Processing
We recommend 260–280°C nozzle heat and 40–80 mm/s for controlled part quality, with a wider tuning window for capable production printers.
Soft-Matte Industrial Black
A deep charcoal-black, opaque surface with fine texture suits visible protective guards and low-glare fixture components.
15% Carbon Fiber Structure
Our custom 15% carbon fiber grade is made for firm lattice ribs, mounting points and support-frame prototypes with well-planned load paths.
Dry, Protected Export Packing
We vacuum-seal every standard spool with desiccant to protect dry storage and export transit before your next production job.
OEM / ODM Program Support
We support your engineering-filament range with custom labels, branded cartons, production-batch identification and access to our grade-specific PA12-CF15 TDS, COA and RoHS test documentation.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| 15% CF Reinforced PA12 | Use for rigid grid panels, structural frame prototypes and tooling where uninterrupted wall paths are important |
| Opaque Charcoal-Black / Fine Matte | Delivers a low-sheen finish on exposed guard ribs, mounting columns and housings without a metallic appearance |
| 0.6mm Wear-Resistant Nozzle | Provides a practical extrusion route for filled nylon and honeycomb rib widths designed around the selected line width |
| 40–80 mm/s Recommended Profile | Balances wall detail and production throughput for guarded lattice and fixture geometries |
| 1kg / 1.75mm / ±0.03mm | Keeps the reorder specification consistent across sample lots, print farms and wholesale replenishment |
| Vacuum Packing / OEM Label Options | Supports dry material handling, import-ready SKU presentation and private-label distribution |
Factory-Direct Value for Guard & Frame Production
We manufacture Industrial Black PA12-CF15 with a defined 15% carbon-fiber formulation, a fine-matte charcoal-black finish and a consistent 1kg export format. Our production team checks 1.75 ±0.03mm diameter, spool winding, vacuum seals and batch identification before shipment; our PA12-CF15 TDS, COA and RoHS documentation supports purchasing and quality approval. You can carry one agreed material and packaging specification from honeycomb-guard sampling through fixture production and replenishment. We offer neutral packaging from 50 spools, OEM presentation for volume programs and direct EXW or FOB Ningbo quotations.
How We Work
1
Requirement Review
2
Specification Confirmation
3
Sample Evaluation
4
Packaging Discussion
5
Production Arrangement
6
Inspection & Shipment
PA12-CF15 Material Comparison Guide
| Material | Reinforcement / Material Behavior | Typical Applications | Printing Conditions | Procurement / Engineering Fit |
|---|---|---|---|---|
| SSSray Industrial Black PA12-CF15 | Our custom 15% CF / PA12 with opaque deep-charcoal matte finish and reinforced rigidity | Open-cell lattice guards, four-column supports, fixture mounts | 260–280°C nozzle; 90–100°C bed; dry feed; 0.6mm hardened nozzle | We support sample-to-bulk consistency with 1.75 ±0.03mm production checkpoints, batch ID and grade-specific TDS / COA |
| Unfilled PA12 | Unreinforced nylon; more ductile behavior than many fiber-filled variants | Snap-fit trials, flexible engineering elements, wear components | Nylon drying and adhesion control; formulation-dependent heat settings | Compare flexibility and wear before choosing a reinforced grade |
| PA6-CF | Carbon-filled PA6; moisture response and heat performance depend on grade | Structural tooling and high-stiffness functional prototypes | High-temperature nozzle; drying; adhesion and enclosure tuning | Review conditioning and batch data for the intended environment |
| PETG-CF | Carbon-filled PETG; generally a lower-temperature processing option | Jigs, housings and functional aesthetic parts | Typically lower nozzle/bed settings than carbon-filled nylon | Assess temperature and long-term load needs before substitution |
Planning an engineering-filament assortment? Explore our wholesale carbon fiber filament range for complementary grades and bulk supply options.
Technical Specifications
| Product Name | SSSray Industrial Black PA12-CF 1.75mm 3D Printer Filament – 15% Carbon Fiber Nylon (เส้นไนลอนผสมคาร์บอนไฟเบอร์) for Lattice Guards & Support Frames |
|---|---|
| Material | PA12-CF (Polyamide 12 / Nylon 12 reinforced with 15% carbon fiber) for FDM/FFF 3D printing |
| Series | SSSray PA12-CF Functional Parts Series – 15% Carbon Fiber Nylon for Protective Guards & Structural Frames |
| Color / Effect | Deep charcoal-black, opaque, non-metallic; fine-textured soft-matte finish |
| Filament Diameter | 1.75mm standard; 2.85mm on project request, subject to specification confirmation |
| Tolerance | ±0.03mm |
| Net Weight | 1kg (2.2 lbs) |
| Gross Weight | 1.3kg |
| Spool Type | Plastic spool |
| Packaging | Vacuum sealed with desiccant |
| Extruder / Hotend | 1.75mm FDM/FFF system with an all-metal hotend capable of at least 280°C |
| Nozzle | Hardened steel / tungsten carbide / wear-resistant equivalent; 0.6mm recommended |
| Printer Compatibility | Selected properly equipped Bambu Lab, Prusa, Creality and industrial open-material FDM systems; verify hotend and bed limits |
| Typical Applications | Lattice protective guards, four-column supports, rigid jigs, brackets and trial assemblies |
| Moisture Handling | Pre-dry at approximately 80°C for 4–6h; dry-box feeding recommended |
| PA12-CF15 Tensile Strength | 120–125 MPa at break (ISO 527) |
| PA12-CF15 Tensile Modulus | 7,300–8,000 MPa (7.3–8.0 GPa; ISO 527) |
| PA12-CF15 Heat Deflection | 150°C at 1.8 MPa and 170°C at 0.45 MPa (ISO 75) |
| PA12-CF15 Density | 1.07 g/cm³ |
| SSSray Grade & Batch Documentation | Industrial Black PA12-CF15-specific TDS, batch COA and RoHS test report available through our sales team; we match the requested grade and order batch before supplying technical files |
| OEM / ODM | Supported |
| Production Quality Checks | Diameter checkpoints to 1.75 ±0.03mm, winding inspection, vacuum-seal and desiccant checks, batch label and carton reconciliation |
For SSSray Industrial Black PA12-CF15 orders, we supply our own grade-specific TDS and the relevant batch COA for product-level confirmation.
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | Our 260–280°C quality-profile starting range for nylon layer fusion and uniform fine-matte walls |
| Process-Tuning Nozzle Window | 250–290°C for suitable high-temperature, wear-resistant extrusion systems |
| Recommended Bed Temperature | 90–100°C |
| Bed Temperature Adjustment Window | 80–110°C where printer and build surface permit; never exceed the machine limit |
| Recommended Print Speed | Our 40–80 mm/s quality-first starting range for defined honeycomb ribs and stable fixture walls |
| Process-Tuning Speed Window | 30–120 mm/s; use the upper end with a high-flow hotend, stable extrusion and larger frame sections |
| Layer Height (0.6mm Nozzle) | 0.20–0.30mm; start at 0.24mm |
| Cooling Fan | 0–10% for normal walls; start at 0%; tune bridges separately |
| Retraction – Direct Drive | 0.5–1.2mm at 20–35 mm/s; start with the printer’s calibrated profile |
| Retraction – Bowden | 2–4mm at 20–35 mm/s; avoid excessive hot retraction |
| Wall Count | 3–5 perimeters; set by wall thickness and load path |
| Infill | 20–35% for guards / 40–60% for higher-demand prototypes; validate load cases |
| First Layer Speed | 15–25 mm/s |
| Bed Adhesion | Smooth or textured PEI, or glass, with PA-specific adhesive/separation layer |
| Filament Drying | 80°C for 4–6h in a controlled dryer; confirm spool temperature rating |
| Print Environment | Enclosure recommended for large or warp-sensitive parts; provide suitable ventilation |
| Nozzle Wear Control | Use hardened ≥0.6mm nozzle; inspect drive gears and melt path during long runs |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Guard Lattice Print Orientation | Align primary load paths with continuous perimeter roads; test Z-direction layer adhesion separately |
| Matte Surface Consistency | Use dry filament, a stable wall speed and controlled nozzle flow to reduce gloss variation on visible walls |
| Thin Honeycomb Ribs | Use a 0.6mm wear-resistant nozzle and set line width/wall count to match the rib geometry |
| Corner Lift & Bed Adhesion | Clean the surface, use PA-specific adhesive, a 5–10mm brim where needed, and avoid cold drafts |
| Humidity & Feeding | Pre-dry nylon; print directly from a dry box to limit moisture-driven bubbling or stringing |
| Retraction & Flow | Calibrate flow and pressure advance; keep retraction conservative to protect the melt path |
| Frame Joints & Fasteners | Increase perimeters around bolt bosses; align main stresses within the XY plane and check fit on the first production sample |
Printer Brand Starting Settings
| Printer Brand | Nozzle | Bed | Speed | Notes |
|---|---|---|---|---|
| Bambu Lab X1 / P1 Series* | 260–280°C | 90–100°C | 40–80 mm/s | Use a compatible hardened nozzle/hotend, PA adhesive and a dry external feed path |
| Prusa CORE One / MK4S* | 260–280°C | 90–100°C | 40–70 mm/s | Fit a wear-resistant nozzle and PA-compatible sheet; keep the filament dry during extended runs |
| Creality K1 / K1 Max* | 260–280°C | 95–100°C | 40–70 mm/s | 100°C maximum bed; install a wear-resistant nozzle and use an enclosure for wide lattice panels |
| QIDI Plus4 / Plus5* | 260–280°C | 90–100°C | 40–90 mm/s | Use a 0.6mm wear-resistant nozzle, dry-box feed and a stable chamber for larger supports |
| Flashforge Creator 4* | 260–280°C | 90–100°C | 40–70 mm/s | Select a PA-CF-capable extruder module with a hardened nozzle; calibrate material flow for lattice details |
*Start with a hardened 0.6mm nozzle, dry filament and a PA-compatible adhesive surface. Adjust volumetric flow and cooling for the selected hotend and lattice geometry; keep the Creality K1 / K1 Max bed at or below 100°C.
PA12-CF15 Process & Performance Characteristics
| Characteristic | Material / Process Reference | Notes |
|---|---|---|
| Carbon Fiber Reinforcement | 15% carbon fiber in PA12 | Our custom Industrial Black composite for rigid lattice ribs and four-column frame prototypes |
| Surface Appearance | Opaque charcoal-black / soft matte | Useful for low-glare guards and visible industrial support hardware |
| Recommended Nozzle | Hardened / wear-resistant ≥0.6mm | Reduces risk of brass nozzle abrasion and improves clearance for fiber-filled melt |
| Moisture Management | 80°C × 4–6h drying guidance | Dry feeding helps control surface bubbling, stringing and extrusion variation |
| Structural Print Setup | 3–5 perimeters; 40–60% infill for load-focused prototypes | Use continuous fiber-filled walls around columns, mounting bosses and corner junctions |
| Print Throughput Range | 40–80 mm/s recommended; 30–120 mm/s tuning | Choose a stable melt-flow profile for large guards and slower outer walls for fine visual detail |
| Directional Properties | Layered FDM/FFF construction | Design and test for load orientation, especially at fastener bosses and Z-axis joints |
Application Focus: Lattice Guards & Support Frames
| Application Focus | Part / Feature | Practical Notes |
|---|---|---|
| Lattice Guards | Honeycomb and mesh-style equipment covers | Match rib pitch to a 0.6mm nozzle line width, reinforce screw anchors and select non-safety-rated cover applications |
| Support Frames | Four-column mounting structures | Plan continuous load paths and verify creep, layer orientation and screw-boss behavior |
| Factory Jigs & Fixtures | Alignment blocks, locating stops and brackets | Allow for dimensional calibration and repeated-clamping trials before production use |
| Equipment Housings | Rigid covers and non-electrical mounting features | The matte industrial-black finish helps visual integration; qualify temperature and chemical exposure |
| Engineering Print Farms | Small-batch trial components and replacement prototypes | Standardize drying, spool handling and build profiles for repeat jobs |
Storage Guide
- Keep unopened units vacuum sealed with their desiccant until the next production run
- After opening, return the spool to an airtight dry box with fresh desiccant
- Dry filament at approximately 80°C for 4–6h before critical jobs; transfer to a heat-safe reel if required
- Feed directly from dry storage during long prints, especially in humid production facilities
- Store away from water, direct sunlight and heat sources; inspect brittleness or moisture symptoms before restarting
OEM / ODM Services
We support PA12-CF15 procurement programs with neutral export units, custom logo labels, fully branded cartons, application-specific product naming and barcode/label layout coordination. For qualified projects, we also discuss custom colors, 2.85mm or larger-spool formats, subject to technical feasibility, purchase volume and written specification approval. Our team aligns the sample, packaging artwork and order specification before scheduling the production batch.
MOQ Reference: Neutral packaging from 50 spools; OEM/private-label packaging typically 500–1,000 spools according to scope.
Quality Control
- We identify the agreed PA12-CF15 formulation and production order before extrusion, keeping the correct grade tied to the batch record.
- We check 1.75mm filament diameter against the ±0.03mm specification at production checkpoints and associate the results with the batch.
- We inspect winding tension, coil appearance and physical spool condition before individual packing.
- We inspect vacuum-seal integrity and confirm desiccant inclusion for moisture-sensitive nylon export units.
- We reconcile the batch ID, SKU labels and approved OEM artwork before sealing master cartons.
- We check carton quantities, export labels and shipment documentation against the order before dispatch.
Certifications & Technical Documentation
- Dedicated PA12-CF15 TDS: We have a technical data sheet for our SSSray Industrial Black 15% carbon-fiber grade and provide the corresponding version for customer material approval.
- Batch COA: Our certificate of analysis supports review of the relevant production batch and the acceptance data recorded for the ordered material.
- RoHS Test Report: We have RoHS testing documentation for this SKU and check the report’s formulation scope and date against the customer’s requested supply.
- SDS / REACH Requests: Our team coordinates handling and shipping documentation and confirms destination-market requirements for the specific grade; REACH evidence is supplied where applicable and available.
- Additional Test Programs: We coordinate agreed customer test standards and sample quantities when a project needs extra independent testing.
- Factory Engineering Support: We connect sample lot identification, print profiles and your guard or fixture geometry to the same production specification used for repeat orders.
Frequently Asked Questions
What does the 15% carbon fiber content mean for part selection?
We combine PA12 nylon with 15% carbon fiber for firm honeycomb ribs, fixture brackets and structural frame prototypes. For four-column supports, position the main load along continuous printed walls and strengthen the fastener locations.
Can I use this PA12-CF15 on Bambu Lab, Prusa or Creality printers?
Yes. We recommend equipped 1.75mm FDM systems with an all-metal hotend reaching 280°C, a 0.6mm wear-resistant nozzle and a suitable heated bed. Bambu Lab, Prusa, Creality, QIDI and Flashforge engineering configurations are useful starting platforms. Keep the spool dry and match the bed temperature to the machine limit.
Which print settings should I start with?
Start at 270°C nozzle, 95°C bed, 60 mm/s, 0–10% fan and 0.24mm layers with a hardened 0.6mm nozzle. Our recommended production-quality range is 260–280°C and 40–80 mm/s. Use the wider tuning range for larger, simpler frame sections after calibrating melt flow.
How do I reduce nylon moisture problems?
Pre-dry at approximately 80°C for 4–6h using a controlled dryer and a heat-rated spool or reel, then print directly from a dry box. Maintain dry storage after use. Wet nylon can cause bubbling, stringing and rough surfaces.
Can qualified B2B buyers request samples?
Yes. Verified B2B customers can request up to three complimentary 1kg sample spools. Send us your printer model, target part and destination; we confirm the sample selection, freight route and payer before dispatch.
What are the MOQ and private-label options?
Neutral packaging begins at 50 spools. OEM/private-label packaging normally requires 500–1,000 spools, depending on box, label, branding and specification scope. We can review custom diameter or color requests separately.
Do you have TDS, SDS or compliance reports for this SKU?
Yes. We have an Industrial Black PA12-CF15 TDS, batch COA and RoHS test documentation for this grade. Send us the product specification, order batch and destination market, and our team will match the correct reports. We also coordinate relevant SDS and market-specific paperwork on request.
What are the payment terms and lead times for bulk orders?
Our standard terms are 30% T/T deposit and 70% before shipment, with FOB Ningbo or EXW pricing. Standard orders typically take 7–15 days; customized orders usually take 15–25 days after specification and order confirmation.
Get Factory-Direct Industrial Black PA12-CF15 Pricing
Tell us whether you are supplying honeycomb guards, structural frame prototypes or a private-label engineering filament line. We will prepare a focused bulk quote, sample route and export packaging proposal around your required volume and destination.



Related products
-

Industrial PA12 Nylon 3D Printing Filament 1.75mm 1kg – Highly Tough, Low Moisture Absorption & Chemical Resistant for Engineering Prototypes & End-Use Parts
-
PA12-GF Glass Fiber Reinforced Nylon Filament 1.75mm 1kg – Industrial Grade Engineering Polyamide for Structural Manufacturing & Functional Prototyping
-
SSSray PA12-CF 10% Carbon Fiber Nylon 3D Printer Filament 1.75mm – Graphite Black for Functional Mounting Frames (نايلون 12 معزّز بالألياف الكربونية)
-
Industrial Grade PETG-CF Filament 1.75mm 1KG | Carbon Fiber Reinforced PETG for High-Strength Tools, Jigs & Functional Prototypes | OEM/ODM Factory Direct