Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

PA12-CF Functional Parts Series | Wholesale | OEM / ODM
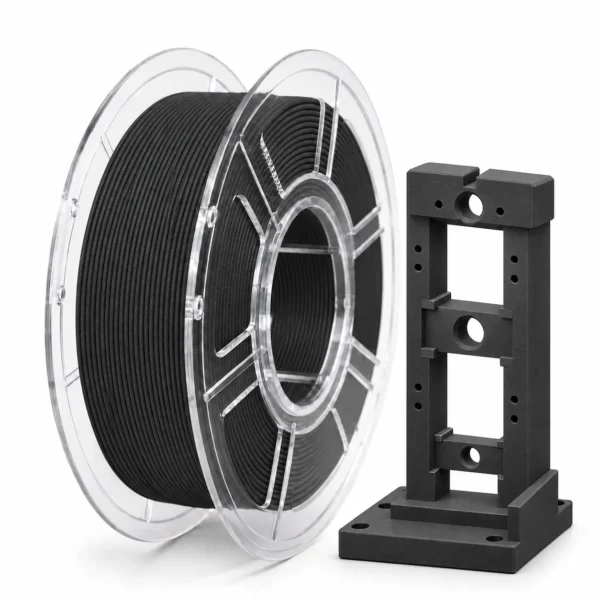
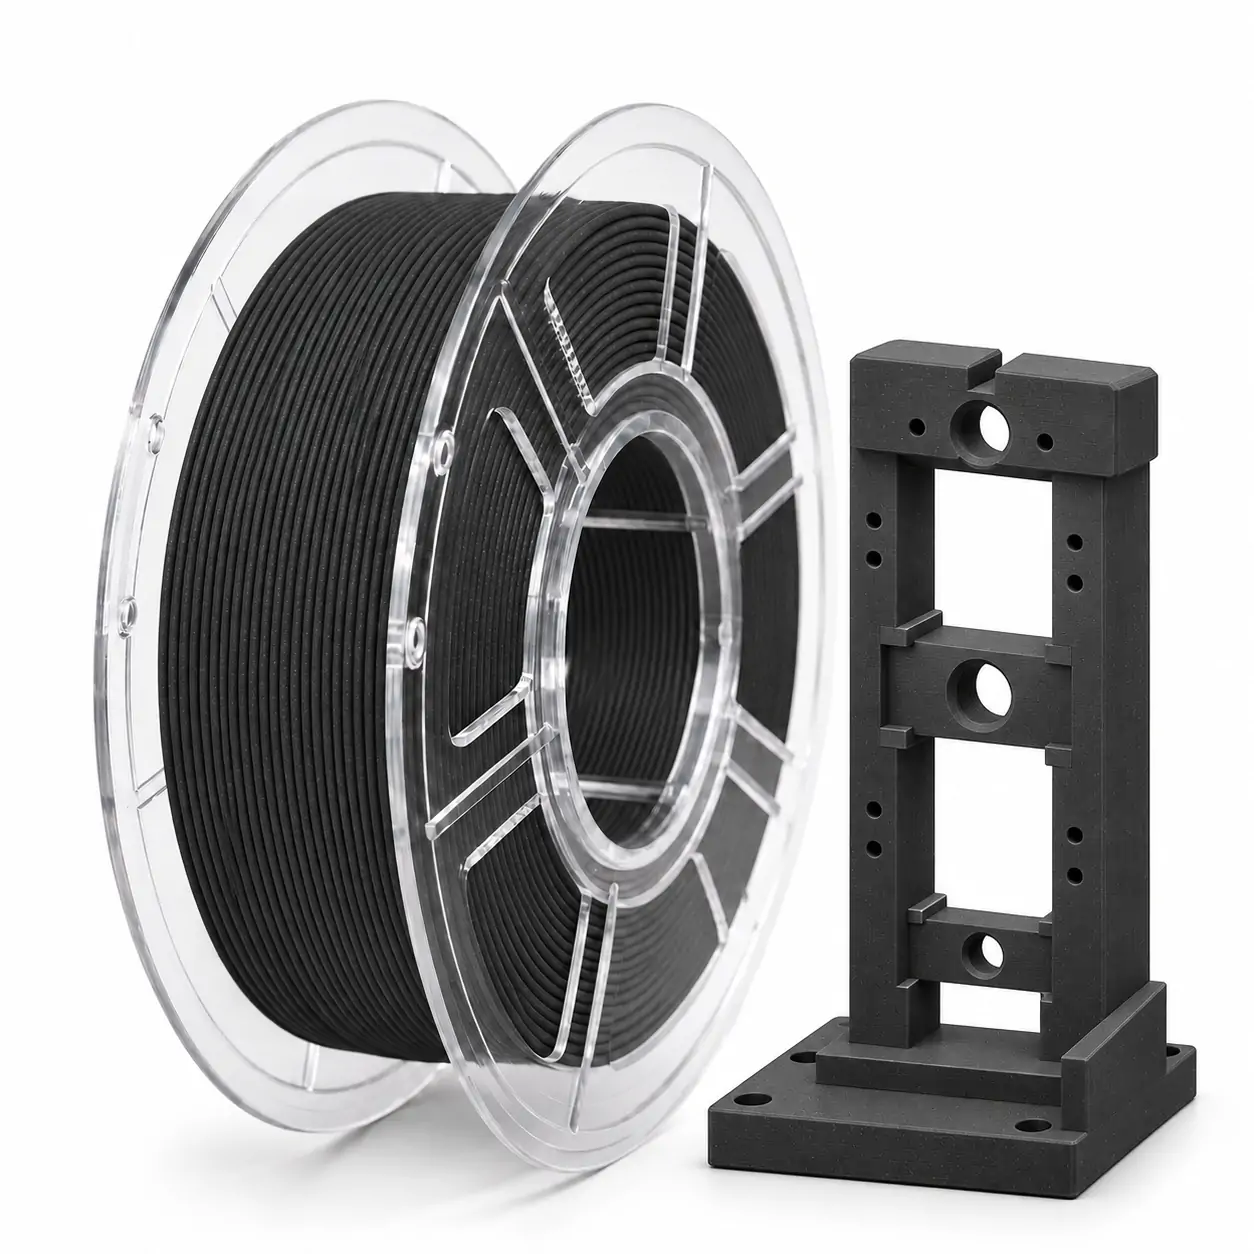
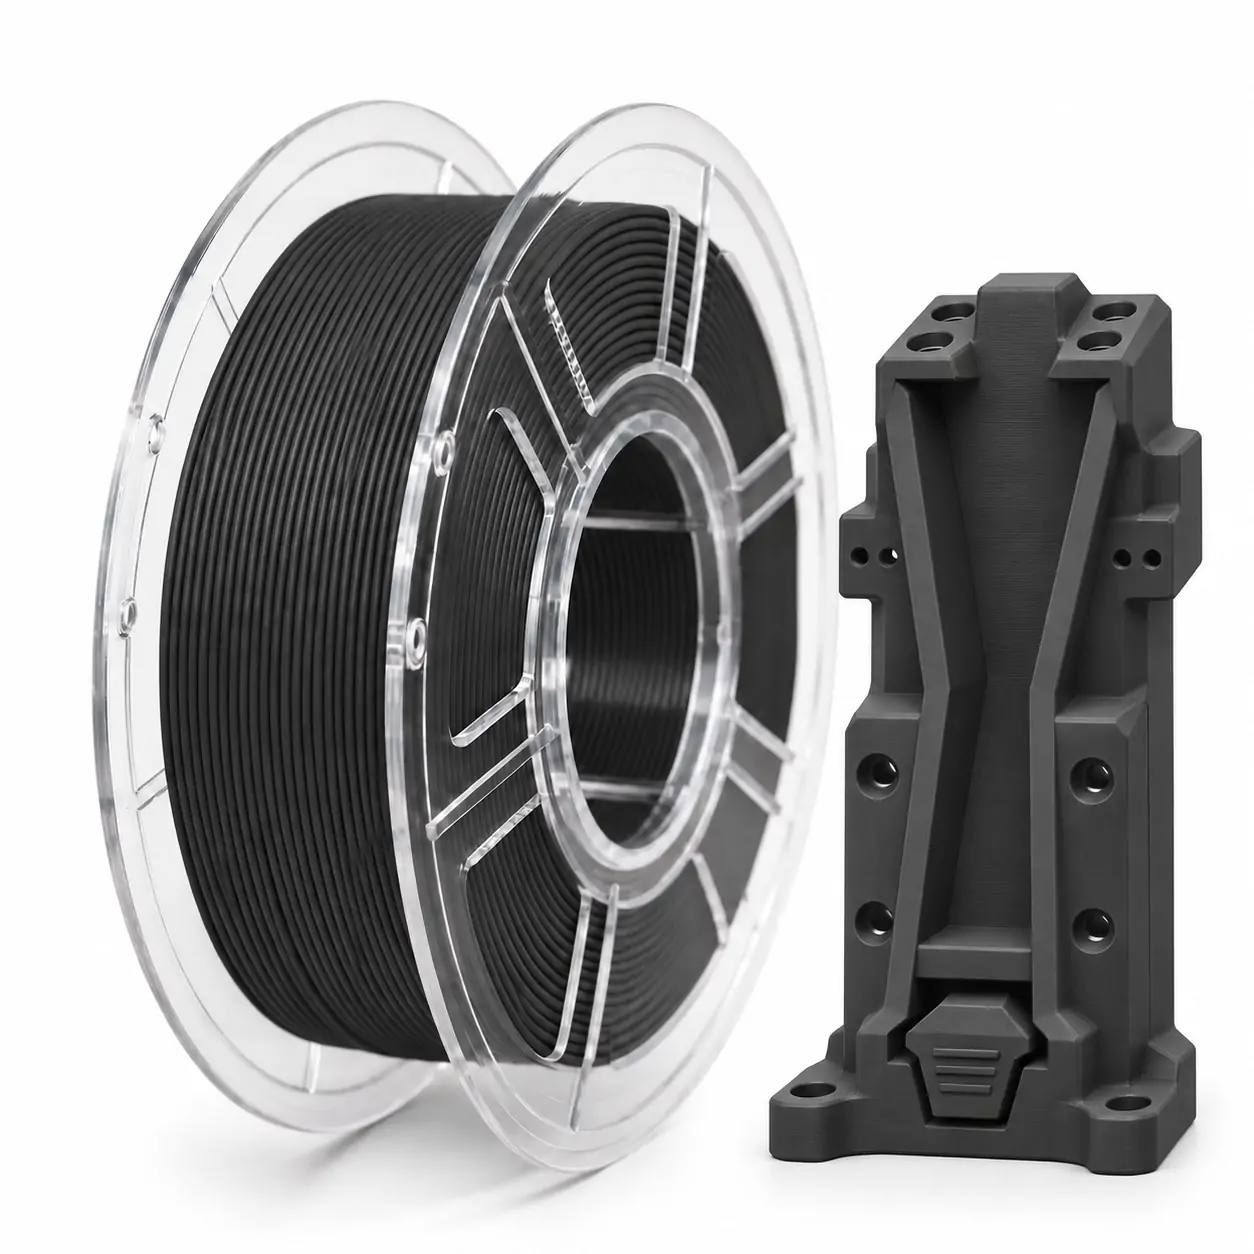
SSSray PA12-CF 10% Carbon Fiber Nylon 3D Printer Filament 1.75mm – Graphite Black for Functional Mounting Frames (نايلون 12 معزّز بالألياف الكربونية)
10% carbon-fiber-reinforced Nylon 12 in a consistent Graphite Black finish, developed for functional frames, jigs, fixtures, and engineering buyers.
Bring us your mounting-frame drawing, fit requirements, and purchasing forecast. We can coordinate filament sample evaluation, repeat-order specifications, private-label packaging, and export supply from a single manufacturing partner.
MaterialPA12-CF 10%
SeriesFunctional Parts
Color EffectGraphite Black / Matte
Diameter1.75mm
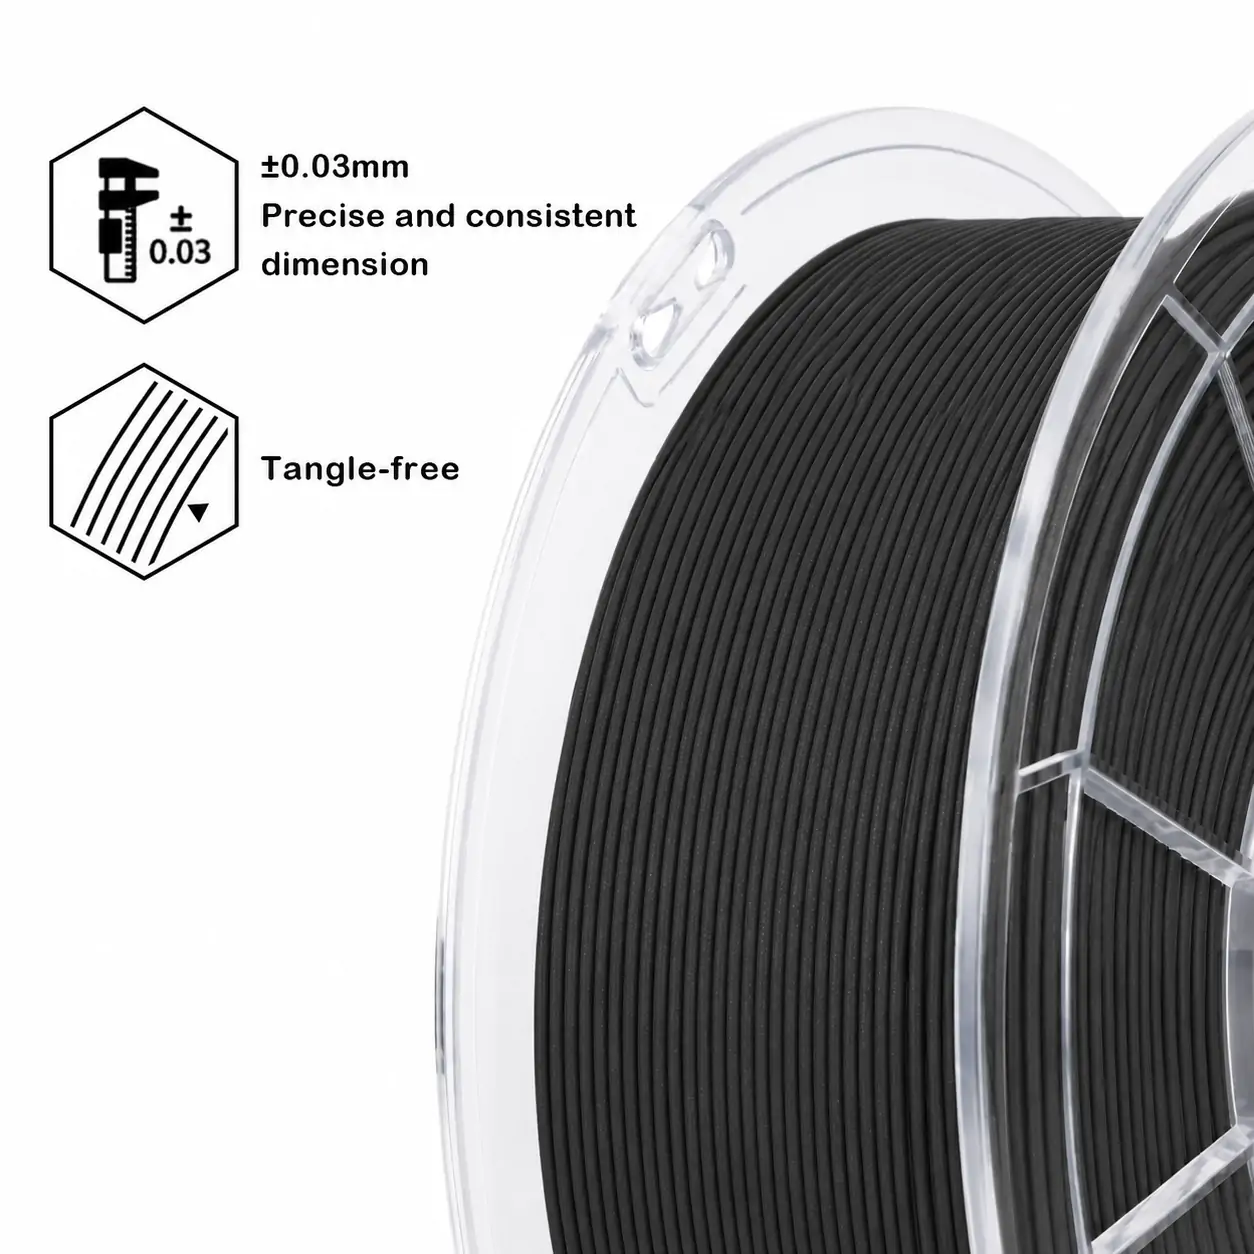
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp260–280°C
Bed Temp70–100°C
Print Speed30–200 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 working days; customized orders typically 15–25 working days.
Product Overview
SSSray PA12-CF 10% Carbon Fiber Nylon delivers an XY tensile modulus of 6,250 MPa, XY tensile strength of 81 ± 3 MPa and a heat-deflection temperature of 145°C at 0.455 MPa for demanding functional-printing projects. Our Nylon 12 compound combines 10% carbon-fiber reinforcement with PA12 moisture stability, making it an effective choice for mounting frames, mechanical brackets, jigs and low-volume industrial fixtures. The Graphite Black shade is deep charcoal-black, solid and opaque, with a refined soft-matte finish. It gives three-bore mounting frames, screw bosses and channelled components a purposeful engineering appearance.
We manufacture this filament in standard 1.75mm diameter with a specified ±0.03mm tolerance, packed as a 1kg plastic spool in a vacuum-sealed bag with desiccant. Our 50-spool neutral-packaging MOQ helps distributors introduce a premium engineering grade without a large opening commitment, while OEM projects typically begin at 500–1,000 spools. Send us your mounting-frame drawings, printer models and purchasing forecast; our team will coordinate samples, label specifications, production scheduling and export delivery. You get a technical nylon product with clear performance figures and a supply program built for repeat orders.
Why This Product Stands Out
Our Graphite Black PA12-CF10 combines 10% carbon fiber reinforcement with a PA12 nylon base for mounting frames, jigs and functional fixtures. We specify an XY tensile modulus of 6,250 MPa and a heat-deflection temperature of 145°C at 0.455 MPa, along with a deep charcoal-black soft-matte finish for visible industrial components. Our 1.75mm filament is manufactured to a ±0.03mm diameter specification and supplied with moisture-protective packaging, application-focused printing guidance, sample support and OEM private-label options.
Key Selling Points
Stable Diameter Control
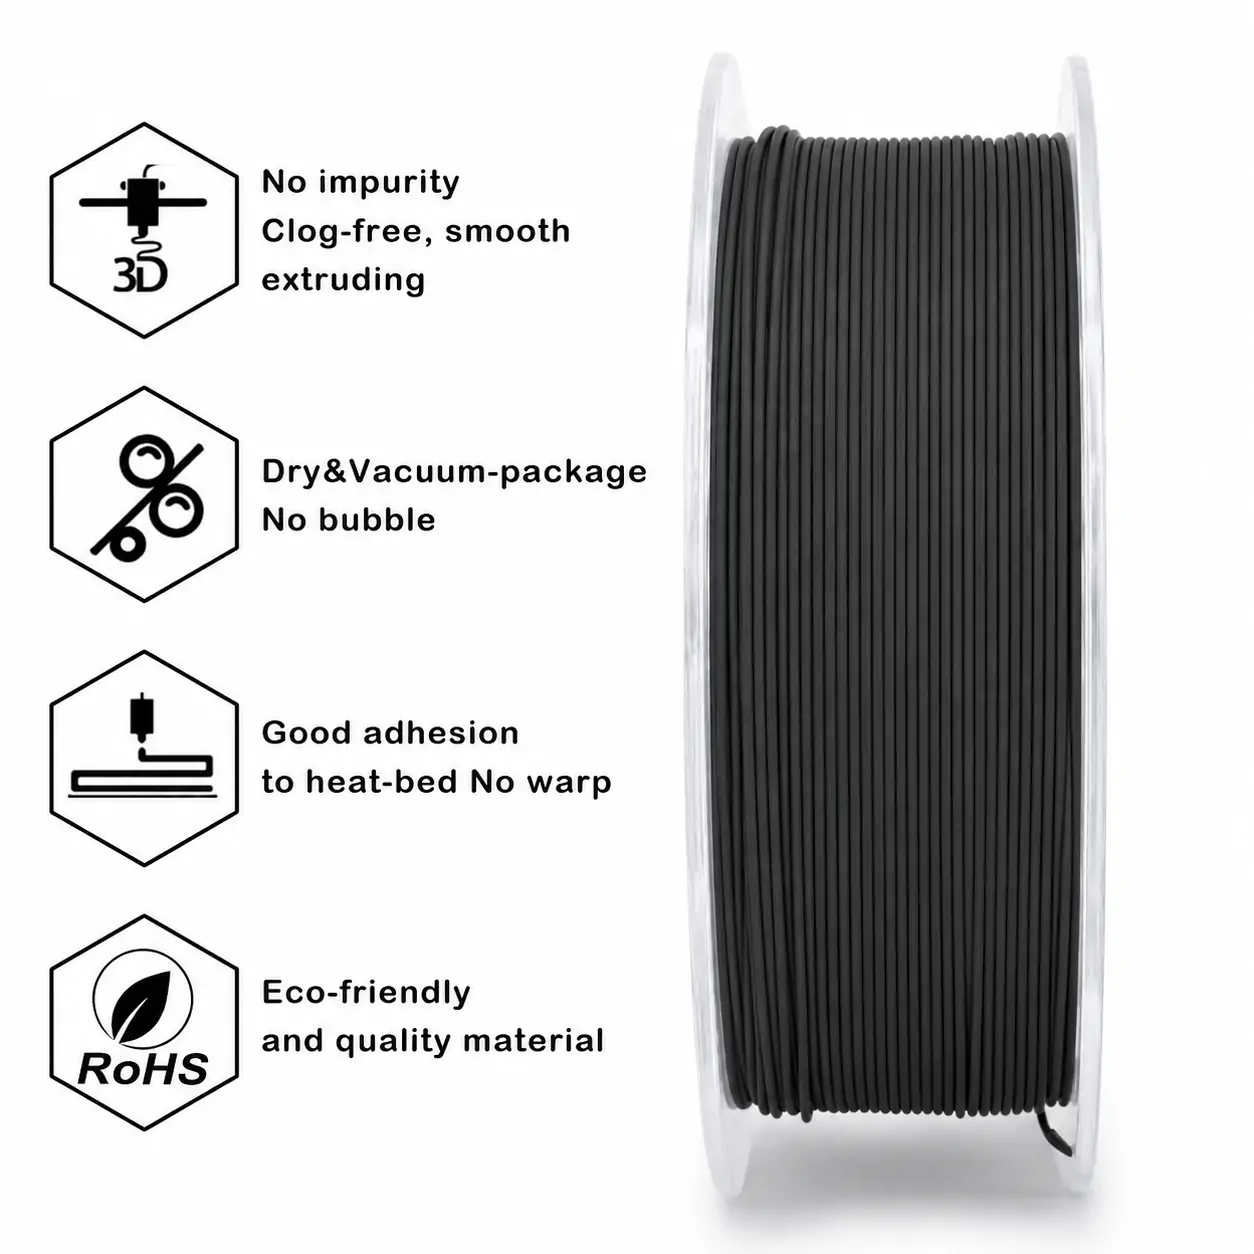
Our 1.75mm ±0.03mm extrusion specification helps your print farm standardize feeding and material acceptance.
Smooth Extrusion
Run our 260–280°C processing window with dry filament and a wear-resistant nozzle for clean, consistent carbon-filled nylon flow.
Graphite-Black Matte Finish
Our opaque charcoal-black shade produces a low-sheen technical surface on visible brackets, housings and frames.
Functional Frame Focus
6,250 MPa XY tensile modulus makes our PA12-CF10 a compelling option for rigid mounting frames, alignment jigs and machinery fixtures.
Wholesale Supply Planning
Order standard 1kg spools from 50 units, with 7–15 working-day standard lead time and FOB Ningbo / EXW terms.
OEM / ODM Ready
We build your PA12-CF range with approved private-label artwork, custom cartons, spool choices and repeat-order planning.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| XY Tensile Modulus: 6,250 MPa | High rigidity for frame rails, alignment supports and functional fixtures |
| XY Tensile Strength: 81 ± 3 MPa | Documented engineering-grade strength for printed-bracket material selection |
| HDT: 145°C at 0.455 MPa | Defined heat-deflection performance for elevated-temperature component design |
| Density: 1.07 g/cm³ | Useful weight and material-consumption reference for lightweight assemblies |
| Graphite Black / Soft Matte | Uniform opaque charcoal-black surfaces for visible industrial components |
| 1.75mm ±0.03mm; Vacuum + Desiccant | Controlled diameter specification and moisture-protective export packing |
Balanced Quality and Cost Efficiency
Your true PA12-CF cost is the cost of consistent, usable functional parts. Our 10% carbon-fiber nylon combines 6,250 MPa XY tensile modulus, 1.75mm ±0.03mm diameter control and vacuum-sealed packaging to support reliable purchasing and production workflows. Start with 50 neutral-packaged spools, then scale into private-label cartons and repeat orders as your frame, fixture or industrial-filament program grows. We work with your team on print settings, approved color, packing specifications and bulk scheduling. For load-critical parts, we can coordinate specimen and part-level qualification against your assembly requirements. Explore our carbon-fiber filament wholesale range and filament qualification services.
How We Work
1
Application & Volume Review
2
Material & Packaging Confirmation
3
Printer & Part Qualification
4
Artwork & Label Approval
5
Order Scheduling
6
Batch Review & Shipment
Material Comparison Guide
| Material | Reinforcement | Print Conditions | Material Behavior | Typical Use |
|---|---|---|---|---|
| PA12-CF 10% (this SKU) | 10% carbon fiber in PA12 nylon | 260–280°C nozzle, 70–100°C bed, hardened nozzle and dry feed | 6,250 MPa XY tensile modulus; 145°C HDT at 0.455 MPa | Mounting frames, brackets, inspection fixtures |
| Unfilled PA12 | No carbon-fiber filler | Dry filament and nylon-compatible adhesion | More flexible response than a fiber-filled grade; grade dependent | Clips, housings, functional prototypes |
| PA6-CF | Carbon-fiber-filled PA6; percentage varies | High-temperature setup and strict moisture control | PA6 chemistry has different moisture response from PA12 | Tooling, load-oriented industrial prototypes |
| PETG-CF | Carbon-fiber-filled PETG; percentage varies | Generally lower nozzle temperature than PA-CF | Different thermal and moisture profile from nylon | Visual fixtures, housings, non-hot-zone brackets |
| PLA-CF | Carbon-fiber-filled PLA; percentage varies | Lower-temperature processing; abrasive nozzle recommended | Stiff surface feel with PLA’s heat-resistance limitations | Concept models, presentation fixtures, visual prototypes |
Technical Specifications
| Product Name | SSSray PA12-CF 10% Carbon Fiber Nylon 3D Printer Filament 1.75mm – Graphite Black for Functional Mounting Frames (نايلون 12 معزّز بالألياف الكربونية) |
|---|---|
| Material | PA12 (Nylon 12) reinforced with 10% carbon fiber; FDM/FFF filament |
| Product Series | SSSray PA12-CF Functional Parts Series – 10% Carbon Fiber Nylon for Mounting Frames & Fixtures |
| Color / Effect | Graphite Black; deep charcoal-black, solid and opaque; soft matte, low-sheen, non-metallic |
| Filament Diameter | 1.75mm standard; 2.85mm subject to order confirmation |
| Diameter Tolerance | ±0.03mm (specified) |
| Net Filament Weight | 1kg (2.2 lb); 3kg / 5kg subject to feasibility confirmation |
| Gross Weight | 1.3kg per standard 1kg packaged unit |
| Spool Type | Plastic spool; larger-capacity and custom spool options by arrangement |
| Packaging | Vacuum-sealed with desiccant; individual outer box |
| Hotend Requirements | All-metal hotend capable of 280°C; hardened steel or equivalent wear-resistant nozzle, preferably 0.6mm |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers with a 280°C-capable hotend, wear-resistant nozzle, heated bed and nylon-ready feed path |
| Typical Applications | Functional mounting frames, sensor brackets, equipment fixtures, alignment jigs, workshop tooling, and low-volume engineering parts |
| OEM / ODM | Neutral, private-label, and custom pack development supported |
| Carbon-Fiber Content | 10% |
| Density | 1.07 g/cm³ (ISO 1183 / ASTM D792) |
| XY Tensile Strength | 81 ± 3 MPa (ISO 527-2 / ASTM D638) |
| XY Tensile Modulus | 6,250 MPa (ISO 527-2 / ASTM D638) |
| XY Flexural Strength | 95 MPa (ISO 178 / ASTM D790) |
| XY Flexural Modulus | 5,000 MPa (ISO 178 / ASTM D790) |
| Elongation at Break | 3–8% (ISO 527-2 / ASTM D638) |
| HDT at 0.455 MPa | 145°C (ISO 75-2 / ASTM D648) |
| HDT at 1.82 MPa | 98°C (ISO 75-2 / ASTM D648) |
| Water Absorption (24h) | 0.15–0.25% (ISO 62) |
| Melting Temperature | 178–185°C (ASTM D3418) |
| Specimen Reference | Dry printed XY specimens; 0.20mm layer height and 100% infill for the stated mechanical and thermal typical values |
| Technical Documents | Download our PA12-CF TDS v2.0 (10% carbon fiber); request the applicable SDS and market-specific documents with your RFQ |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | 260–280°C; 270°C is our standard starting point |
| Usable Nozzle Range | 260–280°C, with an all-metal hotend and wear-resistant nozzle |
| Recommended Bed Temperature | 70–100°C; begin around 85°C with nylon-compatible adhesion |
| Recommended Print Speed | 60–100 mm/s for production-oriented functional parts |
| Usable Print Speed | 30–200 mm/s; tuned high-throughput profiles can reach 100–200 mm/s where extrusion flow and part geometry allow |
| Recommended Nozzle | 0.6mm hardened steel / equivalent wear-resistant; 0.4mm only after a clogging trial |
| Layer Height | 0.16–0.28mm on a 0.6mm nozzle; 0.20–0.24mm suits frame and channel details |
| Part Cooling | 0–20% for structural layers; up to 50% where small bridges need extra cooling |
| Direct-Drive Retraction | 0.5–1.5mm at 25–40 mm/s |
| Bowden Retraction | 2.0–3.5mm at 25–40 mm/s; tune against stringing and feed friction |
| Wall Count | 3–5 perimeters for functional brackets and fixture shells |
| Infill | 20–30% for fit/function prototypes; 40–60% for qualified higher-load designs |
| First Layer Speed | 15–25 mm/s |
| Bed Adhesion | Clean PEI, G10 / Garolite, or glass with a nylon-compatible adhesive/release layer |
| Drying Before Printing | 80°C for 4–6 hours before printing; ensure your spool and dryer are rated for this temperature |
| Dry Feed During Printing | Use a sealed dry box or suitable heated filament dryer; aim for low ambient feed-path humidity |
| Chamber Temperature | 45–65°C recommended in an enclosed engineering printer; match bed adhesion and part geometry |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Starting Point | Dry at 80°C for 4–6 hours and start near 270°C nozzle / 85°C bed with a 0.6mm hardened nozzle |
| Three-Bore Frame Accuracy | Print a small hole-tolerance coupon first; compensate XY hole sizes in CAD or slicer only after measurement |
| Channelled Mount Finish | Use 0.20–0.24mm layers, slower external walls, and consistent extrusion to retain groove definition |
| Layer Adhesion | Reduce unnecessary cooling; run a printed coupon to verify Z-direction bonding before load-bearing use |
| Warping & First Layer | Use PA-compatible adhesion and a brim for broad footprints; tune bed heat from a small test part |
| Moisture Symptoms | Dry again if extrusion pops, bubbles appear, or the matte surface becomes uneven |
| Nozzle Wear | Avoid standard brass and inspect nozzle size/quality across long production runs |
| Volume Qualification | Fix material lot, hardware, slicer settings and acceptance dimensions before repeat production |
Printer Brand Starting Settings
| Printer Brand | Nozzle | Bed | Speed | Practical Notes |
|---|---|---|---|---|
| Bambu Lab X1 Carbon | 265–280°C | 75–90°C | 60–120 mm/s | Hardened nozzle, dry feed and PA-compatible adhesion; tune flow before using the upper speed range |
| Prusa CORE One / One+ | 260–280°C | 75–95°C | 50–100 mm/s | Use a wear-resistant nozzle and nylon-suitable build plate; confirm actual chamber conditions |
| Creality K1 Max | 265–280°C | 75–95°C | 60–120 mm/s | Install or verify a hardened nozzle and dry feed; keep the bed below its 100°C equipment limit |
| QIDI Q1 Pro | 265–280°C | 80–95°C | 60–120 mm/s | Use its controlled chamber and a hardened nozzle to support repeatable fixture production |
| Flashforge Creator 4 | 260–280°C | 75–95°C | 50–100 mm/s | Select the high-temperature extruder and wear-resistant nozzle; keep dry filament feeding continuously |
We supply these machine-specific starting profiles for faster setup. Set the final speed against your part size, extrusion flow, nozzle hardware and required layer adhesion.
Performance Characteristics
| Characteristic | Material Behavior / Reference | Practical Notes |
|---|---|---|
| XY Tensile Strength | 81 ± 3 MPa; ISO 527-2 / ASTM D638 | Material-selection reference for load-bearing brackets and assemblies |
| XY Tensile Modulus | 6,250 MPa; ISO 527-2 / ASTM D638 | Rigidity reference for mounting frames and dimensional support |
| Heat Deflection | 145°C at 0.455 MPa; 98°C at 1.82 MPa | Two stated test loads help customers select the appropriate heat-design margin |
| Density and Moisture | 1.07 g/cm³; 24h water absorption 0.15–0.25% | Useful inputs for weight planning, conditioning and nylon-material selection |
| Surface Appearance | Graphite Black / opaque / soft matte | Consistent low-sheen presentation for visible industrial fixtures |
| Manufacturing Reference | 1.75mm ±0.03mm; vacuum sealing with desiccant | Specified feedstock diameter and packing for bulk distribution |
Applications
| Application | Application Focus | Practical Notes |
|---|---|---|
| Functional Mounting Frames | Alignment and equipment integration | For multi-hole or channelled frames, check hole fit, bolt torque and print orientation |
| Sensor & Camera Brackets | Workshop mounting and enclosure integration | Validate stiffness and vibration response on the actual assembly |
| Manufacturing Jigs | Positioning and workholding aids | Use stable wall thicknesses and locate stress away from layer interfaces |
| Robotics & Automation Fixtures | Custom low-volume functional components | Measure tolerance and verify fastener retention after print conditioning |
| Inspection / Assembly Aids | Repeated setup and alignment operations | Establish dimensional acceptance criteria before multi-spool production |
Storage Guide
- Keep unopened PA12-CF10 units sealed in the supplied vacuum bag with desiccant until required for printing
- After opening, move the spool to a low-humidity dry box; avoid leaving nylon exposed on an open printer for extended periods
- Dry at 80°C for 4–6 hours before printing; use a temperature-rated spool and filament dryer
- During long functional-part prints, feed from a sealed dryer or controlled dry box and watch for popping or porous extrusion
- For repeat orders, label spool lot, opening date, drying cycle and acceptance test results to make reorders easier to compare
OEM / ODM Services
We build PA12-CF wholesale and private-label programs around your target customers and printer fleet. Choose neutral cartons, your own product labels, printed retail boxes, custom shade discussions, or agreed spool/pack formats. Share the design file, required artwork languages, label codes, desired quantities, and destination market. We can align a sample and approval stage before production scheduling.
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools. Standard lead time 7–15 working days; customized 15–25 working days, subject to scheduling and approved specifications.
Quality Control
- Record diameter checks against the 1.75mm ±0.03mm specification at defined sampling points
- Inspect winding appearance and spool edges to reduce feed snags during continuous printer operation
- Check the Graphite Black shade and low-sheen finish against an approved physical control sample
- Inspect vacuum seal condition and desiccant inclusion before export packing
- Link production lot identification with retention samples and applicable inspection documents
- Review carton labeling, count, order artwork and shipment instructions before dispatch
Technical & Compliance Documents
- PA12-CF Technical Data Sheet: our released engineering-grade specification includes tensile strength, tensile modulus, heat deflection and printing conditions
- SDS / MSDS: we provide material-family safety information and match the document revision to your purchase and destination market
- RoHS / REACH requests: send us the required market and report scope so our team can arrange the applicable documentation review
- Independent testing: we coordinate requested test methods and third-party inspection requirements during B2B order planning
- Batch and export records: we support lot identification, packing documents and customer-approved quality requirements
Frequently Asked Questions
What is the minimum order quantity for this PA12-CF10 filament?
Our neutral-packaging MOQ starts at 50 spools. OEM / private-label packaging programs typically start at 500–1,000 spools, depending on approved customization.
Which printers are suitable for this carbon-fiber nylon?
Our PA12-CF10 runs at 260–280°C nozzle temperature with a 70–100°C heated bed, a hardened nozzle and dry filament feed. We supply starting profiles for Bambu Lab X1 Carbon, Prusa CORE One, Creality K1 Max and other open-material engineering printers.
Is Graphite Black a metallic or glossy filament?
No. Graphite Black is a solid, opaque deep charcoal-black shade with a soft matte, low-sheen finish. It is intended for a restrained engineering appearance on mounting frames, brackets, and fixtures.
Is a 0.6mm hardened nozzle necessary?
We recommend 0.6mm hardened steel or an equivalent wear-resistant nozzle as the baseline. Carbon fiber is abrasive. A 0.4mm wear-resistant nozzle requires its own clogging and flow qualification, and ordinary brass is unsuitable for ongoing production.
How should we qualify printed mounting frames before placing a bulk order?
Send us your frame drawing, bore tolerances, screw-fit requirements and planned operating conditions. We help you organize a print trial using our 6,250 MPa XY modulus and 145°C HDT as material-selection references, then finalize the critical dimensions and assembly test targets before repeat orders.
Can qualified buyers request free samples?
Verified B2B buyers can request up to three complimentary sample spools after review. We agree the shipping cost and who pays it before dispatch. We can also ship to your appointed forwarder in China.
Are RoHS, REACH, SGS, TDS or SDS available for this exact SKU?
Our released PA12-CF technical data covers the 10% carbon-fiber grade, including XY strength, stiffness and heat deflection. We can arrange the applicable safety document and review RoHS, REACH or third-party test requests for your destination market and purchase requirements.
What are the payment, delivery and packaging terms?
We offer FOB Ningbo or EXW terms, normally with a 30% T/T deposit and 70% balance before shipment. Standard orders target 7–15 working days and custom orders 15–25 working days after specifications are approved.
Looking for a Reliable PA12-CF 10% Supply Partner?
Send us your PA12-CF10 requirements, target applications and order volume. Our team can coordinate technical qualification, OEM packaging and a clear bulk quotation for your market.



Related products
-

Wholesale PC-PBT-CF20 Carbon Fiber Filament 1kg (1.75mm)
-
Carbon Fiber PLA 3D Printer Filament 1.75mm by SSSray, PLA-CF Slate Gray – filamento PLA com fibra de carbono cinza – for Topology-Optimized Brackets & Vented Enclosures
-
SSSray Charcoal Black PA12-CF 5% Carbon Fiber Nylon Filament 1.75mm – PA12-filament met koolstofvezel for Functional Brackets & Housings
-
Industrial PA12 Nylon 3D Printing Filament 1.75mm 1kg – Highly Tough, Low Moisture Absorption & Chemical Resistant for Engineering Prototypes & End-Use Parts