Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

Engineering Composite Series | PPS-GF | B2B Supply
SSSray PPS-GF in Natural Ivory: Reinforced PPS 3D Printing Filament – filament PPS renforcé fibre de verre for Flanged Duct Elbows & Shaft Support Brackets
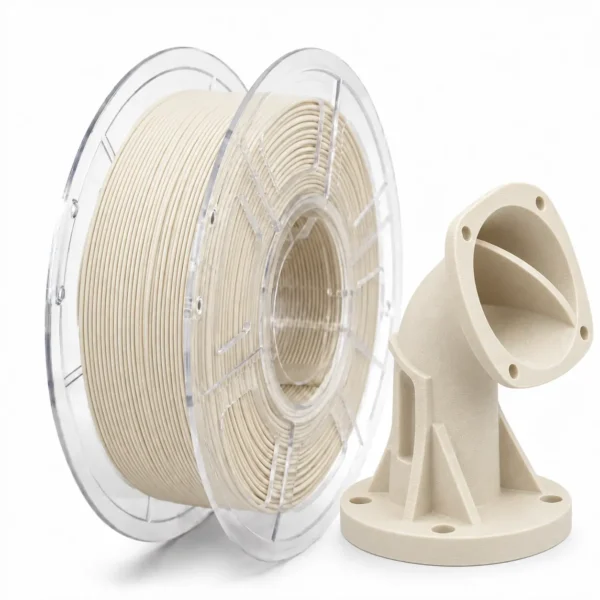
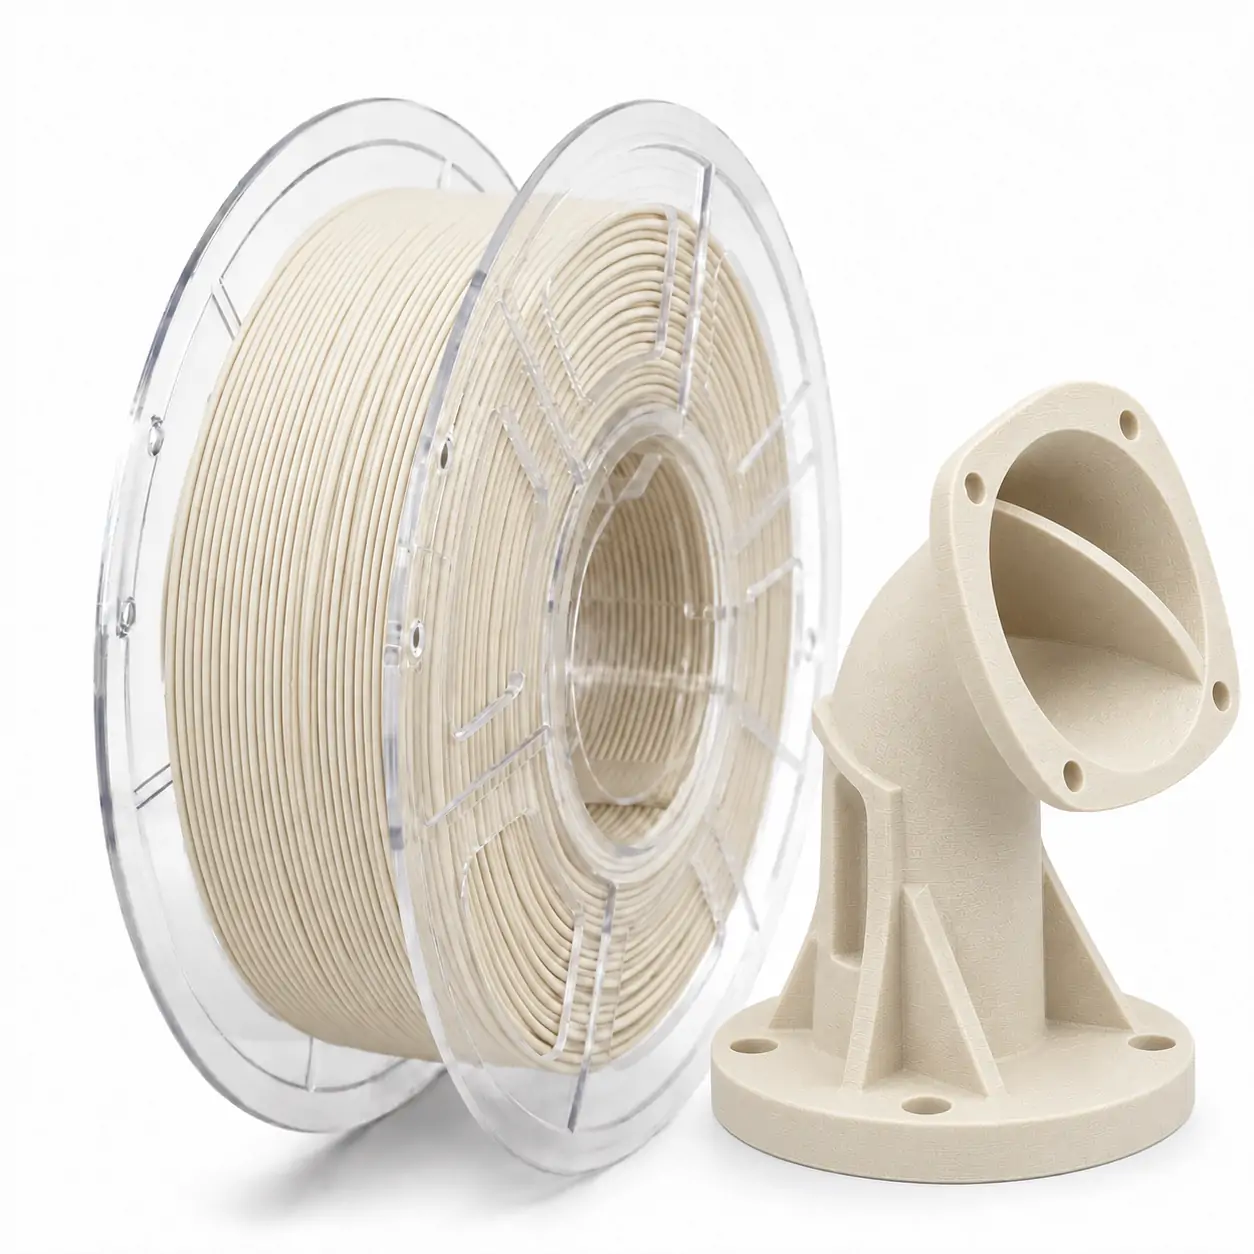
Natural Ivory glass-fiber reinforced PPS for high-temperature FDM/FFF production of duct fittings, shaft supports, mounting arms and dimension-sensitive industrial parts.
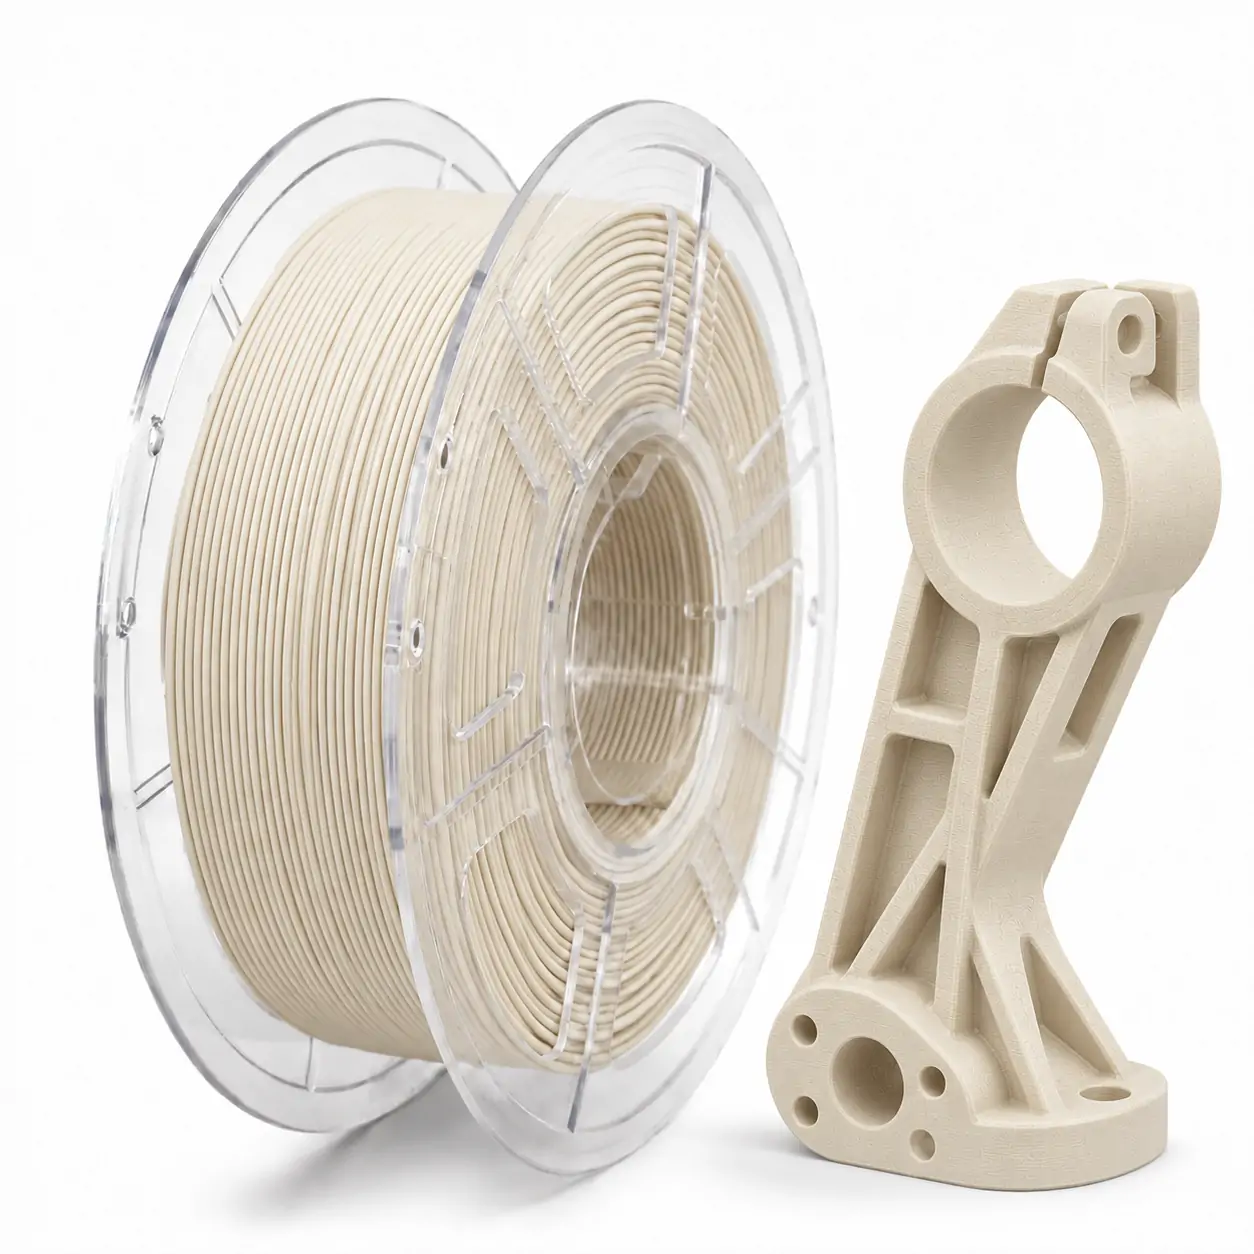
We supply this PPS-GF grade for buyers who need the thermal and chemical advantages of a PPS matrix together with glass-fiber reinforcement for stiffer, more dimensionally controlled functional parts. Natural Ivory gives the finished component a light warm cream tone with a fine matte fiber texture instead of the dark appearance associated with carbon-filled engineering filaments.
MaterialPPS-GF
SeriesEngineering Composite
Color EffectNatural Ivory
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp320–340°C
Bed Temp90–110°C
Print Speed40–100 mm/s
NozzleHardened 0.6mm Preferred
PackagingVacuum + Desiccant
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 days; customized orders typically 15–25 days.
Product Overview
SSSray Natural Ivory PPS-GF is a glass-fiber reinforced polyphenylene sulfide composite for high-temperature FDM/FFF production where stiffness, dimensional control, chemical resistance and stable functional geometry matter. Its Natural Ivory color is the palest shade in this PPS-GF line: a light warm cream tone that is visibly lighter and less yellow-brown than Natural Sand Beige or Desert Tan. Printed parts show a fine fiber-textured matte surface with subtle diffuse highlights rather than a glossy, silk, wood-filled or bone-filled appearance.
We supply this grade for flanged duct elbows with internal guide vanes, split-clamp shaft supports, gusseted mounting arms, fixtures and other industrial flow-path or support components. Standard 1kg spools, ±0.03mm diameter control, vacuum-sealed packaging and OEM/private-label support give distributors and industrial buyers a clear path from sample testing to repeat orders. For related reinforced materials and custom grades, see our wholesale glass fiber reinforced filament and custom engineering filament programs.
Built for Flow-Path Geometry & Rigid Support Parts
We supply Natural Ivory PPS-GF for rigid flanges, guide vanes, split clamps, ribs and gusseted supports where edge definition and dimensional control are important during assembly. Glass-fiber reinforcement supports these rigid geometries, while the light ivory finish gives engineering teams a clear visual distinction from black PPS-CF and darker reinforced grades without giving the part a decorative appearance.
Key Selling Points
Stable Diameter Control
±0.03mm nominal tolerance supports consistent feeding and repeatable PPS-GF process setup across B2B batches.
High-Temperature PPS Platform
Built for engineering parts operating beyond the normal material class of PLA, PETG and standard ABS.
Glass-Fiber Reinforcement
Supports rigid ribs, flange faces, clamp bodies and gusset geometry while maintaining the light Natural Ivory appearance.
Dry Export Packaging
Each standard spool is vacuum sealed with desiccant to protect material condition through warehouse storage and international transit.
Industrial B2B Supply
We supply this grade to distributors, industrial resellers, sourcing teams and private-label engineering-material buyers.
OEM / ODM Ready
We support custom labels, cartons, private-label packaging and project-specific B2B supply programs.
B2B Supply for PPS-GF Buyers
We supply Natural Ivory PPS-GF to distributors, industrial users and private-label buyers that need a reinforced high-temperature PPS material for ducting, mechanical supports, fixtures and industrial assemblies. The light ivory grade provides a clear alternative to black carbon-filled PPS, while the standard 1kg spool, 50-spool neutral-packaging MOQ and sample support allow buyers to test the material and printer setup before moving into repeat or OEM orders.
How We Work
1
Application Review
2
Grade & Document Confirmation
3
Sample Qualification
4
Packaging & Label Approval
5
Production & Batch QC
6
Inspection & Shipment
Material Comparison Guide
| Material | Reinforcement / Behavior | Typical Print Condition | Material Difference | Typical Application Focus |
|---|---|---|---|---|
| PPS-GF | Glass-fiber reinforced PPS with a rigid, fiber-textured engineering finish | High-temperature hotend, wear-resistant nozzle and controlled thermal environment | Light-color reinforced PPS option without carbon-fiber appearance | Duct fittings, shaft supports, rigid fixtures and industrial brackets |
| PPS-CF | Carbon-fiber reinforced PPS with dark carbon-filled surface | High-temperature hotend, wear-resistant nozzle and controlled thermal environment | Higher carbon content changes appearance and can change electrical behavior by formulation | Rigid tooling, brackets and high-temperature structural parts |
| Unfilled PPS | Unreinforced semi-crystalline PPS | High-temperature hotend and careful thermal control | No fiber abrasion; mechanical and shrinkage behavior differ from reinforced PPS | Chemical-resistant functional parts and high-temperature components |
| PA-CF | Carbon-fiber reinforced nylon | Lower processing temperature than PPS; dry handling and wear-resistant nozzle required | More moisture-sensitive nylon matrix and a different temperature/chemical profile | Jigs, fixtures, brackets and general engineering components |
Technical Specifications
| Product Name | SSSray PPS-GF in Natural Ivory: Reinforced PPS 3D Printing Filament – filament PPS renforcé fibre de verre for Flanged Duct Elbows & Shaft Support Brackets |
|---|---|
| Material | Polyphenylene Sulfide (PPS) reinforced with glass fiber; semi-crystalline engineering thermoplastic composite |
| Product Series | SSSray Engineering Composite Series |
| Color / Effect | Natural Ivory; light warm cream-ivory with a soft matte fiber-textured printed finish |
| Filament Diameter | 1.75mm standard; 2.85mm available on request |
| Tolerance | ±0.03mm |
| Net Weight | 1kg; 3kg and 5kg available on request |
| Gross Weight | 1.3kg |
| Spool Type | Plastic spool |
| Packaging | Vacuum sealed with desiccant |
| Recommended Nozzle | Wear-resistant nozzle; hardened steel 0.6mm preferred, 0.4mm minimum starting point |
| Printer Requirement | Open-material high-temperature FDM/FFF printer with an all-metal hotend capable of the required PPS-GF process window |
| Typical Applications | Flanged duct elbows, internal guide vanes, split-clamp shaft supports, gusseted mounting arms, fixtures and industrial support components |
| OEM / ODM | Supported for custom labels, cartons, private-label programs and project packaging |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | 320–340°C |
| Usable Nozzle Range | 310–350°C for process tuning within the printer and hotend limits |
| Recommended Bed Temperature | 90–110°C |
| Usable Bed Range | 80–120°C depending on build surface, part footprint and chamber condition |
| Recommended Print Speed | 40–100 mm/s |
| Usable Speed Range | 30–150 mm/s after extrusion flow, layer bonding and dimensional tuning |
| Retraction – Direct Drive | 1–3mm at 20–40 mm/s starting range |
| Retraction – Bowden | 3–5mm at 20–40 mm/s on a stable high-temperature filament path |
| Layer Height | 0.20–0.30mm preferred with a 0.6mm nozzle; adjust to nozzle diameter and surface requirement |
| Cooling Fan | 0–10%; start with fan OFF and add only the cooling required for small features or geometry control |
| Wall Count | 3–5 perimeters for duct fittings, clamps and structural bracket work |
| Infill | 20–30% for general fixtures; 40–60% for higher-load mounting parts after part-level testing |
| First Layer Speed | 15–25 mm/s |
| Bed Adhesion | Smooth or textured PEI with a compatible high-temperature adhesive or release layer where required |
| Chamber | 50–70°C is a practical starting range for larger or high-infill parts when active chamber heating is available |
| Drying | 100°C for 8–10 hours after moisture exposure; use a heat-safe reel or respool before high-temperature drying where required |
| During Printing | Dry-box feeding with fresh desiccant is recommended for long engineering prints |
Print Optimization Guide
| Production Focus | SSSray Setup Guidance |
|---|---|
| Nozzle Wear | Glass fiber is abrasive. Use hardened steel, carbide, ruby or another wear-resistant nozzle and monitor nozzle condition during repeat production. |
| Dry Filament Path | Keep the spool sealed before use and feed from dry storage during long prints to maintain consistent extrusion and surface quality. |
| Flange Flatness | Use a stable chamber, controlled first layer and suitable build-surface preparation for broad flange footprints. |
| Guide Vane Definition | Use moderate outer-wall speed and minimal cooling to keep internal vane edges and wall junctions clean. |
| Bolt Holes & Clamp Fits | Run a short dimensional coupon first, then tune XY compensation around the actual fastener and shaft fit. |
| Gussets & Load Paths | Orient continuous perimeter paths through ribs and gussets so the printed structure follows the intended load path. |
| Large Components | Keep the enclosure thermally stable across long walls, thick sections and high-infill parts to reduce thermal gradients. |
SSSray Starting Settings for High-Temperature Printer Platforms
| Printer / Configuration | Nozzle | Bed | Chamber | Speed | SSSray Setup Guidance |
|---|---|---|---|---|---|
| Bambu Lab H2D | 330°C | 100°C | 60°C | 50–80 mm/s | Use a hardened 0.6mm nozzle for PPS-GF qualification; start with cooling off and tune flow before increasing speed. |
| Prusa CORE One L+ with HT Hotend | 335°C | 100°C | 60°C | 45–80 mm/s | Use the high-temperature hotend configuration and an abrasion-resistant nozzle; tune first-layer adhesion for the selected PEI surface. |
| Prusa Pro HT90 | 335°C | 105°C | 65°C | 40–70 mm/s | Use the high-temperature printhead and wear-resistant nozzle, then tune flow and chamber conditions around the production geometry. |
| Creality K2 Plus | 330°C | 100°C | 60°C | 50–80 mm/s | Use the hardened-nozzle configuration and active chamber heating; confirm extrusion flow on a short PPS-GF test before increasing speed. |
Use these SSSray starting settings to establish the first PPS-GF profile, then fine-tune flow, first-layer adhesion and dimensional compensation around the actual nozzle, build surface and production part.
Performance Characteristics
| Characteristic | Material / Process Behavior | Production Relevance |
|---|---|---|
| Thermal Processing | High-temperature PPS-GF process window with a 310–350°C tuning range | Designed for true high-temperature FDM/FFF equipment rather than conventional desktop profiles |
| Glass-Fiber Reinforcement | Reinforcement increases nozzle abrasion while supporting stiffness and dimensional control | Useful for rigid flanges, clamp bodies, ribs, gussets and mounting structures |
| Moisture Behavior | PPS has lower moisture uptake than many nylon-family materials, while dry processing still improves extrusion consistency | Supports more stable storage and production handling for engineering filament programs |
| Chemical Environment | The PPS material family is widely selected for demanding chemical and solvent environments | Useful for industrial ducting, fixtures and chemically exposed support parts after media-specific material selection |
| Surface Appearance | Natural Ivory matte surface with fine glass-fiber texture and subtle diffuse highlights | Provides a clean light engineering finish clearly differentiated from PPS-CF and dark reinforced grades |
| Production Tooling | Wear-resistant nozzle and controlled thermal conditions are part of the standard PPS-GF process setup | Supports repeatable qualification and batch production on suitable high-temperature equipment |
Applications
| Application Focus | Practical Notes |
|---|---|
| Flanged Duct Elbows | Use PPS-GF for rigid flow-path geometry where flange flatness, bolt-hole definition and temperature exposure are important to the assembly. |
| Internal Guide Vanes | The reinforced matrix supports clean vane junctions and controlled internal flow-path geometry when wall placement and cooling are properly tuned. |
| Split-Clamp Shaft Supports | Useful for rigid clamp bodies and mounting structures where shaft fit, bolt preload and dimensional repeatability matter. |
| Gusseted Mounting Arms | Well suited to bracket designs using ribs and gussets to distribute loads through reinforced printed geometry. |
| Industrial Jigs & Fixtures | Suitable for fixtures exposed to higher process temperatures or aggressive environments than mainstream desktop plastics. |
| Flow-Path Components | Suitable for non-pressure industrial flow-path components after matching operating temperature, media and mechanical requirements to the final part design. |
| Equipment Support Parts | Useful for machine-side supports, mounting blocks and low-volume replacement parts where rigidity and heat resistance are key material-selection factors. |
Storage Guide
- Keep unopened PPS-GF spools in the original vacuum-sealed bag until qualification or production use
- After opening, return the spool to a sealed dry box with fresh desiccant
- Feed directly from dry storage during long engineering prints where practical
- If moisture exposure occurs, dry at the recommended temperature using a heat-safe reel or respool arrangement
- Keep the filament path free from dust, oil and workshop contamination before high-temperature extrusion
OEM / ODM Services
We supply PPS-GF OEM / ODM orders for distributors, industrial resellers, private-label brands and engineering sourcing teams. Available options include neutral packaging, custom labels, branded cartons, barcode and SKU layouts, project-based color options, private-label packaging and sample qualification before volume production.
MOQ Reference: Neutral packaging starts from 50 spools. OEM packaging programs typically start from 500–1,000 spools depending on label, carton and customization requirements.
Quality Control for Repeat B2B Supply
- 1.75mm filament diameter and ±0.03mm tolerance control
- Natural Ivory color and visible surface consistency inspection
- Winding and spool-condition inspection before final packing
- Vacuum-seal and desiccant inclusion check
- Batch identification for repeat-order follow-up
- Final packaging, label and shipment-preparation review before dispatch
Technical Documents & Qualification Support
| Support Item | What We Provide |
|---|---|
| PPS-GF TDS | Current PPS-GF technical data documentation is available through the SSSray technical document center |
| PPS-GF SDS / MSDS | Safety documentation is available for purchasing, shipping and material-file requirements |
| Sample Qualification | Verified B2B buyers can qualify material, color and printer setup before committing to a bulk order |
| Test Protocol Support | Our qualification workflow helps buyers align incoming samples and repeat production around the same key checks |
| Batch QC Support | Batch identification and QC records support repeat-order follow-up and supplier qualification programs |
| Order Documentation | We match the available technical, compliance and shipment document set to the confirmed SKU, destination and purchasing requirement before order release |
Frequently Asked Questions
What is the MOQ for Natural Ivory PPS-GF?
Neutral packaging starts from 50 spools. OEM packaging typically starts from 500–1,000 spools depending on label, carton and packaging requirements.
What print settings should we use first?
Start at 320–340°C nozzle temperature, 90–110°C bed temperature and 40–100 mm/s. Use a wear-resistant 0.6mm nozzle where practical, keep cooling at 0–10%, and use stable enclosure temperature for larger parts.
Can PPS-GF be printed on a normal desktop printer?
Use a high-temperature open-material FDM/FFF printer with an all-metal hotend capable of the PPS-GF temperature range. A wear-resistant nozzle and controlled enclosure are strongly recommended.
Why do you recommend a wear-resistant nozzle?
Glass fiber is abrasive. Hardened steel, carbide, ruby or another wear-resistant nozzle helps maintain nozzle geometry during sample testing and repeat production.
What makes Natural Ivory different from beige PPS-GF colors?
Natural Ivory is the palest shade in this PPS-GF line. It has a light warm cream appearance and is clearly lighter and less yellow-brown than Natural Sand Beige or Desert Tan, while retaining the characteristic fine matte fiber texture.
Can we request samples before a bulk order?
Yes. Verified B2B buyers can apply for up to three complimentary sample spools for material, color and printer qualification before volume purchasing.
Can SSSray supply private-label PPS-GF?
Yes. We support custom labels, branded cartons, barcode and SKU layouts, private-label packaging and project-based OEM / ODM programs.
What is the standard lead time?
Standard orders are typically 7–15 days. Customized orders are typically 15–25 days depending on packaging, specification and production requirements.
Source Natural Ivory PPS-GF for Your Next Engineering Program
Send us your target part, printer platform, operating environment and annual purchasing volume. Our team can arrange PPS-GF sample qualification, bulk pricing, packaging and OEM / ODM supply for your duct fittings, shaft supports and other reinforced engineering parts.