Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM

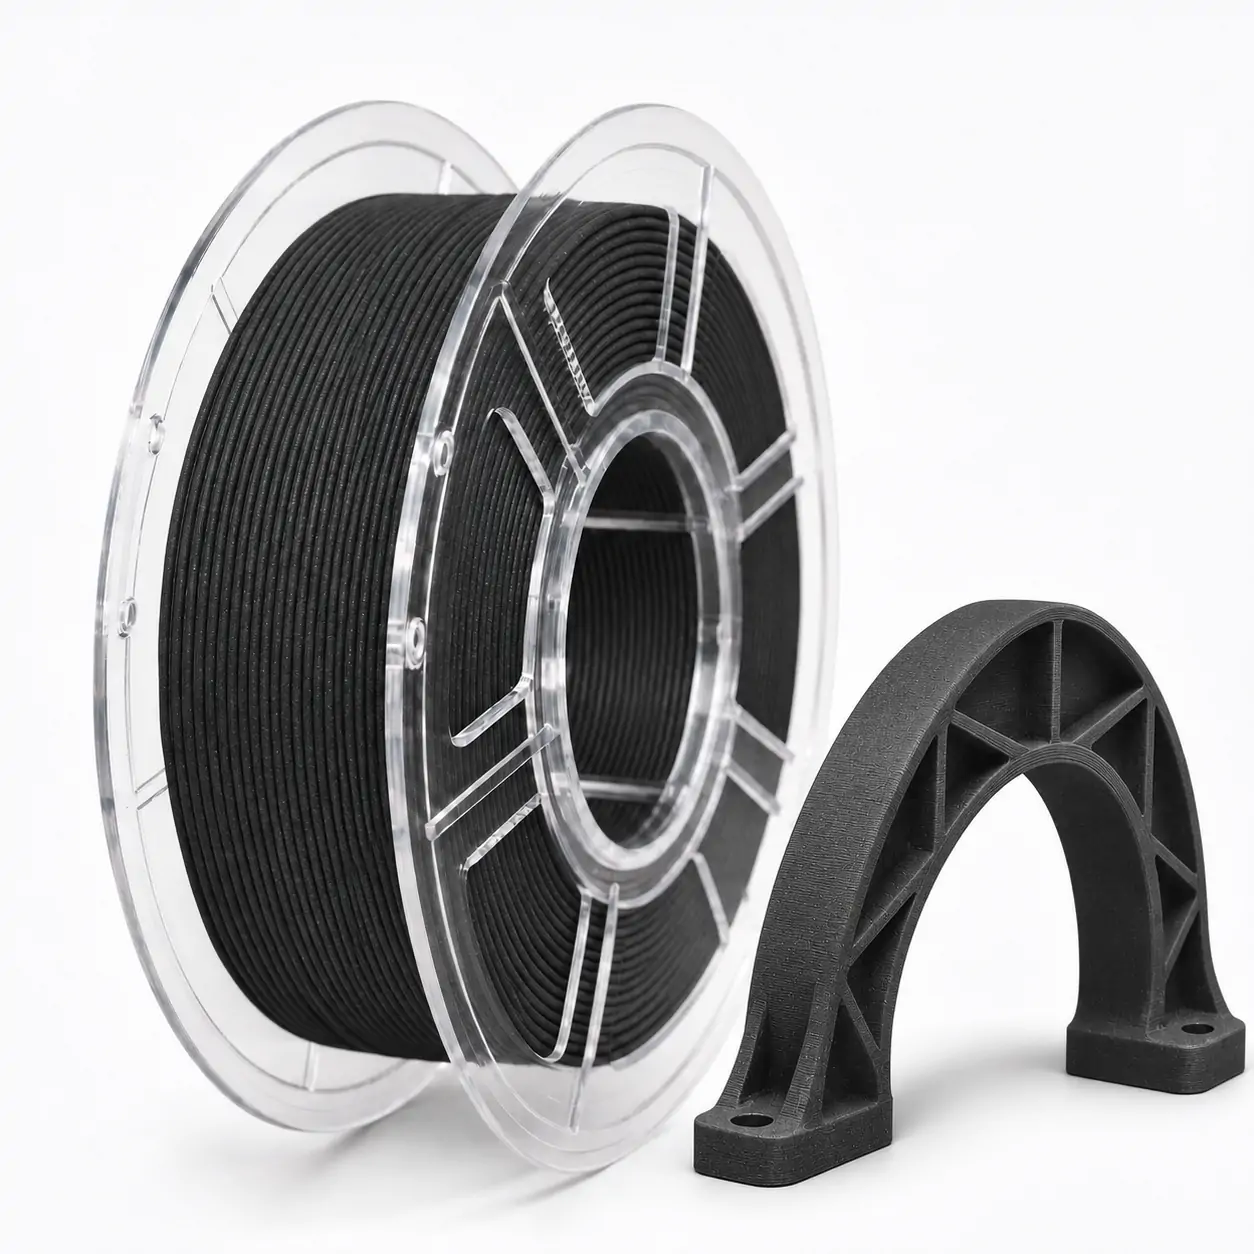
PA12-CF Functional Parts Series | 25% Carbon Fiber | Industrial OEM / ODM
SSSray Matte Black Nylon 12 3D Printer Filament for Mounting Frames – PA12-CF 25% Carbon Fiber, 1.75mm (filamen nilon gentian karbon)
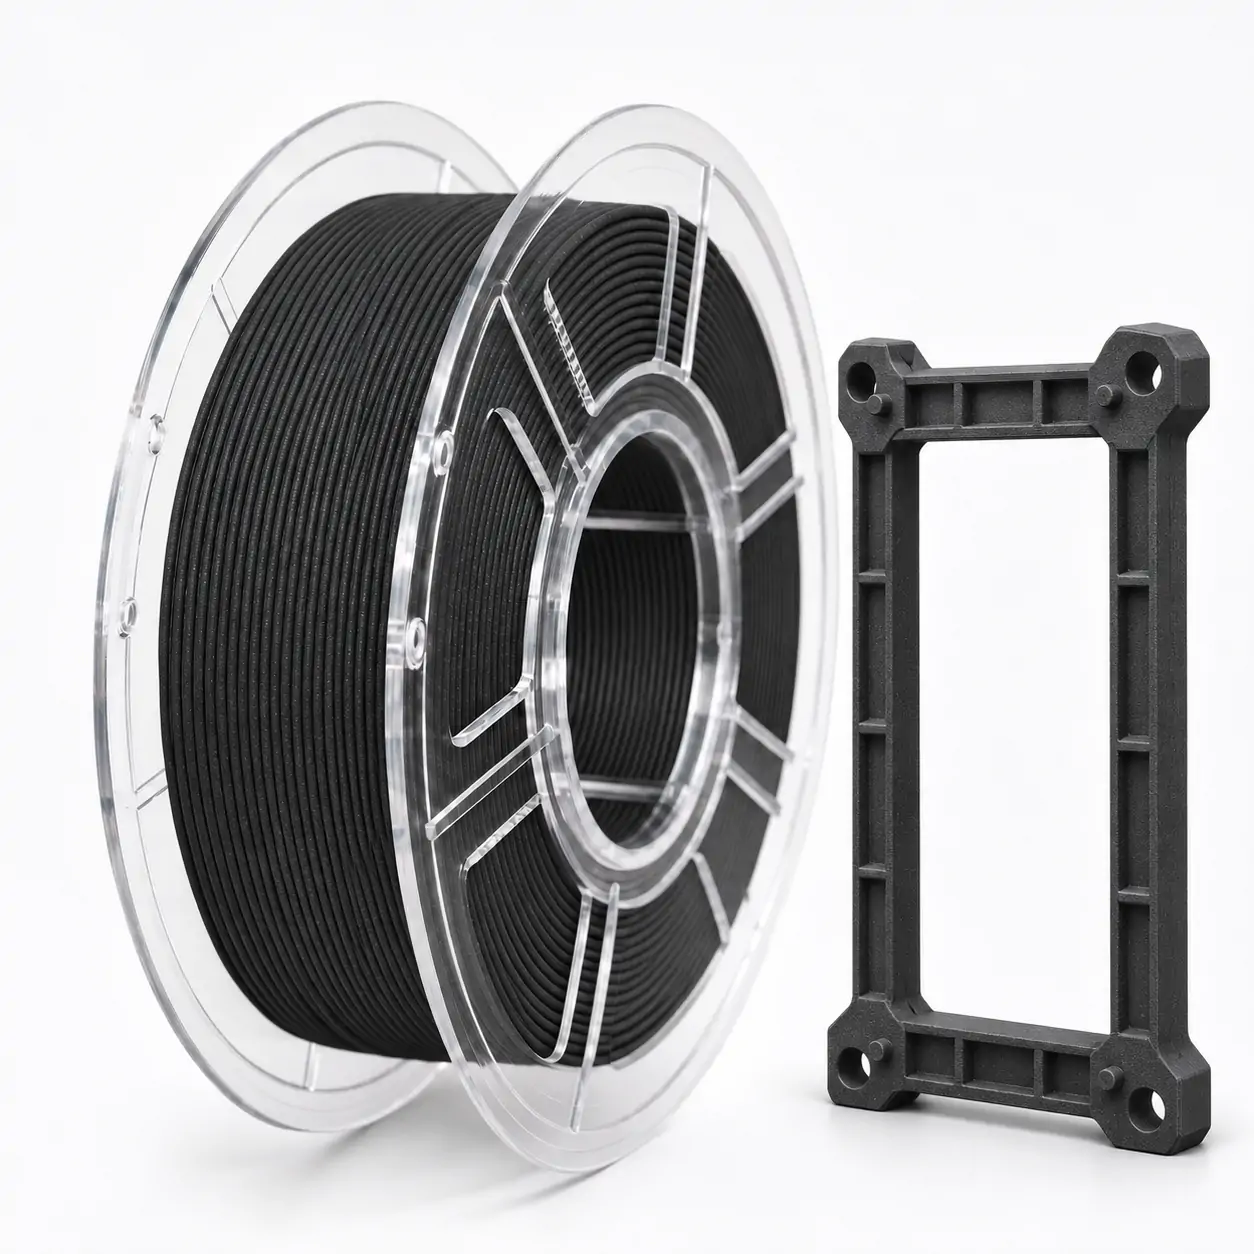
Print rigid mounting frames, radial ribs and precision fixtures with our custom 25% carbon-fiber-reinforced Nylon 12 filament in a deep, low-sheen matte black finish.
We manufacture this high-fiber PA12 grade for industrial FDM parts where defined mounting geometry, stable feed and a clean technical appearance matter. SSSray combines 1.75mm ±0.03mm diameter control, consistent winding, vacuum packing and export-ready OEM supply to support your engineering-material portfolio.
MaterialPA12-CF, 25% CF
SeriesPA12-CF Functional Parts
Color EffectMatte Black / Opaque
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp270–290°C recommended
Bed Temp70–90°C recommended
Print Speed40–90 mm/s recommended
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; semi-custom logo labels from 300 spools; fully custom packaging from 1,000 spools.
Lead Time: Standard 7–15 days; customized orders typically 15–25 days.
Product Overview
We manufacture SSSray PA12-CF 25% Matte Black for industrial buyers producing rigid mounting frames, ribbed supports and assembly fixtures. Its Nylon 12 matrix and 25% carbon-fiber reinforcement give designers a stiffness-focused material for precise, functional FDM/FFF geometry. The filament produces deep neutral black parts with subtle charcoal undertones, an opaque, finely textured matte surface and no metallic sparkle. This low-sheen finish complements radial ribs, mounting flanges, rectangular brackets and camera supports while maintaining a consistent industrial appearance across visible assemblies.
Our standard 1.75mm filament is controlled to ±0.03mm and supplied on a 1kg net plastic spool, vacuum sealed with desiccant. For continuous production, we recommend a hardened 0.6mm nozzle, a high-temperature all-metal hotend and dry-filament feeding. SSSray supports neutral orders from 50 spools, semi-custom logo labels from 300 spools and fully custom packaging from 1,000 spools, including barcodes, export cartons and replenishment planning. Send us your mounting-frame drawings, printer configuration and purchasing forecast; our team will prepare a focused sample and bulk supply proposal.
Why This Product Stands Out
We engineer our proprietary 25% carbon-fiber PA12 for rigid radial-rib mounting frames, broad support flanges and repeatedly fastened fixtures. Carbon-fiber reinforcement supports high stiffness and reduced thermal dimensional change compared with unfilled PA12, while the Nylon 12 matrix offers lower moisture sensitivity than conventional PA6-based nylon. We pair the refined charcoal-black matte finish with 1.75mm ±0.03mm diameter control, practical hardened 0.6mm nozzle guidance and moisture-protected 1kg spools for dependable factory-direct supply.
Key Selling Points
Stable Diameter Control
Our 1.75 ±0.03mm diameter specification supports consistent feeding, defined material input and repeat-order production.
Smooth Extrusion
Our evenly wound, moisture-protected PA12-CF supports smooth extrusion through narrow frame walls and densely ribbed geometry when printed with a hardened hotend.
Functional Matte Black Finish
Opaque charcoal-black, low-sheen surfaces suit visible brackets, machine fixtures and technical housings.
25% Carbon-Fiber Reinforcement
A 25% carbon-fiber formulation gives your engineering portfolio a dedicated high-reinforcement choice for rigid mounting hardware and structural ribs.
Export-Oriented Supply
1kg moisture-protected spools, private labels and shipping coordination support industrial distributor programs.
OEM / ODM Ready
Choose neutral boxes, custom logo labels, branded cartons and project-based color or spool discussions.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| PA12 Matrix + 25% Carbon Fiber | Specify a stiffness-oriented composite for mounting frames, ribs and industrial fixtures |
| Matte Black, Opaque Finish | Create a consistent dark visual language for functional parts and private-label product lines |
| 1.75mm / ±0.03mm | Support reliable spool-to-spool feeding and predictable extrusion setup across repeat orders |
| Hardened 0.6mm Nozzle Workflow | Accommodate abrasive fiber-filled feedstock and reduce restrictions caused by smaller orifices |
| Vacuum Bag + Desiccant | Support moisture control throughout storage and international freight |
| 50-Spool Neutral MOQ / OEM Options | Introduce a specialized 25% CF nylon line with a practical entry quantity and scalable private-label packaging |
Balanced Quality and Cost Efficiency
SSSray brings high-reinforcement Nylon 12 into your supply program with a clear commercial advantage: one factory-direct source for 1kg industrial spools, 50-spool neutral orders and OEM packaging at scale. For print farms and machine shops, on-demand frames and fixtures can streamline low-volume component sourcing and reduce inventories of application-specific brackets. For distributors, our distinctive matte black 25% CF grade creates a focused engineering-material offer backed by consistent packaging, repeat-order planning and responsive technical support. Share your volume forecast to receive a tailored bulk quotation.
How We Work
1
Requirement Review
2
Specification Confirmation
3
Sample Evaluation
4
Packaging Discussion
5
Production Scheduling
6
Inspection & Shipment
Material Comparison Guide
| Material | Reinforcement / Behavior | Print Hardware | Moisture / Heat Workflow | Typical Use |
|---|---|---|---|---|
| PA12-CF 25% | Carbon-filled nylon; stiffness-oriented, abrasive, matte | High-temperature all-metal hotend; hardened nozzle | Pre-dry and print from dry storage; warping depends on geometry | Mounting frames, ribs, jigs, fixtures |
| Unfilled PA12 | Unreinforced nylon; higher flexibility than typical CF-filled grades | Nylon-capable hotend; wear-resistant nozzle generally not required for filler | Pre-dry; heated bed and adhesion control | Clips, compliant components, impact-loaded housings |
| PETG-CF | Carbon-filled PETG; lower print temperature than PA12-CF | Abrasion-resistant nozzle; PETG temperature platform | Dry before printing; moderate bed heat | Brackets and appearance-focused functional parts |
| PA6-CF | Carbon-filled Nylon 6; moisture and thermal behavior differs by grade | High-temperature hotend; hardened nozzle | Rigorous drying; controlled chamber is often helpful | Industrial tools and high-stiffness structural geometries |
Technical Specifications
| Product Name | SSSray Matte Black Nylon 12 3D Printer Filament for Mounting Frames – PA12-CF 25% Carbon Fiber, 1.75mm (filamen nilon gentian karbon) |
|---|---|
| Material | PA12 (Nylon 12) reinforced with 25 wt% carbon fiber |
| Series | PA12-CF Functional Parts Series – 25% Carbon Fiber |
| Color / Effect | Deep matte black; subtle charcoal undertones; opaque, non-metallic, fine-textured |
| Filament Diameter | 1.75mm standard; 2.85mm subject to manufacturing confirmation |
| Tolerance | ±0.03mm |
| Net Weight | 1kg (2.2 lbs); 3kg / 5kg customized on inquiry |
| Gross Weight | 1.3kg |
| Spool Type | Plastic spool |
| Packaging | Vacuum sealed with desiccant |
| Recommended Nozzle | 0.6mm hardened steel or equivalent abrasion-resistant nozzle |
| Printer Compatibility | 1.75mm FDM/FFF printers with 290°C-class all-metal hotends, suitable beds, hardened extrusion path and dry-feed capability |
| Typical Applications | Mounting frames, radial ribs, support brackets, assembly fixtures, custom jigs and industrial housings |
| OEM / ODM | Supported |
| Technical Documentation | Our export team coordinates grade-matched specification, safety and market-entry documentation for custom PA12-CF 25% orders. |
Recommended Print Settings
| Parameter | Recommended Settings / Usable Range |
|---|---|
| Recommended Nozzle Temperature | 270–290°C for reinforced-nylon printing with a hardened 0.6mm nozzle |
| Usable Nozzle Range | 260–300°C on compatible high-temperature hotends; select the setting for your extrusion volume and part geometry |
| Recommended Bed Temperature | 70–90°C with a nylon-compatible adhesion layer |
| Usable Bed Range | 60–100°C with appropriate build surface and enclosure conditions |
| Recommended Print Speed | 40–90 mm/s for mounting frames, brackets and functional fixtures |
| Usable Speed Range | 30–120 mm/s; use the upper range with a high-flow hotend, dry feed and suitable part geometry |
| Layer Height | 0.20–0.30mm with a 0.6mm hardened nozzle; 0.15–0.25mm with a tested 0.4mm nozzle |
| Cooling Fan | 0% on first layers; 0–15% for main walls, with targeted bridge cooling |
| Retraction – Direct Drive | 0.6–1.2mm at 20–30 mm/s; fine-tune to the hotend and feed path |
| Retraction – Bowden | 2–4mm at 20–30 mm/s; maintain a smooth feed path for stiff CF-filled filament |
| Wall Count | 3–5 walls for mounting frames; increase locally around fasteners |
| Infill | 20–30% for fit-check fixtures / 40–60% for stiffness-prioritized mounting structures |
| First Layer Speed | 15–25 mm/s |
| Bed Adhesion | PA-compatible adhesive on suitable PEI or engineering build surface; use a brim for long, thin sections |
| Drying Before Printing | 80°C for 8–12 h; use a temperature-rated spool and dryer or transfer filament to a heat-rated spool |
| Printing Environment | Enclosed, stable-temperature printer preferred for larger frames; feed from an actively dry container |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Ribbed Mounting Frames | Align ribs with principal loads and avoid sharp rib-to-wall transitions; add fillets to reduce stress concentrations |
| Hole & Fastener Accuracy | Calibrate holes and bosses on a coupon before printing a full fixture; use inserts or washers where load demands |
| Matte Surface Finish | Run consistent outer-wall speed and keep the seam away from visible assembly surfaces |
| Bed Adhesion | Use a compatible release/adhesion agent; add a 5–10mm brim on narrow feet and long rectangular frames |
| Moisture & Extrusion | Dry before printing; popping, bubbles, fuzzy walls and weak bonds indicate that the feedstock needs attention |
| Fibers & Feed Path | Use a hardened 0.6mm nozzle, smooth low-curvature routing and a dry box; inspect drive gears during long runs |
| Functional Qualification | Check XY/Z orientation, bolt torque, creep and service-temperature exposure on representative printed specimens |
Printer Brand Starting Settings
| Printer Brand | Nozzle | Bed | Speed | Notes |
|---|---|---|---|---|
| Bambu Lab X1 Carbon | 275–290°C | 80–100°C | 40–90 mm/s | Hardened 0.6mm nozzle, dry external feed and PA-compatible plate adhesive |
| Prusa CORE One L+ | 270–285°C | 75–90°C | 35–70 mm/s | Abrasion-resistant nozzle and enclosed print environment; standard hotend ceiling is 290°C |
| Creality K1C | 270–285°C | 80–95°C | 40–85 mm/s | High-temperature hotend, wear-resistant nozzle and a bed setting no higher than 100°C |
| Creality K1 Max | 270–285°C | 80–95°C | 40–90 mm/s | Hardened nozzle and abrasion-resistant drive path; bed setting no higher than 100°C |
| Raise3D E2CF | 270–290°C | 75–90°C | 40–80 mm/s | Carbon-fiber-ready extrusion system, hardened 0.6mm nozzle and dry-filament feed |
We recommend dry feeding, a hardened nozzle and material-specific flow calibration for consistent frame geometry. Keep nozzle and bed temperatures within the limits of your actual printer configuration.
Performance Characteristics
| Characteristic | Material / Production Reference | Practical Interpretation |
|---|---|---|
| Fiber Reinforcement | Custom 25% carbon fiber PA12 formulation | Suited to stiffness-oriented frame ribs, bolt bosses and rigid mounting geometry |
| Surface Appearance | Deep matte black / opaque / low-sheen | Good for exposed radial ribs, black brackets and fixture assemblies |
| Diameter Control | 1.75mm ±0.03mm specified tolerance | Useful for incoming lot checks and extrusion setup records |
| Moisture Response | Hygroscopic nylon composite | Pre-dry and feed dry to limit bubbles and inconsistent weld lines |
| Nozzle Wear | Abrasive carbon-fiber filler; hardened 0.6mm nozzle recommended | Plan maintenance and wear-resistant spares for production runs |
| Frame Design Guidance | Reinforced ribs, local wall count and print orientation | Our technical team helps you align mounting-frame geometry with the printing process and intended assembly |
Applications
| Application Focus | Printed-Part Design Focus | Practical Notes |
|---|---|---|
| Radial-Rib Mounting Frames | Rib-to-hub transitions and bolt bosses | Print orientation and local wall count affect joint strength; test assembly loads |
| Rectangular Support Frames | Long spans, corner stiffness and flat seating faces | Add corner fillets and brim support to improve edge hold and frame geometry |
| Assembly Jigs & Inspection Fixtures | Repeatable geometry and fixture mounting | Validate fit and repeatability over actual shop conditions |
| Robotics & Camera Mounts | Stiffness-to-weight and vibration exposure | Use reinforcement in load paths and check fatigue-sensitive connections |
| Industrial Equipment Housings | Opaque matte appearance and mounting features | Verify temperatures, chemical exposure and clearance requirements before use |
Storage Guide
- Keep sealed stock dry, away from sunlight and prolonged high-humidity exposure.
- Dry before production at 80°C for 8–12 hours using a heat-rated spool and dryer.
- During printing, feed from a dry box or conditioned enclosure; monitor for popping, stringing and bubbles.
- After every run, reseal promptly with fresh desiccant and label the opened lot for traceability.
- Avoid tight feed-path bends and high-heat storage; CF-filled nylon is stiff and plastic spool heat tolerance must be checked.
OEM / ODM Services
We manufacture custom PA12-CF 25% for industrial filament distributors and private-label importers who want a differentiated high-reinforcement nylon line. Choose neutral packaging, custom logo labels, branded boxes, export carton identification, barcodes, tailored spool formats or project-based color matching. Our team handles sample spools, diameter specifications, printer guidance and packaging artwork directly with your purchasing department.
MOQ Reference: Neutral packaging from 50 spools; semi-custom logo labels from 300 spools; fully custom packaging from 1,000 spools. Custom 2.85mm, 3kg and 5kg formats require a feasibility and production-quantity review.
Quality Control
- Incoming PA12 and carbon-fiber feedstock identity and formulation control
- 1.75mm / ±0.03mm diameter and ovality inspection checkpoints
- Spool winding tension, flange clearance and visible strand condition review
- Lot-linked extrusion setup and sample-print check of surface and feeding behavior
- Vacuum bag seal, desiccant inclusion and packaging label verification
- Final carton count, order traceability and shipping-document review
Technical Documents & Compliance Support
- Custom-grade specifications: We coordinate the dimensional, handling and processing information required for your PA12-CF 25% purchasing program.
- Safety documentation: Our team prepares the SDS documentation scope for the agreed custom formulation and destination market.
- RoHS / REACH support: We coordinate market-specific material testing and documentation requests within the agreed project scope.
- Third-party testing: We support customer-defined laboratory methods and reporting arrangements for custom engineering grades.
- Export documentation: Send your import-market checklist with the inquiry; we organize the applicable technical and shipping documents alongside your order.
Frequently Asked Questions
What is the MOQ for PA12-CF 25% in matte black?
We accept neutral-packaging programs from 50 spools. Semi-custom packaging with your logo labels starts at 300 spools, while fully custom branded packaging starts at 1,000 spools. We confirm the final specification against your artwork, spool and carton requirements.
Which printers can run this 25% carbon-fiber nylon?
Use a 1.75mm FDM printer with a 290°C-class all-metal hotend, an abrasion-resistant nozzle, a nylon-compatible build surface and a dry-feed arrangement. Suitable hardware configurations include Bambu Lab X1 Carbon, Prusa CORE One L+, Creality K1C and Raise3D E2CF. Confirm your machine’s actual hardware limits and profile first.
Is PA12-CF 25% appropriate for mounting frames and ribbed brackets?
Yes, these are our target applications. Focus on rib orientation, bolt-hole design, wall thickness and stress concentrations. Before using a printed mount in a safety-relevant or sustained-load assembly, validate strength, creep and operating temperature on the finished geometry.
Can you supply our branding or a different spool format?
Yes. We support neutral cartons, custom logo labels, branded boxes, barcode layouts and project-based spool options. The standard unit is 1kg on a plastic spool; 3kg, 5kg and 2.85mm requests go through production-feasibility review.
Can we test the material before placing a bulk order?
We offer paid sample orders of up to three spools for verified B2B buyers. Send us your printer model, nozzle size, frame dimensions and planned annual demand; our team will help you move from sample printing to repeat supply.
How does SSSray support technical qualification for this custom grade?
We formulate and print-test this proprietary PA12-CF 25% grade in-house. For qualified B2B projects, our technical team helps confirm purchasing specifications, printer settings and applicable safety and compliance documents while maintaining confidentiality of the custom formulation and internal test data.
How should we dry the filament and configure the print bed?
Dry at 80°C for 8–12 hours on a heat-rated spool and print directly from dry storage. Use a 70–90°C heated bed with a PA-compatible adhesion layer; adjust the build surface and brim to the frame’s footprint.
What lead time and payment terms do you offer?
Our standard orders have a 7–15 day lead time; customized orders run 15–25 days after order confirmation. Payment terms are T/T 30% deposit and 70% before shipment; PayPal is available for small trial orders. We quote EXW or FOB Ningbo.
Ready to Source PA12-CF 25% for Your Mounting-Frame Program?
Send our team your frame drawings, printer platform and estimated annual volume. We will prepare bulk pricing, sample options, private-label packaging and a shipment plan for your engineering-material program.



Related products
-

SSSray PETG-CF 3D Printer Filament – Carbon Fiber Filled PETG in Deep Spruce Green, zelený PETG filament s uhlíkovými vlákny for Functional Brackets & Fixtures
-
SSSray PLA-CF in Dusty Rose: 1.75mm Carbon Fiber PLA 3D Printer Filament – filament PLA fibre de carbone rose – for Motor Mounts & Finned Housings
-
Industrial Shock-Absorbing TPU Filament 1.75mm 1KG | High-Resilience Lattice-Grade Flexible Material for Protective Pads, Vibration Dampers & Robotics Grippers | OEM/ODM Bulk Supply
-
SSSray Olive Drab Green Matte PETG-CF, filamento PETG con fibra de carbono verde oliva – Carbon Fiber PETG 3D Printer Filament for Threaded Clamps & Latched Storage Boxes