Online time
Monday to Friday: 9AM - 8PM
Weekend: 10AM - 5PM
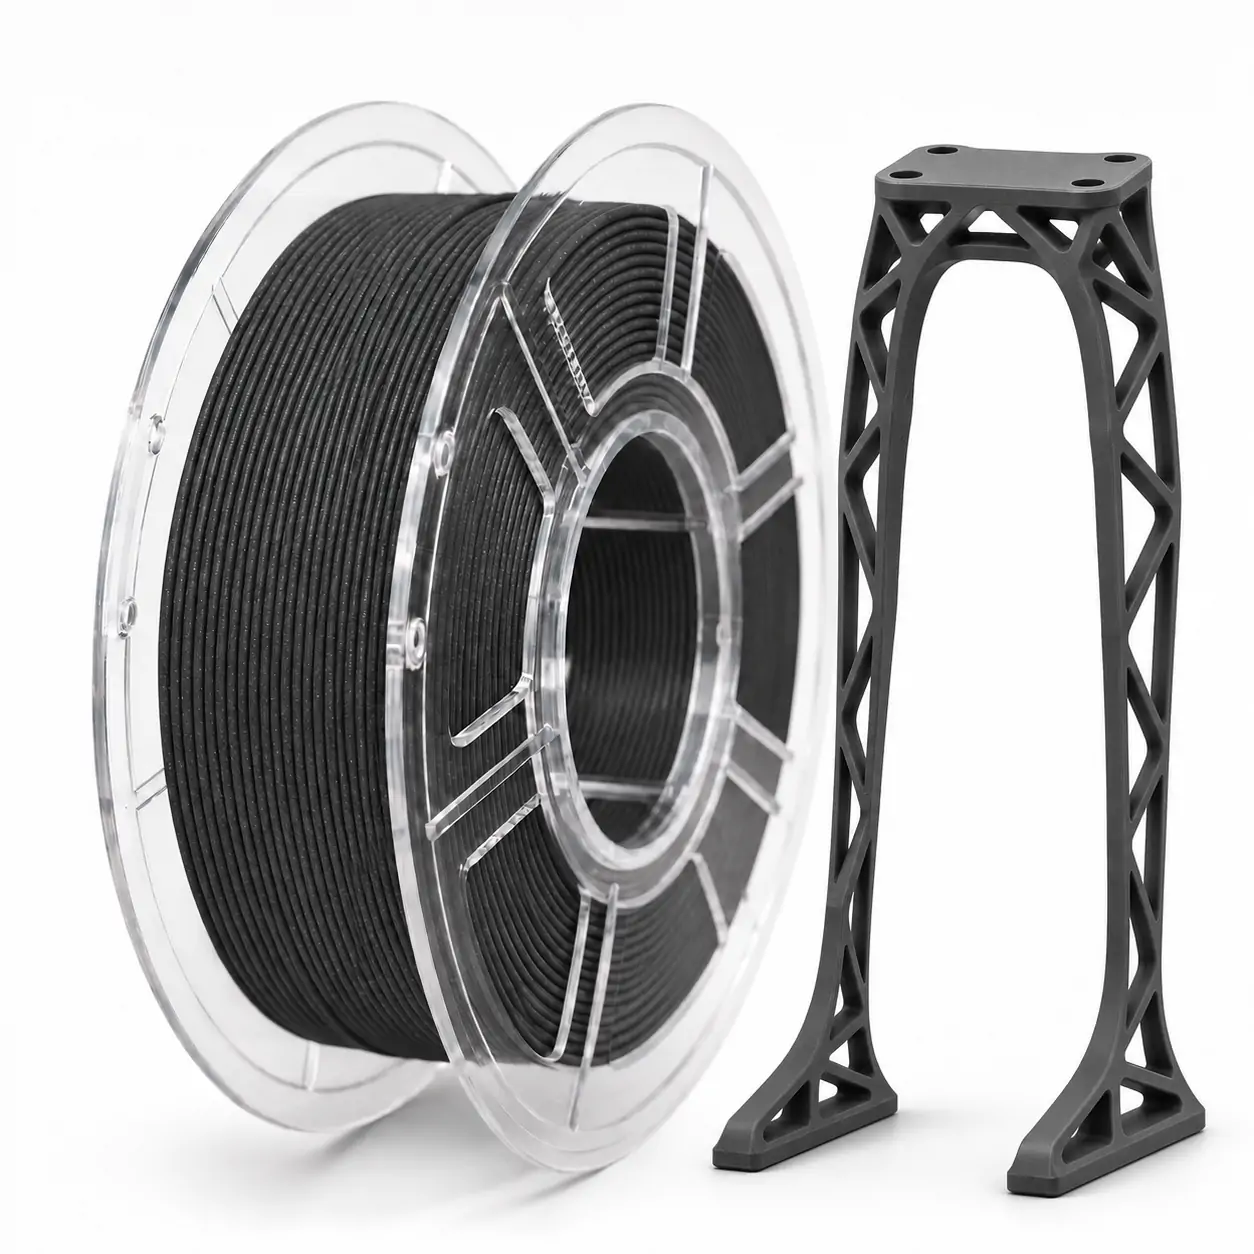
20% Carbon Fiber PA12 | Functional Parts Series | Bulk & OEM Supply
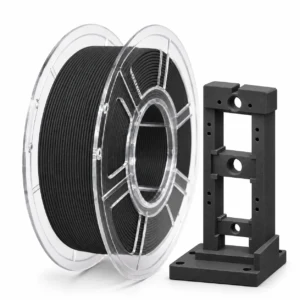
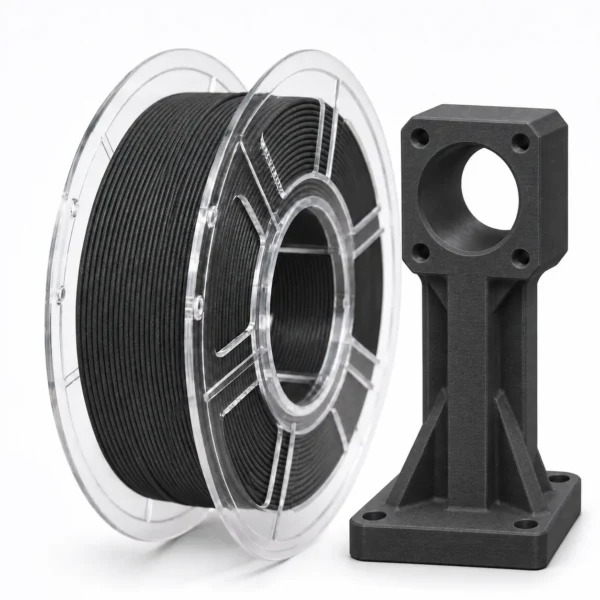
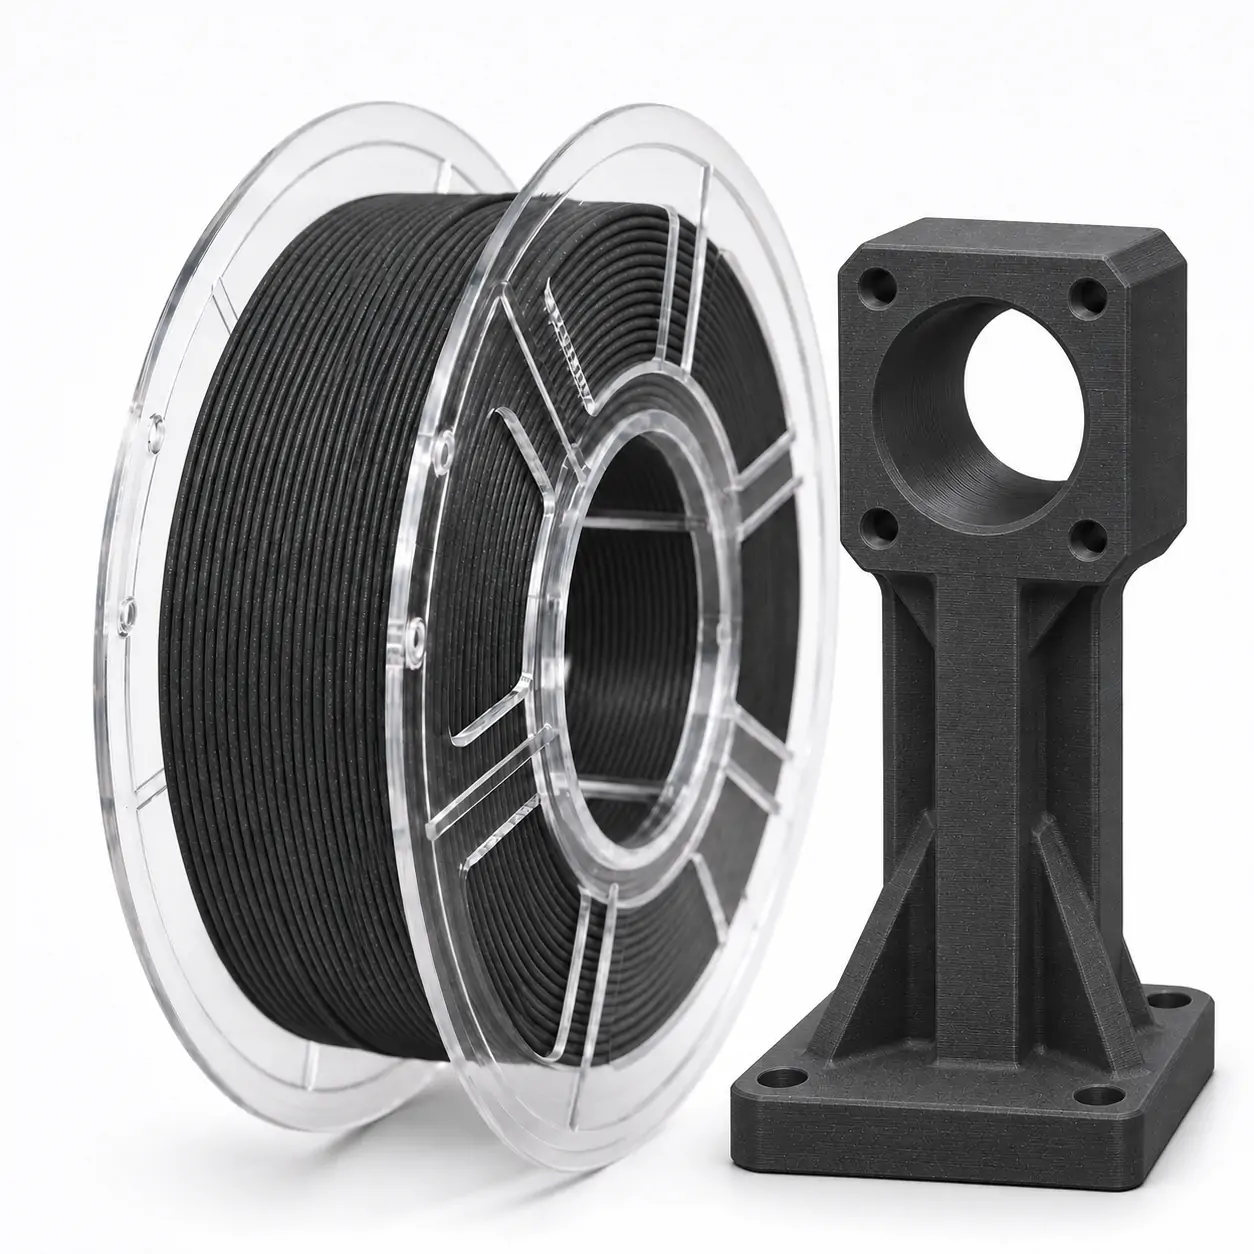
SSSray 20% Carbon Fiber PA12-CF Nylon 3D Printer Filament 1.75mm, Charcoal Black (filament PA12 z włóknem węglowym) for Lattice Supports & Mounts
Charcoal-black, matte 20% CF-reinforced PA12 nylon for engineered lattice supports, mounting brackets, tooling fixtures and private-label industrial filament ranges.
We produce this 20% carbon-fiber PA12 grade for buyers who need rigid lattice supports, secure mounting interfaces and a refined charcoal-black finish. Our 1.75mm ±0.03mm filament arrives vacuum sealed with desiccant; we coordinate engineering samples, scheduled wholesale supply and private-label packaging directly with your team.
MaterialPA12-CF / 20% CF
SeriesPA12-CF Functional Parts
Color EffectCharcoal Black / Matte
Diameter1.75mm
Tolerance±0.03mm
Net Weight1kg
Gross Weight1.3kg
Nozzle Temp260–280°C
Bed Temp60–80°C
Print Speed60–100 mm/s
PackagingVacuum + Desiccant
Spool TypePlastic Spool
MOQ: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools.
Lead Time: Standard 7–15 working days; customized orders typically 15–25 working days.
Product Overview
Our 20% Carbon Fiber PA12-CF filament brings nylon engineering capability to precision-built lattice supports, tooling mounts and load-aware functional components. Short carbon-fiber reinforcement is selected to increase stiffness and help control dimensional movement compared with unfilled nylon, while the PA12 base supports practical applications where low moisture uptake relative to many PA6 grades is valuable. The finish is a deep charcoal black with restrained graphite-gray undertones: opaque, finely textured and matte rather than shiny or metallic. That understated appearance suits robotics brackets, sensor mounts, machine fixtures and technical product ranges.
For industrial print farms, we recommend dry-box feeding, a hardened 0.6mm nozzle and an enclosed high-temperature printer. Start at 260–280°C nozzle, 60–80°C bed and 60–100 mm/s; our wider 40–120 mm/s tuning window lets capable machines balance throughput with dimensional detail. Build load paths along continuous extrusions, reinforce mounting holes with appropriate walls, and check bolt fit in the final assembly. For distributors and OEM brands, we deliver standard 1kg dry-packed plastic spools, repeat-order supply planning, private-label options and engineering sample support.
Why This Product Stands Out
We make this 20% carbon-fiber PA12 grade for engineering buyers who need more than a commodity black spool: stiff lattice members, rigid fixture arms, precise mounting faces and a professional charcoal-black matte finish. Our production team monitors filament diameter against the 1.75mm ±0.03mm specification, inspects winding quality and protects every 1kg spool with a vacuum seal and desiccant. We back that material program with practical 60–100 mm/s starting print settings, 50-spool neutral-pack orders and scalable private-label supply for repeat production.
Key Selling Points
Controlled 1.75mm Diameter
We supply 1.75mm filament to a stated ±0.03mm diameter tolerance for repeatable feeding and consistent slice profiles across wholesale replenishment orders.
Engineering-Grade Feed Setup
Our recommended 260–280°C melt window and 60–100 mm/s production profile help equipped print farms balance extrusion throughput, rib definition and functional surface quality.
Charcoal-Black Matte Finish
Deep opaque charcoal with subtle graphite undertones keeps lattice ribs and fixture surfaces looking purpose-built.
20% CF-Reinforced PA12
Our 20% CF-filled nylon is selected for rigidity-focused mounting brackets, triangulated lattice supports, inspection jigs and mechanically oriented product lines.
Bulk Supply for Engineering Buyers
Start with 50 neutral-pack spools, then plan repeat orders around our standard 10-spool export cartons and OEM volumes of 500–1,000 spools.
Private-Label Program Support
Build a technical nylon range with customized color requests, branded labels, packaging artwork and agreed qualification samples.
Key Features
| Feature | Practical Buyer Benefit |
|---|---|
| 20% Carbon Fiber in PA12 | Develops a clear rigidity-focused offer for triangulated supports, mounting brackets and fixture components |
| Charcoal-Black, Fine-Textured Matte | Delivers an understated industrial finish suited to visible functional parts |
| 1.75mm ±0.03mm | Supports repeatable material feeding and consistent slicer profiles across replenishment orders |
| 1kg Plastic Spool | Fits standard single-spool retail and industrial replenishment programs |
| Vacuum Seal + Desiccant | Helps protect nylon filament from humidity during storage and export transit |
| OEM / ODM Supply | Supports private labels, artwork, packaging options and contract orders |
Balanced Quality and Cost Efficiency
We help engineering distributors control landed cost without stripping value out of the material offer: neutral orders start at 50 spools, our standard export pack carries 10 individual 1kg units per carton, and a reference pallet holds 560 spools. That straightforward packing plan supports stocking forecasts, repeat-order logistics and private-label launches. Pair our Charcoal Black PA12-CF20 with other wholesale carbon-fiber grades and PA nylon materials to build a differentiated engineering portfolio rather than competing on price alone.
How We Work
1
Requirement Review
2
Specification Confirmation
3
Sample Evaluation
4
Packaging Discussion
5
Production Scheduling
6
Inspection & Shipment
Material Comparison Guide
| Material | Material Behavior | Typical Print Conditions | Selection Consideration | Typical Use |
|---|---|---|---|---|
| PA12-CF 20% | Carbon-fiber-filled PA12; increased rigidity, lower ductility than unfilled PA12 | 260–280°C nozzle; heated bed; dry filament; hardened nozzle | Abrasive; validate layer-direction strength and fit | Lattice supports, mounts, jigs and industrial brackets |
| Unfilled PA12 | More ductile nylon behavior, without fiber reinforcement | High-temperature hotend; dry filament; adhesion control | Greater flexibility for snap-fit or impact-oriented design | Flexible brackets, clips and wear parts |
| PA6-CF | Fiber-reinforced PA6 with grade-dependent stiffness and moisture uptake | High-temperature hotend; strict drying; enclosure preferred | Compare moisture conditioning and thermal performance by grade | Tooling, fixtures and mechanical prototypes |
| PETG-CF | Carbon-filled PETG with surface and stiffness changes by formulation | Generally lower nozzle temperatures than PA12-CF; hardened nozzle | Lower-temperature alternative for less demanding thermal use | Housings, brackets and display fixtures |
| PLA-CF | Carbon-filled PLA with rigid, matte printed surfaces | Lower-temperature FDM processing; wear-resistant nozzle advised | Heat resistance remains limited by PLA matrix | Cosmetic prototypes and dimensional mock-ups |
Technical Specifications
| Product Name | SSSray 20% Carbon Fiber PA12-CF Nylon 3D Printer Filament 1.75mm, Charcoal Black (filament PA12 z włóknem węglowym) for Lattice Supports & Mounts |
|---|---|
| Material | PA12-CF (Polyamide 12 / Nylon 12 reinforced with 20% carbon fiber) |
| Series | PA12-CF Functional Parts Series – Lattice Supports & Mechanical Mounts |
| Color / Effect | Deep charcoal black, graphite-gray undertones, opaque fine-textured matte, low sheen, non-metallic |
| Carbon Fiber Content | 20% carbon-fiber-reinforced PA12 formulation |
| Filament Diameter | 1.75mm standard; 2.85mm upon request |
| Tolerance | ±0.03mm |
| Net Weight | 1kg (2.2 lbs); 3kg / 5kg project options upon request |
| Gross Weight | 1.3kg |
| Spool Type | Plastic spool |
| Packaging | Vacuum sealed with desiccant |
| Recommended Nozzle | 0.6mm hardened steel or other wear-resistant nozzle; hardened extruder gears preferred |
| Printer Compatibility | Most open-material 1.75mm FDM/FFF printers equipped with an enclosed build space, a 280°C-rated hotend and a wear-resistant nozzle |
| Typical Applications | Lattice supports, tooling fixtures, robotics brackets, mechanical mounts, sensor holders, low-volume functional prototypes |
| OEM / ODM | Supported |
| Technical Documents | We support PA12-CF20 engineering specification discussions, applicable safety documentation and export paperwork through our technical sales team |
Recommended Print Settings
| Parameter | Recommended Guidance |
|---|---|
| Recommended Nozzle Temperature | 260–280°C |
| Usable Nozzle Range | 260–290°C after flow and layer-bond testing; never exceed printer limits |
| Recommended Bed Temperature | 60–80°C |
| Optional Bed Condition | 50–90°C with a PA-compatible adhesion layer and validated build surface |
| Recommended Print Speed | 60–100 mm/s for enclosed printers with dry filament and a suitable high-flow hotend |
| Usable Speed Range | 40–120 mm/s; match the upper end to volumetric flow, part section and layer adhesion |
| Nozzle Type / Diameter | 0.6mm hardened steel preferred; 0.4mm hardened nozzle after clog-risk testing |
| Layer Height | 0.16–0.28mm with a 0.6mm nozzle; use 0.20mm as an initial profile |
| Cooling Fan | 0–20% for body layers; raise to 20–30% for bridges after bond checks |
| Retraction | Direct drive 0.6–1.2mm at 25–35 mm/s; Bowden 2.0–4.0mm at 20–30 mm/s (tuning starts) |
| Wall Count | 3–5 perimeters for brackets and mount interfaces |
| Infill | 25–40% for tooling; 40–60% for higher-demand parts after load review |
| First Layer Speed | 15–25 mm/s |
| Bed Adhesion | Textured PEI or PA sheet with nylon-compatible glue / release layer; add a 5–10mm brim as needed |
| Moisture Preparation | Dry at 80°C for 10–12h in a suitable dryer with a temperature-rated spool; 70°C for at least 12h is the lower-temperature option |
| Enclosure / Feeding | Enclosure recommended; print directly from a dry box, avoiding tight filament bends |
Print Optimization Guide
| Item | Guidance |
|---|---|
| Lattice Supports | Use 3–5 walls and orient the main load path along the deposited filament when practical |
| Mounting Holes | Print pilot holes where appropriate; drill or ream critical fits after cooling and conditioning |
| Matte Surface Definition | Run 60–100 mm/s for productive internal features, using 40–60 mm/s outer walls and 0.20mm layers for consistent charcoal-black texture |
| Bed Adhesion | Use a clean nylon-compatible surface, adhesion aid and 5–10mm brim for long mounting bases |
| Humidity Control | Dry before printing; keep active spool feed under 20% RH where controlled dry storage is available |
| Carbon Fiber Abrasion | Use a 0.6mm hardened nozzle; inspect drive gears and avoid sharp filament-feed bends |
| Layer Bonding | Use minimal cooling and validate Z-direction strength in representative coupon or part tests |
| Functional Qualification | Check creep, fit, fastener torque and service-temperature exposure in the final assembly |
Printer Brand Starting Settings
| Printer Brand | Nozzle | Bed | Speed | Notes |
|---|---|---|---|---|
| Bambu Lab X1 Carbon | 260–280°C | 65–80°C | 60–100 mm/s | Enclosed; fit a 0.6mm hardened nozzle and feed from a dry box |
| Bambu Lab P1S | 260–280°C | 65–80°C | 50–90 mm/s | Install a hardened nozzle and hardened extruder gears for abrasive PA12-CF use |
| Prusa CORE One+ | 265–280°C | 70–80°C | 50–90 mm/s | Use a wear-resistant 0.6mm nozzle and a PA-compatible sheet in the enclosed build space |
| Creality K1C / K1 Max | 260–280°C | 70–80°C | 50–90 mm/s | Use an installed or upgraded hardened nozzle; keep the K1-series bed at or below 100°C |
| Anycubic Kobra S1 | 260–280°C | 65–80°C | 50–90 mm/s | Enclosed; fit a wear-resistant 0.6mm nozzle for carbon-fiber nylon |
Our starting profiles put extrusion consistency first: run each model with dry filament, a hardened nozzle and a reliable first layer, then raise throughput to suit its hotend and part geometry. Keep every machine within its rated temperature limits.
Performance Characteristics
We develop SSSray PA12-CF20 for rigidity-focused brackets, lattice structures and reliably packed engineering-filament programs. We discuss SSSray-specific technical targets directly with your engineering team.
| Characteristic | Engineering Reference | Practical Note |
|---|---|---|
| Carbon Fiber Loading | 20% CF in the PA12 base | Our rigidity-focused grade supports lattice ribs, sensor mounts and precision fixture designs |
| Diameter Control | 1.75mm ±0.03mm stated tolerance | We manage dimensional consistency for smooth filament feeding and repeat-order production |
| Printed Surface | Opaque charcoal black; fine matte graphite-like texture | Low-gloss appearance emphasizes lattice geometry and visible mounting faces |
| Processing Window | 260–280°C nozzle; 60–80°C bed; 60–100 mm/s | We recommend a controlled 0.6mm hardened-nozzle profile for productive engineering output |
| Moisture & Drying | 80°C for 10–12h with a temperature-rated spool and dryer | Dry-box feeding helps preserve surface definition and steady extrusion through long print runs |
| Mechanical Design Focus | 3–5 walls; 40–60% infill for demanding mounts | We guide buyers on rib orientation, fastener interfaces and consistent print profiles for functional assemblies |
| Tensile Strength | 86 ± 6 MPa | We align our custom SKU qualification with your target load case |
| Flexural Modulus | 5,800 ± 300 MPa | We help buyers assess rib geometry, infill and part orientation |
| Heat Deflection (HDT) | 175 ± 3°C | We discuss your operating temperature and mechanical loading |
Ask our team to discuss acceptance criteria for your SSSray PA12-CF20 order.
Applications
| Application | Application Focus | Practical Notes |
|---|---|---|
| Lattice Supports | Weight-conscious support geometries | Use continuous load paths and qualify thin ribs against bending and layer separation |
| Mechanical Mounts | Sensor, camera and machine mounting points | Account for bolt preload, local stress concentration and insert geometry |
| Assembly Jigs | Inspection fixtures and positioning aids | Keep critical datums accessible for post-processing and dimensional inspection |
| Robotics / UAV Prototypes | Brackets and non-flight-critical housings | Check dynamic loading, vibration and service-temperature limits before deployment |
| Industrial Tooling | Low-volume holders, grippers and custom adapters | Use repeatable orientation and documented profile settings across production batches |
| Technical Product Demonstrators | Charcoal-black display prototypes with functional geometry | Matte surface creates a coherent look across supports, frames and mounted assemblies |
Storage Guide
- Store unopened 1kg spools in their vacuum bag with desiccant, protected from heat and direct sunlight
- Dry at 80°C for 10–12h in a temperature-rated dryer and spool setup; use at least 12h at 70°C when a lower drying temperature is required
- Feed filament directly from a sealed dry box; target below 20% RH for controlled storage and long print runs
- Reseal partial spools immediately after printing and replace saturated desiccant
- Run an extrusion and first-layer check after storage or moisture exposure before printing critical mounts
OEM / ODM Services
We build PA12-CF20 supply programs for wholesalers, importers and engineering-focused private labels. Our team coordinates neutral 1kg plastic spools, custom logo labels, branded cartons, artwork, alternative spool formats, selected diameter options and color development. Share your market, label language, annual forecast and target part; we will organize an engineering sample, finalize the packaging artwork and reserve production capacity for your order. Explore our filament qualification program for a structured route from trial prints to volume purchasing.
MOQ Reference: Neutral packaging from 50 spools; OEM packaging typically 500–1,000 spools, depending on artwork and packing scope. Request volume pricing for 3kg/5kg project formats and 2.85mm supply.
Quality Control
- We match incoming PA12 resin and carbon-fiber grades to the custom PA12-CF20 production order
- We monitor extrusion diameter and ovality against the 1.75mm ±0.03mm filament specification
- We inspect charcoal-black color depth, fine matte texture and uniform spool winding
- We control moisture handling and check representative extrusion appearance during production
- We inspect vacuum-seal integrity, desiccant packs and SKU labels before carton packing
- We match carton counts, lot identification and export labels to the shipment documents
Certifications & Technical Documentation
- Custom PA12-CF20 Technical File: Our technical sales team supports procurement specifications, engineering print profiles and application discussions for the 20% carbon-fiber grade
- Safety Documentation: We coordinate the applicable SDS and export handling documents with each engineering-filament order
- RoHS / REACH Requirements: We work with your purchasing team on the relevant documentation and arrange specified compliance testing as part of the order program
- Third-Party Inspection: We welcome customer-appointed inspection arrangements for samples, packing and shipment readiness
- Export Paperwork: We prepare order, labeling and batch-identification details for smooth wholesale and private-label deliveries
Frequently Asked Questions
What is the minimum order for Charcoal Black PA12-CF20?
Neutral packaging starts from 50 spools. OEM and private-label orders typically start from 500–1,000 spools, depending on label, carton and spool customization. Send your annual forecast for a tailored quotation.
Which 3D printers can process this PA12-CF filament?
We recommend enclosed 1.75mm FDM/FFF printers with a 280°C-rated hotend, a hardened 0.6mm nozzle and a nylon-compatible build surface. Our starting profiles cover Bambu Lab X1 Carbon, upgraded P1S, Prusa CORE One+, Creality K1C/K1 Max and Anycubic Kobra S1.
Can I use it for structural lattice supports and mounts?
Yes. We develop this 20% carbon-fiber PA12 option for rigid lattice supports, machine brackets, tool fixtures and non-safety-critical mechanical mounts. For repeated-load designs, we recommend 3–5 walls, load-aligned ribs and proper fastener interfaces, followed by a fit and function trial on your actual assembly.
Can you supply this grade with my private label?
Yes. We offer neutral packs, custom logo labels, branded carton artwork and project-based spool options. Our team can plan samples, packaging approval and production scheduling for your PA12-CF product line.
Can we qualify samples before a bulk order?
Our sales team arranges engineering-grade qualification samples directly through the contact page. Verified B2B buyers may receive up to three complimentary spools, with freight paid by the recipient. Tell us your printer, nozzle and target lattice or mounting part so we can prepare a focused trial.
Do you have TDS, SDS or RoHS / REACH documents?
We support custom PA12-CF20 procurement with engineering specification discussions, applicable safety documentation and export paperwork. Share your destination and import requirements with our team; we will coordinate the document package and any requested third-party inspection within your supply program.
How should we dry and print the 20% CF nylon?
Dry at 80°C for 10–12h with a temperature-rated spool and dryer, then feed from a sealed dry box. Start with a 260–280°C nozzle, 60–80°C bed and 60–100 mm/s print speed. Our 40–120 mm/s tuning range lets high-flow machines balance productive infill with precise outer walls; use a hardened 0.6mm nozzle and a nylon-compatible build surface.
What are the lead time and payment terms?
Standard orders are planned for 7–15 working days; custom programs generally require 15–25 working days. Our regular terms are 30% deposit and 70% before shipment, with FOB Ningbo or EXW quotations.
Source 20% PA12-CF Filament for Your Next Functional-Parts Program
Bring us your target lattice supports, industrial mounts or distribution requirements. We will quote bulk Charcoal Black PA12-CF20 supply, coordinate qualification samples and plan a private-label solution around your market.



Related products
-

SSSray PA12-CF 10% Carbon Fiber Nylon 3D Printer Filament 1.75mm – Graphite Black for Functional Mounting Frames (نايلون 12 معزّز بالألياف الكربونية)
-
SSSray Carbon Fiber PLA (PLA-CF) 3D Printer Filament 1.75mm in Oxblood Red – filamento PLA con fibra de carbono rojo – for PCB Fixtures & Adjustable Holders
-
SSSray PLA-CF 1.75mm Carbon Fiber 3D Printer Filament, Espresso Brown | 탄소섬유 PLA 필라멘트 | for Drone Frames & Tube Clamp Mounts
-
SSSray 1.75mm PLA-CF 3D Printing Filament, Midnight Navy Carbon Fiber PLA – カーボンファイバー入りPLAフィラメント – for Tooling Clamps & Pulley Brackets